Getting Your Head Around the Portatest II
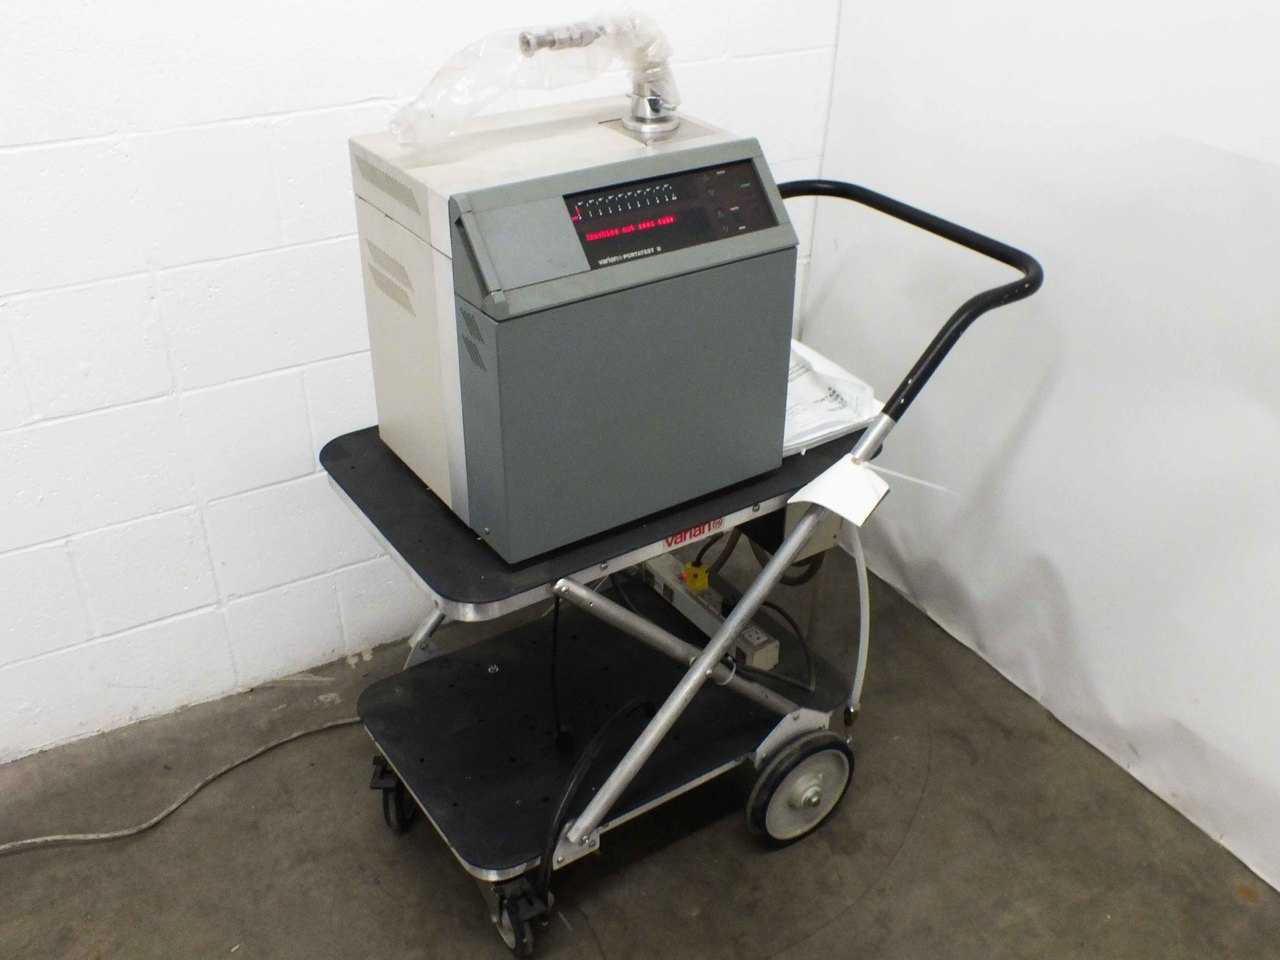
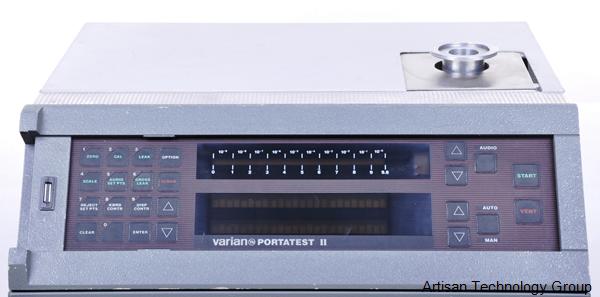
You pick up a Portatest II leak detector and it does exactly what you tell it to do, assuming you actually read the manual before pressing start. The device runs pressure decay testing, which is basically pressurizing a part, isolating it, and watching to see if the pressure drops over a set window. It sounds simple until you try it on a casting with porosity and start questioning your life choices. The unit itself is compact, usually sits on a bench or cart, and connects to a test fixture through tubing. You set your parameters—test pressure, equalization time, test time, and the decay limit—and it handles the rest. The display shows real-time pressure and tells you pass or fail after the cycle completes. That's the outline. The devil is in the setup details that most people gloss over.
Portatest Ii Leak Detector Operation Manual
Most copies of the manual you find floating around online are PDFs scanned from the original paper version or re-uploaded versions that someone skimmed through once. The legitimate ones cover the same core sections: safety warnings, unboxing and inspection, pneumatics connections, software navigation, test parameter setup, calibration procedures, and troubleshooting error codes. If you're looking for the download, search for it through the manufacturer's support portal or authorized distributor pages. Third-party sites host it too, but the file versions can vary in quality. A lot of users just wing it without the manual though, which is how you end up with bad test data. Here's the thing nobody emphasizes enough: the equalization phase matters more than the actual test phase. When you connect the Portatest to your part, there's always a volume mismatch between the regulator line and the test cavity. You have to let the pressure stabilize before the meter starts counting decay. Skip or rush this and you'll get false fails on good parts. I learned this the hard way on a batch of aluminum housings where every single unit flagged as leaking. Turned out the equalization was set to 2 seconds and the thermal equilibrium wasn't reached before testing kicked in. Bumped it to 8 seconds and the yield jumped from zero to ninety-seven percent. That's not a manual typo, that's just physics.
What Actually Happens During a Test Cycle
The sequence goes like this. First, the unit equalizes pressure between the supply line and the part. Then it isolates the part by closing valves. After that, it monitors pressure decay over the programmed test window. Finally, it compares the measured decay against your set limit and displays the result. The whole thing can run in anywhere from five seconds to a couple minutes depending on your parameters. You need to pay attention to the compensation or reference channel if your unit has one. This is a sealed reference volume that runs parallel to the test part and accounts for temperature changes in the environment. Without it, ambient temperature swings will throw off your readings. A shift of even a few degrees Celsius during a production run can look like a leak when there isn't one. I've seen operators miss this on a winter morning when the shop hadn't warmed up yet, running tests on cold parts while the reference channel stayed at room temperature. The results were all over the place until they matched the part temperature to the reference. The decay limit setting is another area where people make mistakes. You want it tight enough to catch real defects but loose enough to account for normal thermal and elastic variation in the part. A limit that's too aggressive will flag everything. A limit that's too loose will let bad parts through. The manual walks you through how to establish a baseline by testing known good and known bad parts, but a lot of shops skip that step and just pick a number out of thin air. Don't do that. Run at least thirty samples of good parts and thirty of deliberately leaky parts to calibrate your limits properly.
Get the Full Details

Common Problems and How to Fix Them
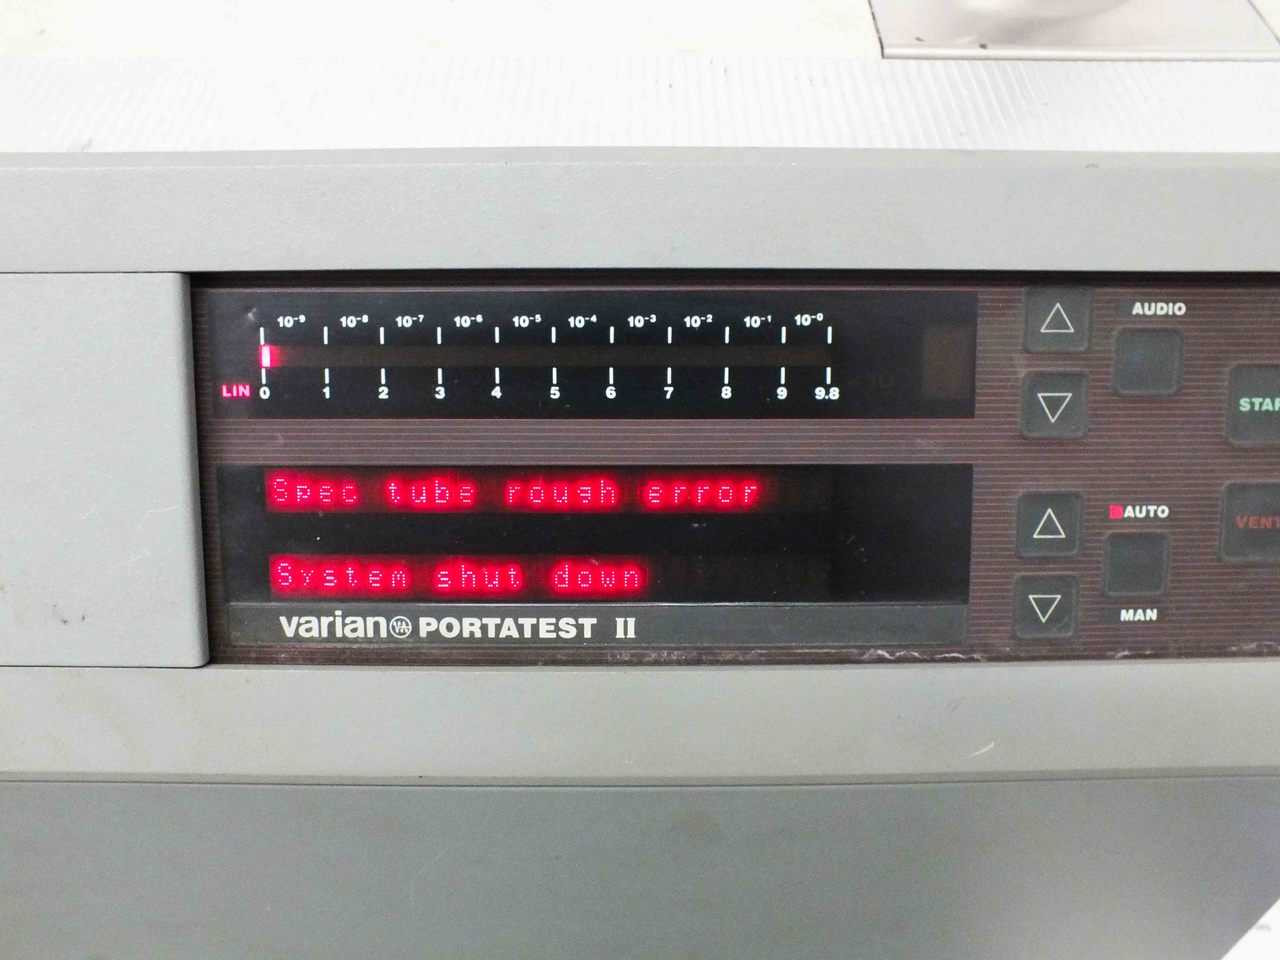
Error code issues show up more often than people expect. The most frequent ones relate to sensor faults, valve malfunctions, or pressure expected levels. If you're seeing repeated sensor errors, check the connections first. The pressure transducer cables can loosen over time, especially if the unit gets moved around a lot. I've had the problem where a loose connector caused intermittent false leak readings, and it took me two days to realize it wasn't the part design at all. Just a rattled cable. Another issue that comes up constantly is inconsistent results between shifts or days. Temperature is usually the culprit. The Portatest compensates for temperature, but only within a certain range. If your shop runs hot in summer and cold in winter, or if the test area is near a door that gets opened frequently, you'll see drift. The workaround is to run a warm-up cycle before testing starts and let the unit reach thermal stability. Twenty minutes is usually enough, but in practice I found that thirty minutes gave me better consistency on sensitive parts. Seal and fixture leaks are a separate category. Sometimes the problem isn't the part, it's the test fixture. I tested what I thought was a leaky casting for an entire afternoon, replaced seals, adjusted pressures, everything. Turned out the O-ring on the fixture itself was worn and leaking into the atmosphere. Once I swapped that, the part tested fine. Always do a block-off test with a sealed cap instead of the part to verify your fixture isn't the source of decay.
Calibration and Maintenance
Calibration shouldn't be something you think about once a year. The pressure transducer and valves on the Portatest II drift over time, especially with heavy use. Run a calibration check weekly at minimum. The manual covers the procedure, but the short version involves connecting a certified reference standard and verifying the reading matches within tolerance. If it doesn't, you adjust or send it in for service. Maintenance is straightforward but often neglected. Check your tubing for cracks or wear. Inspect seals and O-rings regularly. Keep the air supply clean and dry. Moisture in the lines causes all sorts of problems, from erratic readings to valve sticking. I use a basic filtration setup upstream of the Portatest and change the filters on a schedule instead of waiting for symptoms to appear. It costs almost nothing and prevents most of the headaches I used to deal with. The display and keypad can get finicky if you spill liquids on them or expose them to excessive dust. Keep the unit covered when not in use and wipe it down regularly. I learned that one after a part program got corrupted because conductive residue built up on the connections. A quick cleaning with isopropyl alcohol fixed it, but it wasn't pretty figuring out what happened.
When the Portatest Isn't the Right Tool
There are scenarios where a pressure decay tester like the Portatest II just won't cut it. Very small leak rates in the micropascal range often require bubble tests or vacuum chamber methods instead. The Portatest is great for moderate leak detection, maybe in the range of roughly one hundred microns and above depending on part volume and test pressure. Below that and you're chasing noise. Parts with large internal volumes relative to the leak path can also be problematic. The decay signal gets spread thin across the volume, making it harder to distinguish a small leak from normal thermal variation. In those cases, mass flow testing or helium sniffing might be more appropriate. It's not that the Portatest is bad, it's that it has limits and you need to know where those limits are before you trust the results. I also ran into an edge case where testing a flexible rubber part caused false failures. The part itself expanded under pressure and then contracted slowly, mimicking a leak signal. The Portatest couldn't tell the difference between material relaxation and actual leakage. What worked was pre-conditioning the parts by cycling them through pressure three times before testing, which stabilized the material behavior. That's not in the manual, by the way. That was something I figured out after wasting a week trying to adjust test parameters.
If you need more detail on specific error codes, parameter ranges, or alternative test methods, the manual covers most of it. Just make sure you're reading a current version. Some of the older revisions had slightly different procedures for calibration that don't apply to later firmware updates. Check the software version on your unit and match it to the manual revision before you follow any procedure verbatim.