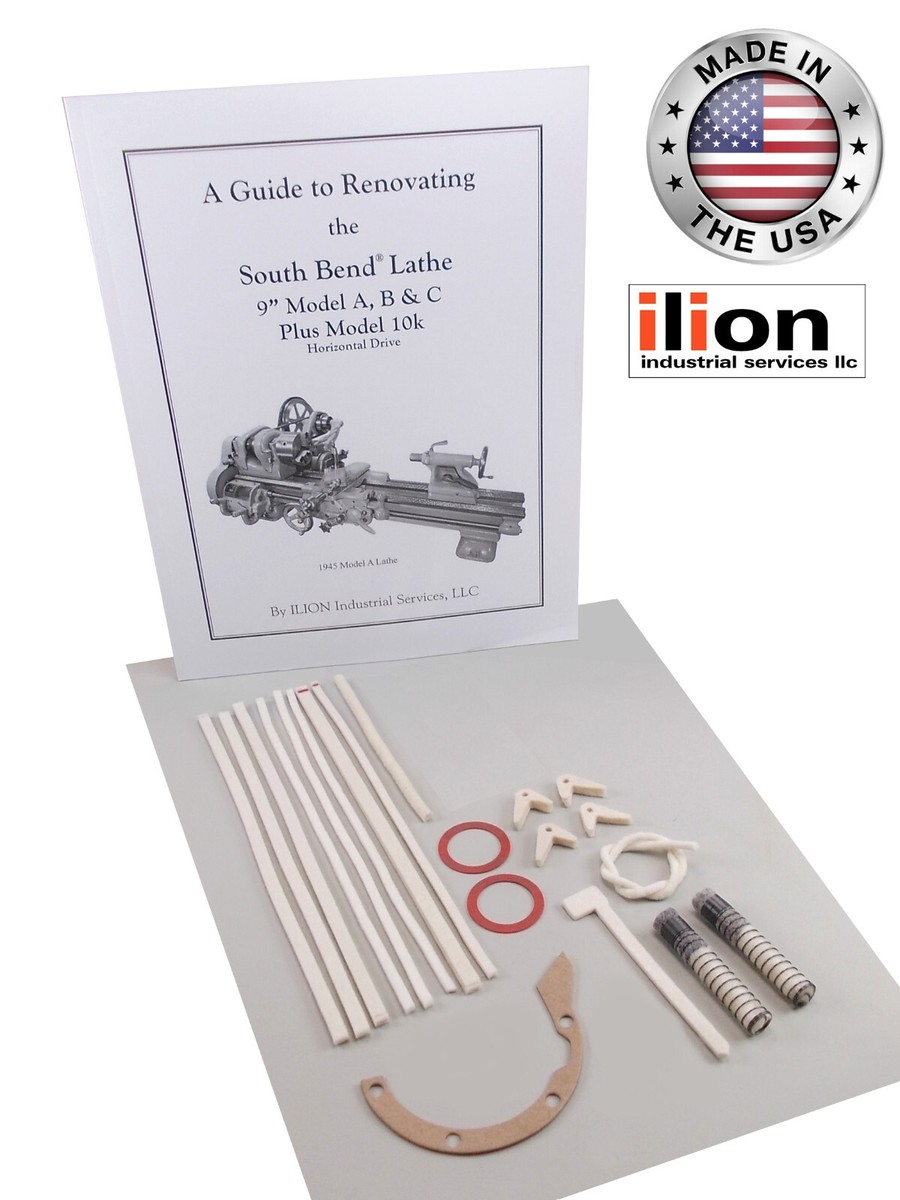
Getting a South Bend Lathe Back on Spec
You don't rebuild these lathes because you enjoy the work. You do it because the machine has been producing sloppy parts for years and you've run out of patience. South Bend lathes, particularly the 9-inch and 10-inch models, were built to last well past their owners' lifespans. The problem is that most of the wear happens in places that aren't immediately obvious. By the time you notice chatter or taper, something inside the headstock has been slipping for a while. A Rebuild Manual For South Bend Lathe gives you the blueprints, but it won't tell you which fastener is stripped when you're three hours into teardown and your hands are already covered in old grease. I've gone through this process on at least a dozen machines. The manual is essential, but the real knowledge lives in the gaps between the drawings.
Where the Rebuild Manual For South Bend Lathe Falls Short
The official South Bend documentation is decent for assembly sequence, but it assumes the parts are in their original dimensions. They never will be. The real insight from any credible rebuild resource is learning what tolerances matter and which ones you can safely ignore. Cross-slide backlash under .002 is worth addressing. The way the tailstock quill rotates around its axis barely matters unless you're doing precision alignment work. I once spent an afternoon wrestling with the compound slide cross-fever mechanism on a 9-inch model because the manual didn't account for a common modification from the 1970s. Someone had replaced the original gib with a flat brass shim, and when I followed the rebuild steps exactly, the compound would lock up the moment I tightened the retaining screw. The fix was to mill the shim down by .015 and add a second shim underneath it for preload instead. That detail doesn't exist in any published manual. You learn it the hard way.
Headstock Rebuild: The Part That Determines Everything
The headstock is where most rebuilds either succeed or fail. The three-speed gear train on a classic South Bend uses a cluster gear setup with sliding gears and dog clutches. What people often miss is that the backlash between the main shaft gear and the layshaft gear is not adjustable in most configurations. If you hear a whine that changes pitch under load, the issue is worn gear teeth, not loose bearings. When I tore down a 1968 Model 9A, the main spindle bearings were still sitting in their original seats with barely any play. But the gear train behind them was completely shot. The cluster gear's sliding dogs had rounded over from years of engagement under load. This is a failure mode the manual doesn't warn about because South Bend didn't anticipate it. The workaround is to check the dog clearance before you even pull the headstock cover off. Use a feeler gauge between the engaged dogs and the housing wall. Anything over .005 inches of clearance means you're going to have problems under cutting load, especially on medium to heavy feeds. Bearings on these spindles are typically ABEC-3 grade tapered roller bearings or precision ball bearings depending on the model year. Replacing them with higher-grade bearings won't meaningfully improve performance. The limiting factor isn't the bearing precision, it's the condition of the bearing seats in the cast iron housing. If those seats are worn or have taken a set from decades of thermal cycling, upgrading the bearings is a waste of money. The correct approach is to check seat runout with a dial indicator before removing anything. More than .001 inch of runout at the bearing seat means the housing needs attention, which usually means sleeving or sending it out for professional reconditioning.
Get the Full Details
Bed Ways: The Real Indicator of Machinability
Bed wear is the single biggest determinant of whether a South Bend lathe can hold tolerance after rebuild. The ways on these machines are box ways, not dovetails, and they wear in a specific pattern. The center of the way takes the most load from the carriage weight and cutting forces. The edges tend to stay relatively clean. What this means in practice is that a dial indicator running along the bed will show a slight valley down the middle after sufficient use, and no amount of shimming will bring it back to level across the entire length. I worked on a 1955 South Bend 10-foot model that had been used primarily for facing operations. The bed ways showed a consistent .003 inch depression in the center third of the bed length. When I tried to grind new gibbs to compensate, the carriage would bind at the center position because the gib contact was too aggressive over the worn section. The solution was to match-grind the gibs to the actual way profile rather than making them flat. It took two days of careful fitting, but the carriage now moves evenly across the entire bed with uniform resistance. This is the kind of detail that separates a functional rebuild from a precision rebuild.
Lead Screw and Chip Guard Considerations
The lead screw on a South Bend lathe is not precision-ground in the way a modern machine tool lead screw is. It's rolled, which means the thread form is consistent but the axis may not be perfectly straight. This is by design and it works fine for threading as long as the half-nuts engage smoothly. The real issue comes from chips forcing their way into the nut housing. I've seen rebuilt lathes develop backlash in the apron simply because someone didn't install the chip guard properly or left the apron cover gasket out during reassembly. When rebuilding the apron, pay attention to the half-nut engagement timing. The throw lever should position the half-nuts to close symmetrically on both sides of the lead screw thread. If one side engages a tooth or two ahead of the other, you'll get a uneven threading pattern that compounds error over multiple passes. A dial indicator on the carriage during a test cut will reveal this before you ever try to thread a part.
Tools and Time Estimates
A complete headstock and apron rebuild on a 9-inch South Bend typically takes one experienced person about 12 to 16 hours if you have the right tools and parts on hand. Without proper pullers and bearing heaters, that number doubles. Budget cutters and a digital caliper are non-negotiable. A dial indicator with a magnetic base and a good set of feeler gauges will save you more frustration than any specialty tool. Parts cost varies widely depending on whether you source from South Bend Heritage Foundation, eBay, or salvage yards. A full bearing and seal kit runs roughly $150 to $300 depending on the model. Gear sets can run another $200 to $500 if you need replacement cluster gears or dog clutches. The main bottleneck in these rebuilds is always the unknown condition of internal components. You can plan for weeks and still discover a cracked housing web or a scored bearing seat when you're halfway through disassembly. This is why getting a pre-purchase inspection from someone who has actually torn one of these apart before is worth the money. It saves you from committing to a rebuild only to find the project is no longer economically viable.
What a Proper Rebuild Actually Achieves
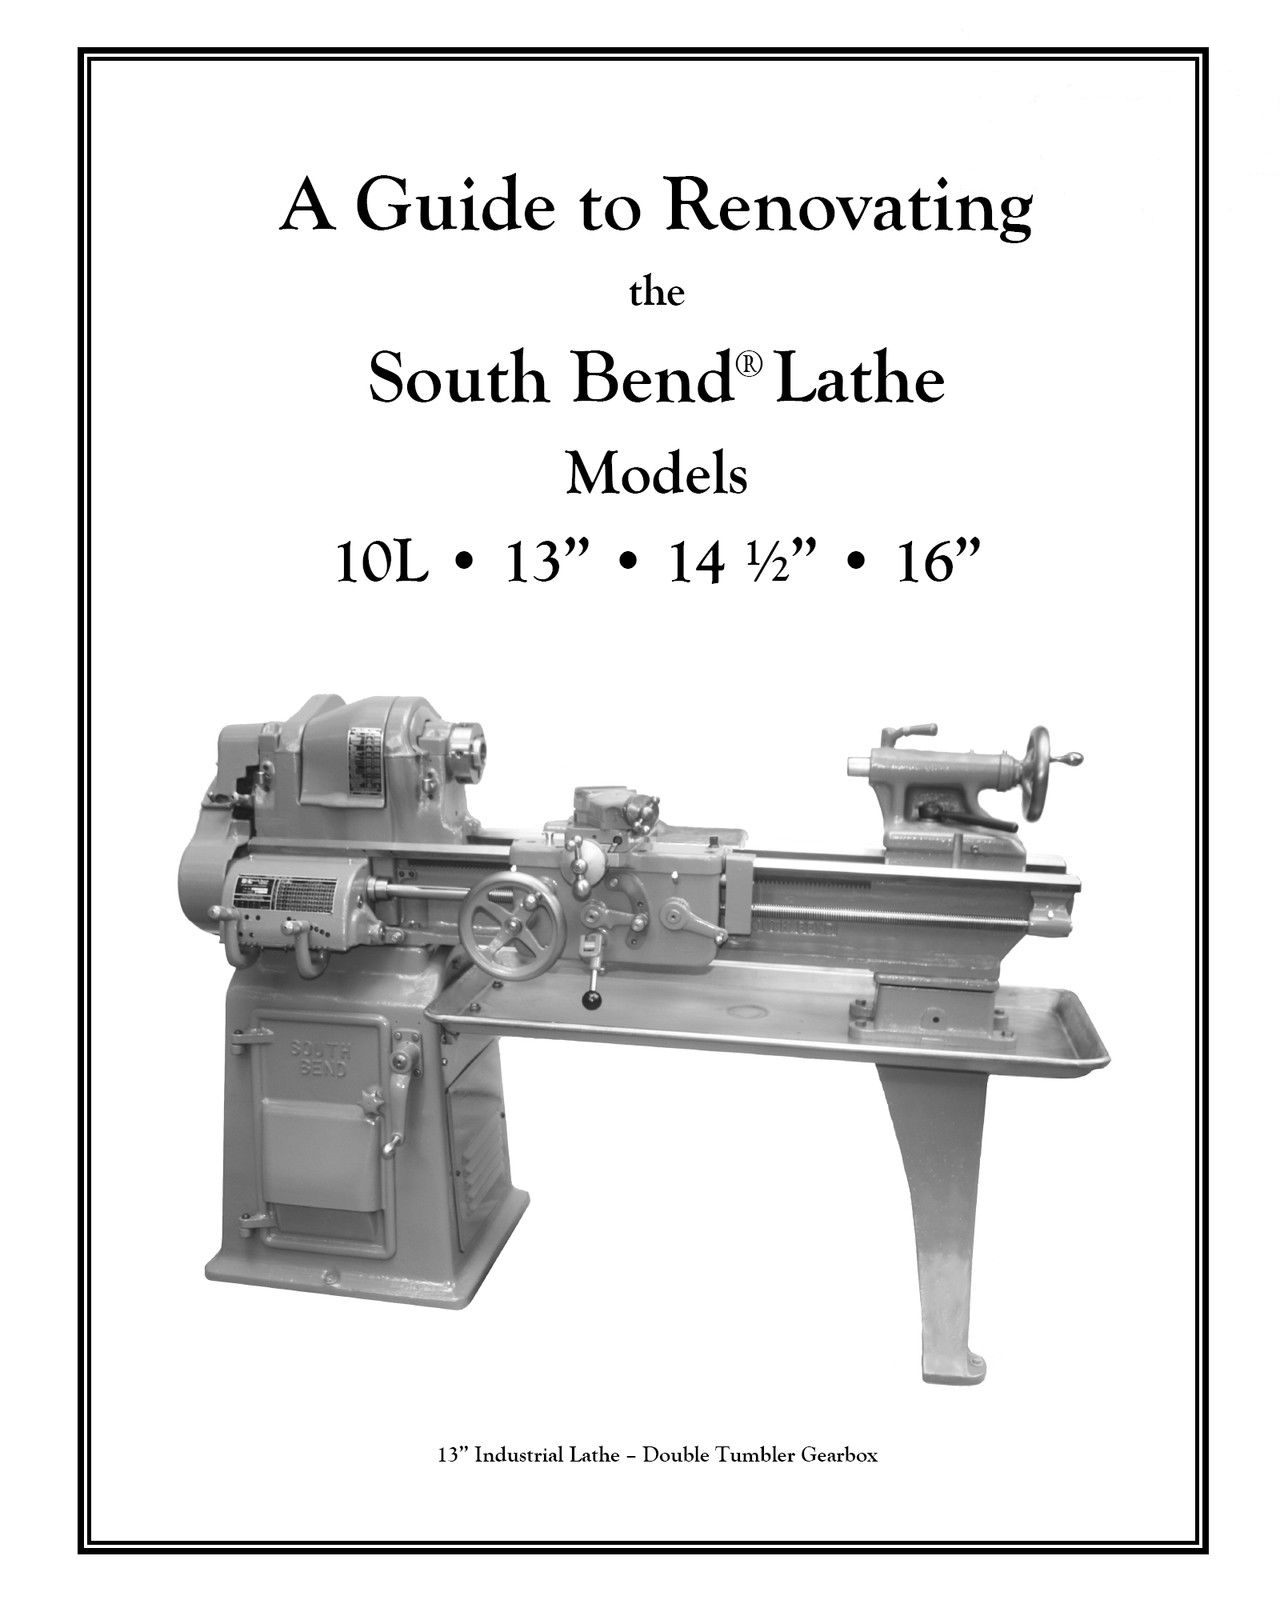
A well-executed rebuild on a South Bend 9-inch or 10-inch lathe will restore it to near-new performance for general machining work. Thread cutting accuracy will be within .002 inch per inch of travel. Facing flatness will be acceptable for most workshop applications. It will not match the consistency of a modern CNC-capable machine, and pretending otherwise leads to disappointment. The cast iron construction means thermal stability is good, but the gear trains and mechanical linkages have inherent play that no amount of adjustment eliminates entirely. If your goal is production-level repeatability, you're better off investing in a newer machine. If your goal is a reliable, accurate workshop lathe that will outlive you by several decades, a thorough rebuild is the right call. The investment is mostly in time and attention to detail, not money. Parts are available. Documentation exists. The community of people who maintain these machines is large enough that almost any problem has been solved before, even if the solution isn't written down anywhere you'll find it easily.
 Rebuild Manual and ...")