Getting Your Team Up to Speed on a Refrigeration Rack Installation
The training process is usually longer and messier than the spec sheet says it will be. I have been walking new technicians through rack systems for about eight years now, and the gap between the manual and the actual job site never really closes. What follows is a practical walkthrough of how to train someone on a typical ammonia or CO2 transcritical rack, what breaks most often, and where the real learning happens. A rack system training program needs to cover far more than just turning the machine on. The core modules are compressor sequencing, oil management, condenser fan staging, liquid separation, and the safety interlocks that keep everything from venting to the atmosphere. On a basic air-cooled ammonia rack, that means understanding why each compressor has its own oil reservoir and how the oil return circuit ties back to the central header. On a CO2 cascade setup, the high-side pressure management and the expansion valve staging are completely different animals. You cannot just hand someone a single P&ID and call it training. The first session I run is always just the safety walk-through. Not the slides. I take them to the actual skid and point out the emergency shutdown button, the relief valve discharge path, the gas detection panel locations, and the two-person rule for entering the compressor room. This takes about twenty minutes. Most people think this is obvious and skip it. Then the system trips on a Sunday night and nobody remembers where the manual shutoff is. Do not skip it.
After safety, I move to the layout review. Each rack is slightly different even within the same brand line. I have technicians who memorized the diagrams for Model R-440 but could not find the oil equalization line on Model R-445 because the manufacturer moved the port from the top of the separator to the side. Walk the physical piping together. Trace the liquid line from the receiver to the flash tank to the economizer. Trace the gas line from the suction header through the scrubber to each compressor inlet. Trace the discharge line through the oil separator back to the condenser. Three passes, thirty minutes, and they actually understand where things go instead of just nodding at a schematic.
Hands-On Training Sequence
Day one is mostly observation. Have them watch a full cold start from ambient temperature. Note how the compressors stage in, how the oil temperatures respond, how long the suction scrubber takes to accumulate liquid before the dryers come on. Typical cold start on a 200-ton ammonia rack in winter takes about forty-five minutes before the first evaporator fan receives a call. In summer, fifteen minutes. Write these numbers down so the trainee has a baseline for what normal looks like. Day two is controlled intervention. Move setpoints. Change the head pressure setpoint by ten degrees and watch what happens to the condenser fan staging and the mass flow through the expansion valves over the next twenty minutes. Change the oil differential pressure alarm and observe the compressor response. This is where the abstract becomes concrete. A technician who has only read about head pressure control will not understand why reducing the setpoint by ten degrees causes three compressors to flood with oil within eight minutes. Running the experiment takes five minutes. The understanding takes about three weeks to settle in. Day three covers fault simulation and troubleshooting. I trigger a false ground fault on one compressor contactor and walk them through the diagnostic tree. Then I block the oil return line on the number two separator with a needle valve closed partially, not fully, because a fully closed line is too obvious. A partially closed line creates a slow oil starvation that shows up as increasing differential pressure over forty minutes. That is the kind of fault that actually kills compressors in the field, and it is almost never in the troubleshooting flowchart.
Get the Full Details

A Problem I Ran Into and How I Fixed It
Last October, I trained a new tech on a hybrid ammonia/CO2 cascade rack at a distribution center in Minnesota. The system was designed for a -25F evaporator temperature space. The trainee was competent, had worked two years on direct-expansion walk-in coolers, and thought he understood rack logic. He did not, not until the first frost hit. The problem was with the cascade heat exchanger frost pattern. The CO2 high-stage compressors were cycling normally, but the ammonia low-stage suction superheat was reading twelve degrees instead of the design value of four to six degrees. The P&ID looked right. The sensors looked right. The trainee spent forty minutes checking every sensor wire before I asked him to look at the cascade pot level gauge. The liquid level was sitting three inches above the normal operating line. That meant the cascade heat exchanger was flooded, the CO2 was not flashing properly, and the ammonia suction gas was not being subcooled before it reached the evaporators. The root cause was a stuck float valve on the cascade pot that was leaking closed, slowly raising the liquid level over six hours of operation. The fix was replacing the float valve assembly, which took about two hours, but the real lesson was learning to read the cascade pot level gauge in context with the suction superheat trend. The alarm never triggered because neither parameter was in alarm territory. The superheat of twelve degrees was still within the wide band the controller accepted. The level gauge is analog and has no remote transmitter. Without the training habit of checking both simultaneously, this fault goes unnoticed until the evaporators starve and the product runs warm. I made my trainee check the cascade pot level every time he reviewed the suction superheat reading from that point forward. That habit changed how he approached every similar system afterward.
What Most Training Programs Miss
Oil management training is almost always inadequate. Technicians learn that oil returns to the compressor, but they do not learn what happens when the oil becomes diluted with liquid refrigerant. On an ammonia rack with a central oil cooler, the oil temperature drop across the cooler should be about eight to twelve degrees under normal load. If you see a drop of twenty-five degrees or more, something is wrong. Usually it is refrigerant flooding the oil cooler and washing the viscosity out of the oil. The compressor does not alarm. It just runs hotter and wears faster. Trainees rarely connect oil temperature trends to bearing life until they have taken apart three blown compressors. Another gap is suction gas density understanding. Most training treats suction pressure as the primary control variable. It is not. Suction gas density determines mass flow through the compressor, and density changes with temperature independently of pressure. On a rack serving multiple temperature zones, the low-temperature zone compressors see denser gas in cold weather even at the same suction pressure. This means higher mass flow, higher power draw, and potentially an overload trip that has nothing to do with refrigerant charge. I had a technician replace six pounds of ammonia on a system that was actually overcharged by four pounds because he chased suction pressure instead of calculating mass flow from density. The system ran worse after the recovery. Adding the correct amount back fixed nothing. He needed to understand density, not pressure.
Limitations of This Approach
This training method assumes access to an operating rack for hands-on work. That is a significant constraint. Many training programs operate out of classrooms with no live equipment, and the gap between schematic literacy and field competence remains large. Online simulations help with valve identification and basic logic, but they cannot replicate the sensory feedback of listening to a compressor unload, feeling the vibration change when oil starts to flood, or seeing the frost pattern shift on a condenser coil as ambient temperature drops. If you cannot provide live equipment access, the next best option is a detailed fault-recovery log from experienced technicians, reviewed session by session with group discussion. It is not the same, but it is better than nothing. The other limitation is time. A proper training cycle, from safety walkthrough through independent fault diagnosis, takes approximately two to three weeks of full-time exposure. Compressing this into a three-day course produces technicians who can follow procedures but cannot adapt when the procedure does not match the situation. The industry standard of a one-day orientation followed by shadowing on call rotations is insufficient for anything beyond the simplest single-compressor package units. If your operational model requires rapid onboarding, accept that the first three months will include more mistakes and longer troubleshooting times than a properly trained team would produce.
Practical Assessment Checklist
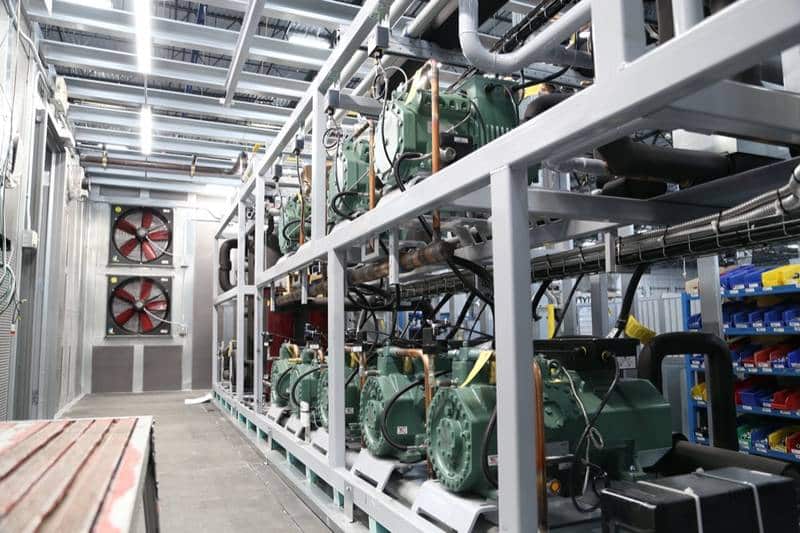
At the end of the training cycle, the technician should be able to do the following without reference material: identify every major component on a live rack by physical location, explain the oil return circuit for both the high-stage and low-stage compressors on a cascade system, interpret a suction superheat versus cascade pot level trend chart to diagnose a flooded heat exchanger, perform a controlled head pressure adjustment and predict the cascade effect on mass flow within five minutes, and execute a safe compressor isolation procedure including oil drainage and refrigerant recovery in the correct sequence. If the technician can do those five things, the training has covered the essential ground. Anything beyond that is specialization, and specialization requires additional on-jobsite experience that cannot be manufactured in a classroom. The rack systems change yearly. New controller algorithms, new variable-speed drive integration, new refrigerant blends for low-GWP compliance. Training is never finished. It just reaches a point where the foundation is solid enough to build on.