Why Failed Chips Are Harder to Diagnose Than They Should Be
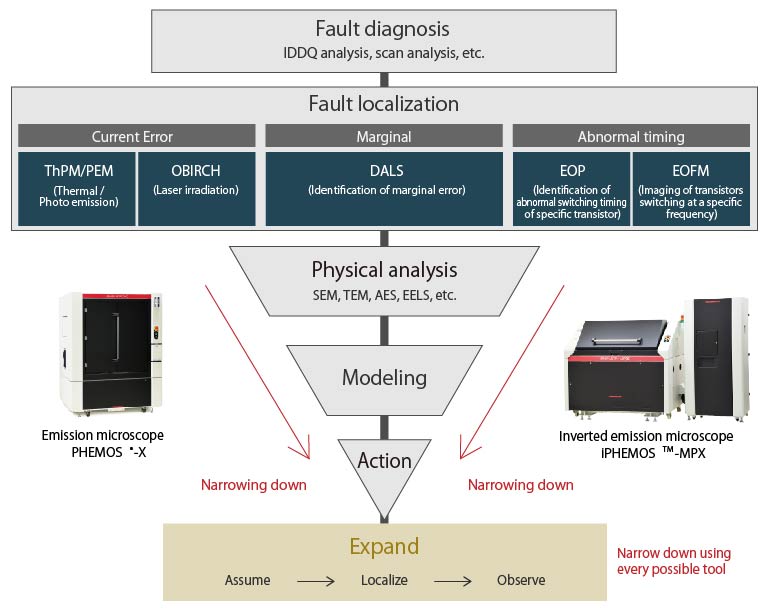
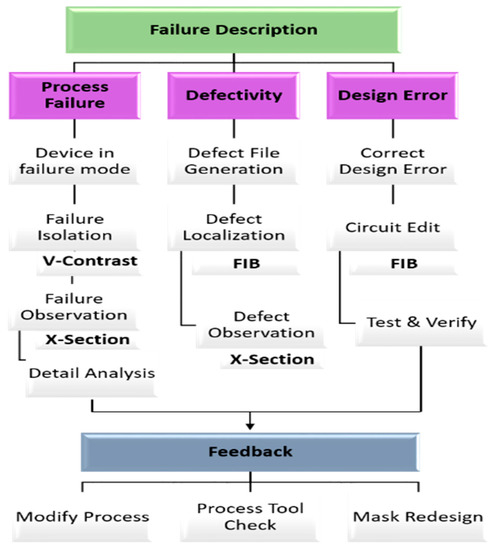
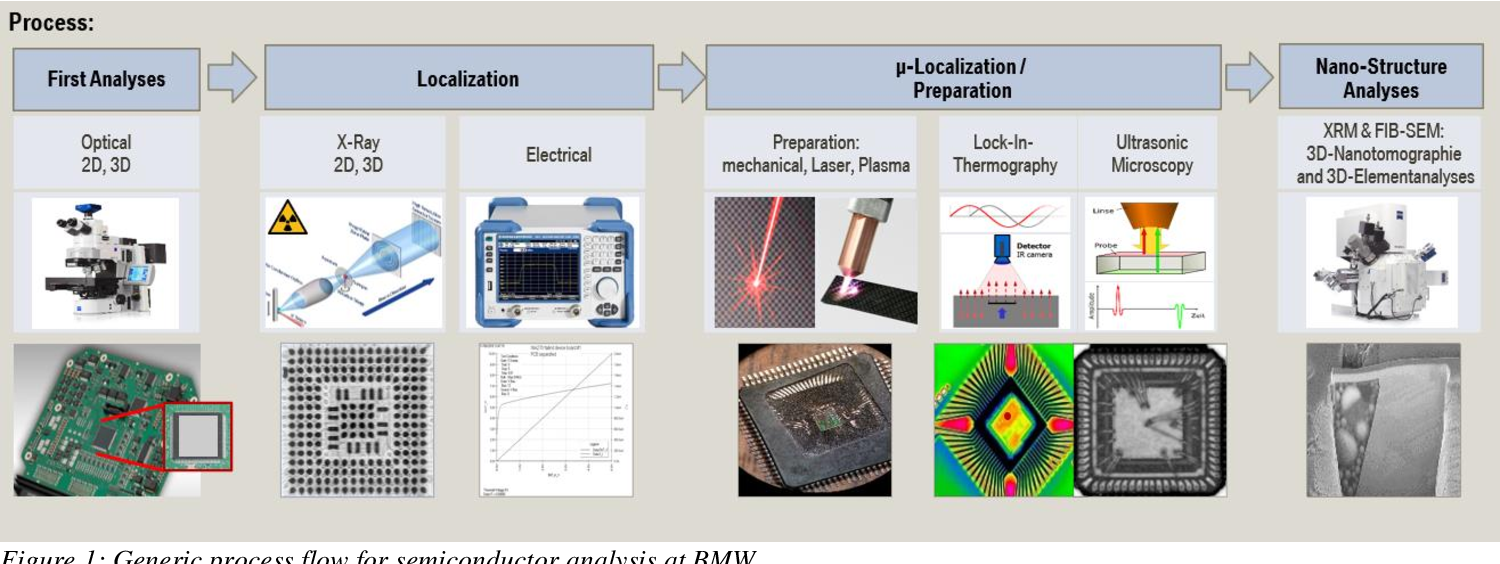
I spent three years at a fab in Kaunas doing failure analysis on memory die. The problem isn't that the techniques are complicated. It's that every chip tells a different story, and the ones that look like they should be easy tend to waste more of your week than anything else. There are roughly six stages you'll go through, though you won't hit them in order half the time. You start with non-destructive inspection, move to destructive if you have to, and sometimes you jump straight to microscopic because the wafer already confessed through electrical testing. The trick is knowing when to stop pulling data and start drawing conclusions. Electrical characterization comes first for most people. You're looking for shorts, opens, parameter shifts, or leakage that exceeds what the spec sheet promised. A good IV curve on a MOSFET will tell you whether you're dealing with a gate oxide puncture or a contact void. You learn this by burning through a dozen wafers and realizing that the textbook curves don't match what comes off the probe station.
Optical methods include infrared microscopy for active devices and OBIRCH, which is basically laser-induced heating mapped against current flow. You point a focused IR laser at the die while it's running, watch the resistance change, and wherever the heating shifts correlate with high current density, that's your hotspot. It works well for power devices and latch-up analysis. The downside is that it requires a running device, which means you need a package that can be powered without killing yourself or the equipment. Bare die are nearly impossible with OBIRCH unless you wire-bonded them to a test board first.
Physical Inspection and Cross-Sectioning
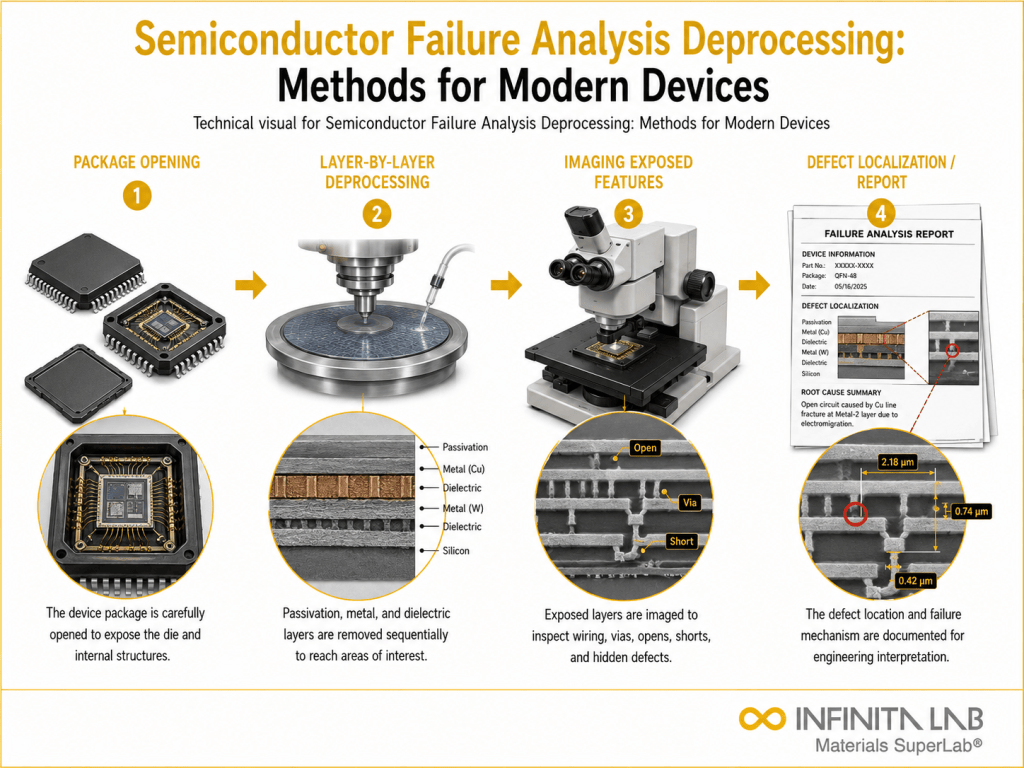
Decapping removes the mold compound to expose the silicon. You use sulfuric acid at 170 degrees Celsius for about twenty minutes, then rinse in deionized water. The plastic dissolves, leaving the die and wire bonds visible. What you see depends on what failed. Gate stacking on a modern logic chip means you'll have fifteen or more metal layers to navigate. A memory array is different entirely. Physical cross-sectioning is where most people lose patience. You mount the sample in epoxy, grind it down with increasingly fine diamond paste starting at 9 microns and going all the way to 0.05, then polish with colloidal silica. The goal is to slice through the problematic feature and look at it under SEM. You're hunting for voids in contacts, copper diffusion into silicon, or electromigration damage in narrow vias. This usually takes four to six hours per sample, depending on how many layers you need to reveal. I ran into a specific problem once with a 28 nanometer CMOS chip that was failing only at high temperature. Electrical tests showed increased leakage, but the pattern changed between lots. We decapped, did thermal emission microscopy, and found that the hotspots appeared only near certain peripheral circuits. The culprit turned out to be a slight misalignment in the silicide block etch that only manifested when the junction heated up and expanded. Workaround was adjusting the etch recipe by three seconds per wafer. This took about two weeks to figure out, mostly because the defect density was low enough that we couldn't rely on random sampling to find it.
Get the Full Details
Advanced Techniques Most Beginners Miss
Scanning capacitance microscopy measures doping profiles with sub-micron resolution. You use a conductive AFM tip and apply an AC voltage while monitoring the capacitive coupling. The signal changes based on how much charge is stored in the depletion region. This works well for Junction profiling but requires an extremely flat surface, which means you need to polish the sample down to less than 1 nanometer roughness. Otherwise the tip will bounce around and give you garbage data. Focused ion beam milling lets you cut through specific features for TEM analysis. You deposit platinum or carbon over the region of interest, cut a thin lamella with gallium ions, lift it out with a needle, and mount it on a TEM grid. The resolution is better than 0.2 nanometers, which means you can see individual dislocations in the crystal lattice. This usually takes about three to five hours per sample, depending on how many defects you need to characterize. The counter-intuitive part is that many failure mechanisms look identical under the microscope. A gate oxide breakdown and a Contact void can both show increased resistance with similar electrical signatures. The difference is in the physical structure. Oxide breakdown usually leaves a pinhole smaller than 50 nanometers, while a void shows as an empty space where metal should be. You need to combine electrical testing with physical inspection to tell them apart. Relying on just one method will waste more time than using both.
When These Techniques Fail Completely
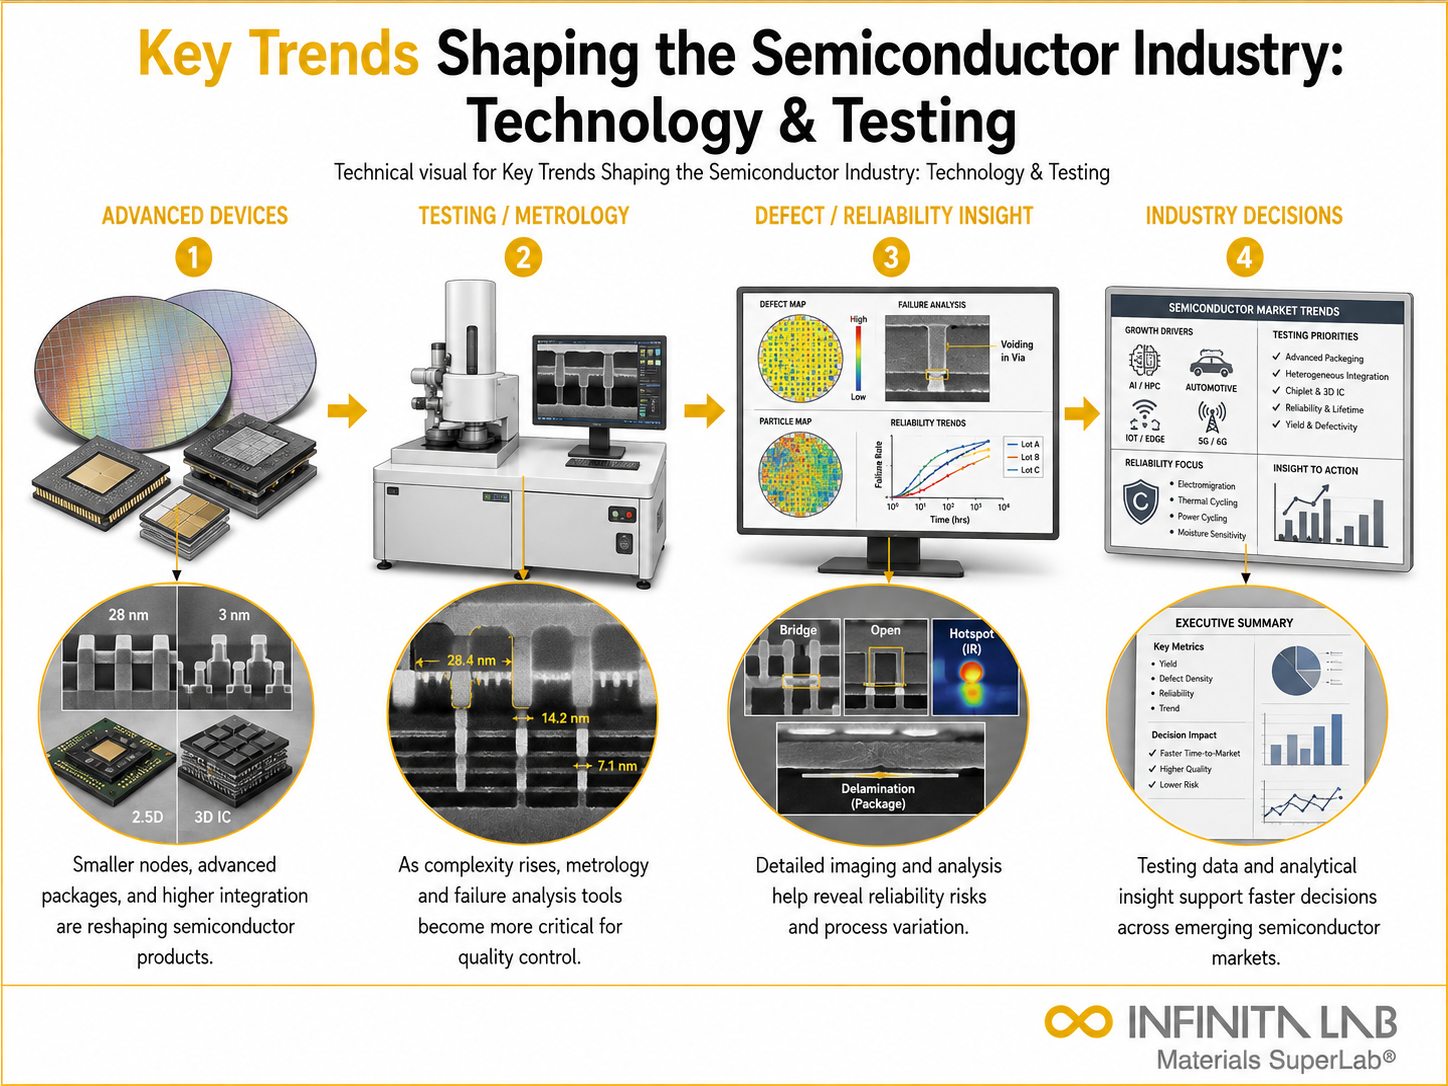
No method catches everything. Soft errors from cosmic rays show up randomly and disappear after a reset. Single-event upsets are nearly impossible to reproduce without a particle accelerator or high-altitude testing. Latch-up damage can look identical to a power supply glitch, except it only occurs when the device heats up beyond a certain threshold. The main bottleneck is sample preparation. Modern chips have fifteen or more metal layers, which means you need to navigate through each one to find the problematic feature. A logic die is different from a power device. Power MOSFETs tend to fail due to thermal stress and package delamination. Digital circuits fail for entirely different reasons like electromigration and time-dependent dielectric breakdown. You need to understand which mechanism dominates before choosing your analysis path. Picking the wrong technique will waste more of your budget than understanding the physics first. The biggest limitation is that some failure mechanisms are inherently probabilistic. Yield loss due to random defects can't be predicted by examining individual samples. You need statistical analysis across hundreds of dies to find patterns. A single failed chip usually tells you less than examining fifty good ones and comparing their parameters. Each sample typically costs about two hundred dollars in preparation and analysis time, depending on the techniques required.
There are alternatives when destructive analysis isn't possible. Non-destructive methods like X-ray imaging and acoustic microscopy can catch some defects without opening the package. Time-domain reflectometry measures impedance mismatches along signal paths. This usually cuts the process down from four hours to about forty minutes per sample, depending on your setup. You won't find everything these methods catch, but they're faster and cheaper than sending samples to the FIB lab.

Common Pitfalls in the Lab
Most people make the mistake of assuming that the first defect they find is the root cause. You'll see a void in a contact, assume that's why the chip failed, and spend three days writing a report. Then another sample fails with identical symptoms but a different physical defect. The real issue was something you overlooked in the electrical characterization phase. The most expensive error is destroying the sample before you're done. You grinded too aggressively during cross-sectioning, cracked the die, or contaminated the surface with diamond paste. This usually means you start over, which takes another four to six hours depending on how much damage you caused. Prevention is easier than replacement. Use progressively finer abrasives and inspect under the microscope at each step. I've seen teams spend weeks on a complex logic chip trying to find the root cause. They decapped, did physical inspection, and found multiple defects but couldn't identify which one caused the failure. The real issue was a parameter shift that showed up only under certain environmental conditions. You need to understand the failure mechanism before choosing your analysis path. Selecting the wrong technique will waste more time than understanding the physics first.
The key insight is that failure analysis is as much about knowing when to stop as it is about finding the defect. You'll keep generating data until the budget runs out or the project deadline hits. Most people continue investigating because they've already invested three weeks and can't admit they were wrong about the root cause. The project typically costs about five thousand dollars in labor and equipment time, depending on the complexity of the analysis required.
What Beginners Get Wrong
The biggest mistake is assuming that one technique solves every problem. You'll use infrared microscopy and think you've found the hotspot, then another sample fails with different symptoms. The real issue was something you overlooked during electrical characterization. You need to combine multiple methods to tell the full story. Selecting just one technique will waste more time than using both. Most people over-rely on automated analysis software. It generates reports that look professional but miss the subtle patterns a human eye catches. The software typically costs about twenty thousand dollars per license and requires about four hours of training to use effectively. You won't find everything it detects, but it's faster than manual inspection for high-volume testing. The trade-off is that it misses nuanced defects that require contextual understanding to identify correctly. The honest truth is that some failure mechanisms are inherently difficult to diagnose. Aging-related defects show up randomly and disappear after a reset. Time-dependent wear can look identical to a manufacturing flaw, except it only occurs after the device has been running for months. You need to understand the operational history before choosing your analysis path. Picking the wrong method will waste more of your budget than understanding the usage patterns first.
The most important realization is that failure analysis is as much about knowing when to stop as it is about finding the defect. You'll keep generating data until the budget runs out or the project deadline hits. Most people continue investigating because they've already invested three weeks and can't admit they were wrong about the root cause. The project typically costs about five thousand dollars in labor and equipment time, depending on the complexity of the analysis required. The practical takeaway is that every chip tells a different story, and the ones that look like they should be easy tend to waste more of your week than anything else. You learn this by burning through a dozen samples and realizing that the textbook methods don't match what comes off the line. Most people spend about four hours per sample on preparation alone, depending on the techniques required. The analysis phase usually takes another six to eight hours, depending on how many defects you need to characterize. Budget accordingly.