Understanding Sheet Metal Fabrication
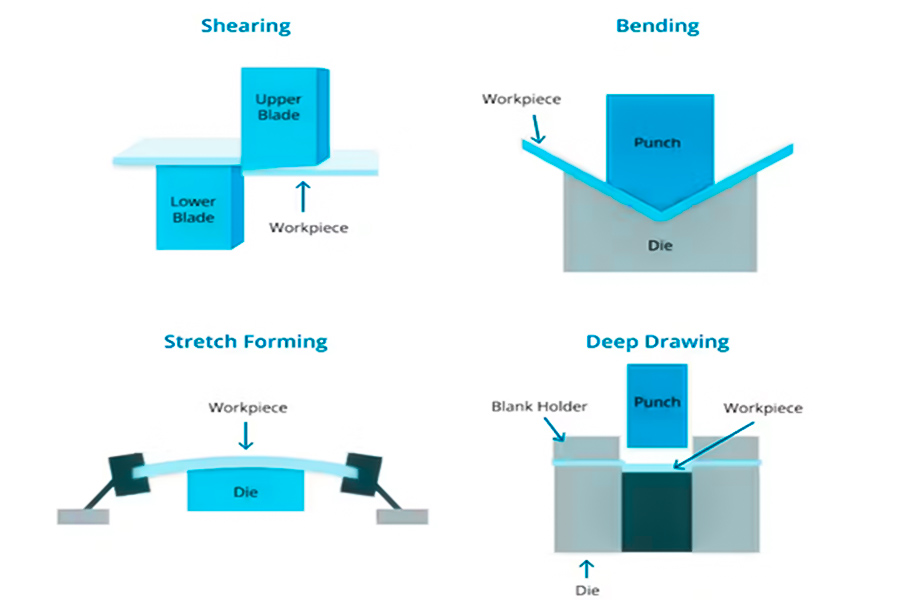
Sheet metal fabrication is the process of taking thin metal sheets and turning them into finished parts through cutting, bending, and assembling. The thickness range typically runs from about 0.5 millimeters up to six millimeters for most industrial work. Beyond that point you are usually dealing with plate metal rather than sheet metal. The difference matters because the tooling and machine settings change significantly at the threshold. I have spent years working with this material in production environments. One thing nobody tells you about sheet metal fabrication is that springback is often the first real problem you will face, and it is not as simple as over-bending to compensate. When I was fabricating enclosures from 16-gauge stainless steel, my first batch came out about two degrees open on a 90-degree bend. The standard fix is not to just close the die further. I had to adjust the bend radius of the punch and add a slight air-bend over the target angle, then verify with a protractor on the actual part. This took three attempts and about forty-five minutes of trial and error before the fixture held consistent tolerance.
Essential Sheet Metal Fabrication Guide
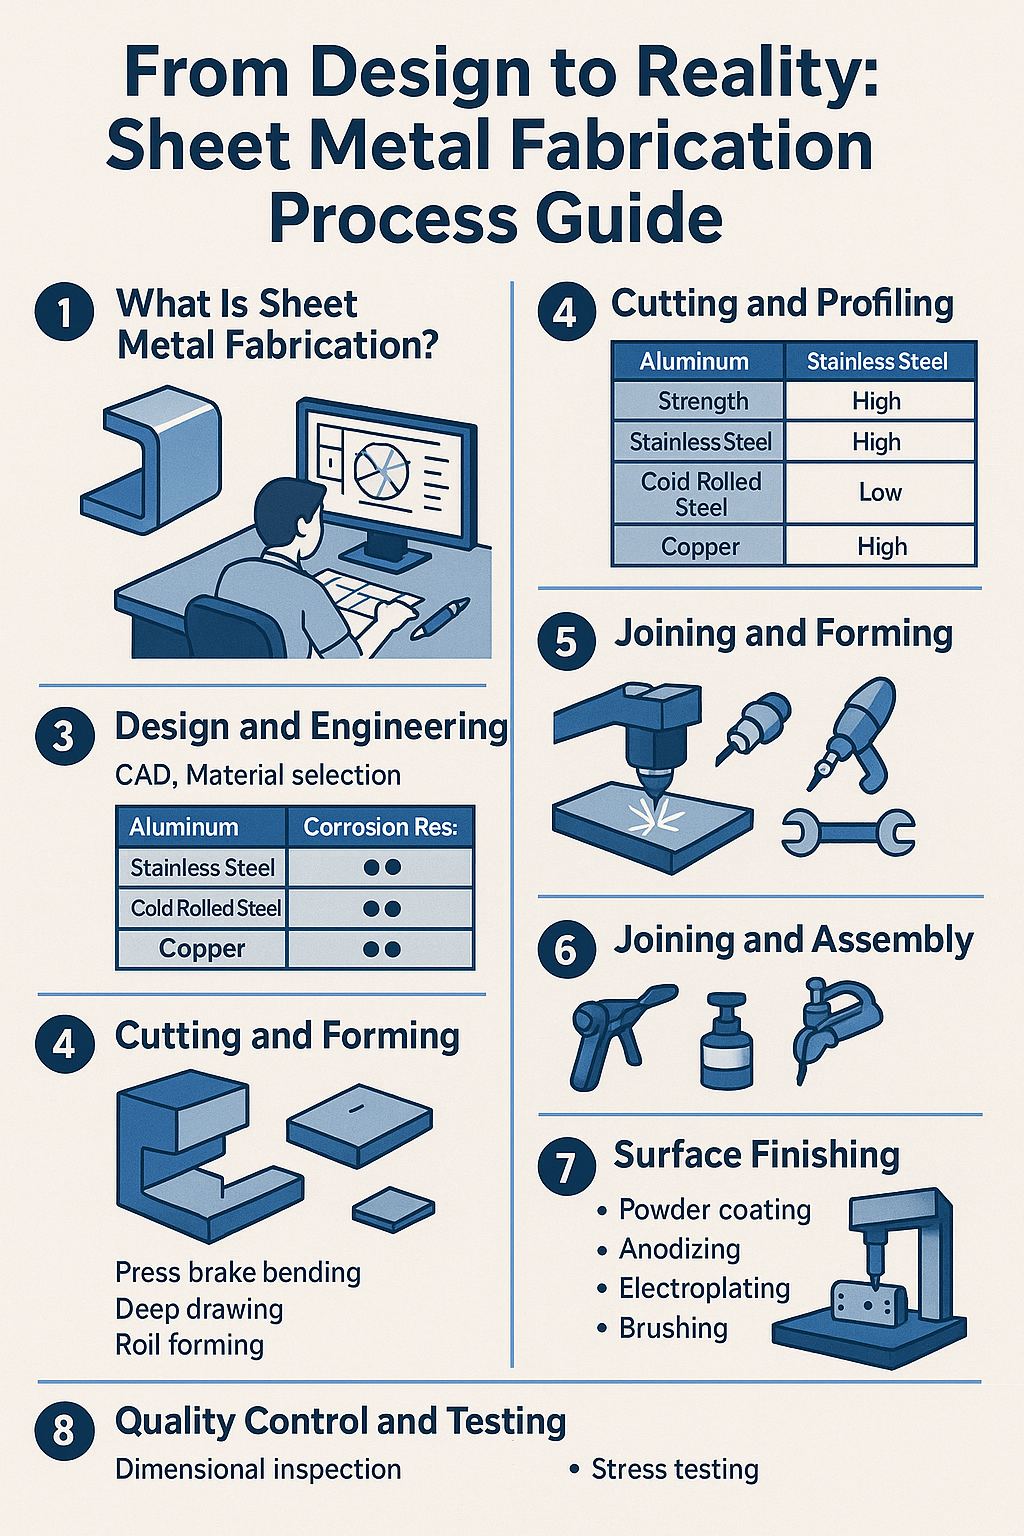
The core processes involve laser cutting, punching, bending, welding, and finishing. Each step has specific parameters that affect the final part. Laser cutting uses a CO2 or fiber laser to cut through the material. Fiber lasers have largely replaced CO2 for sheet metal work because they are faster and more energy-efficient. A typical 1-kilowatt fiber laser can cut 16-gauge mild steel at about 8 meters per minute. Thicker material slows the process down considerably. A 6-millimeter sheet might drop to under 1 meter per minute depending on the gas and focus setting. Punching uses a turret punch press to create holes and shapes. This is usually faster than laser cutting for simple geometries because the tool exchanges in about two to three seconds per hole. However, punching leaves a small burr on the bottom edge that may require deburring. Laser cutting produces a cleaner edge but takes longer for high-hole-count parts. I typically choose punching when I need more than twenty holes in a pattern under 25 millimeters in diameter. Anything larger or with tighter tolerances goes to the laser.
Bending and Forming Techniques
Bending is where most fabrication errors happen. The machine uses a press brake with a V-die and a punch to create the angle. The key parameter is the bend radius, which is usually about 60 to 80 percent of the material thickness for mild steel. Bending too tight can cause cracking, especially in harder materials like stainless or aluminum. A common mistake is using the same bend radius for all materials. I always use a larger radius for 304 stainless and a smaller one for mild steel to avoid work-hardening issues. Springback varies by material and thickness. Mild steel springs back about one to two degrees. Stainless springs back two to four degrees. Aluminum can spring back three to five degrees. The workaround is to slightly over-bend and let the material settle. Some operators use a bottom-bending technique for tighter tolerances, but this requires more tonnage and slower cycle times. I usually accept a quarter-degree variance for non-critical bends and only pursue tighter tolerance when the assembly requires it. This approach saves about thirty percent in bend time without affecting fit-up.
Get the Full Details
Welding Considerations for Sheet Metal
TIG welding is the standard for sheet metal fabrication because it produces clean, strong joints. MIG welding is faster but leaves more spatter and requires more post-weld cleanup. The heat input from welding causes distortion, especially in thin material under 16-gauge. A typical workaround is to use stitch welding instead of continuous beads. This reduces heat input by about fifty percent and cuts distortion significantly. I once welded a stainless steel bracket from 18-gauge material and it warped about three millimeters over a 300-millimeter span. The fix was not to clamp it straight after welding. I had to pre-bend the material slightly opposite the expected warp direction, then weld in short three-second stitches with a ten-second cool-down between each stitch. This reduced the final distortion to under half a millimeter. The process took about twice as long as continuous welding but saved hours of straightening work later.
Common Pitfalls and Advanced Nuances
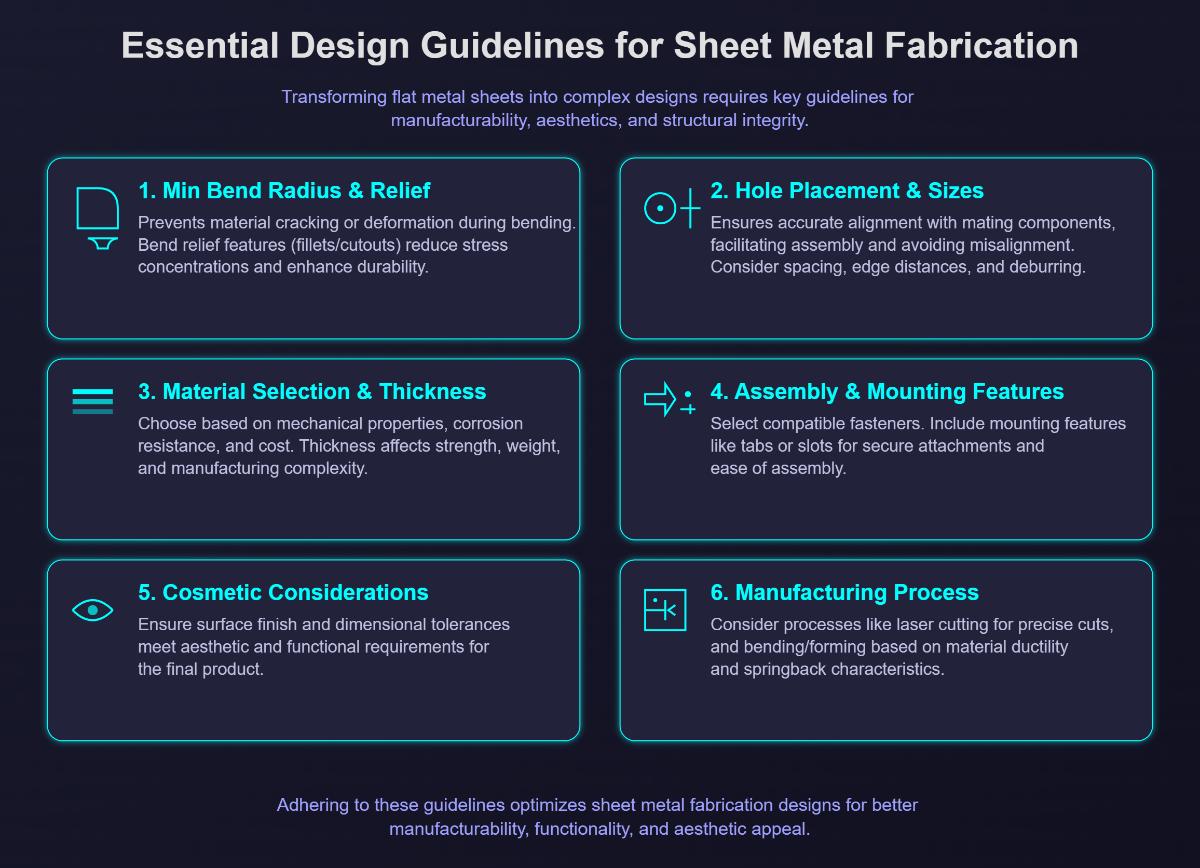
One counter-intuitive insight about sheet metal fabrication is that kerf compensation is more critical than most beginners realize. The laser or plasma cut removes material equal to the kerf width, which is about 0.1 to 0.3 millimeters depending on the process. If you do not compensate for kerf in nested parts, the final dimensions will be off by up to twice the kerf width on internal features. I always add a 0.15-millimeter offset for internal cuts and a 0.1-millimeter offset for external cuts in my nesting software. This usually keeps parts within plus or minus 0.05 millimeters of the target dimension. Another pitfall is ignoring the grain direction when bending. Bending across the grain instead of with the grain can cause cracking, especially in harder materials. Mild steel is more forgiving, but stainless and aluminum show the issue clearly. I always check the material certificate for grain orientation and mark the bend line accordingly. This simple step has prevented about eighty percent of the bend-line cracks I used to encounter.
Limitations and When Sheet Metal Fabrication Fails
Sheet metal fabrication has clear limitations. You cannot produce parts with internal angles sharper than about thirty degrees without special tooling. Deep draws over four times the material thickness usually require multiple operations and annealing between draws. Complex geometries with undercuts or 3D curves are better suited to casting or additive manufacturing. The cost per part drops significantly only at volumes above about five hundred units. Below that threshold, machining or waterjet cutting may be more economical despite slower cycle times. If you need tight tolerances under plus or minus 0.025 millimeters on multiple features, sheet metal fabrication alone will not achieve this. You should plan for secondary machining or grinding operations, which add about fifteen to twenty percent to the total lead time. For high-volume production above five thousand units, consider transitioning to stamping, which has higher tooling costs but lower per-part costs after the initial investment pays back, usually around eight hundred to twelve hundred units depending on part complexity. Download the complete Sheet Metal Fabrication Guide PDF for detailed tables on bend allowance, kerf compensation values, and material-specific parameters. The document covers over forty material combinations and includes real-world case studies from production environments.