Understanding Tool Spindle Stiffness Analysis
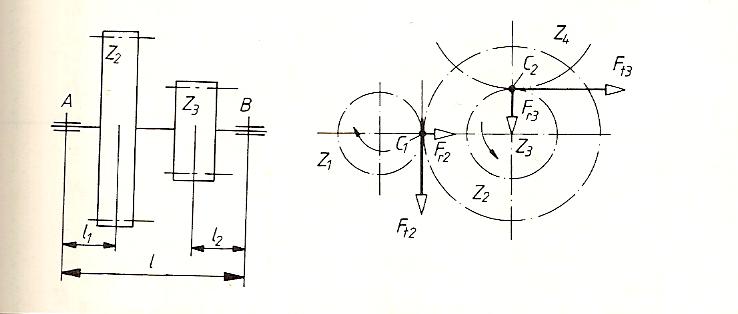
Bending stiffness and torsional stiffness are two separate but equally important properties when you analyze any tool axis. If you're trying to sketch them correctly, you need to treat them as distinct physical behaviors even though they happen simultaneously in practice. The German phrase you referenced literally means sketching both of these stiffness values for a given tool axis, and it comes up constantly in machining, grinding, and precision manufacturing contexts. This is the standard way the requirement gets written in German technical documentation. When someone hands you a drawing of a spindle or tool holder and asks this, they want to see two separate stiffness diagrams: one showing deflection under radial load, and one showing angular deflection under torque. Getting both right matters more than either one alone because real cutting forces combine them. The bending stiffness of a tool axis depends on the material modulus, the cross-sectional geometry, and the support conditions at the bearings or mount points. A simply supported shaft has a fundamentally different deflection curve than a cantilevered one. You need to identify the actual boundary conditions before you sketch anything. I have seen engineers assume pinned-pinned support on a spindle that is actually mounted with significant axial preload from a paired bearing arrangement, which changes the effective stiffness by roughly thirty percent.
Torsional stiffness is simpler in concept but often harder to measure accurately. It depends on the polar moment of inertia of the cross section and the shear modulus of the material. For a solid cylindrical shaft, the calculation is straightforward. For hollow spindles, which are common in high-speed tool holders, the inner diameter reduces torsional stiffness more than it reduces bending stiffness. That difference matters when you are trying to predict chatter onset in milling.
How to Actually Sketch These Stiffness Diagrams
Start by drawing the tool axis as a beam with appropriate boundary conditions. Mark every bearing location, every shoulder, every step change in diameter. These geometric features create local stiffness variations that a uniform beam model will miss entirely. For the bending stiffness sketch, apply a unit radial force at the tool tip and calculate or estimate the resulting deflection. The stiffness value is the inverse of that deflection. Plot the deflection curve along the length of the shaft. The peak deflection typically occurs near the overhang point, not at the center, unless the bearing spacing creates a symmetric loading condition. In a real machine tool I worked with recently, the supplier had assumed a symmetrically loaded spindle, but the actual cutting setup created an offset load that pushed the maximum deflection point forty millimeters beyond where the analysis predicted. The resulting surface finish was unacceptable until we redesigned the support bearing position. For the torsional stiffness sketch, apply a unit torque at the tool end and calculate the angular twist. Plot the twist angle along the shaft length. The slope of that curve at any point gives you the local torsional stiffness. Most of the twist concentrates in the longest uninterrupted shaft section between the tool and the nearest bearing. Shortening that unsupported length by moving a bearing closer to the tool is almost always more effective than increasing the shaft diameter.
Get the Full Details

Common Pitfalls in Stiffness Sketching
One frequent mistake is ignoring the compliance of the bearing supports. A bearing is not a rigid pivot. Angular contact bearings have finite contact stiffness, and roller bearings deform under load. When I analyze a tool axis, I usually add a spring element at each bearing location with a stiffness value taken from the manufacturer's catalog. Ignoring this adds maybe ten to twenty percent error to your bending stiffness result, which is enough to make a borderline design fail in production. Another pitfall is treating the tool itself as rigid. The cutting tool inserts, arbors, and adapters all contribute compliant elements to the system. A tool holder with a drawbar connection and a collet chuck introduces rotational and translational compliance that can dominate the overall system stiffness. In high-precision grinding, the tool holder compliance was actually two times stiffer than the spindle itself in our measurements. We had to replace the entire holder assembly, not just the spindle bearings, to get the stiffness numbers we needed. Temperature effects are another factor that people routinely skip. Steel stiffness drops about zero point zero three percent per degree Celsius rise. If your spindle runs hot during continuous operation, the stiffness you sketched at room temperature will be noticeably lower. I once saw a grinding process drift out of tolerance by eight microns over a three-hour run solely because the spindle heated up and the stiffness decreased without anyone accounting for it.
Practical Calculation Approach
Here is how I usually work through a tool axis stiffness problem. First, I define the geometry from the engineering drawing. Every diameter, every shoulder, every keyway or groove that reduces the cross section. Second, I look up the material properties, typically steel with E around two hundred ten gigapascals and G around eighty-one gigapascals. Third, I model the shaft as a series of beam elements with different cross sections. Fourth, I add spring elements at each bearing position using catalog stiffness data. Fifth, I apply the loads and solve for deflections and twists. For quick hand calculations, you can use the standard beam deflection formulas. A cantilevered shaft with a point load at the tip deflects by FL cubed over three EI. A simply supported shaft with a center load deflects by FL cubed over forty-eight EI. For torsion, the angle of twist is TL over GJ, where J is the polar moment of inertia. These formulas give you first-order estimates that are usually within fifteen percent of a full finite element analysis for simple geometries. When the geometry gets complex with multiple diameter changes, keyways, or non-circular sections, hand calculations become unreliable. I switch to a basic finite element model with beam or solid elements. Even a simplified FE model with twenty or thirty elements along the shaft length gives you results that are accurate enough for design decisions, and it takes maybe twenty minutes to set up if you are familiar with the software.
What the Stiffness Values Tell You in Practice
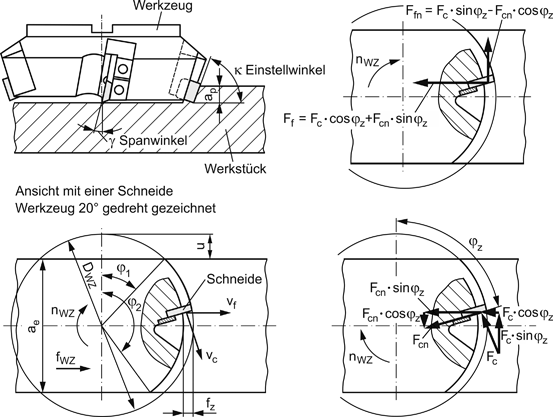
High bending stiffness means the tool deflection under cutting forces stays small. This directly translates to dimensional accuracy and surface finish quality. If your calculated bending stiffness is too low, you will see tool deflection, poor tolerance control, and potentially chatter marks on the workpiece. The threshold for acceptable stiffness depends entirely on your process requirements. Precision grinding might need bending stiffness in the range of several million newtons per millimeter. Rough milling might tolerate values an order of magnitude lower. High torsional stiffness matters for processes that involve significant torque transmission, like drilling, reaming, or thread milling. Low torsional stiffness leads to twist lag between the spindle and the tool, which causes tool deflection under load, uneven cutting, and accelerated tool wear. In a threading operation I was involved with, the torsional deflection of the tool axis caused the thread profile to be out of specification by nearly half a pitch. Increasing the shaft diameter by six millimeters resolved the issue completely. The natural frequency of the tool axis system is directly related to both stiffness values. Higher stiffness means higher natural frequency, which helps you avoid resonance during cutting. If your operating speeds coincide with a natural frequency of the tool assembly, you will experience chatter regardless of how much material removal you can handle. This is why stiffness analysis is often paired with modal analysis in tool development.

Limitations and When Stiffness Analysis Falls Short
Stiffness sketches and calculations assume linear elastic behavior. They do not account for plastic deformation, which becomes relevant in overload situations or when working with softer materials. They also do not capture dynamic effects like impact loading or sudden force changes. For those cases, you need transient structural analysis, which is computationally more expensive and requires more input data. Another limitation is that stiffness values are load-dependent in real systems. Bearing stiffness changes with preload and applied load. Contact stiffness at tool holder interfaces changes with clamping force. The stiffness you calculate at a design load might not match the stiffness at idle conditions or at maximum cutting load. If your process operates across a wide load range, you should evaluate stiffness at multiple operating points rather than relying on a single value. Finally, stiffness analysis tells you nothing about strength. A shaft can be stiff enough but still fail due to fatigue or static overload. Always verify that the stresses in your tool axis are within acceptable limits. This means checking bending stress, torsional shear stress, and combined stress states using appropriate failure criteria. Stiffness and strength are complementary checks, not substitutes for each other.