Getting Your First Injection Moulded Part Right
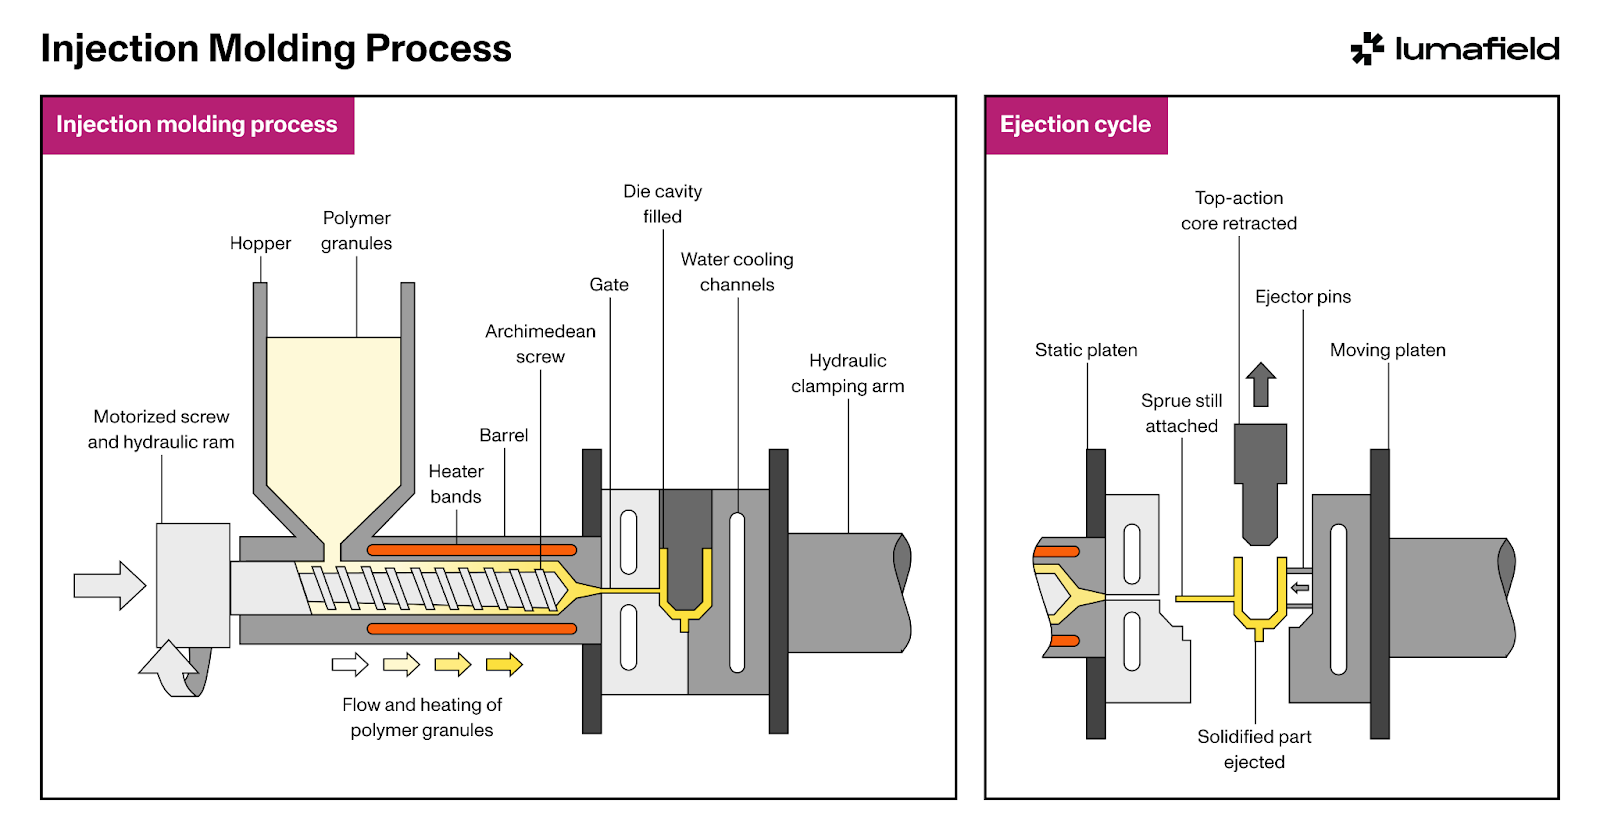
Injection moulding is one of those processes that looks completely straightforward until you try it. You melt plastic, inject it into a cavity, let it cool, open the mould, take the part out. That's the textbook version. The actual version involves dealing with warpage, sink marks, short shots, and an endless parade of parameters that all interact in ways that don't always make intuitive sense. The basic machine setup comes down to four controllable parameters: barrel temperature, injection speed, injection pressure, and cooling time. Those are your dials. Everything else is consequence. Most beginners set all four at once and then spend three days wondering why the parts look like they lost a fight with a microwave. The proper approach is to change one thing at a time and document the result. I learned this the hard way on a run of 40mm polypropylene housings about five years ago. The parts kept coming out with a slight dimensional twist and a visible sink mark on the inner face. My first instinct was to increase holding pressure. That actually made it worse. The part was overstuffed, which increased internal stress and made the warpage more pronounced. The real issue was the gate location and cooling balance, not the pressure. I moved the gate from the center to an edge position and reduced the cycle time by 20 percent. Warpage went from about 0.8mm down to under 0.15mm across the batch. Took me two days to figure out what should have been obvious from the start.
Melt temperature is probably the parameter people get most wrong. Setting it too high doesn't just waste energy. It degrades the polymer, reduces molecular weight, and weakens the part. For PP, that usually means 200 to 240 degrees Celsius. For ABS, 220 to 250. Nylon is the outlier, running around 260 to 290 depending on the grade. But the number on the barrell setting is not the actual melt temperature. It's an average. The shear heating inside the barrel during injection can add 20 to 40 degrees on top of what the display reads. If you're running high injection speeds with a viscous material like PC, the actual melt could be well above the setting. Always measure with a thermocouple if you have access to one. Cooling time is where most people lose money without realizing it. The rule of thumb is about 1 second per millimeter of part thickness. A 3mm wall gets roughly 3 seconds minimum. But that's a floor, not a target. If you cut cooling time too aggressively, the part will still be flexible when it ejects and will warp as it relaxes on the conveyor. If you overshoot, you're just burning cycle time. The sweet spot is usually 20 to 30 percent above the minimum required for ejection without deformation. You can tell by popping the part out and holding it for ten seconds. If it stays dimensionally stable, you're close. If it starts sagging or twisting, the cooling wasn't sufficient even though it ejected cleanly. Injection speed is less about how fast you fill the cavity and more about managing the flow front. Fast injection creates high shear, which lowers viscosity and helps thin materials fill complex geometries. But it also generates more heat through friction and can cause jetting, where the material shoots into the cavity like a waterfall instead of filling smoothly. Jetting shows up as wispy streaks or snake-like patterns near the gate. The fix is usually a combination of reducing speed near the gate and switching to a multi-stage profile: slow at first to establish a smooth front, then faster for the bulk fill, then slow again as you approach the end of the cavity. Slower speeds also reduce the chance of flash because there's less resistance pushing against the clamp force.
Speaking of flash, that's one of the most common problems and it's almost never about insufficient clamping force. Flash happens when molten polymer squeezes out through the parting line or around ejector pins. Usually the cause is one of three things: worn or damaged mould surfaces, contamination on the parting face, or simply too much injection pressure for what the machine can hold closed. Check the parting line first. A single speck of dust or a small nick in the steel will let flash form right through. Clean the parting thoroughly before every run. Then check if your injection pressure exceeds 80 percent of your clamping force capacity. If it does, you need a larger machine or a lower viscosity material. Another thing nobody tells you about is material drying. Some polymers are hygroscopic and will degrade if they contain any moisture when heated. Nylon is the worst offender. Acetal and polycarbonate also require thorough drying. The standard is 80 to 100 degrees Celsius in a hopper dryer for 4 to 6 hours, sometimes longer depending on the material thickness and ambient humidity. If you skip this with nylon, you'll get silver streaks in the part and a significant drop in impact strength. The parts might look fine on the surface but shatter under minimal stress. I've had batches of nylon 6/6 castings fail a basic snap test simply because the drying cycle was cut short due to a hopper dryer malfunction that went unnoticed for a full production shift. Ejector design is another area where beginners consistently cause problems. Ejector pins leave marks. That's a fact. The goal is to make those marks as small and strategically placed as possible. Too many pins and you weaken the part structure. Too few and you create uneven ejection forces that deform the part. Place pins on ribs, boss supports, or areas that won't be visible in the final assembly. For shallow parts, consider using a ejector plate system instead of individual pins to distribute the force more evenly across the part surface.
Get the Full Details
The process also has hard limits. Injection moulding is not economical for production runs below roughly 500 to 1,000 units. The tooling cost for a properly designed steel mould runs anywhere from $5,000 to $50,000 depending on complexity, cavity count, and steel type. If you need 200 parts, CNC machining or 3D printing will be cheaper and faster. Even vacuum casting with silicone molds makes more sense at that volume. Injection moulding shines at scale, where the per-unit cost drops dramatically after the initial tooling investment is absorbed. At 10,000 units, you're often looking at pennies per part for simple geometries. Part geometry matters more than most people expect. Uniform wall thickness is one of the biggest factors in reducing defects. Sudden thickness changes cause differential cooling rates, which cause warpage and internal stress. If your design requires a thick section, consider modifying it to use a rib or gusset for support instead of increasing wall thickness uniformly. Draft angles are non-negotiable. Without them, the part will stick to the mould cavity and tear on ejection. The standard is 1 to 2 degrees per side for most plastics. Textured surfaces need more, sometimes up to 3 degrees, because the texture increases friction between the part and the steel. Gate design is where the process gets genuinely tricky. The gate is the narrow channel connecting the runner system to the part cavity. Its size, shape, and location determine how the material flows into the mould and where the weld lines form. A gate that's too small will create excessive shear heating and potentially degrade the material. A gate that's too large will leave a bulky mark that's difficult to trim and may cause sink marks. For cosmetic parts, gate location should be on a non-visible surface. The gate size typically ranges from 0.5 to 2mm in thickness and 1 to 5mm in width, depending on the material and part geometry. Tab gates, fan gates, and submarine gates each have their own use cases and trade-offs that take a while to internalize.
One counter-intuitive thing about process optimization: sometimes the solution to a defect is to make the process less efficient. If you're getting weld lines that weaken a structural part, you might need to slow down the injection speed to allow the flow fronts to merge more completely. If you're getting burn marks from trapped air, you need to slow down the injection at the point where air gets compressed, or redesign the venting. The mould vents are thin channels, usually 0.01 to 0.03mm deep, machined into the parting line or integrated into ejector pins. When they're too shallow, air can't escape and gets compressed to the point of charring the plastic. I once spent a week troubleshooting burn marks on polycarbonate before realizing the vents were clogged with degraded material from a previous run. Cleaning them with a copper brush and a specialized vent cleaner solvent resolved it immediately. Post-processing is often overlooked. Parts coming out of the mould rarely have perfect surface quality. Gate vestiges need trimming. Ejector pin marks might need sanding. Dimensional tolerances might require secondary machining for precision fits. Allow 10 to 20 percent of your total production time for these steps depending on part complexity. Don't assume the moulded part is the finished part. It's usually the starting point. If you're just starting out and don't want to invest in a full machine, consider outsourcing your first runs to a job shop. They'll have the experience to flag design issues before you cut steel. A good contract manufacturer will tell you when something won't work rather than just making it and charging you anyway. The cost of their feedback is negligible compared to the cost of a redesigned mould.