Building Specs For Injection Molding That Actually Work on the Floor
The way most people build specs is backwards. They start with the CAD model and a list of pretty-printed material properties they copy from a datasheet. Then they wonder why the first tooling sample needs two weeks of adjustments. I started by reverse-engineering the process from what actually happens inside the machine. Here is how that looks in practice. You need to define a part specification before you ever talk about mold steel or cavity layouts. That means wall thickness everywhere, draft angles, cosmetic requirements, and the actual functional tolerances the part needs to hold after it cools. Not what the CAD says, what it needs to do when it is assembled. I have seen too many projects fail because the drawing called for ±0.1mm on a surface that will never actually matter, while the hiding feature that holds the assembly together was left uncontrolled. Tolerance discipline on injection molded parts starts with understanding shrinkage variation, not with slapping tight callouts on every dimension.
Specs For Injection Molding: The Practical Breakdown
A complete spec package for injection molding includes at minimum the 3D CAD data, a material grade with processing window guidance from the supplier, surface finish requirements per AMI or VDA standards, parting line expectations, gate location preferences if you have any, and a clear distinction between critical and non-critical dimensions. Add a drawing with GD&T where it matters and leave the rest alone. Every tight tolerance you specify is a cost multiplier and a process headache. Keep them where the product actually requires them. Wall thickness is where most specs go wrong. Uniform wall thickness is not just a nice-to-have rule. It is the single most important factor for dimensional stability and cycle time. When you vary wall thickness within a single part, you create differential cooling rates that produce sink marks, voids, and warpage that no amount of process tweaking will fully eliminate. I had a project once where the client wanted a ribs internal geometry that tapered from 2.5mm down to 1.2mm over a 40mm span. The shrinkage variation across that transition was causing about 0.3mm of warpage at the far end. We ended up adding a localized overpack zone near the gate and compensating in the cavity by machining 0.15mm out on the core side in that region. That bought us acceptable flatness without changing the rib design. It took three weeks and two test shots to dial in, and even then it was borderline. The right move from the start would have been keeping the rib at a consistent 1.5mm with a 0.75 ratio to the main wall. Shrinkage values from material datasheets are starting points, not guarantees. The actual shrinkage of a part depends on packing pressure, melt temperature, mold temperature, flow direction relative to the gate, and wall thickness. I use a rule of thumb that crystalline materials like PA66 or POM shrink between 1.5 and 2.5 percent, while amorphous materials like ABS or PC shrink between 0.5 and 0.8 percent. But those numbers shift significantly when you change the mold temperature by even 10 degrees Celsius. A higher mold temperature generally increases shrinkage in semi-crystalline materials because the polymer chains have more time to pack tighter as they cool. That means if your spec calls for a specific dimension and the mold runs hotter than expected, you will get a smaller part, not a larger one. That is counter to what most people assume going in.
Draft angles are another area where specs tend to be unnecessarily aggressive. The minimum draft depends on surface finish, material, and cavity texture. A polished steel cavity in PP might get away with 0.5 degrees per side. A textured surface in a glass-filled nylon could need 2 to 3 degrees per side to eject cleanly without drag marks. I once worked on a housing with a VDI 3300 E4 texture that had draft angles specified at just 0.75 degrees. The parts were sticking hard on the core side and we were getting burnish marks during ejection. We ended up adding 1 degree of additional draft and re-polishing the affected zones on the core. That fixed the sticking but we had to rework the parting line to hide the witness mark from the added draft. It was a tradeoff you could have avoided by specifying realistic draft from the beginning. Gating strategy is part of the spec whether the molder wants it or not. If you do not communicate gate location preference, cosmetic requirements around the gate, or acceptable gate vestige size, the molder will pick the easiest option for them, which is rarely the best option for your part. I always specify gate type and approximate location in the spec. Runnerless hot manifold systems are standard now for most production runs, so gate position is largely a design decision. But if you are doing cold runner work or using a family mold, you need to think about how the gate will be broken off and whether that will affect assembly or appearance. A standard fan gate on a 3mm wall part leaves a vestige about 0.3mm high and 2mm wide. That is noticeable on a Class A surface and requires secondary trimming or polishing. If the part will be visible in the final assembly, specify a point gate or a sub-gate instead and make sure your spec calls out the acceptable repair method. Cooling time is built into the cycle, and the spec should acknowledge that cooling is the dominant portion of the cycle for most thermoplastics. A rough estimate is that cooling time scales with the square of the thickest wall section divided by the thermal diffusivity of the material. For a 3mm wall in standard ABS, you are looking at roughly 2 to 3 seconds per millimeter of half-thickness, so about 6 to 9 seconds of cooling time minimum. Thicker parts scale up quickly. A 6mm wall part in the same material needs roughly 24 to 36 seconds of cooling. That is why wall thickness optimization is not just about quality. It is about economics. Every extra millimeter of wall adds significant cycle time.
Get the Full Details

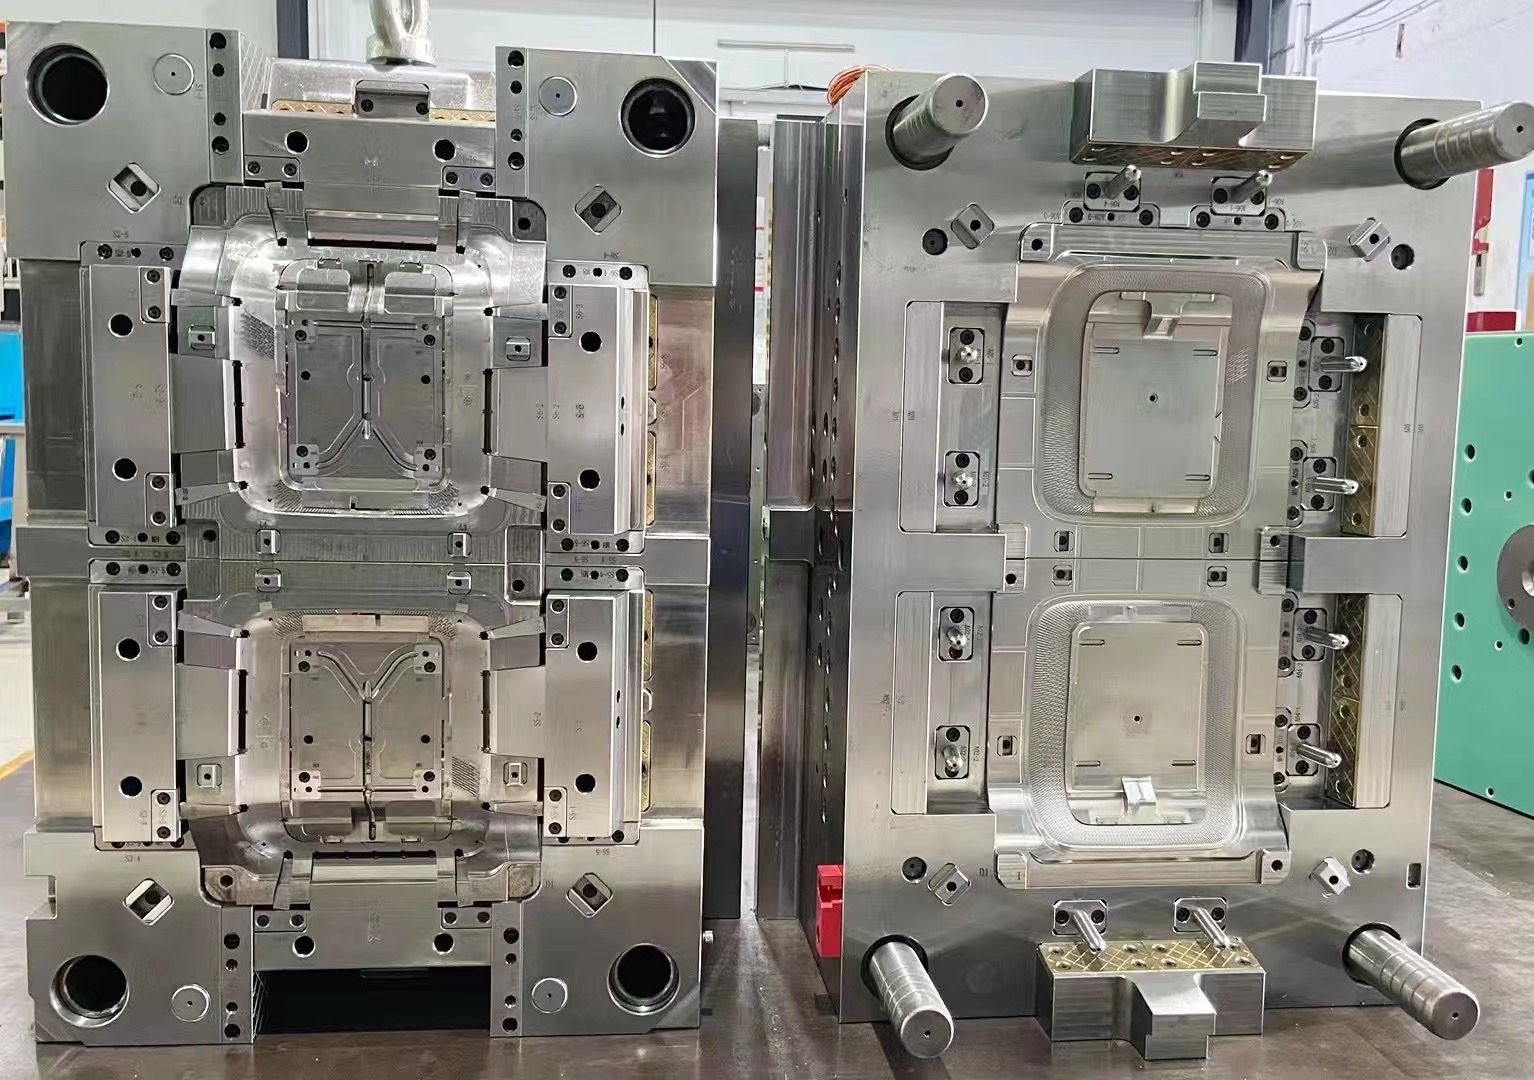
Mold steel selection is usually left to the molder, but your spec should at least call out the expected production volume and any special requirements like corrosion resistance or hardness. For a short run of fewer than 10,000 parts in a standard material like ABS, P20 pre-hardened steel is fine. For 100,000 parts or more, or for abrasive materials like glass-filled nylons, you need hardened steel, typically H13 heat treated to 48 to 52 HRC. There is no reason to overspec here. I have seen projects specify 420 stainless steel for a consumer electronics cover that will never see moisture or chemicals. That added about 15 percent to the mold cost for zero benefit. Match the steel to the actual requirements. One thing that catches people off guard is the impact of ambient conditions on spec compliance. Injection molding is usually done in climate-controlled environments, but if your spec is going to be manufactured at different facilities or in different seasons, you need to account for that. Mold temperature control units can drift. Ambient humidity affects hygroscopic materials like PA and PC. If a part spec calls for electrical insulation performance and the material absorbed moisture during processing, the dielectric strength can drop by 30 to 40 percent. Always specify material drying requirements and post-mold conditioning if the part will be used in sensitive applications. I learned this the hard way on a connector housing spec where the parts passed all dimensional checks but failed dielectric strength testing in the field. The material had been dry-processed correctly, but the storage and shipping conditions allowed moisture reabsorption before assembly. Adding a post-mold baking step and specifying hermetic packaging for storage solved it. When building your spec package, organize it so the molder can find the information in the order they need it. Start with the part function and required performance. Then give them the geometry and material. Then the tolerances that matter. Then the cosmetic requirements. Everything else is secondary. A spec that reads like a wish list of tight tolerances and perfect surfaces for every feature will get you a very expensive mold and a very unhappy molder. A spec that focuses on what the part actually needs to do will get you a mold that runs well and parts that pass inspection on the first shot.
If you want a template to work from, most tooling houses will provide a standard spec sheet, but you should adapt it to your project. At minimum, include part number, material grade, color standard if applicable, surface finish code, critical dimensions with tolerances, draft angles, wall thicknesses, gate location preference, parting line expectation, and estimated annual volume. Anything beyond that is negotiation. The molder will push back on things they consider unreasonable, and most of the time they are right. Listen to that feedback. It is free expertise.