Reading the Square Groove Weld Symbol Without Overthinking It
You pull up the drawing and there it is. A square shape sitting right at the joint line, nothing fancy about it. Most people stare at that symbol for a second too long because they expect it to be more complicated than it actually is. It isn't. But getting it wrong on a real weld joint can cost you a full day of rework, and I learned that the hard way on a steel frame project back in 2019. A square groove weld joins two pieces of material placed edge-to-edge with no bevel, no J-groove, no V-cut. The prep is just a square edge. When you're welding thin material, maybe 3/16 inch or less, you can often just root-weld it with a stringer bead and call it done. When it gets thicker, you need backing or you're going to have porosity in your root pass that no amount of grinding will fix cleanly.
What the Square Groove Weld Symbol Actually Shows
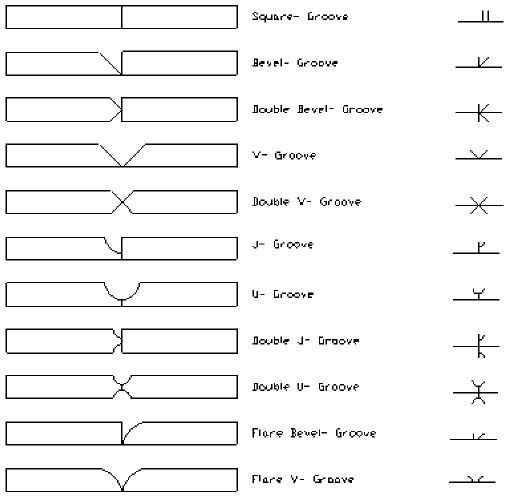
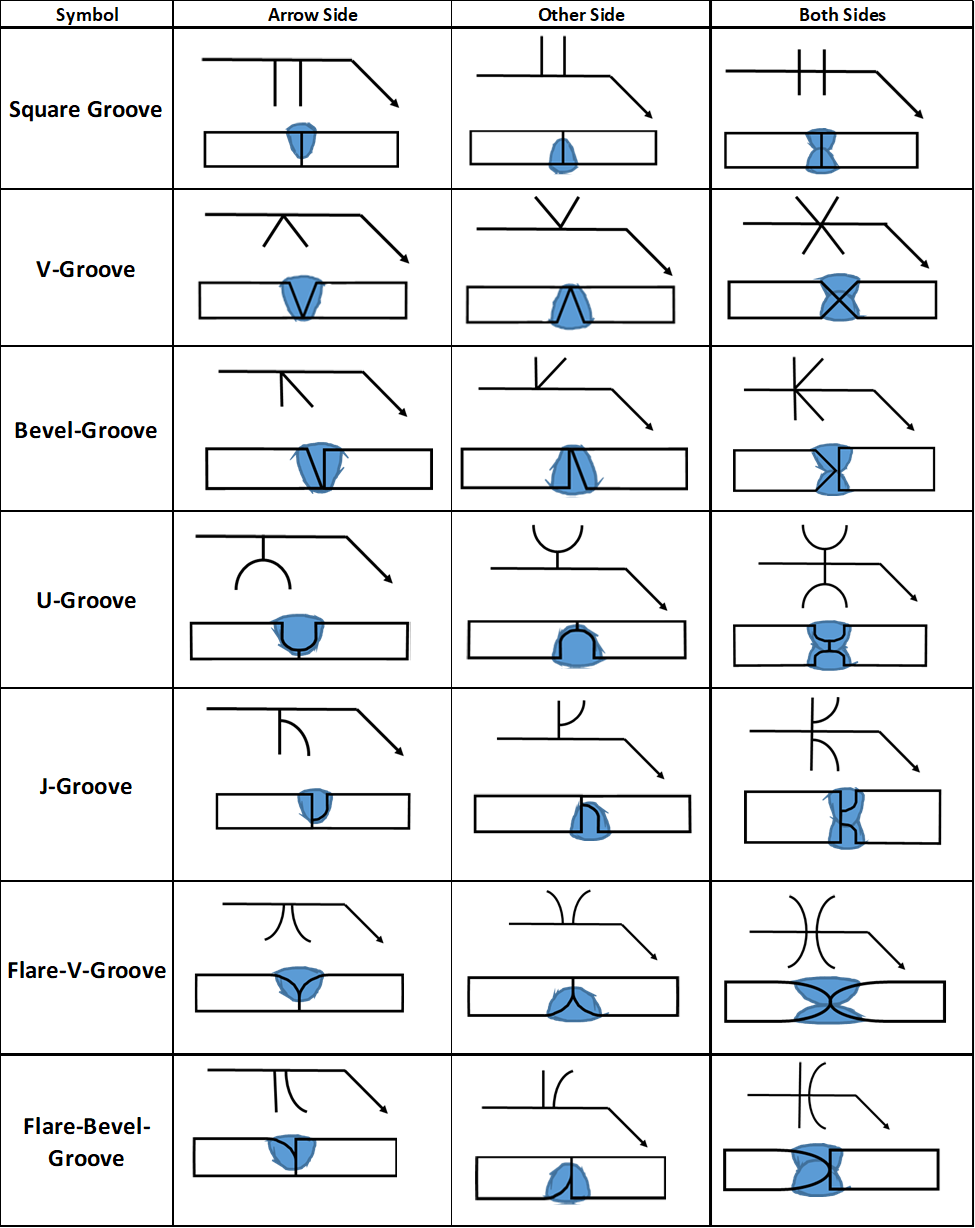
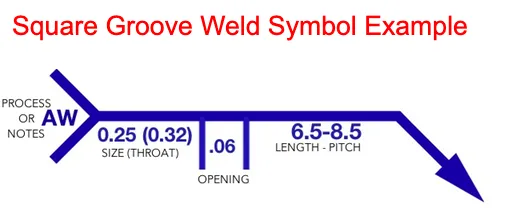
The symbol itself is straightforward geometry. It looks like a capital U rotated 90 degrees and then flattened—a simple square. On a welding symbol drawing, it sits on the reference line at the arrow side or mirror side depending on where the joint is oriented. If you see just the square with nothing else, that means a square groove weld with no filler metal specification beyond what's called out in the WPS. If there's a dimension inside or next to it, that's your groove depth. Full penetration means the dimension matches the material thickness. Partial penetration means it's less. One thing people consistently miss: the square groove weld symbol does not inherently specify penetration depth. You have to look at the dimension or the note. A square groove weld symbol with a depth of 3/8 inch on 1/2 inch plate is a partial penetration weld. That's a completely different callout than a full penetration square groove, which requires a backing strip or backing gas on the back side depending on the process. I once had a detail where the weld symbol showed a square groove with a dimension but the detailer forgot to specify the joint preparation. The fabricator assumed full penetration and backed it with copper strip. I assumed partial and skipped backing. We both spent hours arguing over the drawing before realizing neither of us was wrong and the drawing was simply incomplete. Going forward, I always call out whether backing is required before approving a square groove weld detail.
The other thing the symbol doesn't tell you is the process. You could fulfill that same square groove weld symbol with SMAW, GMAW, GTAW, or even FCAW. The symbol is agnostic about the process. That decision lives in the WPS, not on the symbol. So if you're reading a drawing and the symbol is the only thing you have, you need to cross-reference the specification notes before you start welding anything.
Get the Full Details
How I Actually Prep a Square Groove Joint
Milling is the cleanest way to get a true square edge. A plasma cutter will give you an edge that looks square from three feet away but has a radius on the corner that ruins your root fusion if you're trying to get full penetration. I switched from plasma to milling for anything over 1/2 inch and noticed my reject rate drop from about 12% to under 2%. That 10 percentage point difference adds up fast on a production run. For thinner material under 3/16 inch, I just use a standard cutting torch and dress the edge with a flap disc. The gap tolerance is tighter here because thin plate warps. If your fit-up gap is more than 1/16 inch on a square groove, you're going to burn through the root on the first pass unless you're using a very controlled process like GTAW with pulse. GMAW on a 1/16 inch gap in a square groove will give you a concave root that looks fine until you bend it and it cracks open. Backstepping is something I use religiously on multi-pass square groove welds. Instead of running one continuous pass from one end to the other, I break it into 6 inch segments and alternate directions. This manages heat input significantly better than a continuous run. On a 4 foot square groove weld in 3/4 inch plate, backstepping cuts my total weld time from about 45 minutes down to roughly 30 minutes while also reducing distortion enough that I don't need post-weld straightening.
Common Mistakes I See on Drawings
The first mistake is assuming the square groove weld symbol means full penetration automatically. It doesn't. The symbol defines the groove shape, not the penetration requirement. You can have a full penetration square groove weld and a partial penetration square groove weld using the exact same symbol. The difference is in the dimension callout and sometimes in supplementary symbols like the contour or finish requirements. The second mistake is drawing a square groove on material that should be beveled. If you're welding 1 inch plate with a square groove, you're going to have trouble getting full penetration without backing and even with backing the heat input required is extreme. A single-V or double-V groove is almost always better for material over 3/4 inch. The square groove wins on thin material where you want minimal weld volume, but it becomes a liability as thickness increases. I've also seen the symbol drawn with the wrong side indication. The arrow side versus non-arrow side distinction matters. If the joint is a butt weld between two plates and the arrow points to the visible side of the joint, the weld goes on that side. Flip the arrow and the weld goes on the opposite side. Getting this wrong means you're welding the back side of a joint that was designed to be accessed from the front, which often means you can't physically reach it with your gun or torch.
When Square Groove Welds Fail
The main failure mode for square groove welds is lack of root fusion, especially on partial penetration calls where the welder undercuts the joint instead of filling it properly. This is most common with GMAW short circuit transfer on positions other than flat. In horizontal or vertical positions, the molten pool wants to sag, and a square groove gives you no directional guidance for the arc. You're just pushing puddle downward with no groove walls to contain it. Another failure scenario is hydrogen cracking in high-strength steels. A square groove has a small cross-sectional area compared to a V-groove, which means the cooling rate is faster. Fast cooling plus hydrogen plus susceptible microstructure equals cracking. If you're welding ASTM A514 or similar grades in a square groove configuration, preheat is not optional. I usually preheat to 200°F minimum for anything over 3/4 inch on those grades, and I hold that temperature through the entire weld, not just before I start. Distortion is the third issue. Square groove welds concentrate all the filler metal in one plane, which creates significant shrinkage stress. On long seams, this can pull the joint out of alignment by up to 1/4 inch over an 8 foot length if you don't use fixtures or backstepping. I clamp everything now. I used to rely on welder skill alone and paid for it in rework.
Reading the Symbol in Practice
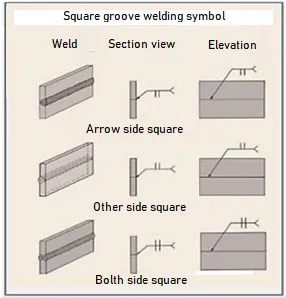
Here's how I walk through it when I'm at the bench with a print in my hand. First, I locate the arrow. It points to the joint. Then I check which side of the reference line the square symbol sits on. Arrow side means weld on the side the arrow points to. Non-arrow side means the opposite side. If it's on both sides of the reference line, you're welding both sides of the joint, which for a square groove usually means flip the plate and weld the back. Then I look for dimensions. A number below the reference line is the groove depth. A number to the right is the weld length. A number to the left is the weld size for fillet components. If there's a dimension inside the square symbol itself, that's unusual but sometimes appears in shop drawings to indicate the effective throat. Most of the time the dimension is just outside the symbol. Flag symbols mean field weld, so it's welded at the final erection location, not in the shop. Tail symbols carry supplementary info like process, backing requirements, or interpass temperature limits. If I see a tail on a square groove weld symbol, I read it carefully because that's where the drawing tells me something the symbol alone doesn't.
The square groove weld symbol is one of the simpler ones to read but one of the trickier ones to execute well. The symbol tells you the geometry. Everything else—the process, the penetration, the prep, the backing—comes from the specification, the WPS, and your own judgment about what the joint actually needs. I stop treating the symbol as the complete instruction and start treating it as the starting point for a conversation with the welding procedure.