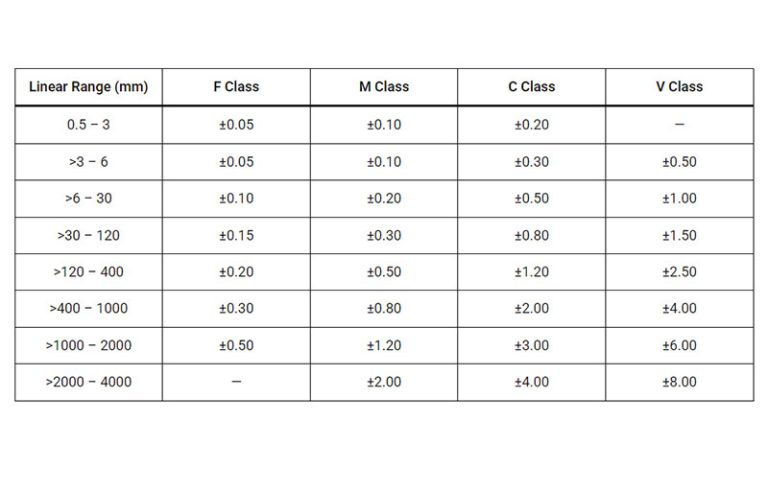
What These Charts Actually Do
The Standard Engineering Tolerance Chart is basically a lookup table that pairs a nominal dimension with a fit class and spits out the upper and lower deviation limits. You give it a shaft or hole size and an ISO or ANSI fit designation, and it tells you exactly how much leeway the manufacturer has before the part fails inspection. Nothing magical about it. I've spent years watching people misuse these charts because they don't understand what they're actually looking at. The most common mistake I see is someone treating the chart like a set of hard rules instead of a starting point for a conversation with the shop floor. A tolerance value on paper means almost nothing if the machining process can't consistently hold it.
Standard Engineering Tolerance Chart
Before diving into how to use one, you need to understand the system underneath it. Most commercial charts are based on ISO 286, which defines tolerance grades from IT01 all the way up to IT16. The IT number tells you the width of the tolerance zone, not the position of it. That distinction matters more than people realize. The position of the tolerance zone is handled separately by fundamental deviations. For holes you get letters like H, K, N, P. For shafts you get h, k, n, p. These letters shift the entire tolerance zone up or down relative to the nominal size. When you combine an IT grade with a fundamental deviation, you get a specific fit — clearance, transition, or interference. Here's something most beginners miss: the chart values change with nominal size even within the same tolerance grade. IT7 at 10mm is not the same absolute tolerance as IT7 at 50mm. The chart accounts for size steps, usually grouping dimensions into ranges like 0-3mm, 3-6mm, 6-10mm, 10-18mm, 18-30mm, and so on. If you pull a tolerance value without checking which size range your dimension falls into, you will order the wrong part. I learned that the hard way on a hydraulic cylinder bore project where the designer pulled IT6 values from the wrong size bracket and the machinist handed me parts that were out of spec by nearly double the intended tolerance.
Reading a Chart Without Making Stupid Mistakes
Find your nominal diameter on the left column. Trace across to the tolerance grade column you need. The number you land on is the tolerance magnitude in micrometers or thousandths of an inch depending on the system. For holes the fundamental deviation is usually the lower deviation (EI). For shafts it's the upper deviation (es) in most common fits. The opposite deviation is calculated by applying the tolerance magnitude. Let me give you a concrete example that I deal with regularly. You need a bearing seat on a shaft. The bearing manufacturer specifies a k6 fit for a 40mm diameter shaft. You look up the chart, find the 30-50mm size range, and grab the k6 row. The upper deviation comes out to +0.018mm and the lower to +0.002mm. Your shaft must land somewhere between 40.002mm and 40.018mm. If it goes outside that window the bearing won't seat correctly and you'll have either a loose fit that allows fretting corrosion or an interference fit so tight you crack the bearing inner ring during installation. For the mating bore, you'd typically pair that with an H7 housing fit. The H7 for the same size range gives you a lower deviation of zero and an upper deviation of +0.025mm. The hole ranges from 40.000mm to 40.025mm. Stack those together and you've got a mild interference fit that the bearing manufacturer designed for. The math is straightforward. The execution is where things fall apart.
Get the Full Details

When the Chart Lies to You
This is the part nobody puts in textbooks. Standard Engineering Tolerance Chart values assume ideal conditions: stable temperature at 20°C, proper measuring equipment calibrated to NIST or equivalent standards, and a capable manufacturing process. None of those assumptions hold on most production floors. Thermal expansion alone can eat up half your tolerance budget on aluminum components. A 100mm aluminum shaft that reads correct at 20°C will be roughly 0.013mm larger at 35°C because aluminum expands at about 23 micrometers per meter per degree Celsius. If your inspection room is warmer than standard temperature and you're checking parts without temperature compensation, you're inspecting them wrong. I had a whole batch of aluminum control arms rejected because the inspection lab was running at 26°C and the CMM wasn't temperature-compensated. We saved the lot by establishing a correction factor and re-inspecting at the corrected temperatures rather than scrapping three days of production. Gaging strategy also matters. A chart might specify a tolerance of 0.025mm on a diameter. That's tight enough that ring gauges and snap gauges become your best friend. Calipers and micrometers introduce too much variation for consistent decisions at that level. I switched an entire production line from micrometers to Go/No-Go ring gauges once and reduced our measurement-induced scrap by about forty percent in a single week. The parts weren't changing. Our ability to measure them consistently was.
There's another counter-intuitive thing about tolerance stacking that trips people up constantly. When you add multiple tolerances in a stack-up analysis, adding them linearly (worst case) gives you enormous accumulated variation that often doesn't exist in reality. Using root-sum-square statistical tolerancing usually gives a more realistic picture, but only if your processes are actually in control and centered. If your process is drifting or biased, RSS becomes dangerously optimistic. I once saw a statistical stack-up predict a 0.05mm clearance where the actual production run produced negative clearance on twenty percent of assemblies. The processes weren't centered. The math looked beautiful on paper and the parts didn't assemble. Chamfers and undercuts don't show up on tolerance charts. They're geometric features that exist outside the scope of diameter or length tolerances. You need GD&T callouts for those. A hole might be perfectly within its diameter tolerance but the chamfer depth could vary enough to cause interference with a mating part's seal face. That's not a tolerance chart problem. That's a drawing completeness problem.
Which System to Pick
ISO 286 with the hole basis system is the default for most international work. It's convenient because you can standardize on a limited set of hole sizes and vary the shaft to get different fits. That reduces tooling inventory significantly. ANSI B4.1 is still used in the United States, particularly in industries with legacy equipment or American suppliers. The values are close but not identical to ISO in every case. If you're mixing components from ISO and ANSI sources, verify the actual deviation values rather than assuming interchangeability. For really tight applications like optical mounts or precision instrumentation, you might need IT5 or IT4 grades. These require ground surfaces and careful environmental control during both manufacturing and measurement. The cost jump from IT6 to IT5 is substantial. I've seen projects where the design called for IT5 on a feature that only needed IT7 for functional reasons. The client was paying for precision they didn't need because the original equipment manufacturer specified it that way and nobody questioned it for twelve years. If your parts are large — over 500mm — or made from materials with high thermal expansion coefficients, you should consider whether a standard tolerance chart is even the right tool. At those scales, form errors, straightness, and flatness often dominate over dimensional tolerance. A plate might be within plus or minus 0.1mm everywhere you measure it but bowed enough to fail assembly. That's a form tolerance issue, not a size tolerance issue, and the Standard Engineering Tolerance Chart won't help you with it. You need geometric dimensioning and tolerancing callouts for that.