Understanding How Material Structure Dictates What Things Actually Do
I spent three weeks troubleshooting why a batch of aluminum alloy castings kept cracking at the gate. The metallurgist on the other end of the call asked me the wrong question first—yield strength, hardness, everything looked fine on paper. It wasn't until we actually looked at the grain structure under SEM that we found the problem. Columnar grains growing directly from the mold wall into the casting, each one several centimeters long, with segregation pockets of eutectic phase trapped along the boundaries. The fix wasn't changing the alloy. It was lowering the melt temperature by 40 degrees and adding a vibration source to the mold during solidification to break up those grains. That's the whole deal with Structure And Properties Of Materials in practice. You read the spec sheet, the numbers look right, and then the part fails because nobody checked what the microstructure was actually doing. The concept sounds simple when someone explains it for the first time. Atoms arrange themselves in patterns. Those patterns create grains. Grains create boundaries. Boundaries determine how a material responds when you apply stress, heat, or environmental attack to it. The trick is that the relationships aren't linear, and they're not the same across length scales. A tensile test gives you one number for yield strength. The same material can behave completely differently depending on whether you're loading it in tension, compression, torsion, or fatigue cycling. The crystal structure, the defect population, the grain size distribution—these things all interact in ways that are difficult to predict without actually measuring them.
The Foundation: What Structure And Properties Of Materials Actually Means
When people in materials science say "structure," they're not talking about a single thing. They're talking about a hierarchy that spans from angstroms to meters. At the smallest scale you have the crystal structure—that's the arrangement of atoms in a repeating unit cell. Face-centered cubic, body-centered cubic, hexagonal close-packed. These aren't just geometry exercises. They determine which slip systems are available for plastic deformation, which directly controls ductility and formability. A BCC metal like ferritic steel behaves very differently from an FCC metal like austenitic stainless steel at room temperature, even when the chemistry is similar. The difference comes down to how dislocations move through those different atomic arrangements. Moving up one level, you have the microstructure. This is where things get interesting and also where most failure analysis starts. Microstructure includes grain size and shape, the phases present, where those phases are located, whether there are precipitates and how big they are, what the grain boundaries look like chemically and structurally. A steel with a fine pearlitic microstructure will be stronger and harder than the same steel with a coarse pearlitic structure, even though both are technically the same alloy. The difference is in the spacing between the ferrite and cementite lamellae. Smaller spacing means dislocations have a shorter distance to travel before they hit an interface, which means you need more stress to continue deformation. This is the Hall-Petch relationship, and it's one of the most reliably useful equations in the field. At the macro scale you have the component-level structure. Weld zones, heat-affected zones, surface treatments, residual stress distributions, porosity, inclusions. These are the features that actually matter when something breaks in service. A lab sample machined from the center of a forging might show excellent properties. The actual forged part might fail because the surface layer has a different microstructure than the core, or because a nonmetallic inclusion is sitting at a stress concentration point. I learned this the hard way with a titanium bracket that failed after only 200 cycles in a fatigue test. The chemistry was perfect. The tensile properties were perfect. SEM revealed a ~15-micrometer alpha case layer on the surface from improper furnace atmosphere control during heat treatment. That layer was brittle and cracked at the surface, which initiated the fatigue crack. Fix was re-machining 0.5mm off the surface and tightening the argon backfill specs.
The properties side covers mechanical, thermal, electrical, magnetic, and chemical behavior. Mechanical properties are the ones most people think about first—strength, hardness, toughness, ductility, fatigue resistance, creep resistance. But "properties" in this context isn't just a list of numbers you look up in a handbook. A property emerges from the structure. You can't fully understand why a material has a certain property without understanding what's happening at the structural level. And you can't reliably predict how a property will change without knowing how the structure will change under the conditions you're exposing it to.
Get the Full Details

How I Approach Structure-Property Relationships in Practice
My workflow usually starts with the application requirements, not the material. I need to know what loads the part will see, what temperature range it operates in, what the environment looks like, what the expected lifespan is, and what failure would actually cost. Then I narrow down to candidate materials based on those constraints. After that comes the structural analysis, which is the part most people skip or gloss over. For structural analysis, I typically begin with optical microscopy. It's fast, it's cheap, and it tells you more than you'd expect if you know what to look for. Grain size, phase distribution, obvious defects, evidence of improper heat treatment or processing. A quick etch with nital on a steel sample and you can see whether you've got a proper normalized structure or whether someone baked the material in an oven that runs hot and held it there too long. Then I move to SEM with EDS for anything that isn't obvious. The SEM shows features at resolutions that optical microscopy simply can't reach. EDS tells you what those features are made of. Combined, they can identify segregations, intermetallics, contamination sources, and failure mechanisms that would otherwise be invisible. X-ray diffraction comes in when I need to know phase composition quantitatively or measure residual stress. XRD won't tell you where a crack started, but it can tell you whether your expected phase is actually present and in what proportion. I've had cases where someone claimed a stainless steel was austenitic based on the grade designation, and XRD confirmed it was mostly austenite but also had enough ferrite to cause problems in a specific environment. The grade alone wouldn't have caught that.
Hardness testing is my quick-and-dirty proxy for strength and microstructural uniformity. It's not precise, but it's fast. If I'm inspecting a heat-treated batch and the hardness varies by more than 5 HRC across the part, something is wrong with the process. Could be uneven heating, quench rate variation, or contamination on the surface affecting the thermal transfer. Whatever it is, the microstructure isn't uniform, and non-uniform microstructure means unpredictable properties. Here's a counter-intuitive point that beginners consistently miss: higher strength doesn't always mean better performance. In many applications, a moderately strong material with good toughness and good fatigue resistance will outperform a high-strength material that's brittle or sensitive to notches. I once saw a spec call for a minimum tensile strength of 2000 MPa on a shaft that operated at moderate loads with frequent reversal. The supplier delivered exactly that. The shaft lasted three weeks. A lower-strength alloy at about 1400 MPa tensile with noticeably better fracture toughness would have lasted three years. The high-strength material was hypersensitive to the keyway geometry as a stress concentrator. The structure-property relationship here isn't just strength—it's the tradeoff between strength and the ability to tolerate defects. Another thing that isn't obvious: grain size matters more at lower temperatures for BCC metals than at higher temperatures. For FCC metals, the trend is generally the opposite. Fine grains help strength across the board through Hall-Petch, but they can actually hurt creep resistance at elevated temperatures because grain boundary sliding becomes a dominant deformation mechanism. So if you're designing a component that operates at both room temperature and high temperature, you might need a grain size that's a compromise, or you might need to consider a single-crystal or directionally solidified structure if you're working in the superalley space. I worked on a turbine blade project where the solution was directional solidification to eliminate transverse grain boundaries entirely. The blades ran for thousands of hours at temperatures where a polycrystalline equivalent would have cracked within hundreds of hours.
Common Pitfalls When Working With Structure And Properties Of Materials
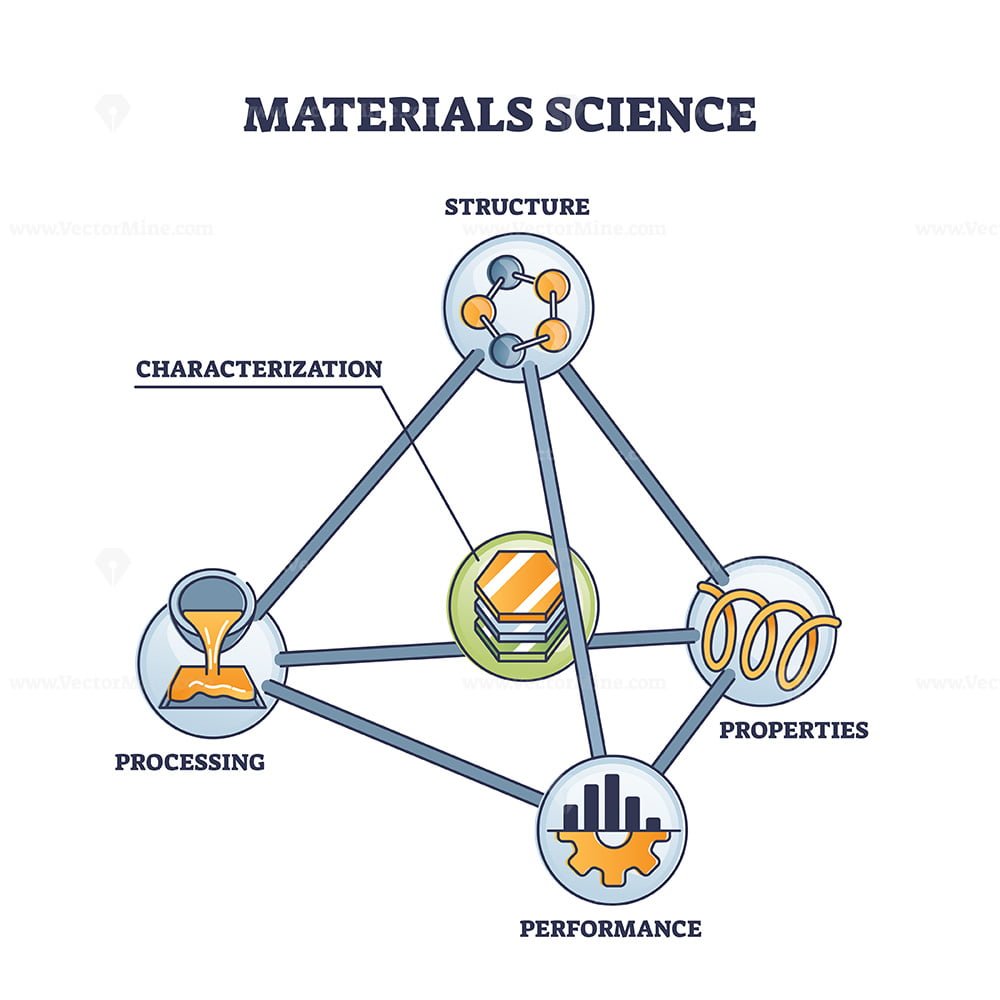
The biggest mistake I see is treating material specs as absolute rather than as targets with a known range of variation. A grade designation like 4140 or 316L tells you the chemistry window and the general processing route. It does not tell you the exact microstructure you'll get. Two batches of the same grade from the same supplier can have different grain sizes, different inclusion populations, and different residual stress states depending on how they were rolled, cooled, and cut. If your application is sensitive to any of those variables, you need to specify more than just the grade. You need to specify the processing history, the acceptable microstructural features, and the testing requirements. The second big mistake is ignoring the processing-structure-property chain. You can't change the properties without changing the structure, and you can't reliably change the structure without changing the processing. If a part is failing and you try to fix it by switching to a "stronger" material without understanding why the original material failed, you'll probably just swap one failure mode for another. In the aluminum casting example I mentioned earlier, switching to a higher-strength alloy wouldn't have helped. The cracking was a solidification defect issue, not a bulk strength issue. Lowering the melt temperature and vibrating the mold addressed the root cause. A higher-strength alloy would have been more susceptible to the same defect, not less. A third pitfall is focusing only on room-temperature properties when the service environment involves temperature excursions. Many materials undergo significant microstructural changes between room temperature and their service temperature. Precipitate coarsening, phase transformations, grain growth, oxidation scaling—these all happen over time and they all change the properties. A material that passes your qualification tests at room temperature might degrade substantially after 1000 hours at 600°C. I've seen this repeatedly with stainless steels exposed to elevated temperatures in the 500-800°C range. Sigma phase precipitation can embrittle the material significantly, and it's not something you'd detect with a standard tensile test at room temperature. You need either elevated-temperature testing or accelerated aging followed by characterization to catch it.

There's also the issue of anisotropy. Rolled plates, extruded profiles, additively manufactured parts—these all have directional properties because the processing creates directional microstructures. A rolled plate will typically have higher ductility and toughness in the rolling direction than in the transverse direction. An additively manufactured part can have columnar grains growing along the build direction with completely different properties than you'd expect from a wrought equivalent. If you're designing around isotropic material data from a handbook but your actual part has a strongly textured microstructure, your safety factors might be wrong in ways that aren't obvious until something breaks. One more limitation worth stating bluntly: computational materials design is getting better but it's not a substitute for experimental validation. CALPHAD calculations can predict phase equilibria reasonably well for well-characterized systems. Phase-field models can simulate microstructure evolution under controlled conditions. Machine learning models can find patterns in large datasets. But none of these replace actually making the material, characterizing it, and testing it. I've seen projects where the simulation predicted a desirable microstructure and the actual result was completely different because a processing parameter was off by a small amount that the model didn't account for. The tools are useful for narrowing the search space, but they can't eliminate the need for empirical work.
Practical Steps For Characterizing Structure And Properties
Start with what you already know about the material. Get the chemistry, the processing history, and the baseline mechanical properties. Then decide what questions you actually need to answer. Are you verifying that a heat treatment worked? Are you investigating a failure? Are you qualifying a new material for an existing application? Each of these has a different characterization plan. For heat treatment verification, optical microscopy is your primary tool. Prepare a cross-section, polish it, etch it appropriately for the material system, and compare what you see against the expected microstructure for that treatment. Grain size can be measured using standardized methods like ASTM E112. Phase identification can be confirmed with XRD or sometimes just with the contrast and morphology you see under the optical microscope. Hardness mapping across the cross-section will tell you whether the treatment was uniform. For failure investigation, you need to approach it differently. Document the failure mode first. Is it brittle fracture with a flat, shiny fracture surface? Ductile fracture with dimples? Fatigue with beach marks and crack propagation zones? Creep with intergranular voids? The fracture morphology tells you something about the mechanism before you even look at the structure. Then prepare specimens from the failed region and from a reference region if you have one. Compare the microstructures. Look for differences in grain size, phase distribution, presence of cracks or voids, evidence of overheating or underheating. SEM with EDS is essential here for identifying local chemical variations that might indicate segregation or contamination.
For material qualification, you need a more systematic approach. Test a set of samples under the conditions you expect in service. If the service involves cyclic loading, do fatigue testing. If it involves elevated temperature, do creep testing or prolonged exposure testing followed by property measurement. Characterize the microstructure before and after exposure to understand what changes occurred. Document everything. The qualification data is only useful if someone five years from now can look at it and understand exactly what was tested and under what conditions. I should mention that sample preparation is where a lot of people lose ground. A poorly prepared metallographic specimen can show artifacts that look like real microstructural features. Scratch depth, etch time, polishing compaction, smearing—these can all create misleading results. If you're doing your own preparation, invest time in learning the techniques properly. If you're sending samples out, choose a lab that documents their preparation methods and can show you the intermediate steps. The final micrograph is only as good as the preparation that produced it.

Where This Approach Breaks Down
There are situations where structure-property analysis hits real limits. Nanocrystalline materials are one example. When grain sizes drop below about 100 nanometers, the Hall-Petch relationship can reverse. Fine grains that should make the material stronger actually make it softer because grain boundary sliding and diffusion-mediated deformation become dominant. This inverterse Hall-Petch effect is real and it's documented, but it's also difficult to predict for any specific material system without experimental data. Standard characterization methods work, but interpreting the results requires understanding mechanisms that aren't covered in introductory courses. High-entropy alloys are another area where traditional structure-property thinking gets stretched. These materials have multiple principal elements in roughly equal proportions, and they often form simple solid solution structures instead of the complex intermetallic phases you'd expect from a conventional phase diagram. The properties don't always follow the patterns you'd predict from adding up the properties of the constituent elements. Some of them have exceptional combinations of strength and ductility that don't fit neatly into existing frameworks. The field is still developing the vocabulary and the models to describe what's happening. Amorphous metals, or metallic glasses, represent yet another category. They lack crystalline structure entirely, so the entire concept of grain boundaries and slip systems doesn't apply. Their properties are governed by different mechanisms—shear band formation, free volume, local atomic rearrangement. Understanding them requires a different mental model than the one you use for crystalline materials. If your background is primarily in conventional metals and you encounter a amorphous alloy, the assumptions you bring with you might lead you astray.
The limitations aren't reasons to avoid this kind of analysis. They're reasons to be honest about what you can and can't predict, and to validate your conclusions with actual testing. The aluminum casting problem I described at the beginning could have been solved by guessing at a new alloy composition, but that would have been expensive and uncertain. Looking at the structure gave us a direct answer. That's the value of this approach. It doesn't guarantee success in every case, but it gives you a framework for asking the right questions and finding answers that are grounded in what's actually happening inside the material rather than in what a handbook says should happen.