Calibration Isn't Just About the Timing Marks
I spent about eight hours last week chasing a stitch quality issue on a Juki DDL-9000C that turned out to be a cascading failure. The operator had been adjusting top tension to compensate for bunching on the underside, not realizing the hook timing had shifted just 0.3 millimeters after a recent needle plate change. Every twist of the tension dial was making things worse. This is the kind of problem most beginner guides don't cover because they assume each calibration step exists in isolation. It doesn't. The technical manual sewing machine calibration manual you'll find online or bundled with industrial units is essentially a troubleshooting flowchart for a machine that doesn't behave the way the factory says it should. It's most useful when you understand the hierarchy of adjustments. Most people approach calibration backwards, starting with thread tension when the real culprit is often something upstream. Needle bar height, hook timing, presser foot pressure, loop formation point — these all interact. Change one, and everything else shifts slightly. Let me walk through what I actually do when a machine comes in with vague stitch complaints. First, I check the needle. Not the tension. The needle. A bent needle, even one you can't see the bend in, will throw off loop formation enough to make you chase problems that don't exist. I hold it up to the light and roll it on a flat surface. Takes thirty seconds. Most people skip this and go straight to timing adjustments that fix nothing.
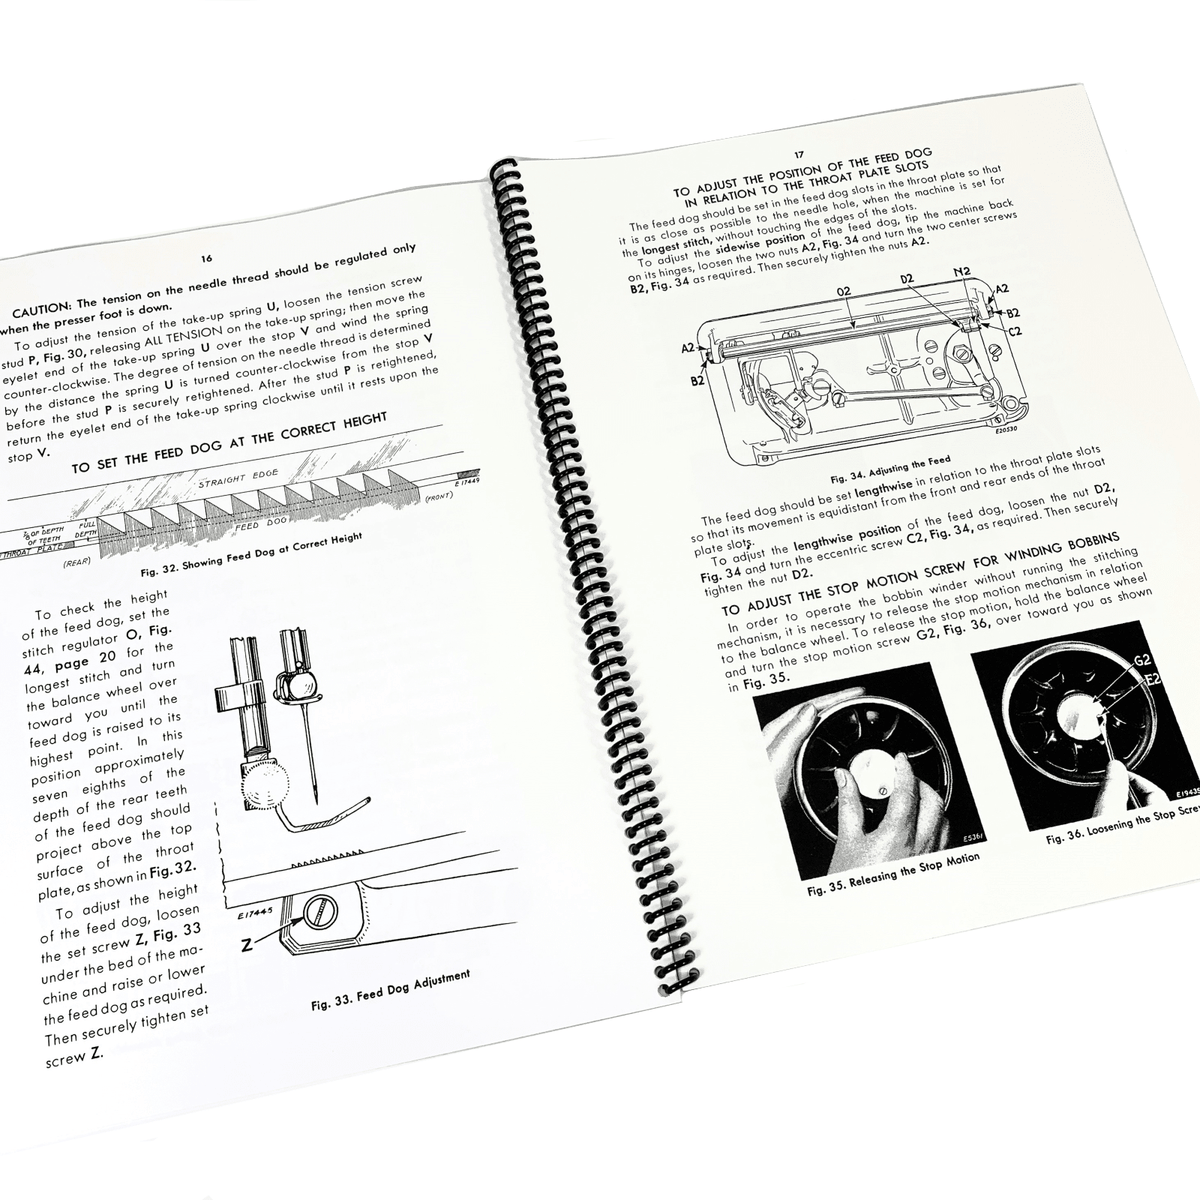
After confirming the needle is straight and correctly inserted, I move to the needle bar height. On a standard industrial lockstitch machine, the hook should catch the thread loop when the needle eye is approximately 2 to 2.5 millimeters above the bobbin case top. If it's too high, the hook misses the loop entirely. Too low, and you get thread breakage and bird nesting. I use a dial indicator for this, not the manufacturer's markings alone. Those painted lines on the pulley wear out or get misaligned during previous repairs. Hook timing comes next, and this is where most DIY calibration goes wrong. The gap between the hook point and the needle should be 0.05 to 0.1 millimeters — roughly the thickness of a sheet of paper. I've seen technicians use feeler gauges here and get it close, but the real test is visual with a fresh thread. Load the machine, run it at low speed, and watch the loop formation. If the hook is hitting the needle, you'll hear it. If it's too far away, the loop collapses before capture. Neither shows up on a feeler gauge. Presser foot pressure is another adjustment people ignore until it's causing issues. Heavy fabric needs more pressure, light fabric needs less. The spring tension on most industrial machines is adjustable via a screw on top of the presser foot bar. I typically set it around 8 to 10 newtons for midweight materials. Too much pressure and you're distorting the fabric, which changes stitch length consistency. Too little and the feed dogs can't move the material properly, causing uneven stitches that look like a timing problem but aren't.
Here's something counter-intuitive that took me years to learn: lubrication affects calibration. When I rebuilt a brother industrial last year, the timing was perfect after reassembly, but after running it for twenty minutes with fresh oil, the hook timing shifted by about 0.15 millimeters. The oil film changed the effective clearances in the hook race. I had to cold-set the timing slightly off from spec, knowing it would settle into the sweet spot once warmed up. Most manuals don't mention this because they write for ideal conditions. Real machines have viscosity variables. Electronic servo machines add another layer. The upper dead center position isn't mechanically fixed the same way it is on clutch motor machines. Belt stretch, encoder drift, and voltage fluctuations can all shift the needle position relative to the hook over time. I calibrate these by referencing the encoder zero point first, then verifying mechanical alignment, rather than the other way around. Skip the encoder check and you're calibrating to a position that might not actually be where the machine thinks it is. The bobbin case itself needs inspection during calibration. Worn hook points, nicks in the race, or lint-compacted tension discs will make a perfectly timed machine sew poorly. I clean the bobbin area with a brass brush and inspect under magnification. A hairline nick on the hook point will fray thread and cause breaks that look like timing issues. Replacing the bobbin case is cheap compared to hours of troubleshooting.
Get the Full Details
Thread path alignment is the step I see skipped most often. The thread should pass through all guides without touching the sides. If the take-up spring travel is too short, you get inconsistent tension regardless of what the tension dial says. I measure take-up spring travel at 2 to 3 millimeters of free movement. Anything less and the tension discs don't open and close cleanly during each stitch cycle. After all mechanical adjustments, I run a test seam on the actual material the machine will be sewing. Not a scrap, not the test cloth that came with the manual. The actual production fabric with the actual thread and needle combination. Stitch quality can change dramatically between materials, and a calibration that looks perfect on cotton poplin will fall apart on nylon or leather. One edge case I ran into recently involved a multi-needle bar-tacking machine where two needles were timing fine but the third was consistently producing loose stitches on the underside. The individual needle timing was correct for all three. The problem turned out to be that the thread guide for the third needle was positioned 1 millimeter too far from the needle eye compared to the other two. This changed the loop formation dynamics just enough to cause intermittent capture failure at higher speeds. The calibration manual covered each needle independently but didn't address inter-needle consistency, which matters when all needles are supposed to produce identical stitches.
For anyone working through this process, keep a written record of every adjustment. Mark positions with a fine marker on the pulley, note tension dial readings, record presser foot pressure settings. Machines drift. You'll be glad you have a baseline when the problem returns three weeks later. Most online resources for a Technical Manual Sewing Machine Calibration Manual provide the specifications but not the decision tree for when things don't match those specifications. That's the part that only comes from doing this work repeatedly and accumulating a set of shortcuts that aren't in any manual.
When Calibration Won't Help
Some problems look like calibration issues but aren't. Worn drive belts, loose main shaft bearings, cracked cam plates, and degraded timing gears all produce symptoms identical to misadjustment. If you've gone through the full calibration sequence and the machine still doesn't sew right, stop adjusting and start inspecting wear. I've wasted entire days on machines that needed a new main shaft bearing rather than a timing adjustment. The bearing play was causing the hook assembly to wobble just enough to miss loops intermittently, which no amount of timing correction would fix. Thermal expansion also matters on machines that run for extended periods. A machine calibrated cold will drift as components heat up and expand at different rates. If your stitch quality is acceptable at the start of a shift but degrades after an hour, the calibration was done at the wrong temperature. Let the machine reach operating temperature first, then verify and adjust. This is especially relevant for high-speed machines running above 4,000 stitches per minute where friction heating is significant. Environmental factors like humidity and ambient temperature affect thread behavior independently of machine calibration. Polyester thread expands differently than cotton in humid conditions, and thread diameter changes can make a perfectly calibrated machine appear out of specification. I once spent two days troubleshooting a tension issue that was actually caused by a warehouse HVAC failure shifting humidity from 40% to 75%. The machine was fine. The thread wasn't.