Proteins in food systems are functional tools, not just nutrients
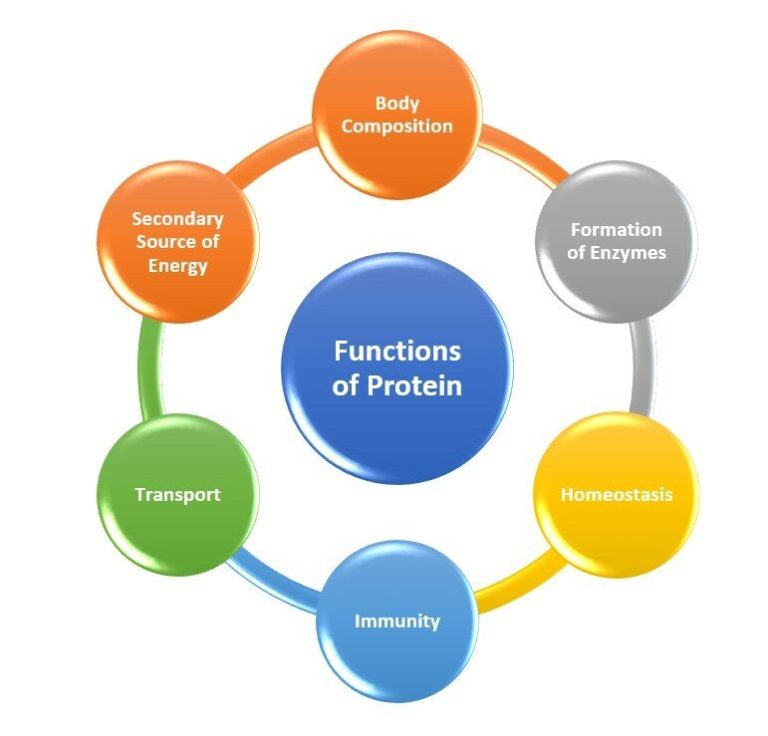
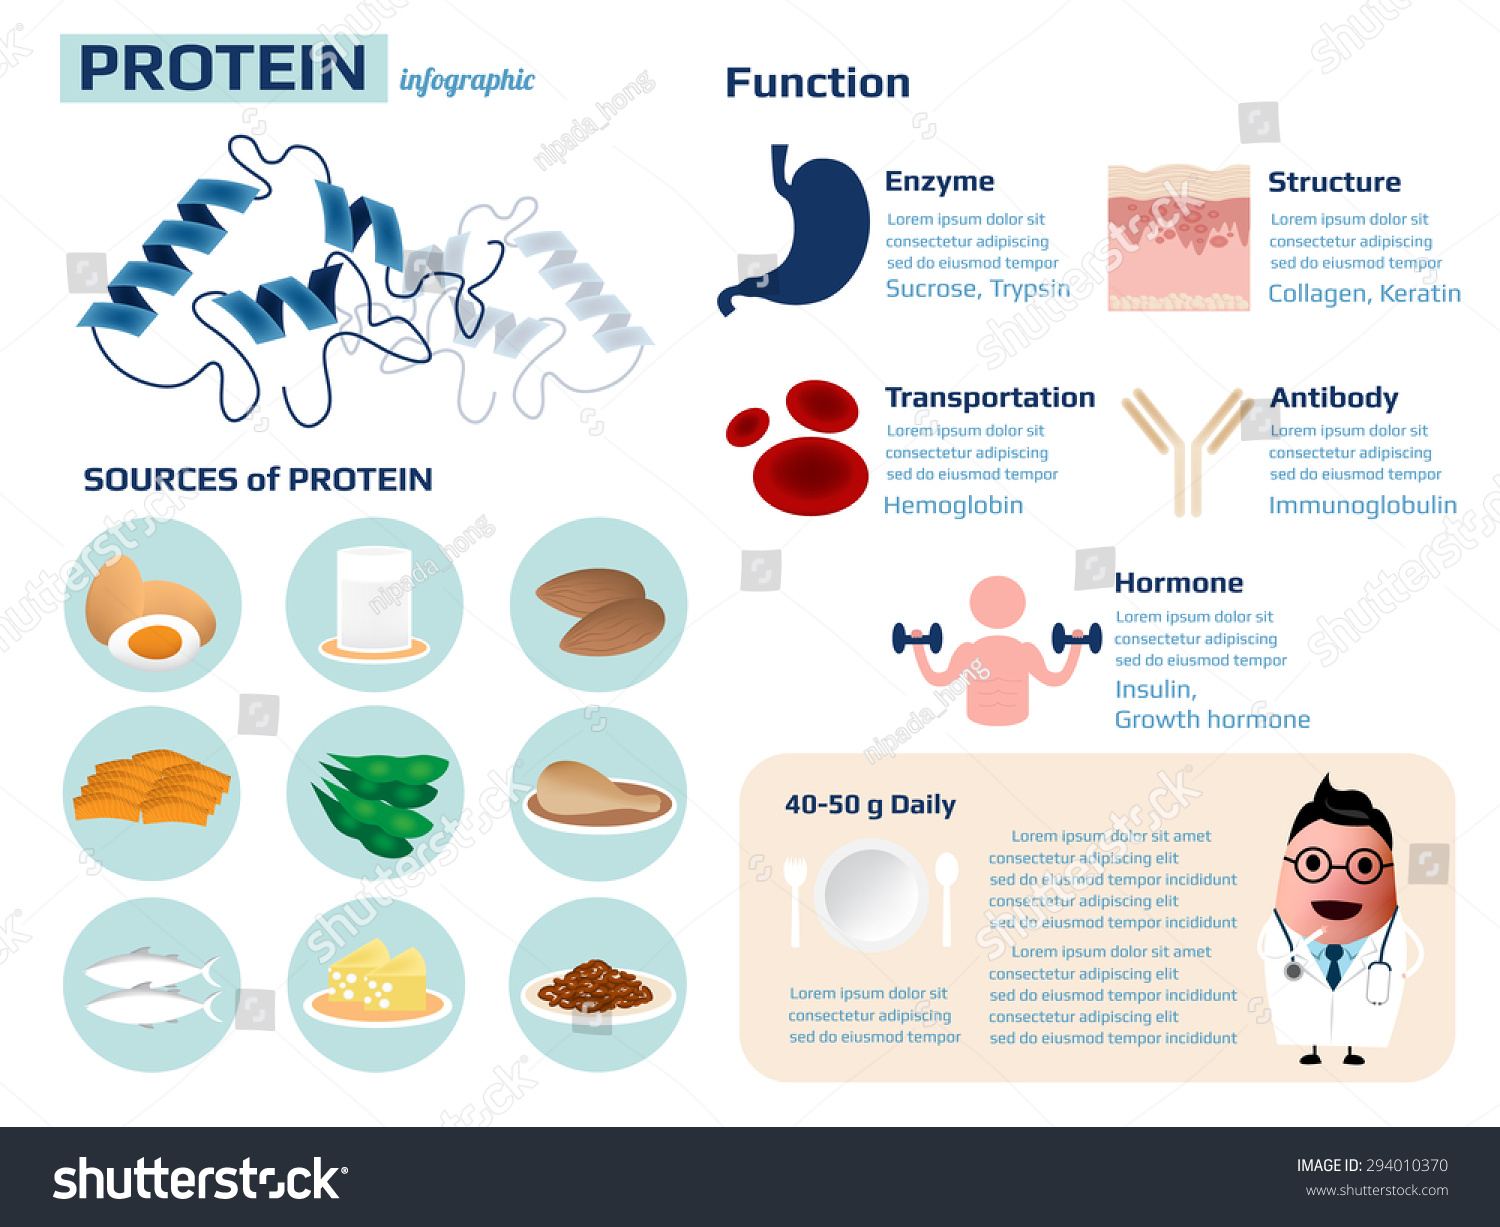
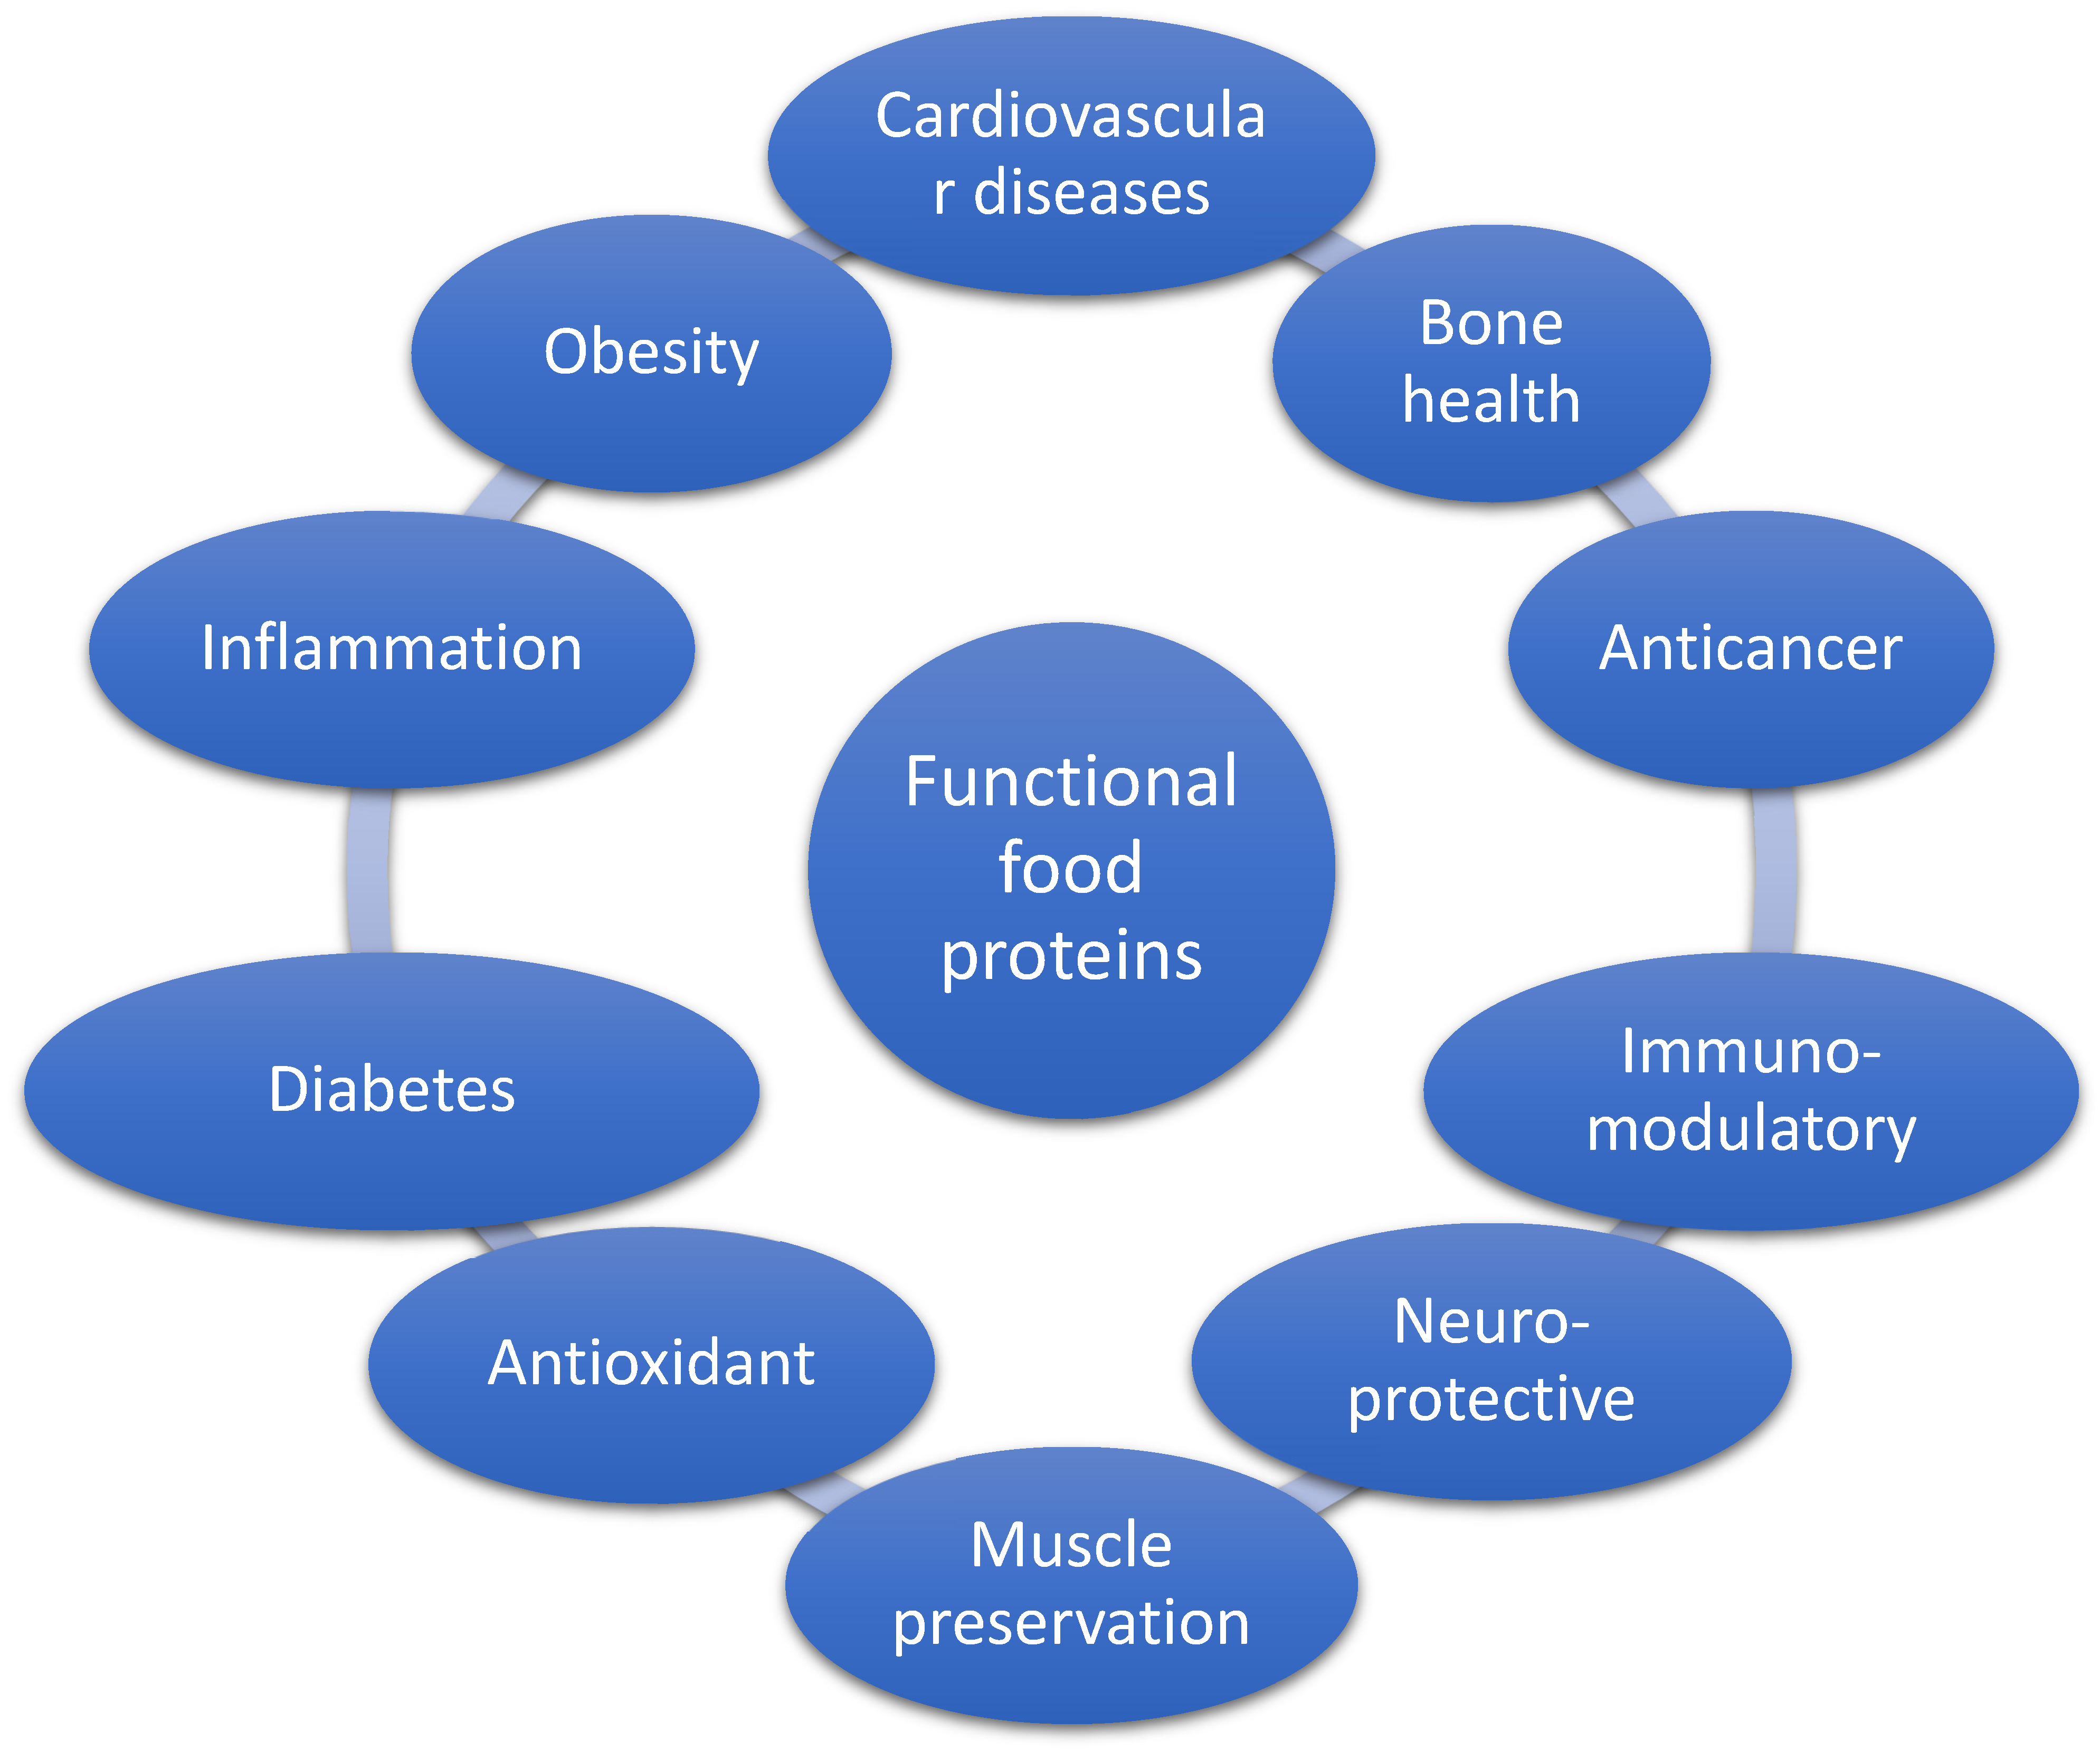
When I first got into food formulation, I treated proteins as ingredients to count on the label. That changed quickly when I was working on a shelf-stable emulsion that kept breaking during thermal processing. The product separated before it even hit the shelf. The problem wasn't the protein's amino acid composition. It was how I was handling its functional properties—water binding, emulsification, gelation—at different pH levels and temperatures. Water binding and retention is probably the most frequently overlooked function. Protein molecules have hydrophilic regions that attract and hold water through hydrogen bonding. This matters because water activity controls microbial growth and texture. Meat processors use this to reduce cooking loss. Bakeries rely on it for crumb structure. The key is getting the protein to the right state where those binding sites are exposed and accessible. Emulsification comes next. Proteins sit at oil-water interfaces. Their amphiphilic nature means hydrophobic amino acid side chains anchor into the oil phase while hydrophilic portions extend into the aqueous phase. This reduces interfacial tension and stabilizes the emulsion. Milk casein is the classic example, but soy and whey proteins work too depending on the system. The critical factor is how much protein is available at the interface and how well it forms a viscoelastic film around the dispersed droplets.
Gelation creates the 3D network that gives products structure. When proteins denature and aggregate under heat, acid, or salt, they form a mesh that traps water and other components. Gelation temperature and strength depend heavily on protein source, pH, ionic strength, and concentration. Gels can be thermally reversible like some fish myofibrillar proteins or irreversible like set yogurt from acid-induced casein micelle aggregation. Aeration and foaming involve proteins stabilizing air pockets by forming films at the gas-liquid interface. Egg white proteins are the gold standard here, but pea and whey proteins can work too. Foams require proteins that unfold enough to spread at the interface but not so much that the film collapses. Meringue works at relatively high protein concentrations with gentle handling, while some industrial foams need specific processing conditions. Thickening and viscosity modification happens when proteins absorb water and swell without forming a complete gel network. This increases the continuous phase viscosity and affects mouthfeel. The effect is concentration-dependent and varies significantly by protein source. Gelatin thickens at low concentrations but gels above its melting point, while soy concentrates thicken more at higher pH levels.
The Functional Roles Of Proteins In Foods in practice
Getting the The Functional Roles Of Proteins In Foods right on paper is one thing. Doing it in a real production environment is another. I ran into a specific problem last year that still makes me wince. I was developing a plant-based beverage using pea protein isolate. Everything looked fine at the lab scale. The pH was adjusted to 7.0, the protein concentration was 8%, and the homogenization parameters were solid. Then I moved to pilot scale and the product developed a gritty texture and slight phase separation within 48 hours. The issue turned out to be the residual fiber and starch co-extracted during the isolate production. At the higher throughput of the pilot line, those particles acted as nucleation sites for protein aggregation. The fix wasn't changing the protein source or the pH. It was adding a small amount of carrageenan—about 0.05%—which formed a weak gel network that stabilized the suspension without affecting flavor. The carrageenan didn't replace any protein function. It just filled a gap that protein alone couldn't cover in that particular matrix.
Get the Full Details
Key parameters to control when working with proteins
The pH dependency is the first thing I check. Every protein has an isoelectric point where its net charge is zero and solubility drops to its minimum. For whey proteins, that's around pH 5.2. For soy protein, it's closer to pH 4.5. Working near the pI gives you maximum aggregation and gelation potential, but it also gives you precipitation headaches if you drift even a fraction of a pH unit. I always keep a pH profile on hand before I start adjusting anything else. Denaturation state matters enormously. Heat, acid, shear—all of these unfold proteins and expose hydrophobic regions. Sometimes that's what you want. A denatured whey protein gels more readily. Sometimes it's what you don't want. Over-denatured egg white proteins lose foaming capacity because the molecules unfold too far and form strong but brittle intermolecular bonds. The trick is controlling the severity and duration of whatever denaturing force you're applying. Protein source and degree of purification affect everything. Isolate, concentrate, and flour behave differently even when they come from the same raw material. I once swapped a soy protein concentrate for an isolate in a reformulation and spent three weeks debugging viscosity issues that traced back entirely to the different carbohydrate and mineral content. The protein percentage was the same on paper. The functionality was completely different.
Processing history is another factor that gets ignored too often. Whey protein that's been spray-dried at high inlet temperatures denatures more during production itself. That pre-denatured protein behaves differently than native whey in both gelling and emulsifying applications. I've seen spec sheets list the same amino acid profile for two products and assume they'd perform identically. They never do.
Common pitfalls and limitations
Protein functionality is notoriously difficult to predict from first principles. I've lost count of the formulations that looked perfect based on textbook behavior and failed in production. Temperature swings during processing can shift pH, ionic strength, and denaturation rates simultaneously. A change of 5 degrees Celsius can alter gelation kinetics enough to ruin a batch that would have been fine at the original temperature. High-protein systems tend to be expensive. Beyond the ingredient cost, they often require additional processing equipment or steps—high-shear mixing, controlled pH adjustment, precise thermal processing—that smaller operations simply don't have. And masking off-flavors from plant proteins, particularly bitterness from polyphenol complexes and beany notes from lipoxygenase activity, eats into formulation margins faster than most people expect. If you're working in a context where protein functionality alone isn't delivering the desired texture or stability, combining proteins with hydrocolloids is usually the most practical path. Carrageenan, xanthan gum, and locust bean gum each interact with proteins in different ways. Carrageenan forms complexes with whey proteins. Xanthan provides shear-thinning that helps suspend particles. Locust bean gum synergizes with carrageenan to modify gel texture. These combinations aren't always obvious from the ingredient list alone.
The bottom line is that protein functionality sits at the intersection of chemistry, physics, and process engineering. You can study the theory until you understand every interaction, but the actual behavior of a protein in a complex food matrix depends on variables that are easy to miss until something breaks. Keeping detailed records of pH, temperature, timing, and ingredient batches pays for itself the first time a problem surfaces and you need to trace it back.