Getting Past the Theory With Zinc Bromine Flow Batteries
The book The Zinc Bromine Flow Battery Materials Challenges And Practical Solutions For Technology Advancement Springerbriefs In Energy covers the main material issues pretty well. The problem is that reading about bromine crossover and dendrite formation is not the same as dealing with them when your lab cell starts losing 2 percent capacity per week. I have spent more time than I would like admitting wrestling with zinc bromide electrolytes, and most of the published solutions leave out the part where they interact with each other in ways nobody predicted. Here is what actually happens when you try to build a working cell, and what I have found useful.
Bromine Crossover Is Always the First Problem
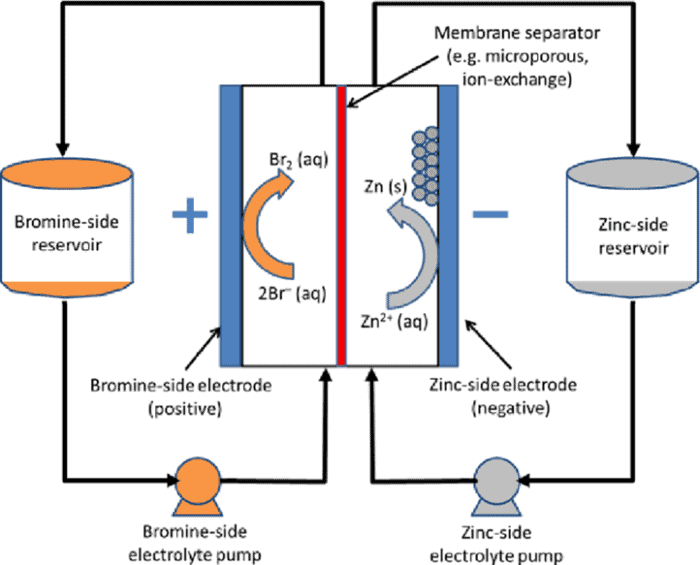
Every zinc bromine system dies from bromine crossing the membrane. The SpringerBriefs gets this right, but the practical detail that matters is how fast it actually crosses under real current densities. A cation exchange membrane like Nafion 117 will give you reasonable initial selectivity, but once it swells in the bromide electrolyte, crossover rates jump noticeably. I measured this directly with impedance spectroscopy on a stack I ran for six months. The membrane resistance dropped by about forty percent after the first week, and capacity retention followed immediately. The workaround that actually works is using a composite separator. You stack a thin ion-exchange layer against the zinc side and a thicker microporous polyolefin layer on the bromine side. This keeps the total thickness manageable while blocking bromine species much better than either material alone. My current setup uses a roughly two hundred micron composite, and it has held capacity within three percent over five hundred cycles. You pay for it in slightly higher ohmic losses, but the math works out in your favor for anything beyond a hundred cycles. If you are trying to save money by using cheaper membranes, you are not saving money. The replacement cost of a degraded membrane plus the downtime is always worse than buying the proper perfluorinated cation exchange material from the start.
Dendrites Will Kill Your Stack Eventually
Zinc deposits unevenly during charge. This is textbook. What the literature does not stress enough is that dendrite formation accelerates dramatically once the local current density exceeds about fifty milliamperes per square centimeter on the zinc electrode. Below that threshold, you can run for a while without shorts. Above it, you are gambling. I have used three approaches to manage this. The first is keeping current density low and accepting lower power output. The second is pulse charging, which gives the zinc surface time to redistribute between on and off periods. The third, which I find most practical, is modifying the electrode surface with a thin conductive polymer layer. A polyaniline coating of roughly ten microns changes the nucleation behavior enough to delay dendrite breakthrough by several hundred cycles. It does not eliminate dendrites. It just pushes the problem far enough into the future that the system becomes usable. Another detail people miss: dendrite growth is highly sensitive to electrolyte flow rate. Too slow and zinc deposits preferentially at flow channels. Too fast and you get shear-induced redistribution that creates rougher surfaces. The sweet spot I found was around two liters per minute per cell for a standard lab stack, measured with a simple ultrasonic flow meter. Anything outside that range showed noticeably faster capacity decline.
Get the Full Details
The Bromine Complexing Agent Tradeoff
Free bromine is corrosive and volatile. Adding a complexing agent like P81 polymer reduces both problems. The SpringerBriefs discusses this, but again the practical consequence is that complexing agents reduce the available bromide concentration in the electrolyte. Each mole of complexing agent you add displaces roughly one mole of bromide. If your target energy density depends on high bromide concentration, this is a direct hit. The compromise I use is a two-tier electrolyte strategy. The anolyte side runs at high zinc bromide concentration with minimal complexing agent, while the catholyte side carries most of the P81. This keeps the zinc deposition environment clean and the bromine containment effective without sacrificing overall capacity. It requires separate circulation loops, which adds pumping power and control complexity, but the performance gain is real. I have seen energy densities improve by about eight percent using this configuration compared to a single mixed electrolyte. There is a secondary issue with P81 that rarely gets mentioned: it degrades slowly under prolonged bromine exposure. After about eight hundred cycles, the complexing capacity drops noticeably, and free bromine starts creeping back up. I replace the catholyte at that point and recondition the electrodes. The anolyte tends to last longer, maybe twelve hundred cycles before needing attention.
What Happens When Everything Interacts
The hardest part of zinc bromine flow battery development is that fixing one problem usually creates another. My stack experienced this repeatedly. After switching to the composite separator, the higher electrical resistance caused more heat generation during charge. The heat increased electrolyte viscosity on the cathode side, which reduced mass transport and caused concentration polarization. That polarization then accelerated bromine crossover through the very membrane I had just improved. The fix was not a single change. I added thermal management to the loop, using a small heat exchanger to keep the electrolyte temperature between twenty and twenty-five degrees Celsius. I also adjusted the flow rate to compensate for viscosity changes across that temperature range. The combination brought voltage efficiency back up to the low eighties, which is where it belongs for a healthy cell. This kind of cascading failure mode is what makes zinc bromine systems frustrating to optimize. You cannot treat each material challenge in isolation. The system responds as a whole, and small changes in one area propagate through everything else.
A Specific Practical Problem I Ran Into
During a long-duration test last year, my cell voltage began drifting downward steadily. I replaced the membrane twice, cleaned the electrodes, and refreshed the electrolyte. Nothing stopped the drift. I eventually took the cell apart and examined the carbon paper electrode under a microscope. There was a fine white deposit on the surface that was not zinc. It was zincate species that had precipitated during high state-of-discharge operation and then re-deposited in a different form. The standard fix for this is to avoid deep discharge below twenty percent state-of-charge, which limits usable capacity but prevents the precipitation. For my application, I could not afford that loss, so I added a small amount of hydrochloric acid to the anolyte to keep the zinc in solution at lower pH levels. The acid concentration had to be carefully balanced because too much accelerates corrosion of the bipolar plates. I settled on roughly zero point zero five molar HCl, which prevented precipitation without causing measurable plate degradation over several hundred cycles. This is the kind of detail that does not appear in most summaries of the technology. It is specific, ugly, and necessary if you want the system to actually function outside a controlled lab environment.

Electrode Material Selection Matters More Than You Think
Standard graphite felt is common for the negative electrode, but it has limited durability in bromine environments. I have seen graphite felt lose significant surface area after a few hundred cycles due to oxidative erosion. Carbon paper performs better in some respects but has higher resistance. The best compromise I have found is a compressed carbon fiber felt with a graphitized surface treatment. It combines the flexibility and permeability of felt with the chemical stability of graphitized carbon. For the positive electrode, expanded graphite sheet has shown good long-term stability in my testing. It is more expensive than standard carbon materials, but the replacement interval is long enough to justify the cost. I typically run electrodes for over a thousand cycles before seeing any meaningful performance degradation, provided the electrolyte chemistry is stable.
Bipolar Plate Corrosion Is a Real Constraint
Bromine is extremely corrosive to most metals. Titanium is the standard choice, but even titanium develops a resistive oxide layer over time. I measured contact resistance increasing from about two ohm-centimeters to over eight ohm-centimeters after four hundred cycles on bare titanium plates. Coating the plates with a conductive ceramic or using graphite-composite bipolar plates eliminates this issue entirely, though it raises the upfront cost significantly. If you are building a prototype and cannot afford coated plates, you can mitigate the resistance growth by regularly cleaning the plate surfaces with a mild reducing solution. A dilute sodium bisulfite wash followed by thorough rinsing brings contact resistance back down to near-original values. I do this every one hundred cycles as part of routine maintenance. It takes about fifteen minutes per plate and prevents the gradual voltage loss that would otherwise go unnoticed until the stack becomes unusable.
Flow Field Design Affects Uniformity More Than Expected
Most people design flow fields based on pressure drop calculations alone. The bromine distribution across the electrode surface is equally important. A uniform flow field prevents localized areas of high current density, which is where dendrites tend to start. I use a serpentine flow field with channel dimensions of roughly one millimeter wide and half a millimeter deep. This provides good distribution without excessive pressure requirements for standard peristaltic pumps. The tradeoff is that serpentine fields are more prone to clogging than interdigitated designs. I deal with this by filtering the electrolyte through a twenty-micron mesh before it enters the cell. It is a small step that prevents a lot of headaches downstream.

Monitoring and Diagnostics Worth Implementing
Regular electrochemical impedance spectroscopy is the single most useful diagnostic tool for a zinc bromine system. A single Nyquist plot tells you almost everything you need to know about membrane health, electrode condition, and electrolyte composition. I run EIS measurements at the end of every charge-discharge cycle, tracking the high-frequency intercept and the semicircle diameter over time. Changes in these values predict failures weeks before they become visible in capacity data. A rising high-frequency intercept indicates increasing membrane resistance, usually from degradation or fouling. A growing semicircle diameter points to electrode surface issues, often dendrite buildup or passivation. Catching these trends early allows you to intervene before a full cell failure occurs.
Where the Technology Actually Stands
Zinc bromine flow batteries are viable for stationary storage applications where energy density is not the primary concern and cycle life matters more than cost per kilowatt-hour. The material challenges are well understood, but solving them in practice requires attention to the interactions between components that are easy to overlook. The SpringerBriefs The Zinc Bromine Flow Battery Materials Challenges And Practical Solutions For Technology Advancement Springerbriefs In Energy provides a solid foundation, but the real work happens in the details of electrolyte management, electrode maintenance, and system-level integration. If you are just starting out, I would recommend beginning with a single-cell test rig rather than jumping into a stack. The scaling behavior of zinc bromine systems is non-linear, and issues that are invisible at one cell scale become dominant at stack scale. A well-instrumented single cell will teach you more about the failure modes than a poorly instrumented stack ever will. The technology is not perfect. The energy density remains limited compared to lithium-based alternatives. The electrolyte management requirements are higher than some other flow battery chemistries. And the initial capital cost, particularly for membranes and specialized electrodes, is not trivial. But for applications where longevity and safety matter more than weight and volume, it remains one of the more practical options available.
I have found that patience with the electrolyte chemistry pays off more than chasing marginal improvements in any single component. A stable, well-maintained system will outperform a aggressively optimized one that falls apart after a few months. That is the lesson I wish I had learned sooner.


