What You Actually Need to Know Before You Use It
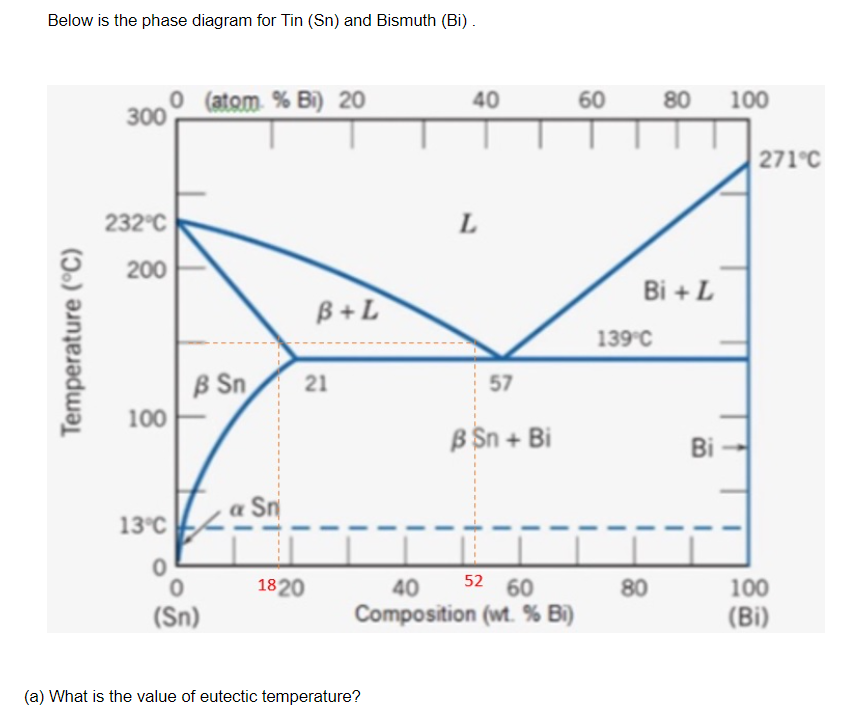
The Tin Bismuth Phase Diagram is one of those things people look up when they're trying to figure out why a solder joint failed or why their low-temperature melt isn't behaving the way the datasheet said it would. The diagram itself is straightforward enough. Tin and bismuth form a simple eutectic system with no intermetallic compounds. The eutectic point sits at 139°C with a composition of roughly 58% bismuth and 42% tin by weight. Below that temperature, you get a mixture of solid tin and solid bismuth. Above it, everything's liquid. That's about the whole story. I ran into a situation a while back where someone was using a Sn-Bi solder for rework on a board with thermally sensitive components, and the joint kept coming loose after thermal cycling. The problem wasn't the phase diagram itself - it was that the eutectic composition shifts slightly depending on cooling rate and prior thermal history. Fast cooling can trap non-equilibrium phases that aren't represented on the standard diagram. I ended up baking the joints at 80°C for a couple hours after soldering to let things equilibrate properly. That fixed the delamination issue.
Reading the Tin Bismuth Phase Diagram Correctly
When you pull up a Tin Bismuth Phase Diagram, the axes are temperature versus composition. Temperature runs vertically from room temp up past 300°C. Composition runs horizontally from pure tin on the left to pure bismuth on the right. The liquidus line starts high on the tin side around 232°C and drops down to the eutectic minimum. The solidus line is flat at the eutectic temperature across the compositional range near the eutectic point. Between the liquidus and solidus, you're in a two-phase region where liquid and solid tin coexist on the left side, and liquid and solid bismuth coexist on the right side. One thing most people miss is that the eutectic composition isn't exactly 58-42 across every source you'll find. Some references say 57% Bi, others say 58%, and a few go as high as 60%. The variation comes from different measurement techniques and how they define the eutectic point. For practical soldering work, it doesn't matter much. But if you're doing metallurgical analysis or casting alloys, pick a source and stick with it, because the difference shows up in your calculations. Another thing that catches people off guard is what happens when you're not at equilibrium. The diagram assumes slow cooling. If you're drop-soldering a component and cool it in seconds, the microstructure you end up with won't match what the diagram predicts. You get finer grain structures, and in some cases, you can actually undercool the liquid a few degrees below the eutectic temperature before solidification kicks in. This matters if you're trying to predict thermal behavior in a production environment.
Where the Diagram Falls Short
The standard Tin Bismuth Phase Diagram doesn't account for trace impurities, which is a real problem in practice. Lead-free solders often contain small amounts of copper, silver, or iron from the substrate or tooling. Even 0.1% copper can form Cu6Sn5 intermetallics at the interface that change the local melting behavior. The diagram will tell you the alloy melts at 139°C, but your actual joint might start softening several degrees lower because of these interfacial reactions. Another limitation is that the diagram assumes bulk material. When you're working with thin films or micro-joints, surface energy effects become significant. The melting point can depress by 10 to 20°C at the micron scale compared to what the bulk phase diagram shows. This is relevant if you're doing anything with flip-chip solder bumps or fine-pitch rework. There's also the issue of bismuth volatility. Bismuth has a measurable vapor pressure at soldering temperatures, and over repeated thermal cycles, you can actually lose bismuth from the joint. The composition drifts toward the tin side, which moves you away from the eutectic point and raises the melting temperature. I've seen joints where the eutectic composition shifted enough that a rework that should have melted at 139°C required 155°C to fully liquefy after five thermal cycles. The phase diagram didn't predict any of that.
Get the Full Details

Practical Sources and How to Use Them
If you need an actual diagram to reference, the most reliable sources are theASM Handbooks and the Thermo-Calc database. Both are behind paywalls, but if you have university or corporate access, use it. The open-source alternatives like the NIST Webbook have the data points but the visual diagrams are less polished. For quick reference, the diagram from the JPRAS database is decent and freely available, though it lacks the detail you'd want for serious work. When I need to look something up fast, I keep a PDF of the Sn-Bi diagram bookmarked in my browser alongside my standard Sn-Pb reference. The two systems look similar at a glance but the eutectic temperatures are very different - 183°C for Sn-Pb versus 139°C for Sn-Bi. Mixing them up in a design document is an easy mistake to make and a costly one to correct after manufacturing has started. For simulation work, you can export the thermodynamic data from Thermo-Calc or calculate it yourself using the Calphad method if you have the binary interaction parameters. The Redlich-Kister polynomial coefficients for the Sn-Bi system are well documented. It takes maybe 20 minutes to set up a proper calculation, and the output is more flexible than a static diagram because you can get isothermal sections and compute phase fractions at any temperature.
The diagram is useful. It just doesn't tell the whole story, and anyone who treats it as the final word on tin-bismuth behavior is going to have problems in the field. The differences between theory and practice show up in cooling rates, impurities, thin-film effects, and compositional drift. Knowing those gaps matters more than memorizing the eutectic temperature.


