What You Actually Need to Know Before Working With Titanium
Titanium is the material of choice when you need strength without weight, but it will chew through your tooling and waste half your working time if you treat it like steel. I spent three years machining titanium parts for aerospace contractors before I stopped fighting the material and started working with it. The most important thing to understand is that titanium's apparent weakness at room temperature is actually its superpower at elevated temperatures. Commercial pure titanium (Grades 1 through 4) sits at the mild end of the spectrum. Grade 1 is soft, nearly formable, and used where corrosion resistance matters more than strength. Grade 4 is significantly stronger but considerably less ductile. The jump from Grade 3 to Grade 4 is where you start running into real machining difficulty without a proper setup.
Titanium And Titanium Alloys Fundamentals And Applications
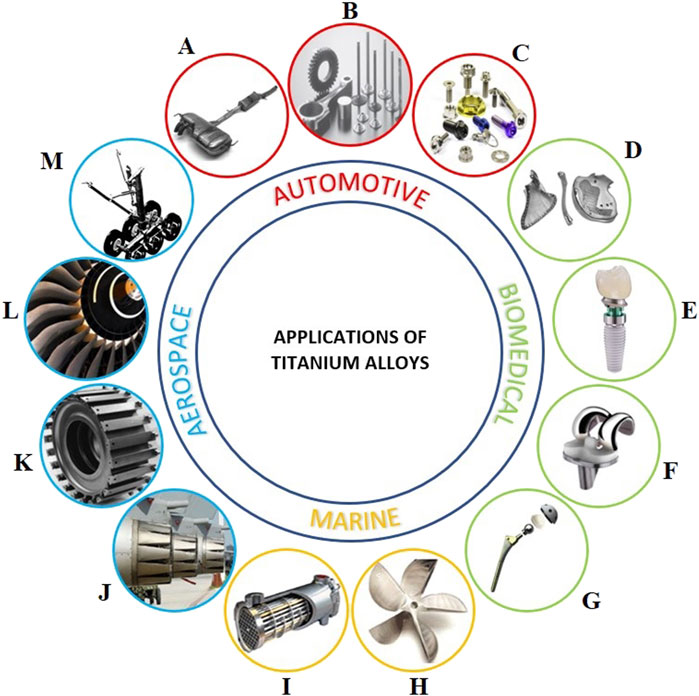
Ti-6Al-4V, also known as Grade 5, accounts for roughly 50 percent of all titanium consumed worldwide. It is the workhorse alloy for aircraft engine components, landing gear fittings, and medical implants. The aluminum stabilizes the alpha phase while vanadium stabilizes the beta phase, creating a microstructure that responds predictably to heat treatment. That predictability is what makes it preferred over other alpha-beta alloys for critical structural applications. Here is something most introductory guides do not mention. Titanium has an extremely low thermal conductivity, approximately 22 watts per meter kelvin compared to steel's 50. This means the heat generated during cutting does not dissipate into the chip or the workpiece. It stays concentrated at the cutting edge. When I was running Ti-6Al-4V on a Haas VF-2, I discovered this the hard way after a batch of roughing cuts destroyed three carbide end mills in under forty minutes. The breakthrough came when I switched to a low helix, large core end mill with a coated substrate designed specifically for titanium, reduced my feed rate by 30 percent, and increased the depth of cut just enough to keep the tool consistently engaged rather than rubbing. Tool life jumped from roughly fifteen parts to over two hundred parts per insert. Wrought titanium alloys generally fall into three categories: alpha, alpha-beta, and beta. Alpha alloys like Ti-5Al-2.5Sn offer excellent creep resistance at temperatures up to about 600 degrees Celsius but cannot be heat treated for significant strength improvement. They are used primarily in jet engine compressor components where high temperature performance matters more than room temperature strength. Alpha-beta alloys span the widest range of properties. Ti-6Al-4V is the dominant member. Beta alloys such as Ti-10V-2Fe-3Al can be solution treated and aged to achieve tensile strengths exceeding 1400 megapascals. These are the alloys you reach for when weight savings are critical and the part geometry allows for proper heat treatment.
Cast titanium presents a different set of challenges entirely. The casting process introduces porosity and grain structure variation that no amount of post-processing fully eliminates. For this reason, cast titanium is almost never used for primary structural components in aerospace. It finds applications in complex-shaped valve bodies, pump housings, and ornamental architectural work where near-net-shape casting provides economic advantages that outweigh the mechanical property limitations.
Get the Full Details

Machining Reality Check
If you are planning to machine titanium, stop reading introductory articles and find someone who has actually done it. The theoretical cutting parameters you find online assume ideal conditions that do not exist in a real shop. Ti-6Al-4V at Rockwell C 33 requires significantly different approach angles, coolant delivery, and spindle speed strategies than the same alloy at Rockwell C 39 after aging treatment. The rule of thumb for cutting speed is dramatically lower than steel. A common starting point for Ti-6Al-4V with a coated carbide end mill is around 80 to 120 surface feet per minute. This is not a suggestion. Going faster will generate enough heat at the cutting interface to accelerate tool wear exponentially and risk work hardening the near-surface layer of the part. Once you work harden titanium, subsequent passes become dramatically more difficult because the hardened layer acts as a ceramic-like barrier that destroys cutting edges. One persistent misconception is that titanium is inherently gummy or adhesive. It is not. The problem is that titanium has a strong affinity for oxygen and nitrogen at elevated temperatures. During cutting, the freshly exposed metal surface reacts with atmospheric gases, forming a hard oxide layer that accelerates diffusion wear on the tool. This is why inert gas shielding or minimal mist coolant performs better than flood coolant in some situations. Flood coolant can actually wash away the protective oxide film and expose fresh titanium to oxidation at the cutting zone.
I encountered a particularly stubborn issue when machining thin-walled Ti-6Al-4V sleeves for a hydraulic application. The walls would deflect during finishing passes, causing inconsistent chip loads and premature tool failure. The workaround was switching from a climb milling strategy to a conventional milling approach for the final pass, reducing radial engagement to 10 percent of the tool diameter, and implementing a spiral lead-in rather than a straight plunge. This eliminated the deflection problem entirely and produced surfaces within 15 microinch Ra on the first try.
Welding Titanium Requires A Different Mindset
Titanium welding is not difficult if you understand what makes it difficult. The metal becomes highly reactive above 800 degrees Fahrenheit, absorbing oxygen, nitrogen, and hydrogen from the atmosphere. This contamination embrittles the weld zone and the heat-affected zone, sometimes reducing fracture toughness by 60 percent or more if the shielding is inadequate. Argon shielding is mandatory. Back purging is mandatory if the weld joint is accessible on both sides. I learned this on my first titanium TIG weld after a contractor complained that our pressure vessel coupons were failing bend tests at 90 degrees instead of the required 180. We had assumed that a standard argon flow rate from the torch was sufficient. It was not. The root side of the weld had oxidized to the point of severe embrittlement. The fix was installing a temporary back-purge fixture and maintaining argon flow on both sides throughout the entire weld and cool-down cycle, keeping the shield until the metal dropped below 600 degrees Fahrenheit. For automated welding, gas tungsten arc welding and electron beam welding are the standard processes. Laser beam welding has gained traction in recent years for precision joints where the smaller heat input minimizes the width of the heat-affected zone. Friction stir welding is emerging for titanium plate joining, offering excellent mechanical properties without the contamination risks associated with fusion welding.

Forming and Fabrication Considerations
Springback is the dominant challenge in titanium forming operations. Ti-6Al-4V has a modulus of elasticity approximately 55 GPa, roughly a third of steel's modulus. This means the material stores significantly more elastic energy during bending and releases it aggressively when the forming force is removed. Expect springback angles of 2 to 3 degrees for every 90 degrees of bend unless you intentionally overbend to compensate. Hot forming is commonly employed for complex geometries because it reduces the required forming force by 60 to 70 percent compared to cold forming. The standard forming temperature range for Ti-6Al-4V is between 700 and 950 degrees Celsius depending on the specific alloy condition and the severity of the deformation. Above 950 degrees Celsius, grain growth accelerates rapidly, and the mechanical properties of the finished part become unpredictable without controlled cooling. Surface treatment of titanium deserves attention because the natural oxide layer that provides corrosion resistance is also quite thin, typically 100 to 300 angstroms thick. For applications requiring enhanced wear resistance, anodizing, thermal oxidation, or physical vapor deposition coatings are applied. Plasma electrolytic oxidation produces a ceramic-like surface layer approximately 25 to 75 micrometers thick that significantly improves wear performance. However, this process alters the surface chemistry and can introduce microcracks in the coating if the voltage parameters are not carefully controlled.
Where Titanium Fails as a Solution
Titanium is not a universal solution and it is frequently specified inappropriately. The material cost ranges from $30 to $80 per kilogram for wrought bar stock depending on the grade and form. Machining costs are typically 3 to 5 times higher than equivalent steel parts due to slower cutting speeds, shorter tool life, and longer cycle times. If your application does not require the specific combination of high strength, low density, and corrosion resistance that titanium provides, you are spending money for no measurable benefit. Stainless steel 17-4 PH achieves comparable strength to annealed Ti-6Al-4V at less than half the material cost and machines at speeds three to four times faster. Aluminum 7075-T6 provides better specific strength than titanium for many structural applications where temperatures remain below 150 degrees Celsius. In these cases, choosing titanium is simply poor engineering economics. Titanium also has limitations in high-temperature applications that beginners often overlook. While Ti-6Al-4V retains useful strength up to approximately 400 degrees Celsius, above this temperature the aluminum content begins to oxidize selectively, and the alloy loses strength rapidly. For sustained service above 400 degrees Celsius, alpha alloys or newer beta-tungsten containing alloys are more appropriate, but they come with their own processing difficulties and significantly higher costs.
Selecting the Right Alloy for Your Application
The selection process should begin with a clear specification of the three most critical requirements: maximum operating temperature, required mechanical properties, and the corrosive environment the part will encounter. Everything else is secondary. For marine and chemical processing environments where chloride stress corrosion cracking is a concern, commercial pure titanium Grade 2 is often the most economical and reliable choice. It has excellent resistance to caustic solutions, chlorides, and oxidizing acids but performs poorly in reducing acids such as sulfuric acid at elevated temperatures. For aerospace structural components, Ti-6Al-4V remains the default choice for good reason. Its combination of strength, fatigue resistance, and fracture toughness is well understood by design engineers and manufacturers alike. The extensive database of material properties and established manufacturing processes reduces development risk significantly compared to less common alloys.

Medical implant applications require special attention to biocompatibility standards. Ti-6Al-4V ELI (extra low interstitials) is the standard material for most orthopedic implants. The reduced interstitial content improves ductility and fatigue performance, which is critical for implants that experience cyclic loading in the human body. Some newer implant designs use beta-type alloys such as Ti-15Mo for improved elastic modulus matching with bone, reducing stress shielding effects that can lead to implant loosening over time. The fundamental takeaway is straightforward. Titanium rewards careful engineering and proper process selection with outstanding performance. It punishes rushed decisions and inappropriate application with costly failures and unnecessary expense. Understanding the material's behavior under actual working conditions matters far more than memorizing property tables from a handbook.