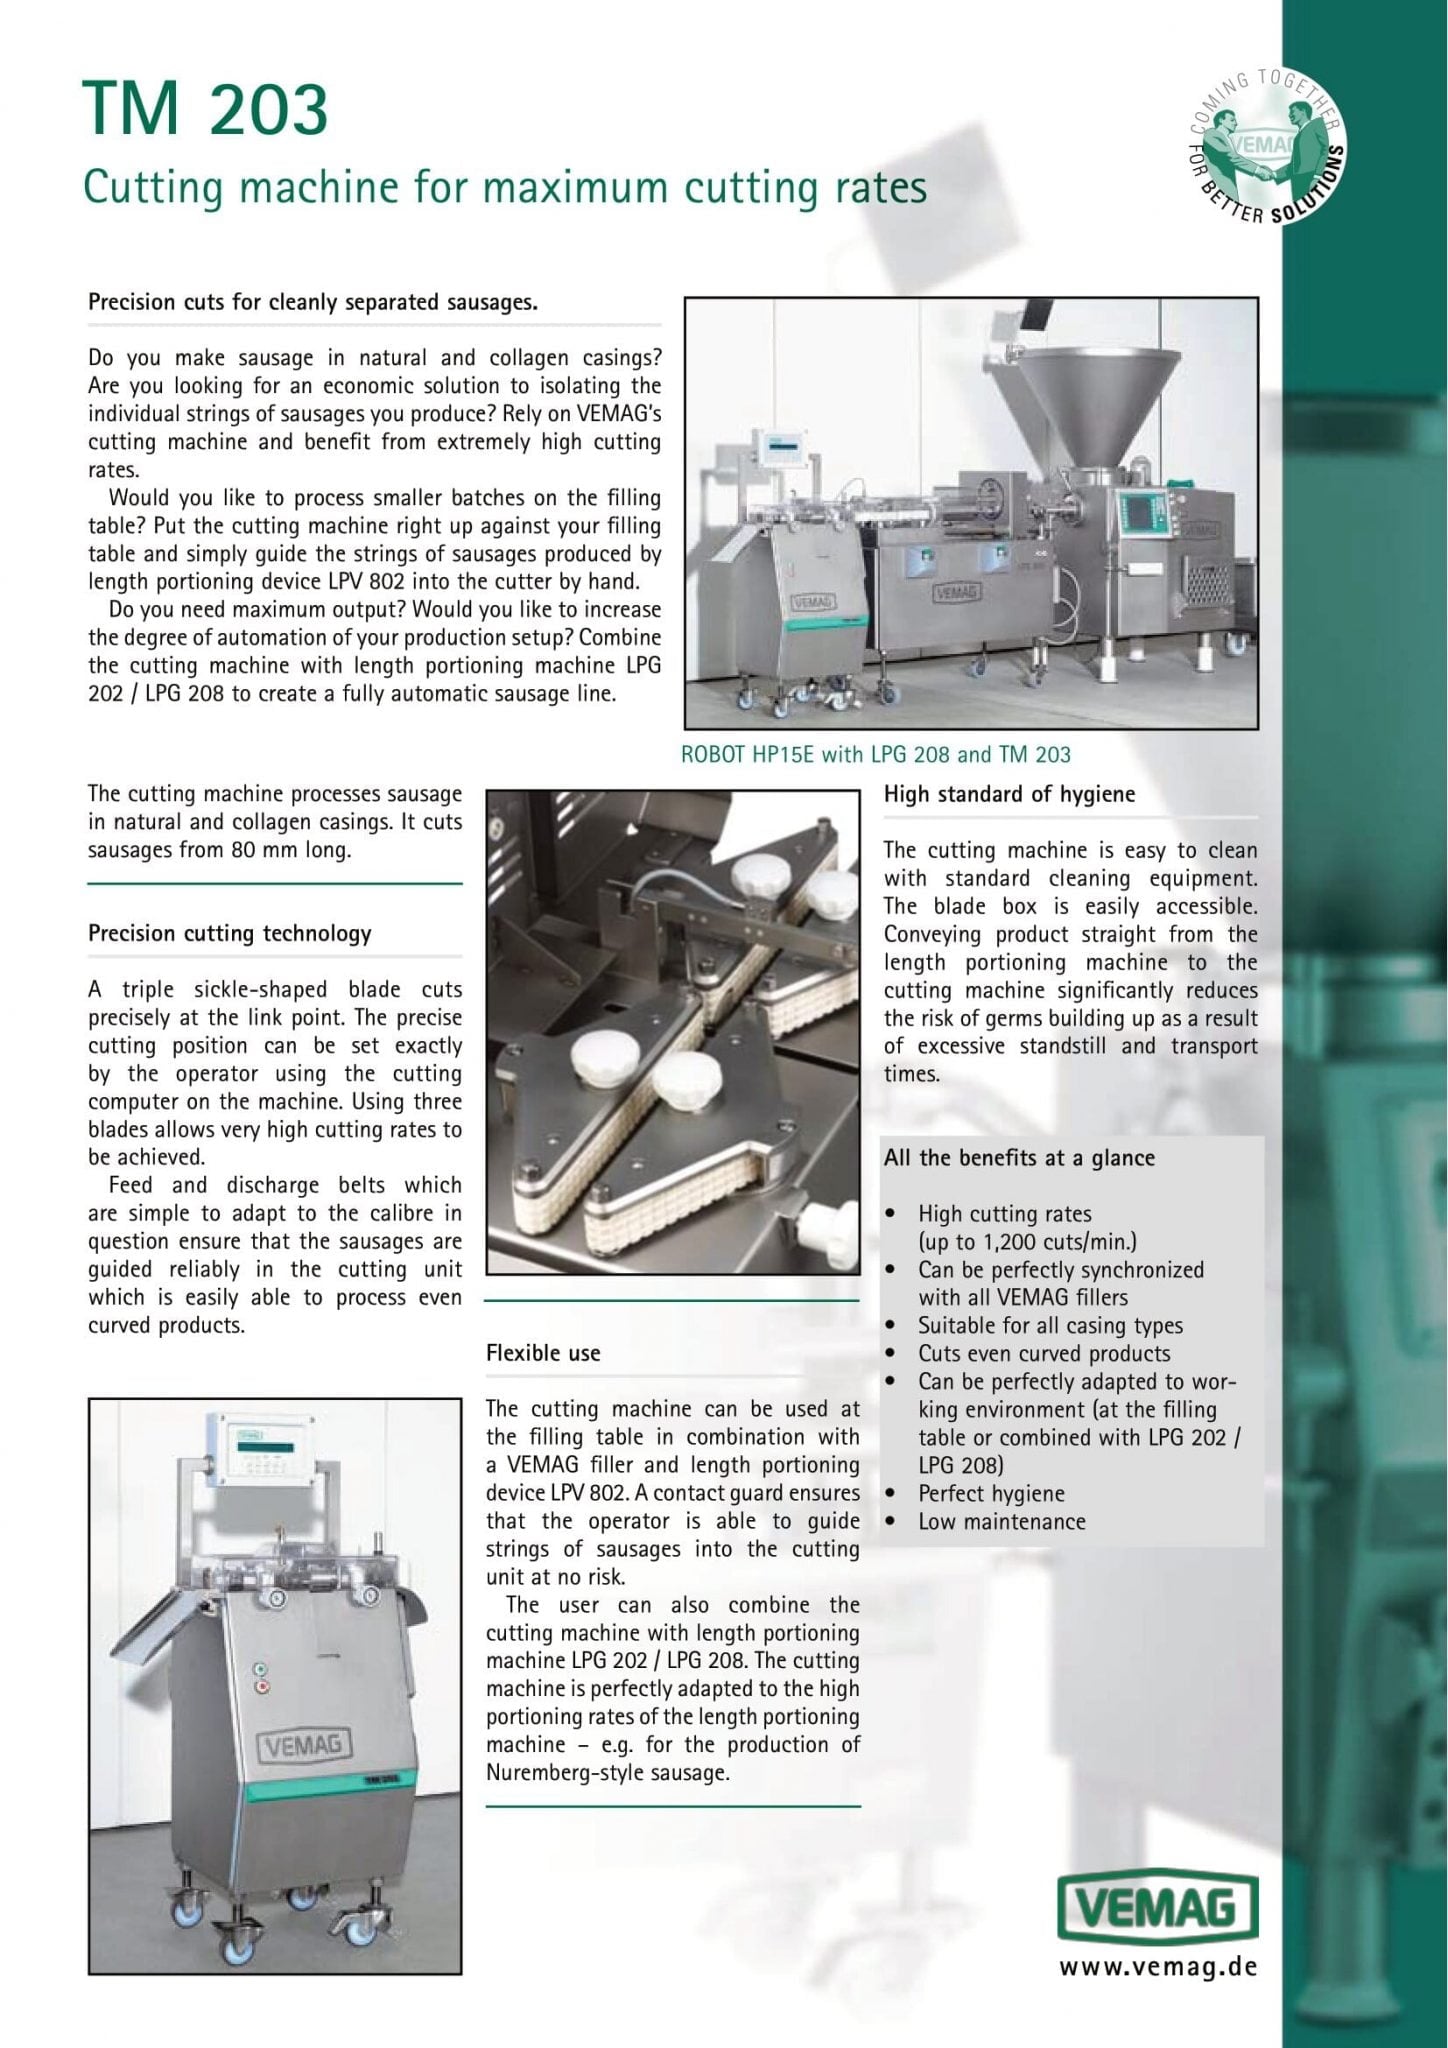
Getting Started With Your TM Cutting Machine
Most people pull these machines out of the box and immediately start trying to cut material without reading the manual. That is how you ruin a blade within the first week. The TM series is relatively straightforward but it has a few specifics that matter. I have seen too many operators skip the calibration step and then wonder why their cuts are drifting half a millimeter after an hour of runtime. These instructions are not just paperwork. The manual covers belt tensioning, blade alignment, thermal settings, and material feed rates. I will walk through the process in order because the sequence matters. If you tension the belts before you calibrate the blade path, the tension will shift during calibration and you will end up with inconsistent cuts. That happened to me on a Tuesday with a batch of 400 gsm board. I lost about sixty pieces before I realized the calibration had moved the knife carriage off-axis. Took me forty minutes to redo it properly. The first thing you need to do is power on the machine and let it warm up for at least fifteen minutes. Do not skip this. The thermal equilibrium affects the stability of the cutting bed and the blade housing expands slightly when cold. When the machine reaches operating temperature, run the self-diagnostics. The display will show you sensor readings for the Y-axis, X-axis, and blade height. All three should read within tolerance. If any axis shows an error code, stop and check the rail lubrication before proceeding. I recently had a unit throwing an E-04 fault on the Y-axis and it turned out to be a dried-out linear rail. A few drops of synthetic grease fixed it.
Blade Setup and Calibration
Blade selection depends entirely on your material. The TM cutting machine uses standard 54mm rotary blades but the thickness and coating of the blade matter more than people realize. For thin vinyl and adhesive films, use the standard blade at a 15-degree angle with a downward pressure setting of 120 grams. For heavier materials like corrugated board or foam board, switch to a serrated edge blade and increase the angle to 30 degrees with pressure around 200 grams. To install the blade, loosen the retaining screw with the included hex key, slide the blade onto the arbor making sure the flat side faces the motor, and retighten to 5 Newton-meters. Do not overtighten. I have stripped two arbor threads this way. A torque screwdriver makes this a five-second job instead of a guess. Calibration involves running the built-in test pattern. The machine will cut a series of squares and circles at varying speeds and pressures. You then measure the results with calipers and input the correction values into the control panel. The correction offsets compensate for blade deflection, which is the main source of dimensional inaccuracy. For most users, the default calibration profile works fine for light materials. Heavy materials require a custom profile. The difference between a properly calibrated machine and one that is not can be the difference between parts that fit together and parts that do not. This is not theoretical. I once had a client return a full production run because the corners were rounded by 0.8mm on a part that needed sharp edges for assembly. The fix was recalibrating with a zero-deflection blade and reducing the cutting speed from 400mm/s to 180mm/s.
Material Loading and Feeding
The cutting bed has an vacuum hold-down system. Make sure your material is flat and free of debris before engaging the vacuum. Even a small bump under the sheet will cause the blade to miss the surface at that point, resulting in incomplete cuts. I once spent twenty minutes debugging what I thought was a dull blade, only to find a stray screw on the cutting bed that was lifting one corner of the material by two millimeters. For roll-fed operations, set the registration marks and run a test strip before committing the full roll. The sensor needs to detect the mark consistently. If it is skipping, check the sensor alignment and clean the lens with isopropyl alcohol. Dust on the sensor lens is one of the most common causes of registration drift, and it is also one of the most overlooked.
Get the Full Details
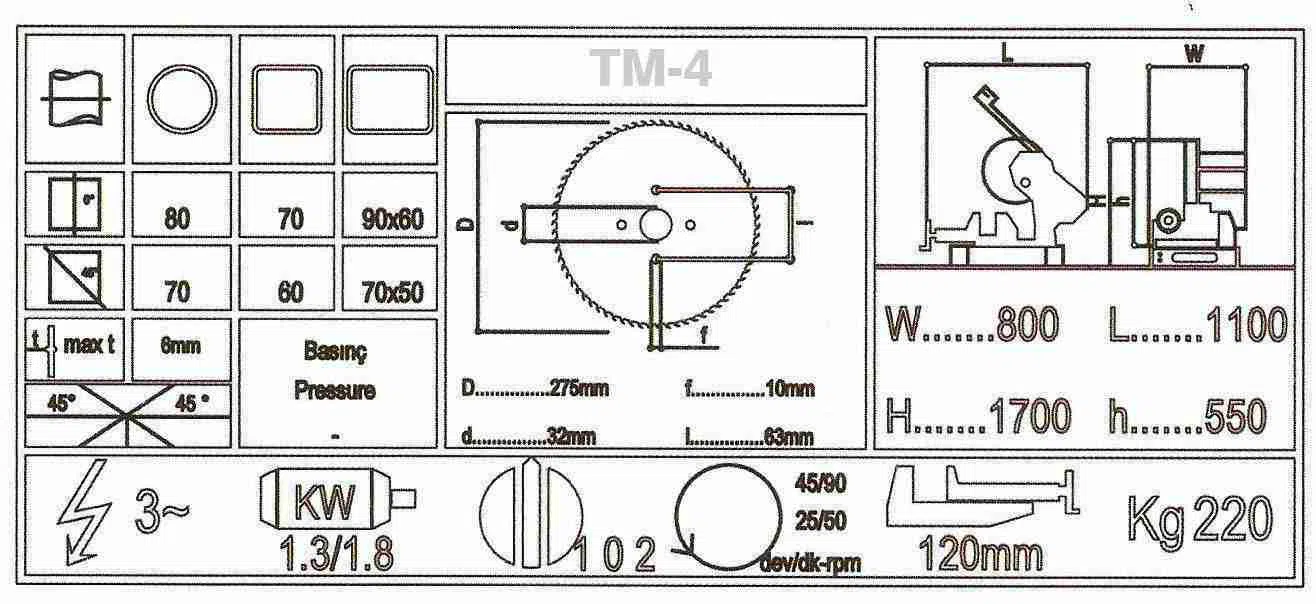
Operational Settings and Safety
The control software allows you to set multiple parameters: cutting speed, pressing force, blade rotation direction, and pause points. For production runs, save your settings as named profiles so you do not have to re-enter them every time. I keep separate profiles for each material type I use regularly. Switching between vinyl, foam, and cardstock used to take me ten minutes of adjustment. Now it takes three seconds to load the right profile. Always engage the safety guard before starting a cut. The blade rotates at high speed and the emergency stop is located on the front panel. Keep your hands clear of the cutting zone. I have heard stories about operators reaching in to clear a jam while the machine is still powered. Do not be that person. Lock out the power before clearing any obstruction. Additionally, monitor the blade temperature during extended cuts. The friction can heat the blade to over 80 degrees Celsius on long continuous runs. If the blade gets too hot, it can soften certain materials and cause tearing instead of clean cutting. Let it cool for a minute between batches if you are doing heavy work.
Maintenance and Troubleshooting
Clean the cutting bed after every shift. Residue from adhesive materials builds up quickly and affects vacuum hold-down performance. Use a soft cloth and mild solvent. Avoid abrasive cleaners. Inspect the belts monthly for wear and adjust tension if you notice any slippage during acceleration. The blade should be replaced when you see visible chips or when cut quality starts degrading even after adjusting pressure and speed. A fresh blade typically lasts between 8 and 12 hours of continuous cutting depending on material hardness. Common issues and their fixes: Incomplete cuts usually mean the blade is dull, the pressure is too low, or the material is not held flat. Check all three before assuming it is a mechanical fault.
Drifting dimensions point to calibration drift or belt slack. Re-run the calibration test and check belt tension. Noise during operation is often a sign of insufficient lubrication on the guide rails or a misaligned blade arbor. Clean and grease the rails, then verify the blade sits square on the arbor. The TM cutting machine is a solid piece of equipment when maintained properly. It will not compensate for poor setup habits, and some materials simply cut better on dedicated die-cutting equipment. If you are running very thick or very hard substrates regularly, you may find that a hydraulic die cutter gives you more consistent results. But for vinyl, foam, cardstock, and similar materials in the 0.1mm to 5mm range, this machine handles the work well within its specified limits.


