Getting Your Training Manual Synthesizer Up to Spec
I spent three weeks last year chasing oscillators that drifted off pitch after a thermal cycle in a mid-tier analog synth line. The factory specs sheet said +/- 5 cents over the operating range. We were hitting 40 cents. What fixed it wasn't a better calibration algorithm or a fancier temperature chamber. It was the manual. Most training manuals for synthesizer manufacturing skip the edge cases. They tell you how to calibrate a fresh board under ideal conditions. They don't tell you what to do when the VCO tuning pot is binding, or when the op-amp you swapped in has a different input bias current than the one the schematic called for. That gap is where production lines bleed time and money.
Why Training Manual Synthesizer Factory Specs Exist
Factory specs for a synthesizer training manual are really just a standardized way to communicate everything an operator needs to build, test, and ship a unit without needing a degree in electrical engineering or six months of apprenticeship. The spec includes tolerance tables, adjustment sequences, test point locations, and pass/fail criteria for every major subsystem. If you've ever watched a new tech spend forty minutes trying to get a filter to sweep cleanly because they didn't know which trimmer controlled resonance versus cutoff, you know why this matters. The training manual synthesizer factory specs serve two audiences. Line operators need enough detail to catch problems without guessing. Quality engineers need the same manual to validate that the line operators are actually following procedure. Those two needs often conflict, which is why the best specs I've seen include a separate escalation matrix that tells you when to stop and call a senior tech instead of pushing forward. One thing beginners consistently miss is that factory specs are living documents. A manual that was valid when your synthesizer design went into production won't necessarily remain valid after a component substitution six months later. I learned this the hard way when a vendor quietly changed the tolerance band on a batch of potentiometers. The training manual still said the old values. We shipped forty units before anyone noticed the impedance mismatch was causing audible crackle on the filter section. The fix was both a manual update and a full retrain, which cost us roughly two days of lost output on that line.
The Core Components of Factory Specs
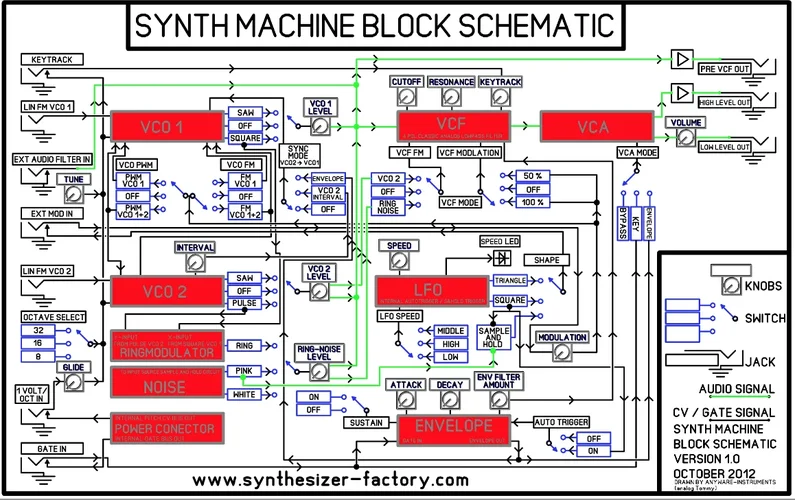
A complete training manual synthesizer factory specs package should cover at minimum the oscillator section, the filter, the amplifier stage, the modulation sources, and the control voltage routing. Each section needs its own calibration procedure, test equipment requirements, and acceptance criteria. Don't combine them into a single undifferentiated block. Operators will skip the parts they find tedious, and those are exactly the parts that cause failures down the line. VCO calibration is usually the first step and also the most common source of errors. The spec should list the reference frequency standard to use, the expected tuning range, and the maximum acceptable deviation at each point across the octave span. I've seen specs that only check the top and bottom notes and call everything else fine. That misses nonlinearity in the tuning curve, which is exactly what causes a synth to sound in tune at middle C and sharp at the high end. The test procedure should require a full sweep from the lowest to the highest note, recording each reading. Then it should require a return sweep back down to confirm hysteresis isn't introducing additional error. If your spec only asks for one direction, you're missing half the picture. This doubles the time per unit during initial calibration but cuts the return rate in the field by a significant margin. Worth it.
Get the Full Details
Filter Section Testing
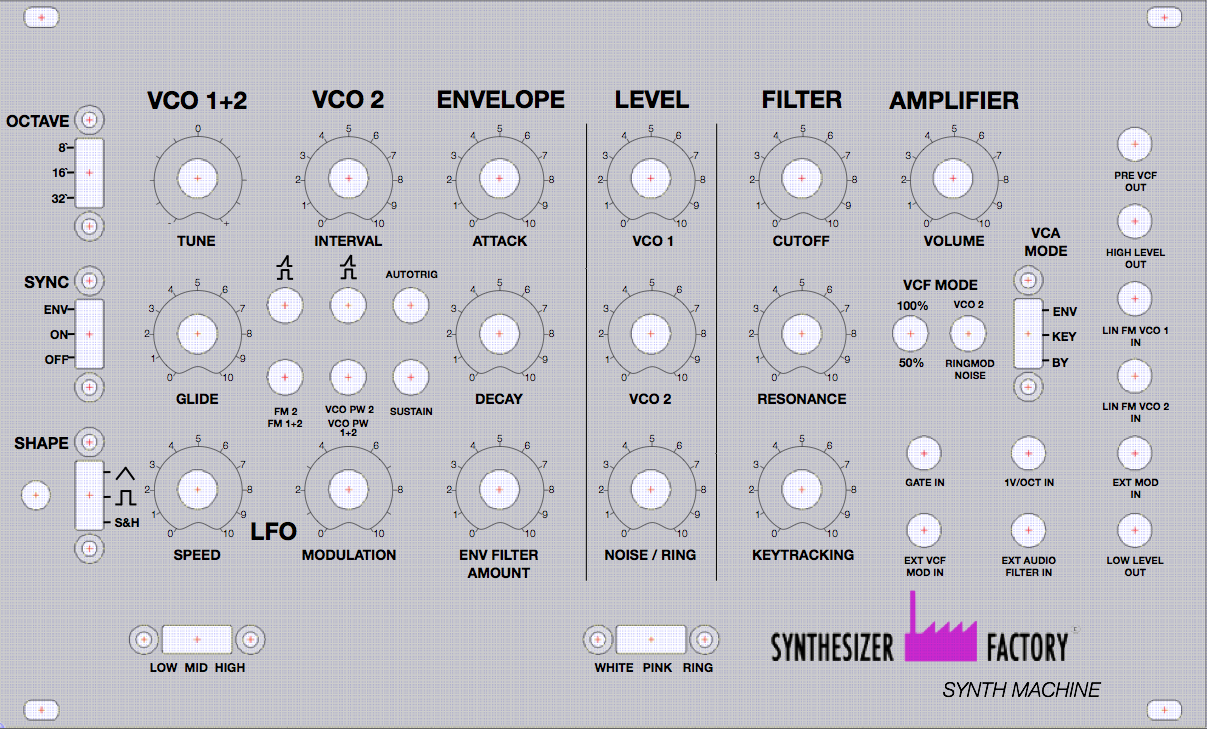
Filter specs tend to be vague because filter behavior depends heavily on the oscillator driving it. The training manual should specify the exact input signal characteristics: amplitude, frequency, and waveform. Resonance self-oscillation tests need a defined threshold. I recommend marking the exact dB level where the filter starts to oscillate on its own and requiring that measurement to fall within a narrow band. Anything outside that band usually indicates a component value shift or a PCB trace issue that won't show up on simpler tests. Another often-overlooked test is the skirt slope check. Measure the attenuation at a frequency one octave below the cutoff point and one octave above. Compare against the theoretical slope for the filter topology you're using. If you're building a 24dB per octave ladder filter and the measurement comes in at 16dB per octave, something is wrong with the cascade arrangement or the coupling capacitors. Write that into the spec. Most manuals don't bother.
Amplifier and Output Stage
Output stage specs should include DC offset measurement at the main output. Even a few millivolts of DC offset can damage speakers and causes unwanted pops during power cycles. The spec should also define maximum ripple at rated output and minimum signal-to-noise ratio with all controls at their normal operating positions. Include a test for gain staging across the entire control range. Some units will have perfectly fine specs at unity gain and terrible specs at maximum output because the gain staging between stages isn't properly matched. I once calibrated a batch of units where the DC offset spec was met but the pop test consistently failed at the output jack. The root cause was a capacitor in the protection circuit that was charging too slowly. The factory specs didn't include a pop test because nobody thought to add one. After we added it, the failure rate dropped and we caught three other subtle issues in the same test cycle. Add a simple pop test to your spec sheet. It takes thirty seconds per unit and saves you warranty claims.
Calibration Sequence and Workflow
The order of calibration operations matters more than most manuals acknowledge. If you calibrate the filter before the oscillators, the filter response you measure might change once you re-tune the oscillators later. The correct sequence runs from the most fundamental signals outward: power supply first, then oscillators, then filters, then modulation, then the output stage. Each step should have a clear go/no-go decision point. Don't let operators continue down the line if an early step fails. I've seen too many instances where a tech calibrates the VCO successfully, moves on, and returns two hours later to find the filter won't tune because the VCO had drifted after the power supply settled. The initial VCO calibration was technically correct at the time it was done. It just wasn't stable. Include a settling time requirement in the spec. After powering up a unit, wait a specified duration before beginning any calibration measurements. For most analog synthesizer designs, this is between fifteen and thirty minutes. The spec should state the exact number for your particular design. Don't leave it to the operator's judgment.

Test Equipment Requirements
List every piece of equipment needed for the calibration process with acceptable tolerance ranges. A multimeter that reads to three and a half digits is fine for checking resistance values but inadequate for measuring the sub-millivolt DC offsets that matter in output stage testing. The training manual should specify minimum instrument grades for each type of measurement. This prevents operators from using whatever spare equipment is lying around and wondering why their results don't match the spec sheet. Include a calibration date requirement for all test equipment. If an oscilloscope probe compensation is off by even a small amount, it can introduce measurement errors that look like synthesizer faults. Operators will spend time chasing ghosts. The spec should require probe verification at the start of each shift and document the verification result.
Documentation and Traceability
Every calibrated unit should have a data record. This record includes serial number, operator ID, calibration date, test equipment lot numbers, measured values for each critical parameter, and the pass or fail determination. Modern factory systems can automate much of this through direct instrument communication. Older facilities rely on manual entry. Either way, the training manual should specify exactly what gets recorded and where it gets stored. Data retention policies should be explicit. Some specs require records for the product lifetime. Others require five years. Define it in the manual. I've worked at facilities where the spec was vague about retention and we kept records for three years before realizing a recall notice had come in and we had no way to trace which calibration batches the affected units came from. That was an expensive lesson.
Common Pitfalls in Factory Spec Implementation
Specification creep is a real problem. Every time a quality engineer finds a marginal case, there's a temptation to add another test or tighten a tolerance. Before long, the calibration process takes three times longer than the design intends and the line can't meet its throughput targets. The training manual should include a formal revision process that requires approval from both engineering and production management before any spec change goes into effect. A single change might save you a few bad units but cost you ten times that in labor hours across every unit produced thereafter. The opposite problem is spec stagnation. The manual gets written and never updated. This happens frequently when a design is modified for cost reduction or performance improvement and the training documentation doesn't get revised in parallel. Every version change on the schematic should trigger a review of the corresponding training manual section. Make this a tracked item in your engineering change process, not an informal suggestion. Another frequent failure mode is inadequate coverage of environmental conditions. Factory specs are typically written and tested in a climate-controlled environment at room temperature. Real-world conditions vary. If your synthesizer uses components with temperature coefficients that aren't accounted for in the spec, units will drift when they reach customers in different climates. Include temperature and humidity ranges in your spec documentation. If the design can't meet specs across a reasonable operating range, that's a design issue, not a manufacturing one, and it needs to be flagged before you ship anything.
What This Doesn't Cover
These specs address the analog signal path. Digital control layers, MCU programming, firmware validation, and MIDI implementation are entirely separate domains with their own testing requirements. If your synthesizer design includes a digital interface section, you'll need an additional spec package for that portion of the build process. Combining analog and digital testing into a single manual usually results in neither being treated with adequate attention. Keep them separate and reference each from the main document. The training manual synthesizer factory specs I've described here are a foundation. They won't prevent every possible failure mode, and they certainly won't replace experience on the line. But they will catch the issues that cause the most downstream problems: oscillators that drift, filters that don't behave as designed, and output stages that introduce noise or distortion into the signal path. That's most of what actually matters in practice.