Understanding TTT Diagrams Without Losing Your Mind
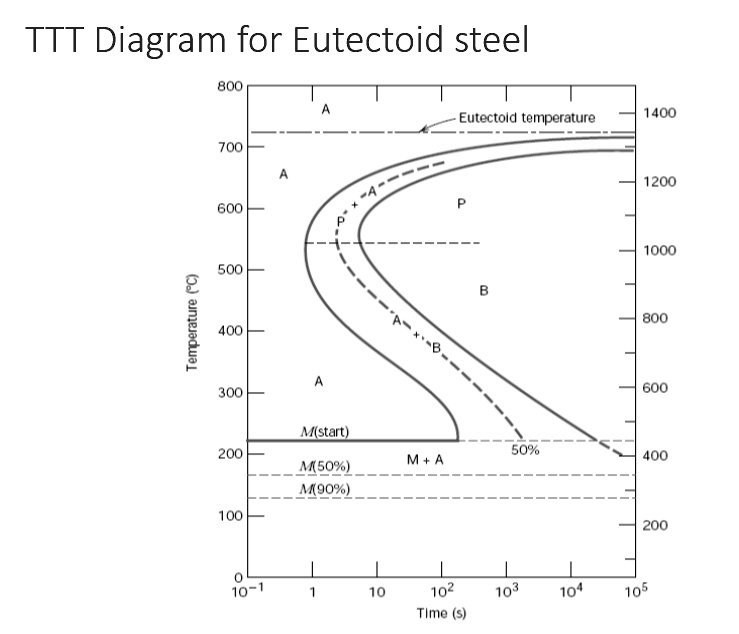
TTT diagrams are one of those things everyone in metallurgy has to deal with eventually. Time-Temperature-Transformation diagrams show you what happens to steel when you cool it down from the austenite region. The curves tell you when pearlite forms, when bainite starts appearing, and where martensite kicks in. That is the basic version. The actual application is messier. I spent years working with medium-carbon steels in heat treatment operations. The first time I tried to interpret a TTT diagram for actual production work, I learned pretty quickly that the textbook version assumes conditions you will rarely see outside a lab. The diagram I used for 4140 showed a nice clean pearlite nose around 550°C with a start curve and finish curve neatly separated. What actually happened in the furnace was different because the cooling rate through that nose region depends on part geometry, furnace atmosphere, and exactly how the steel was austenitized beforehand. Here is the practical way to read these diagrams. You need three sets of curves. The first set marks when transformation starts. The second shows when it finishes. The third, usually further to the right, indicates where martensite begins and ends. The martensite start temperature is designated as Ms and the finish as Mf. Between these points you get a mixture of phases. Below Ms you are mostly dealing with martensite, though some retained austenite might still be hanging around depending on the alloy content.
The critical insight that most people miss is that TTT diagrams are only valid for a specific starting condition. If you austenitize at a lower temperature than what was used to generate the diagram, your grain size changes and the whole curve shifts. Fine grains push everything to the right. Coarse grains do the opposite. I learned this the hard way when a batch of 1045 steel came back with inconsistent hardness after normalizing. The diagram I was following assumed a grain size that our normalizing cycle didn't produce. We adjusted the holding time at austenitizing temperature and got consistent results within two runs. Another thing nobody warns you about is the difference between TTT and CCT diagrams. Continuous cooling transformation diagrams are often more useful for actual heat treatment because they reflect what happens when you cool at a steady rate rather than holding at constant temperatures. Most commercial steel suppliers provide CCT data now, but older references and some educational materials still push TTT diagrams as the primary tool. They are related but not interchangeable. Using a TTT diagram for quenching predictions will give you optimistic results compared to what actually occurs during continuous cooling. If you are looking for actual diagrams, the best sources areASM Handbooks Volume 1 and 4, which have comprehensive TTT data for most commercial alloys. Some steel manufacturers like Bethlehem Steel and US Steel publish their own proprietary diagrams for specific grades. There are also digitized versions floating around on university metallurgy department sites, though the accuracy varies depending on how well they preserved the original curve data.
Common Mistakes That Waste Time and Material
I have seen people use TTT diagrams for stainless steels without realizing that austenitic stainless steels do not transform the same way as carbon and low-alloy steels. The diagram you pick up for 4140 will not help you with 304 stainless at all. You need separate diagrams for each alloy family. Martensitic stainless steels have their own curves and the chromium content shifts everything significantly compared to plain carbon steels. The iso-temperature transformation regions matter too. When you are holding at a specific temperature in the bainite region, the diagram tells you when transformation starts and finishes at that temperature. But in practice, getting the entire cross-section of a part to that temperature takes time, and during that soak period partial transformation may already be occurring at the surface. This is why quenching media selection and agitation matter just as much as the diagram itself. A diagram does not account for your quench severity. One edge case I ran into involved thin sections versus thick sections of the same steel. The TTT diagram is based on thermal equilibrium assumptions that break down with large thermal gradients. A 25mm bar and a 5mm bar of the same 4340 steel will follow completely different paths even in the same quench bath. The thin section might hit martensite while the thick center stays in the bainite or pearlite region. I solved this by combining the diagram with simple Arccool calculations and validating with hardness profiles across cross-sections. The diagram alone would have led me to specify a faster quench that would have cracked the thin sections.
Get the Full Details

Retained austenite is another area where diagrams can mislead you. The Mf temperature on a TTT diagram might suggest complete transformation to martensite, but many alloy steels have Mf temperatures below room temperature. After quenching, you can end up with significant retained austenite that softens the part over time or causes dimensional changes during service. Temper painting or cryogenic treatment are common remedies, but the diagram itself does not tell you this. You have to know the alloy composition and calculate the Ms and Mf points using formulas like the one from Andrews or independently derived equations based on chemical composition. The practical takeaway is that TTT diagrams are starting points, not answers. They give you the phase diagram landscape under ideal conditions. Your actual process needs to account for part geometry, heating rates, quench severity, and the difference between isothermal and continuous cooling. Spend time with the diagrams, learn to read them, but never treat them as gospel. Validate with test coupons and hardness measurements every time you change a variable, and you will save yourself a lot of scrap and rework.