Working Through a Turbo Blue Torch Assembly
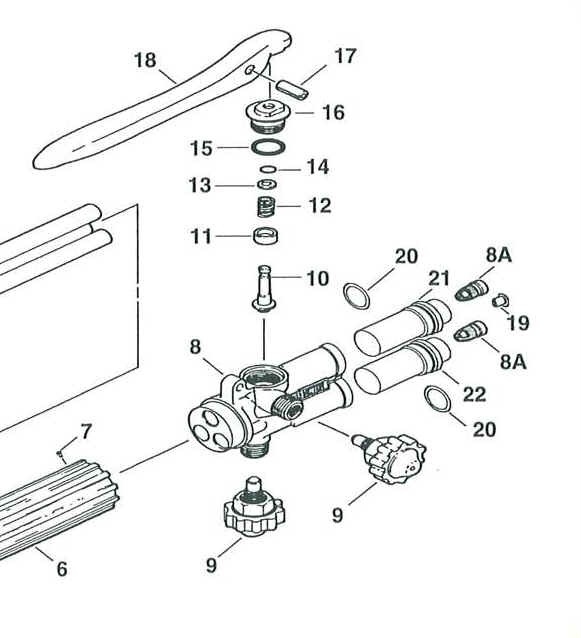
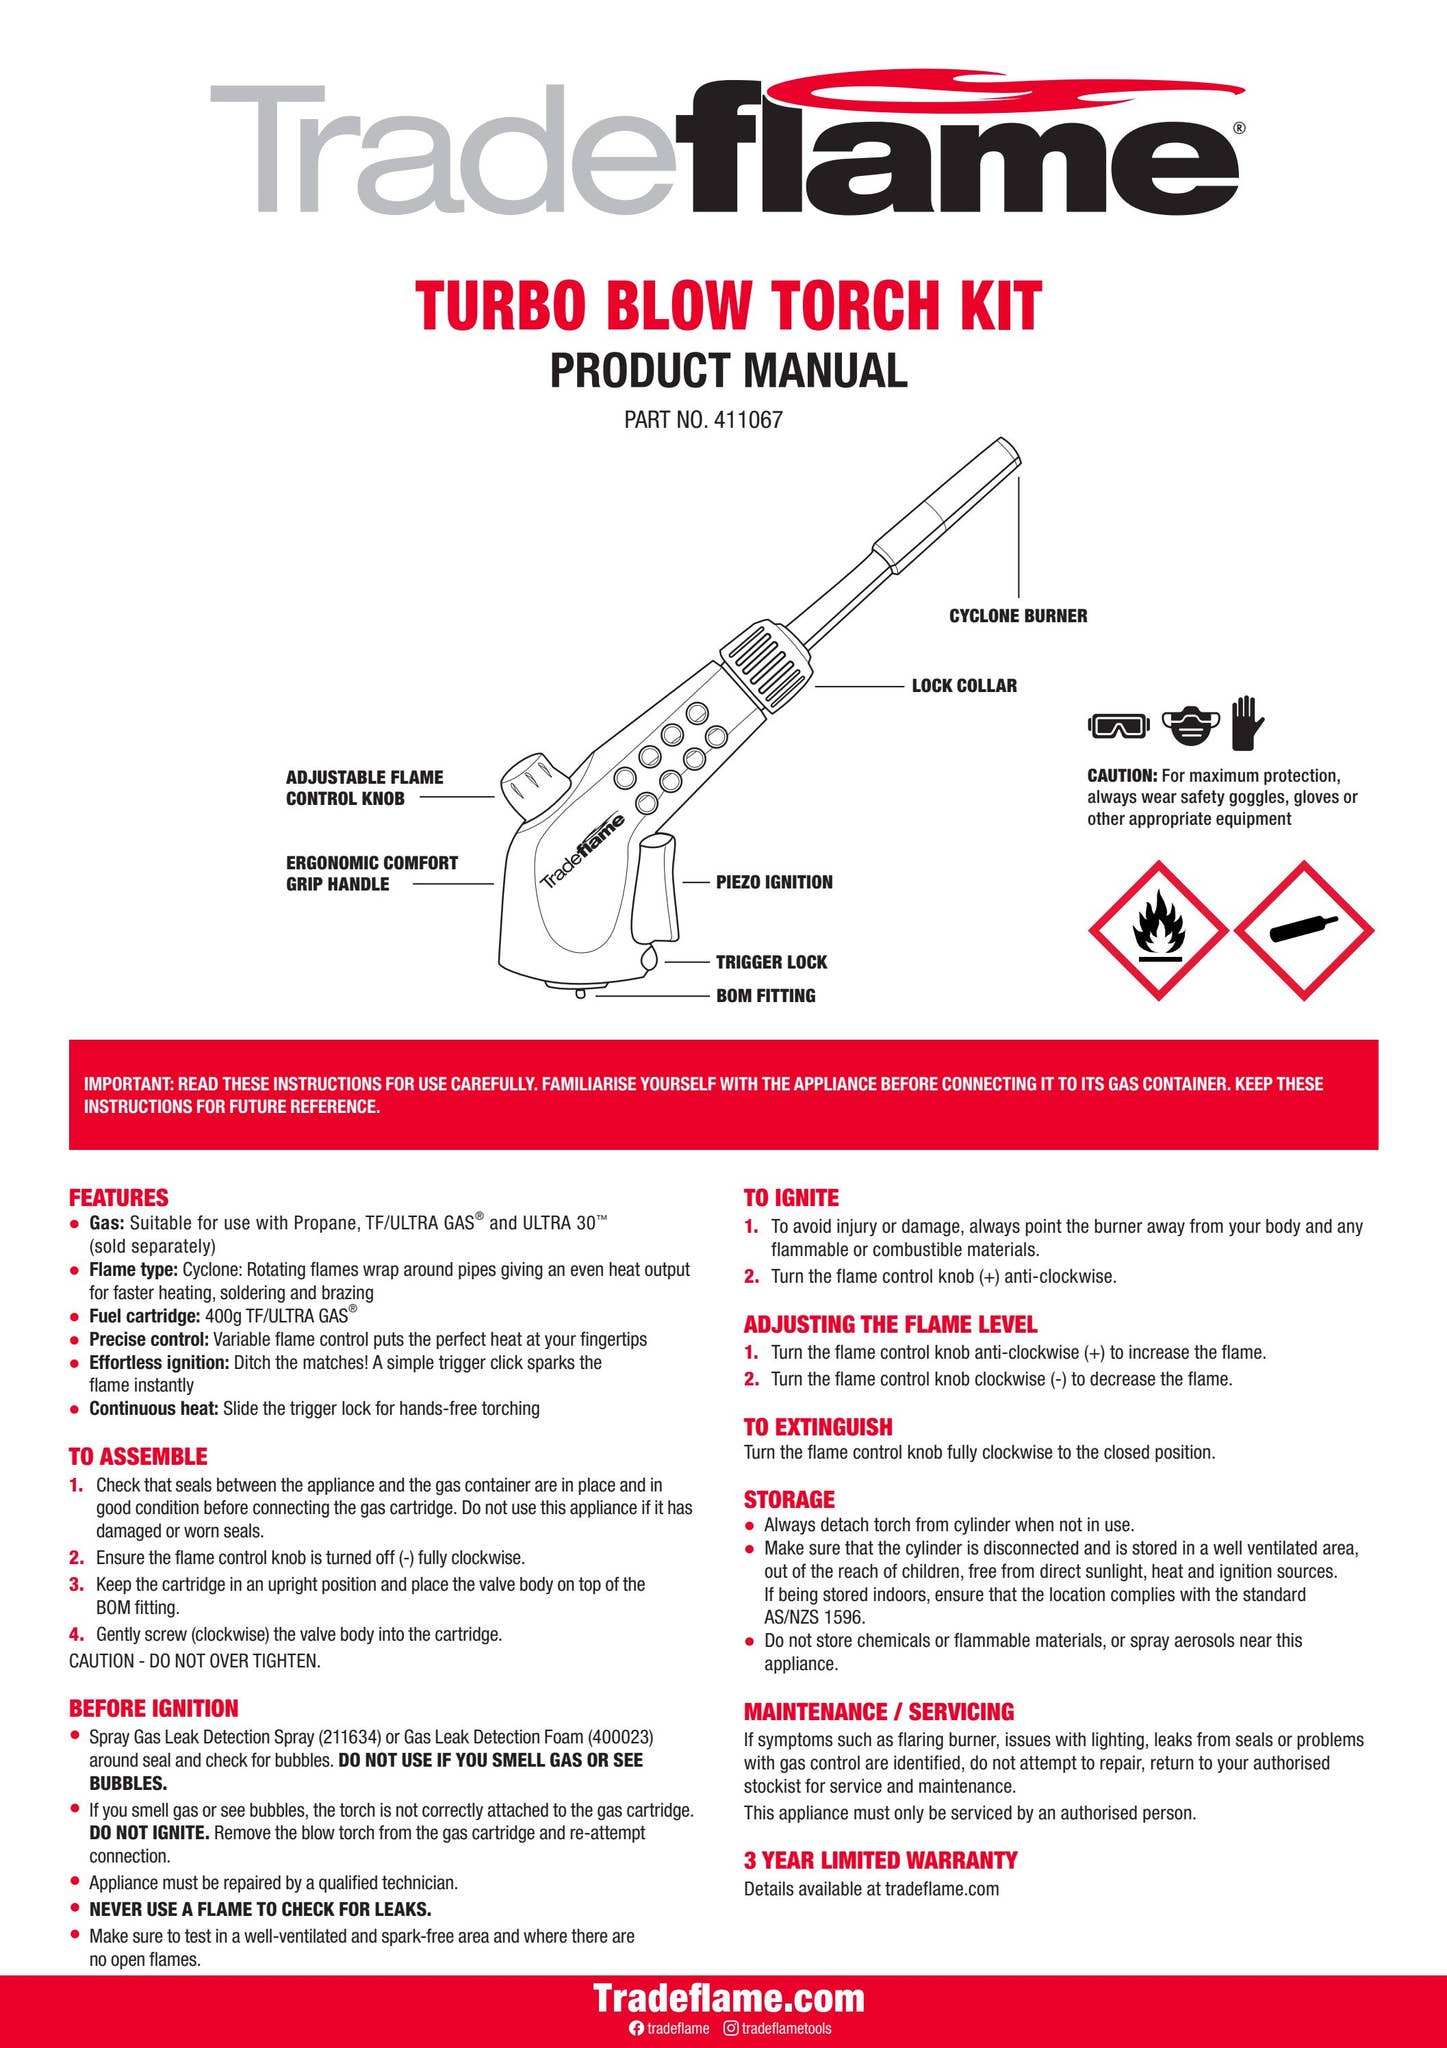
I ran into this when a shop called me in about a blue flame torch that wouldn't hold pressure past about 40 PSI. Turns out the upstream regulator and the torch body had different thread pitches than what was stamped on the parts. Anyway, if you're looking at a Turbo Blue Torch Assembly Diagram, it's basically the parts map for getting a pressurized oxy-fuel torch put together correctly so it doesn't leak, flashback, or fail mid-job. The diagram breaks down into five main sections: the handle grip and trigger mechanism, the gas inlet and shank, the mixing chamber with its venturi tube, the barrel or torch tip stack, and the oxygen/fuel delivery manifold. What most people miss is that the venturi tube inside the mixing chamber has a specific orientation. The tapered side faces the fuel inlet, not the wide side. I learned that the hard way replacing a worn jet on a Mark IV model — took three attempts to get the flow right after I reversed it on the second rebuild. Here's how the actual assembly goes:
Start with the trigger assembly. Install the spring retainer pin first, then the main return spring, then the trigger blade, and finally the retainer clip. Don't torque anything here. The spring needs to seat freely. If it binds, your trigger response will be sluggish and inconsistent, which matters when you're trying to transition from cutting to welding mode. Next is the gas inlet section. The fuel line connects to the rear of the torch body through a compression fitting. Most assemblies use a 3/8-inch compression nut with a brass ferrule. Finger-tighten first, then give it an additional quarter-turn with a wrench. Over-tightening this fitting cracks the brass ferrule and you'll have a small fuel leak that smells terrible and creates a genuine safety issue. Under-tightening gives you the same problem but harder to find because the gas escapes slowly. The mixing chamber comes next. This is where the oxygen and fuel meet. In a turbo blue torch, the oxygen is supplied at higher pressure than the fuel, which draws the fuel into the stream through the venturi effect. The diagram will show you the exact position of the oxygen valve and the fuel adjustment needle. These two controls don't operate independently. Opening the oxygen valve first, then adjusting the fuel, gives you the cleanest blue flame. Flip that order and you'll get a sooty yellow flame that deposits carbon on whatever you're working on and makes your eyes water.
The barrel and tip section is straightforward but easy to strip. Use the correct tip size for your application. A #2 tip on a medium-pressure setup will flame out if you try to cut through more than quarter-inch mild steel. I've seen people force it by cranking the pressures way up past the manufacturer's spec. That melts the tip seating surface and you end up replacing the whole barrel assembly instead of just a thirty-dollar tip.
Get the Full Details
Parts and Specifications You Need to Know
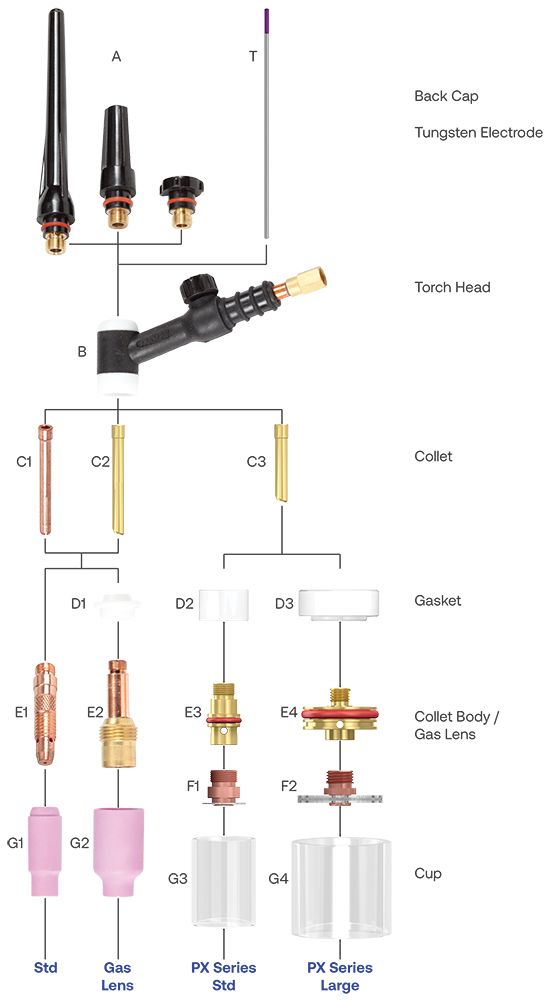
Standard turbo blue torch assemblies use 1-inch NPT threads for the oxygen inlet and either 3/8 or 1/2-inch NPT for the acetylene or MAPP gas line. The torch body itself is usually brass or stainless steel depending on the price tier. Cheap ones are brass and will develop micro-cracks after two or three years of regular use, especially around the valve seats. Mid-range and professional models use stainless steel bodies which handle thermal cycling much better. The spark igniter on these torches is piezoelectric. You press a button, it generates a spark inside the mixing chamber, and the gas mixture ignites. The igniter tip needs to be positioned exactly 1.5 millimeters from the mixing chamber entrance. Too far and the spark won't cross the gap. Too close and it gets coated in carbon every time you light it and stops working within a week. I mark mine with a tiny dot of nail polish once I get the gap right so I can tell at a glance if it's drifted. The flame arrestor is a critical component that most people ignore until it clogs. It's a small metal mesh screen sitting inside the barrel near the tip. Its job is to prevent flashback — that's when the flame travels backward through the gas lines instead of burning at the tip. A clogged arrestor shows up as a hissing sound coming from the torch body during operation and a noticeable drop in flame temperature. Clean it with compressed air monthly. Replace it if you see any discoloration or melted mesh. That costs about eight dollars and prevents the kind of damage that costs eight hundred in torch replacement.
Common Problems and What to Check First
If the torch won't light, check the spark gap before you touch anything else. That's the single most common failure point. If the spark is weak or absent, the igniter cartridge itself might be failing. These last a long time but they do wear out. A new one runs about fifteen dollars. Leaking gas at the connection points almost always means the compression fitting wasn't seated correctly or the ferrule is damaged. Remove the fitting, inspect the ferrule, replace it if there are any visible deformities, and reassemble. Don't reuse a deformed ferrule. It won't seal properly and will leak again within hours. A flame that won't stay lit after initial ignition usually means the thermocouple or flame sensor is misaligned. The flame needs to actually touch the sensor element, not just hover near it. Adjust the sensor position by about half a millimeter toward the flame centerline. This resolved a recurring issue on a customer's unit where the flame would ignite and then die after four or five seconds. Turns out the tip was slightly clogged from prior over-fueling, which pushed the flame tip away from the sensor just enough to break the holding circuit.
Where to Find the Diagram
The Turbo Blue Torch Assembly Diagram is available directly from the manufacturer's website under the support and documentation section. It's also on the packaging insert for new units, though those copies are often faded and hard to read after a few years in a hot tool shed. Third-party sites sometimes have them but I wouldn't trust versions found there against the official document because the part numbers and thread specifications need to match your exact model. The diagram on the official site matches the parts list on the box — that's your verification method. These torches are designed for light to medium-duty fabrication work. Thin sheet metal, small repairs, bench-level welding, and general heating tasks. They're not suitable for thick structural steel work, heavy casting repair, or continuous industrial use. If you need those capabilities, you're looking at a different class of equipment with separate regulators, larger tips, and often a dual-hose design instead of the single-handle setup. Trying to push a turbo blue torch past its rated capacity just destroys components and creates unsafe conditions. The flame temperature peaks around 3,500°F with the right gas mix, and that's sufficient for materials up to about half-inch thickness in practice. Beyond that, you're fighting physics and losing. One thing worth noting: these torches are sensitive to oxygen pressure variance. If your shop air compressor or oxygen tank output fluctuates more than ten percent from your set pressure, the flame will become unstable. That's normal for the design. If you need consistent performance under variable supply conditions, you should look into installing a dedicated pressure regulator between your supply source and the torch inlet. It adds about twenty dollars and eliminates a lot of troubleshooting time.