V Belts Are Everywhere and Nobody Remembers the Part Numbers
You open a maintenance cabinet and there are boxes stacked floor to ceiling, most of them labeled in fading marker or not at all. Someone replaced a belt three years ago and wrote "A42" on the bag. The actual belt inside says "A48/3". You try to order from a distributor and everyone speaks a different language. This is why cross reference work exists. It isn't glamorous. It gets done. A V Belt Cross Reference Guide is simply a mapping table that lets you take a manufacturer's part number—say, a Gates B100—and find the equivalent from another brand, like Optibelt or Habasit, with matching cross-section, effective length, and material rating. The goal is to prevent ordering the wrong belt during a downtime situation. Most guides exist as PDFs from the major belt manufacturers, and many of them are also available on sites like Motion, Misumi, and even McMaster-Carr. I keep a local copy of the Gates/Optibelt/ContiTech table bookmarked because I've pulled it more times than I can count.
V Belt Cross Reference Guide Basics
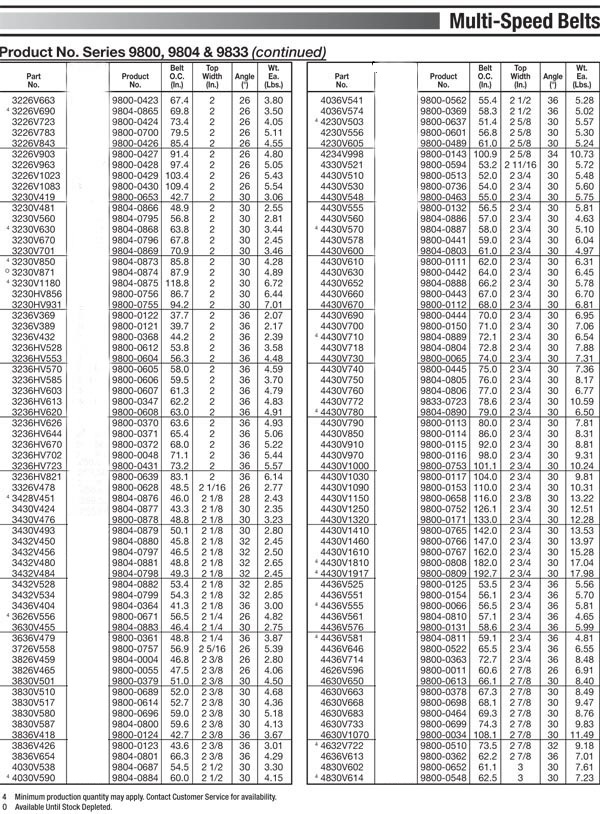
The first thing you need to understand before you look up any number is what the belt's code actually tells you. V belts have a nominal top width and a height that define their cross-section. The letter codes are standardized across most of the industry: A section: top width around 1/2 inch, height about 3/8 inch. B section: roughly 17mm top width, 10.3mm height. C section: about 22mm by 13mm. D and E sections are large industrial types you see on heavy conveyors and steel mill drives. There are also narrow belts like 3V, 5V, and 8V—those are not the same as the classical A/B/C series and mixing them up is an easy way to shut down a line. The number after the letter encodes the effective or outside length. A B100 belt is approximately 100 inches in outside circumference. The difference between effective length and outside length matters when you're fitting a belt onto existing sheaves. Effective length is the pitch length where the belt actually transmits power. Outside length is what's stamped on the belt and what you'll measure with a tape. Most catalogs list both. If you only have the outside measurement, your cross-referenced replacement needs to match within a tolerance of about 0.5 percent for length, or you'll be stretching the tensioner to its limit and still running hot.
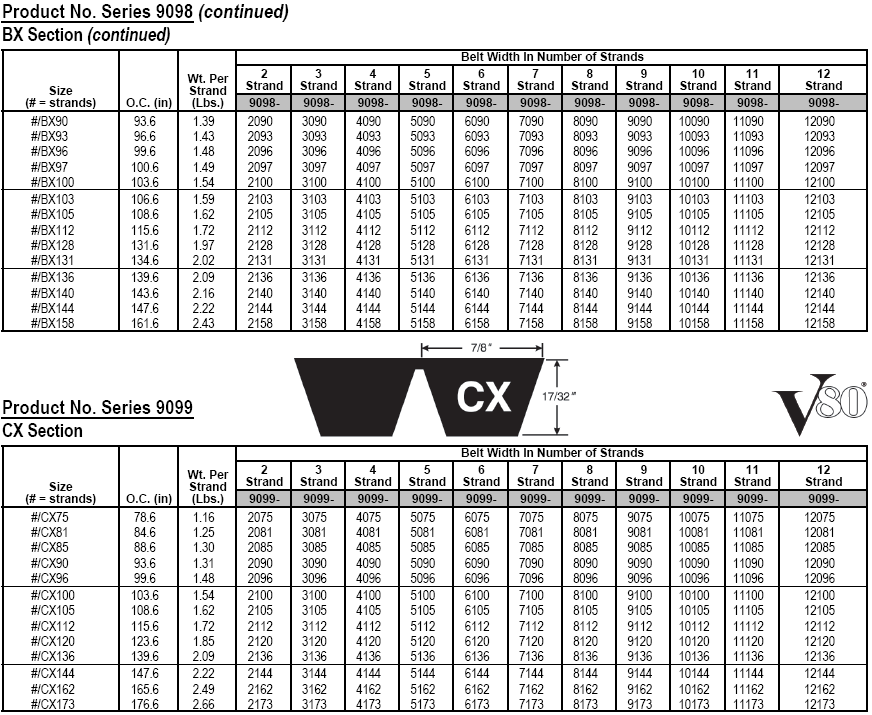
Here's the practical workflow I use. When a belt fails on the floor, I remove it and read whatever is legible. If the marking is worn off, I measure the top width with calipers and the overall outside length with a tape. Then I round to the nearest standard size. If the width comes out to 16.5mm, that's a B section. If it's 12.7mm, that's an A. For narrow belts, 3/8 inch width points to 3V, 5/8 inch to 5V. Once I know the section and the length, I go into the cross reference table and pull the equivalent from whichever manufacturer my distributor carries that day. In my experience, this takes me about 15 minutes from removing the old belt to placing the order, compared to 45 minutes or more if I'm calling around without the table open. The counter-intuitive part that catches people is that not every "equivalent" is truly equivalent. Cross reference tables are built on nominal dimensions. They do not account for belt construction differences. A Gates B75 and an Optibelt B75 will fit the same sheave and have the same outside length, but one might be wrapped in neoprene and the other in polyurethane. One might have a cord grip made of polyester and the other of aramid. That changes heat resistance, chemical compatibility, and lifespan. If you're running a belt in a high-temperature environment above 150 degrees Fahrenheit, swapping a standard neoprene-wrapped belt for an equivalent poly-V or urethane option might look fine on paper and fail within weeks. Always check the compound rating, not just the dimensions. Another thing nobody tells beginners is that sheave compatibility is a silent failure point. A belt marked as a direct cross-reference might have a slightly different root radius or side angle. Classical A-section sheaves are nominally 36 degrees. Some aftermarket sheaves run 34 degrees. The belt will seat, it will look correct, and it will slip under load within a month. I ran into this exact problem on a conveyor drive that used ContiTech BX212 belts on sheaves I'd replaced from a discount supplier. The cross reference table said BX212 matched the Optibelt equivalent perfectly. It did, dimensionally. But the sheave groove had a 34.5-degree profile instead of 36. The belt tracked fine at idle, then walked off the sheave after three weeks of operation at full load. The workaround was to source sheaves from a manufacturer that guarantees 36-degree grooves for classical sections, and I stopped using the cheap equivalents entirely for anything running more than 12 hours a day.
Get the Full Details
Where to Find Reliable Tables and What They Miss
Gates publishes their cross reference tables openly on their website. Optibelt does the same. ContiTech and Habasit make theirs available through dealer portals. You can also find compiled references on engineering sites like Isoliq and Belt Specialist. I usually download the Gates table and the Optibelt table and keep them side by side. The two occasionally disagree on narrow belt equivalences, and when they do, I verify by checking the actual dimensional drawings rather than trusting either table blindly. The biggest limitation of any cross reference guide is that it assumes standard manufacturing tolerances and standard operating conditions. It does not help you when you need a belt rated for food-grade oil resistance, or UV exposure, or anti-static properties in a grain handling facility. It also does not handle custom-length orders well. If you're working with a non-standard center distance and need a belt cut to an exact length, the tables won't give you a clean match. You'll end up selecting the nearest stock length and adjusting the center distance with a tensioning mechanism, which works until the machine doesn't have enough adjustment travel. For those cases, the better approach is to measure the old belt's pitch length directly using a belt measuring tool or by wrapping it around a known-length reference and calculating. Then use the manufacturer's custom catalog rather than a general cross reference table. Gates and Optibelt both offer custom-length classical and narrow belts in most sections, and the lead time is usually three to five business days. That's faster than the two-week downtime caused by guessing with a standard-size substitute.
One more thing that trips people up regularly: dated reference charts. I found a printed Gates table from 2012 on a shelf in a warehouse that listed some obsolete part numbers as direct equivalents to current ones. The belts themselves have changed over time, and manufacturers drop lines or rebrand. Always verify the publication date on any reference guide you're using. If it's older than five years, check the manufacturer's current website to confirm the part still exists under the same number.
Practical Quick Reference for Common Sections
A section (classical): top width approximately 1/2 inch or 12.7mm, height 1/4 inch or 6.35mm. Outside length codes are in inches. A common replacement chain runs from Gates A-series to Optibelt R-A to ContiTech SPZ. Don't confuse SPZ with A. SPZ is a metric narrow belt equivalent that is slightly different in profile. It fits some A-section sheaves but not all, and the load rating is different. B section (classical): top width 17mm, height 10.3mm. Gates B to Optibelt R-B to ContiTech SPB. Again, SPB is the narrow-metric cousin of B, not an exact dimensional twin. 3V narrow belt: top width 9.5mm, height 8mm. This is a fractional-horsepower narrow belt. Gates 3V to Optibelt 3VX to ContiTech XPZ. These are closer matches than the classical-to-narrow conversions I mentioned above, but still check the sheave groove specification before committing.
5V narrow belt: top width 16mm, height 15mm. Gates 5V to Optibelt 5VX to ContiTech XPH. Used on mid-range industrial drives. C section (classical): top width 22mm, height 13mm. Gates C to Optibelt R-C to ContiTech SP C. These are heavy-duty and common on large fans and compressors. When you're working with these conversions, the rule of thumb is that classical and metric narrow belts are interchangeable only when the sheave manufacturer explicitly states it. Most sheave catalogs note whether a groove is designed for classical A/B/C or for narrow 3V/5V/8V. If the catalog doesn't specify, assume they are not directly swappable and test fit before running a full production order.
What I Do When the Table Doesn't Have an Answer
Sometimes the belt is an old imported unit with Japanese or European markings that don't appear in the standard Western tables. JIS standards use different length measurement conventions. A Japanese belt marked with a metric length like "1250" might be 1250mm of pitch length, not outside length. If you treat it as an outside length and search for a Western equivalent, you'll end up with a belt that's too short by several inches. I've had to deal with this on a legacy packaging machine that came from a German supplier. The belts were marked B140, but when I measured the outside circumference, it came out to 3550mm, which is a B140 in JIS metric terms, not the American B140 which is 140 inches. The workaround was to send a photo of the belt marking and the sheave dimensions to the supplier's engineering support and ask for the exact equivalent. They confirmed it was a B140JIS and pointed me to an Optibelt R-B1400, which is the metric narrow equivalent. The entire process took about an hour instead of the two days I would have wasted on wrong substitutions. If you're maintaining equipment that has been modified over the years with mismatched sheaves and belts from different eras, a cross reference table alone won't solve the problem. You need a measurement protocol: document the sheave pitch diameters, measure the center distance, record the actual belt outside length, and then select the replacement based on those measurements rather than the faded stamp on the old belt. I keep a simple spreadsheet for each machine with these values, and it has saved me from ordering the wrong belt more times than I want to admit. The tables are useful, but they are starting points, not final answers. The real work happens in the details—compound ratings, sheave groove angles, length conventions, and whether the belt is running in a condition the standard tables were designed for. Keep a current reference open, measure everything twice, and don't assume a match on paper means a match on the line.