Why Most People Get Belt Sizing Wrong
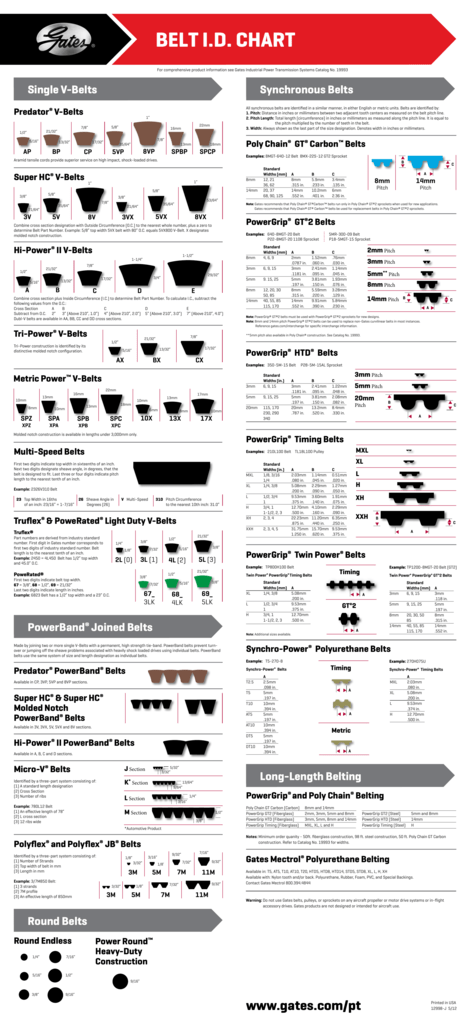
The main issue I see on the shop floor isn't that people can't measure a belt. It's that they measure the wrong thing and call it a day. A lot of folks grab a tape, measure the outside circumference of an old belt, flip through a chart, and buy what looks close. That approach works until the new belt slips immediately or the motor doesn't track right. The difference between a belt that lasts six months and one that lasts six years is usually just knowing how the sizing system actually works. V Belt Size Guide isn't one single chart. It's a family of measurement systems that overlap in confusing ways. You've got the old imperial numbers like 3L475, the metric equivalent AX42, and then the wedge belt designations like SPZ or SPA that serve completely different applications. If you're replacing a belt on a machine that's been running for twenty years, the label might be faded or stamped in a spot you never noticed before. That's when the real work starts.
How to Actually Measure a Worn V Belt
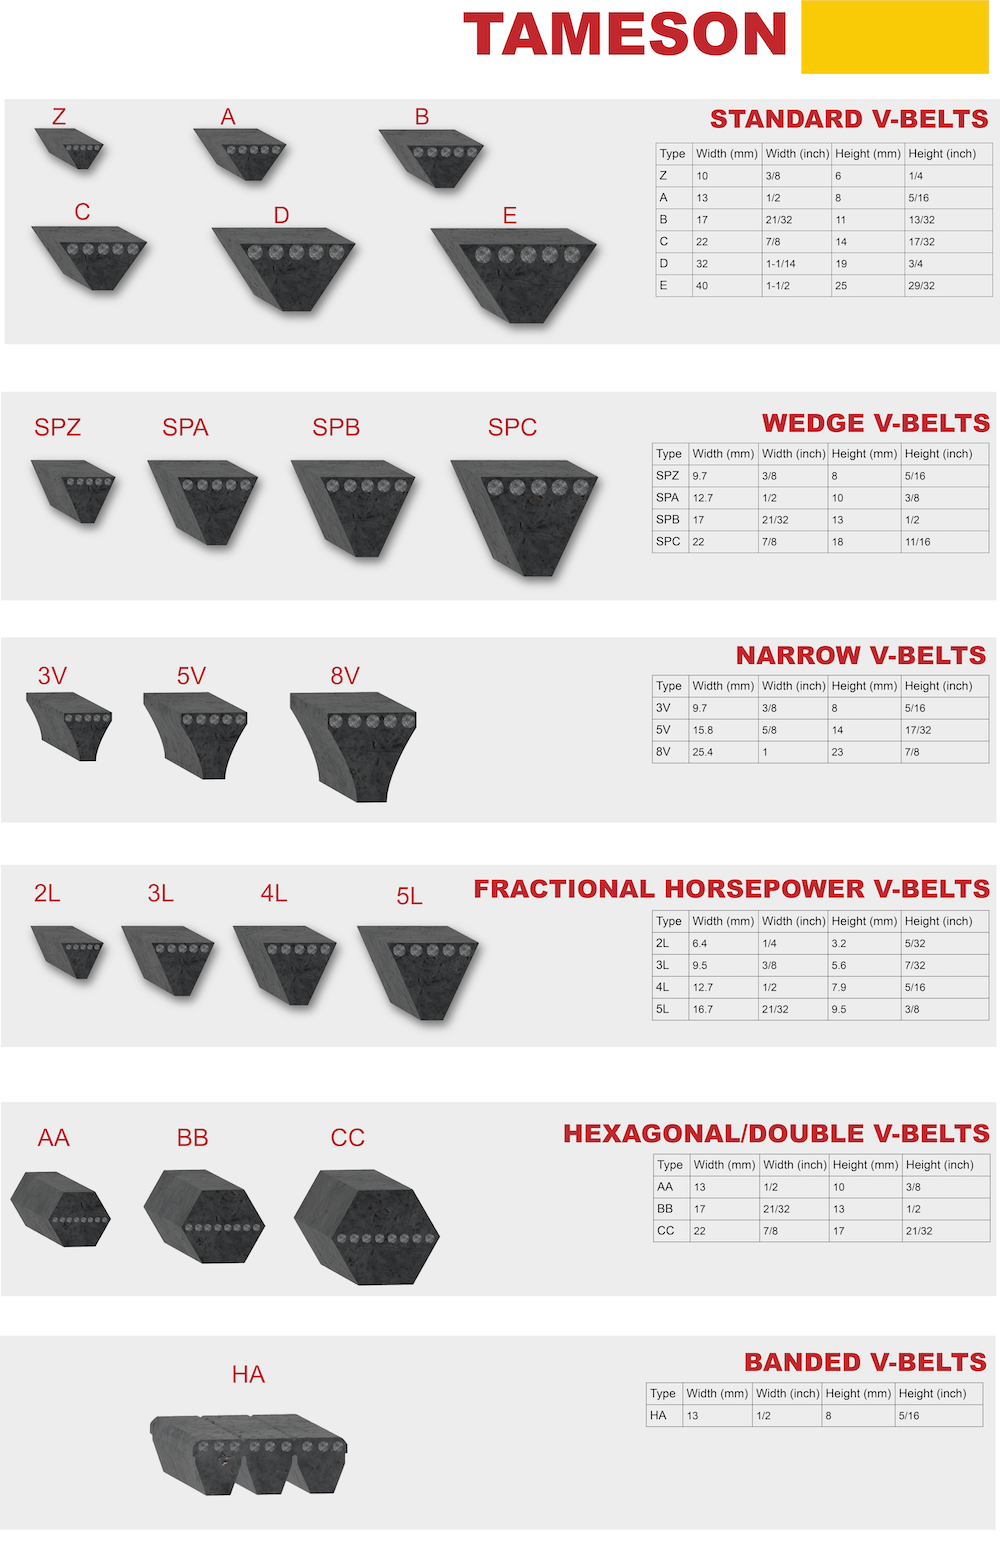
Start with what's still readable. Most belts have the size code molded into the inner surface. If you can find it, great. But these days a lot of OEM belts have the part number on the outer diameter surface where heat and friction eventually rub it smooth. I've worked on conveyor drives where the code was completely gone from both sides because someone over-tightened the belt years ago and it glazed over. When the code is gone, you measure the top width and the effective outside length. For classical cross sections, the top width is the critical dimension. An A-section belt is one inch wide at the top. A B-section is 13 millimeters, roughly half an inch. That measurement alone tells you the cross section. Then you measure the outside circumference with a flexible tape. Don't wrap it tight. The tape should sit against the belt without compressing the material. A 5L250 belt has an outside circumference of about 250 inches. The designation tells you the nominal size directly. For the narrow wedge types, the numbering system is different. An SPA1400 belt means the effective length is 1400 millimeters and the top width is 15 millimeters. The codes SPZ, SPA, SPB, and SPC represent four different wedge cross sections that all share the same groove profile family. They are not interchangeable. I've seen a maintenance tech try to swap a SPZ for an SPA because they looked similar on the pulley. The groove angle is the same at 40 degrees, but the belt sits at a different depth and the compression on the sides is completely off. The belt would ride out of the groove under load within a week.
Understanding the Cross Section Systems
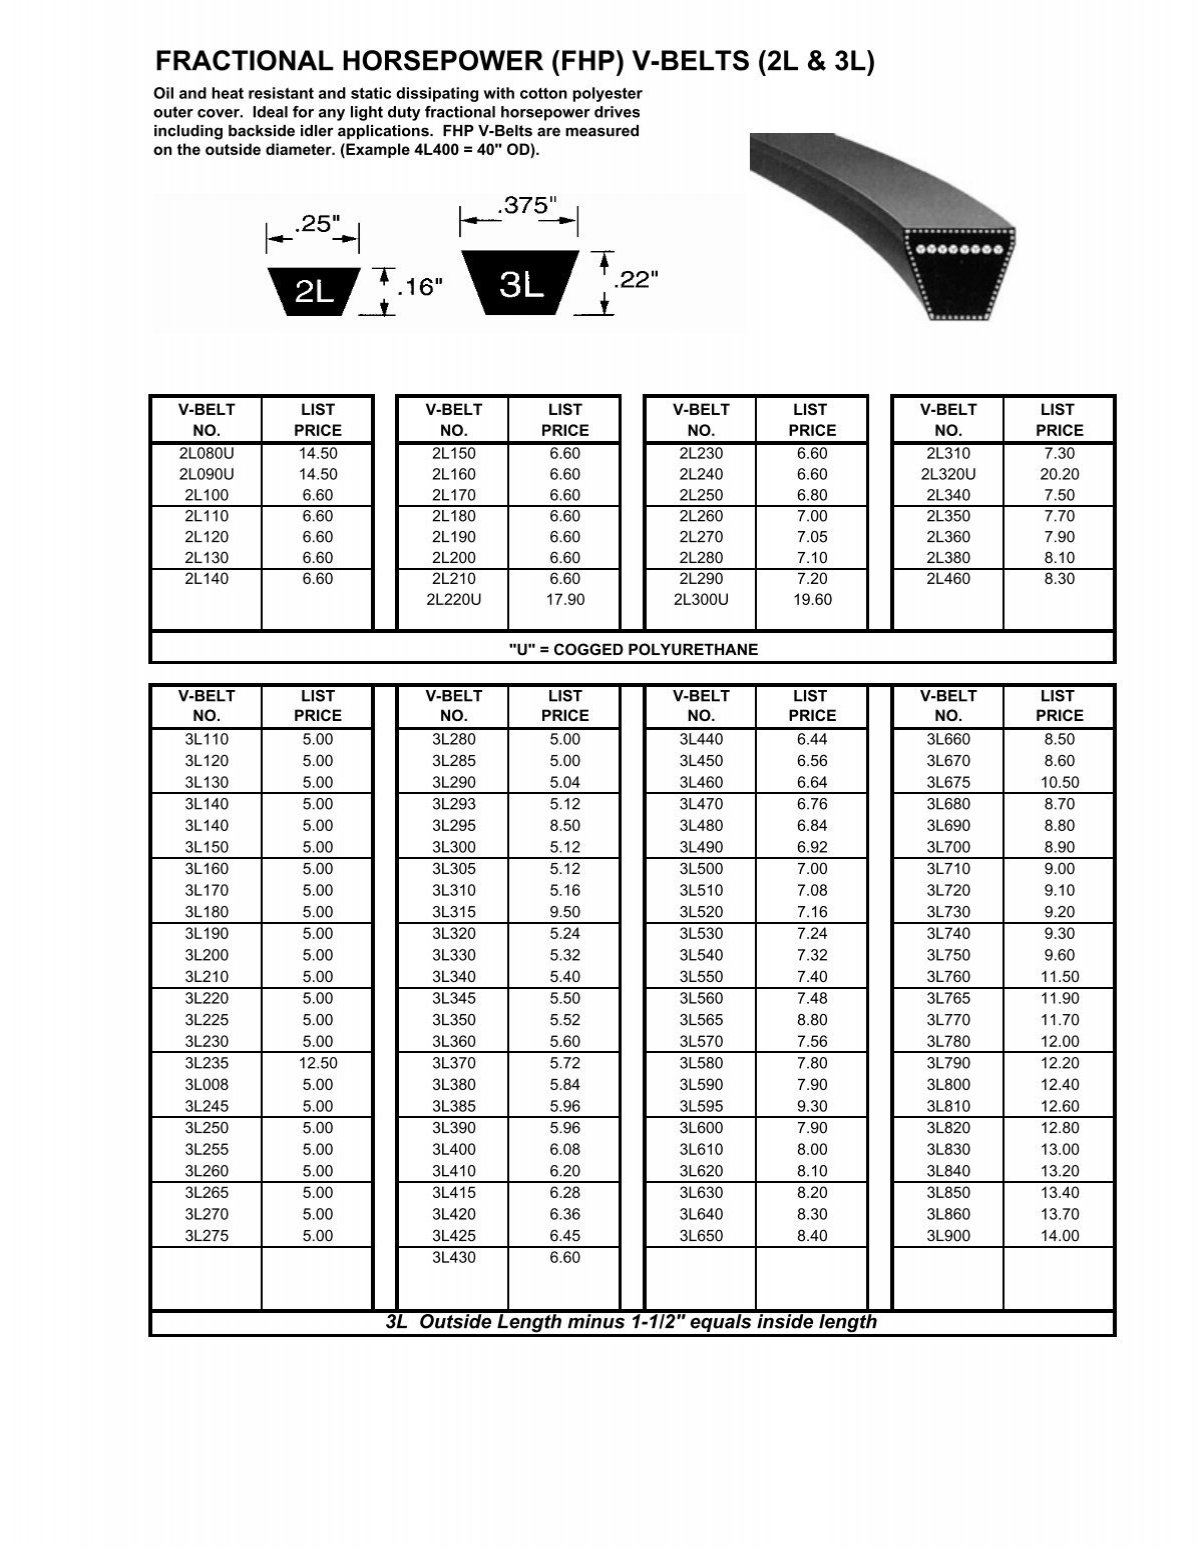
The classical V belt sections run from A through E in order of increasing size. A is the smallest and E is the largest. The metric equivalents use an X prefix followed by a number. AX replaces A, BX replaces B, and so on. The relationship isn't perfectly linear because the imperial and metric systems define the groove geometry slightly differently. An AX belt measures 12 millimeters at the top instead of exactly one inch. That one millimeter gap matters when you're working with a pulley that's worn to a specific groove profile. The 3L and 4L sections belong to the fractional horsepower belt family. These are the thin, narrow belts used on lawn mowers, small compressors, and light industrial machinery. A 3L475 has an effective length of 47.5 inches and a top width of 3/8 inch. The 4L series is wider at half an inch. The difference between 3L and 4L is small but it determines which pulley grooves fit. A pulley cut for 3L will accept a 4L belt loosely, but the belt won't seat properly and will vibrate itself out of the groove. I pulled one of these apart once on a vintage woodshop lathe. The original 3L belt had been swapped for a 4L by someone who thought the wider belt would last longer. It hadn't. The pulley was already worn wide from the improper seating. The L-section belt, sometimes called the light duty class, sits between the fractional horsepower types and the classical A section. It has a top width of 5/8 inch and is used on medium duty applications. The designation looks like L500 or L600. The number is the effective outside length in tenths of an inch. An L500 is 50 inches outside circumference. This is one area where the numbering is actually consistent and reliable. Just make sure you know whether the measurement is effective length or outside length. Some manufacturers list outside length and some list pitch length. They differ by roughly two inches on most common sizes.
Get the Full Details
Where People Go Wrong and How to Fix It
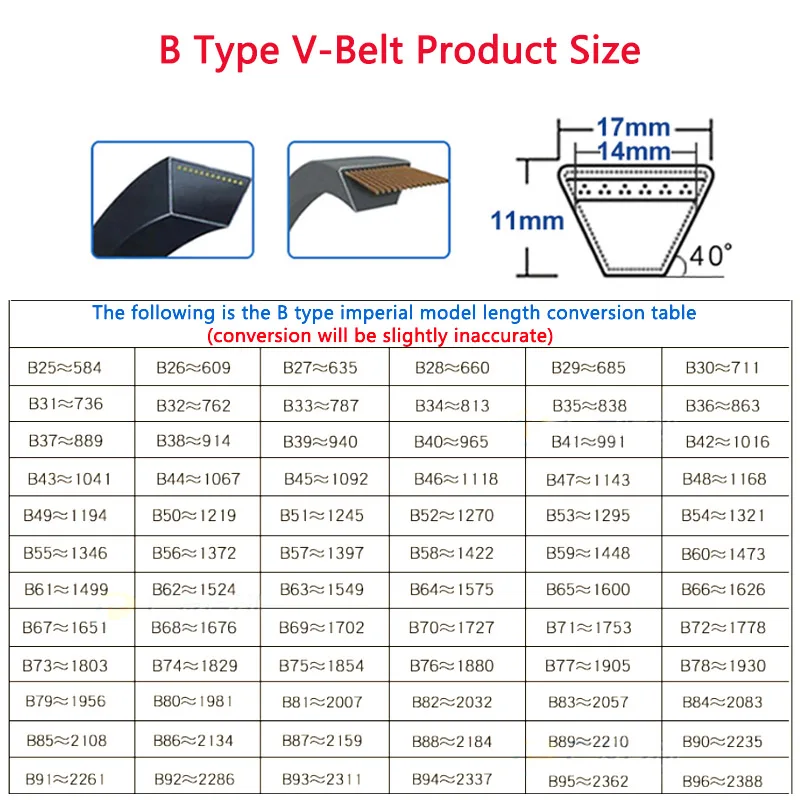
The biggest mistake is assuming that two belts with the same outside circumference will work interchangeably in different cross section families. They won't. A classical A belt and a narrow wedge SPA belt might both measure around 60 inches on the outside, but they sit in completely different pulley grooves. The A section has a trapezoidal profile with a 40 degree angle and a flat bottom. The SPA wedge has a more triangular profile designed to grip the sides of a narrower groove. Put an A section in an SPA pulley and it bottoms out. Put an SPA in an A pulley and it wobbles. Another issue is old imperial belts that use the old numbering convention where the number represents the outside circumference in inches times ten. A 5L2120 means 212 inches outside circumference and a 5L cross section, which is 17 millimeters wide at the top and 11 millimeters thick. This system was standardized by the Rubber Manufacturers Association in the 1960s. It replaced the older arbitrary numbering that different manufacturers used. If you're dealing with equipment from before 1965, the belt might have a non-standard designation that doesn't match any modern chart. In those cases, measuring the actual dimensions and matching them to the nearest standard section is the only reliable path. I had a situation last year with a vintage packaging machine that came back from a rebuild with what someone had labeled a "standard" B section belt. The pulleys were clearly cut for B groove. But when I measured the belt, the top width came out to 17 millimeters instead of the 16 millimeter standard for a B section. It was actually an 8L section, which uses the same outside circumference numbering as the L series but has a different cross section profile. The belt was too thick for the groove and was riding high on the pulley flanges. Replacing it with a proper BX section belt resolved the tracking issue immediately. The machine had been running hot and making a chirping sound for three months before anyone figured out what was wrong.
Pitch Length vs. Outside Length
This is the detail that causes the most ordering errors. Pitch length is the effective length where the belt actually transmits power. It's measured at the neutral axis inside the belt, roughly where the tension member sits. Outside length is the full outer circumference. For most classical belts, the pitch length is about one to two inches shorter than the outside length depending on the cross section. Modern specifications prefer pitch length because it's the functional measurement. Older charts and some supplier catalogs still list outside length. When you're crossing reference between sources, always check which measurement system is being used. A belt listed as 100 inches pitch length and a belt listed as 100 inches outside length are not the same belt. If you're measuring an installed belt on a machine with fixed center distance, you can't just take it off and measure it easily. In that case, you calculate the required length from the pulley diameters and center distance. The formula is straightforward: twice the center distance plus pi times the average pulley diameter plus the square of the diameter difference divided by four times the center distance. That gives you the pitch length in inches if all your inputs are in inches. It's not glamorous but it's accurate and it saves a trip to get the old belt off and measured.
Matching Belts to Pulley Grooves
The groove angle on most V belt pulleys is 34 to 38 degrees, not the full 40 degrees of the belt itself. That's intentional. The belt wedges into the groove and the sides do the work. The groove angle needs to be slightly smaller so the belt compresses properly and generates friction against the sidewalls. A pulley worn from years of use will have a wider groove angle at the top because the belt has been riding and abrading the edges. In those cases, even a perfectly sized belt will slip because the groove profile no longer matches the belt profile. I've replaced belts on older machines only to have them still slip afterward. The pulleys were the real problem. Regrooving or replacing the pulleys fixed it permanently. There's also the issue of sheave face width. A belt that's too narrow for the groove will rock side to side and wear unevenly. A belt that's too wide will not seat to the bottom of the groove and will contact only the upper edges, reducing the friction surface. Both conditions lead to premature failure. The tolerance on top width for a classical B section is typically plus or minus a fraction of a millimeter. It's tight enough that you can't substitute a C section for a B section and expect it to work.
When a V Belt Size Guide Chart Isn't Enough
Sometimes the chart stops helping. Dual section belts exist, which have two different cross sections on opposite sides of the same belt. They're used on machines that need different torque capacities on different pulleys in the same drive. A combined 3V and 5L belt, for example, would have a narrow wedge profile on one side and a classical profile on the other. These are specialty items and most standard charts don't list them in a useful way. You need to measure both sides independently and then cross reference with the manufacturer's catalog. Another edge case is belts with cogged or notched backsides. These are designed to flex more easily around small diameter pulleys and run cooler. The sizing is the same as the equivalent smooth belt, but the flexibility means they can handle smaller sheaves. A cogged A belt might run on a pulley as small as four inches diameter where a smooth A belt would fail from repeated flexing. If your application has tight spaces and small pulleys, checking whether a cogged variant exists in the size you need can extend belt life significantly. The cost is usually twenty to thirty percent more per belt. Temperature and chemical exposure also affect belt selection in ways that a basic size guide won't tell you. Standard rubber compounds degrade above 165 degrees Fahrenheit. If your drive runs hot, you need a belt rated for higher temperatures, usually made with EPDM or neoprene compounds. Oil exposure is another factor. Standard neoprene belts resist oil reasonably well, but sustained immersion or heavy splash will swell and soften the belt material over time. Specialty belts with reinforced cords and oil resistant covers exist for those conditions.
Common Pitfalls to Avoid
Don't mix old and new belts on a multi-belt drive. Even if they're the same size designation, the old belt has stretched and the new one hasn't. The new belt takes most of the load and fails quickly because it's overloaded while the old belt does almost nothing. Replace all belts in a drive at the same time. The cost difference between replacing one belt and replacing a set is usually small compared to the downtime and labor involved. Don't ignore the alignment check. A belt that's misaligned by even a quarter inch over a three foot span will wear the edges rapidly and may jump off the pulley under load. Laser alignment tools make this fast. Two minutes with a laser aligner beats two hours of troubleshooting a belt that keeps coming off. And don't over-tighten. The old rule of thumb about pressing down on the belt midpoint to check tension is wrong. Proper tension is measured with a tension gauge or by calculating the correct deflection force for the belt type and span length. Over-tightening loads the bearings and wastes motor power. Under-tightening causes slip and heat buildup. Both conditions destroy the belt faster than normal operation would.
A V Belt Size Guide is only as good as the measurements behind it. Take the time to get the cross section right, confirm whether you're working with pitch or outside length, check the pulley condition, and verify alignment before you install anything. The chart is a starting point, not the finish line.