Getting the V Groove Right Before You Even Strike an Arc
I spent about four hours yesterday reworkiing a failed V-groove weld on a 3/4" plate joint. The issue wasn't the technique or the amperage. It was the bevel angle drawn wrong on the prints. The engineer specified a 60-degree included angle but the fabricator laid out a square-edge fit-up. By the time we caught it during crip inspection, the root was completely unwelded with a slag inclusion hiding at the bottom. That kind of thing happens all the time when nobody actually reads the welding symbol before threading material. Here is what you need to know about reading and applying the V Groove Weld Symbol so that does not happen on your watch.
Reading the V Groove Weld Symbol Correctly
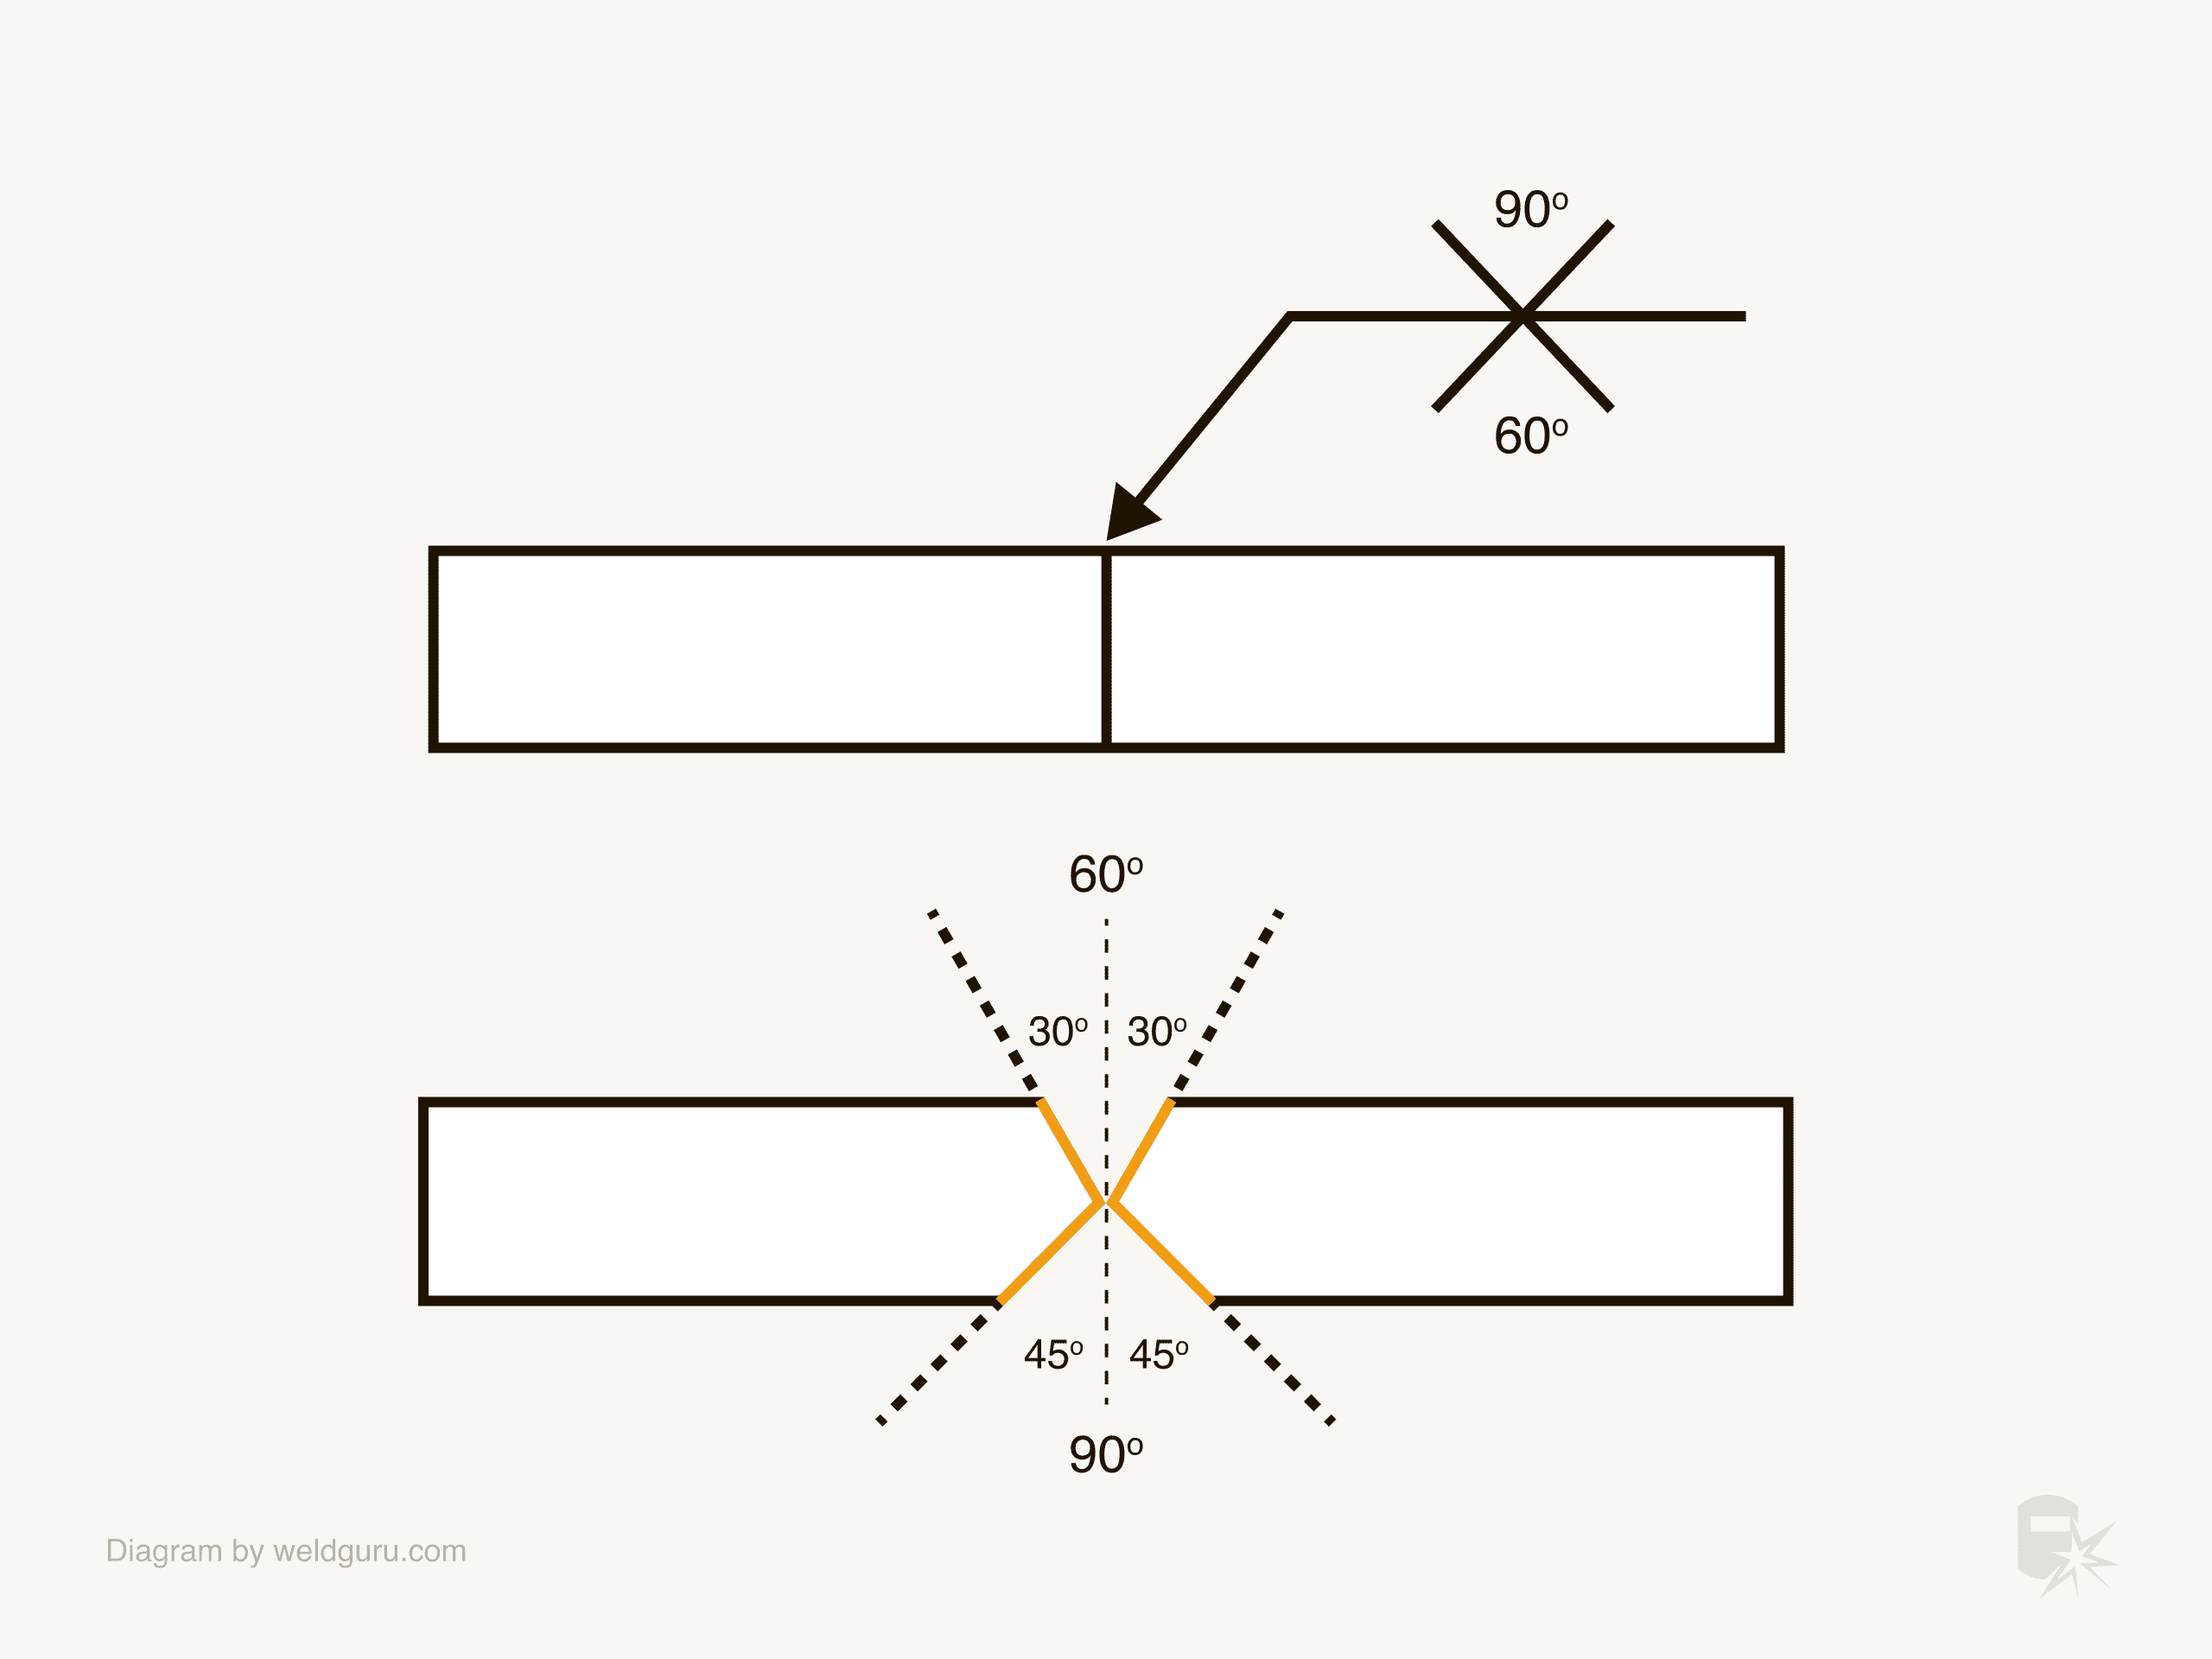
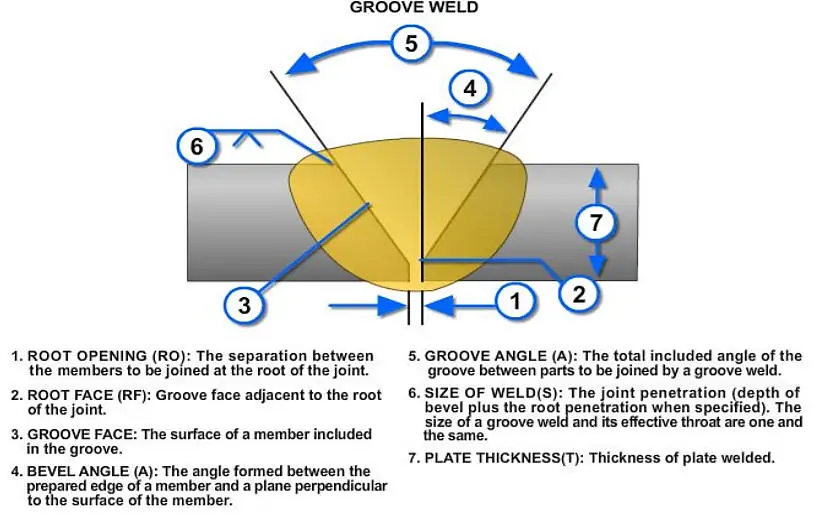
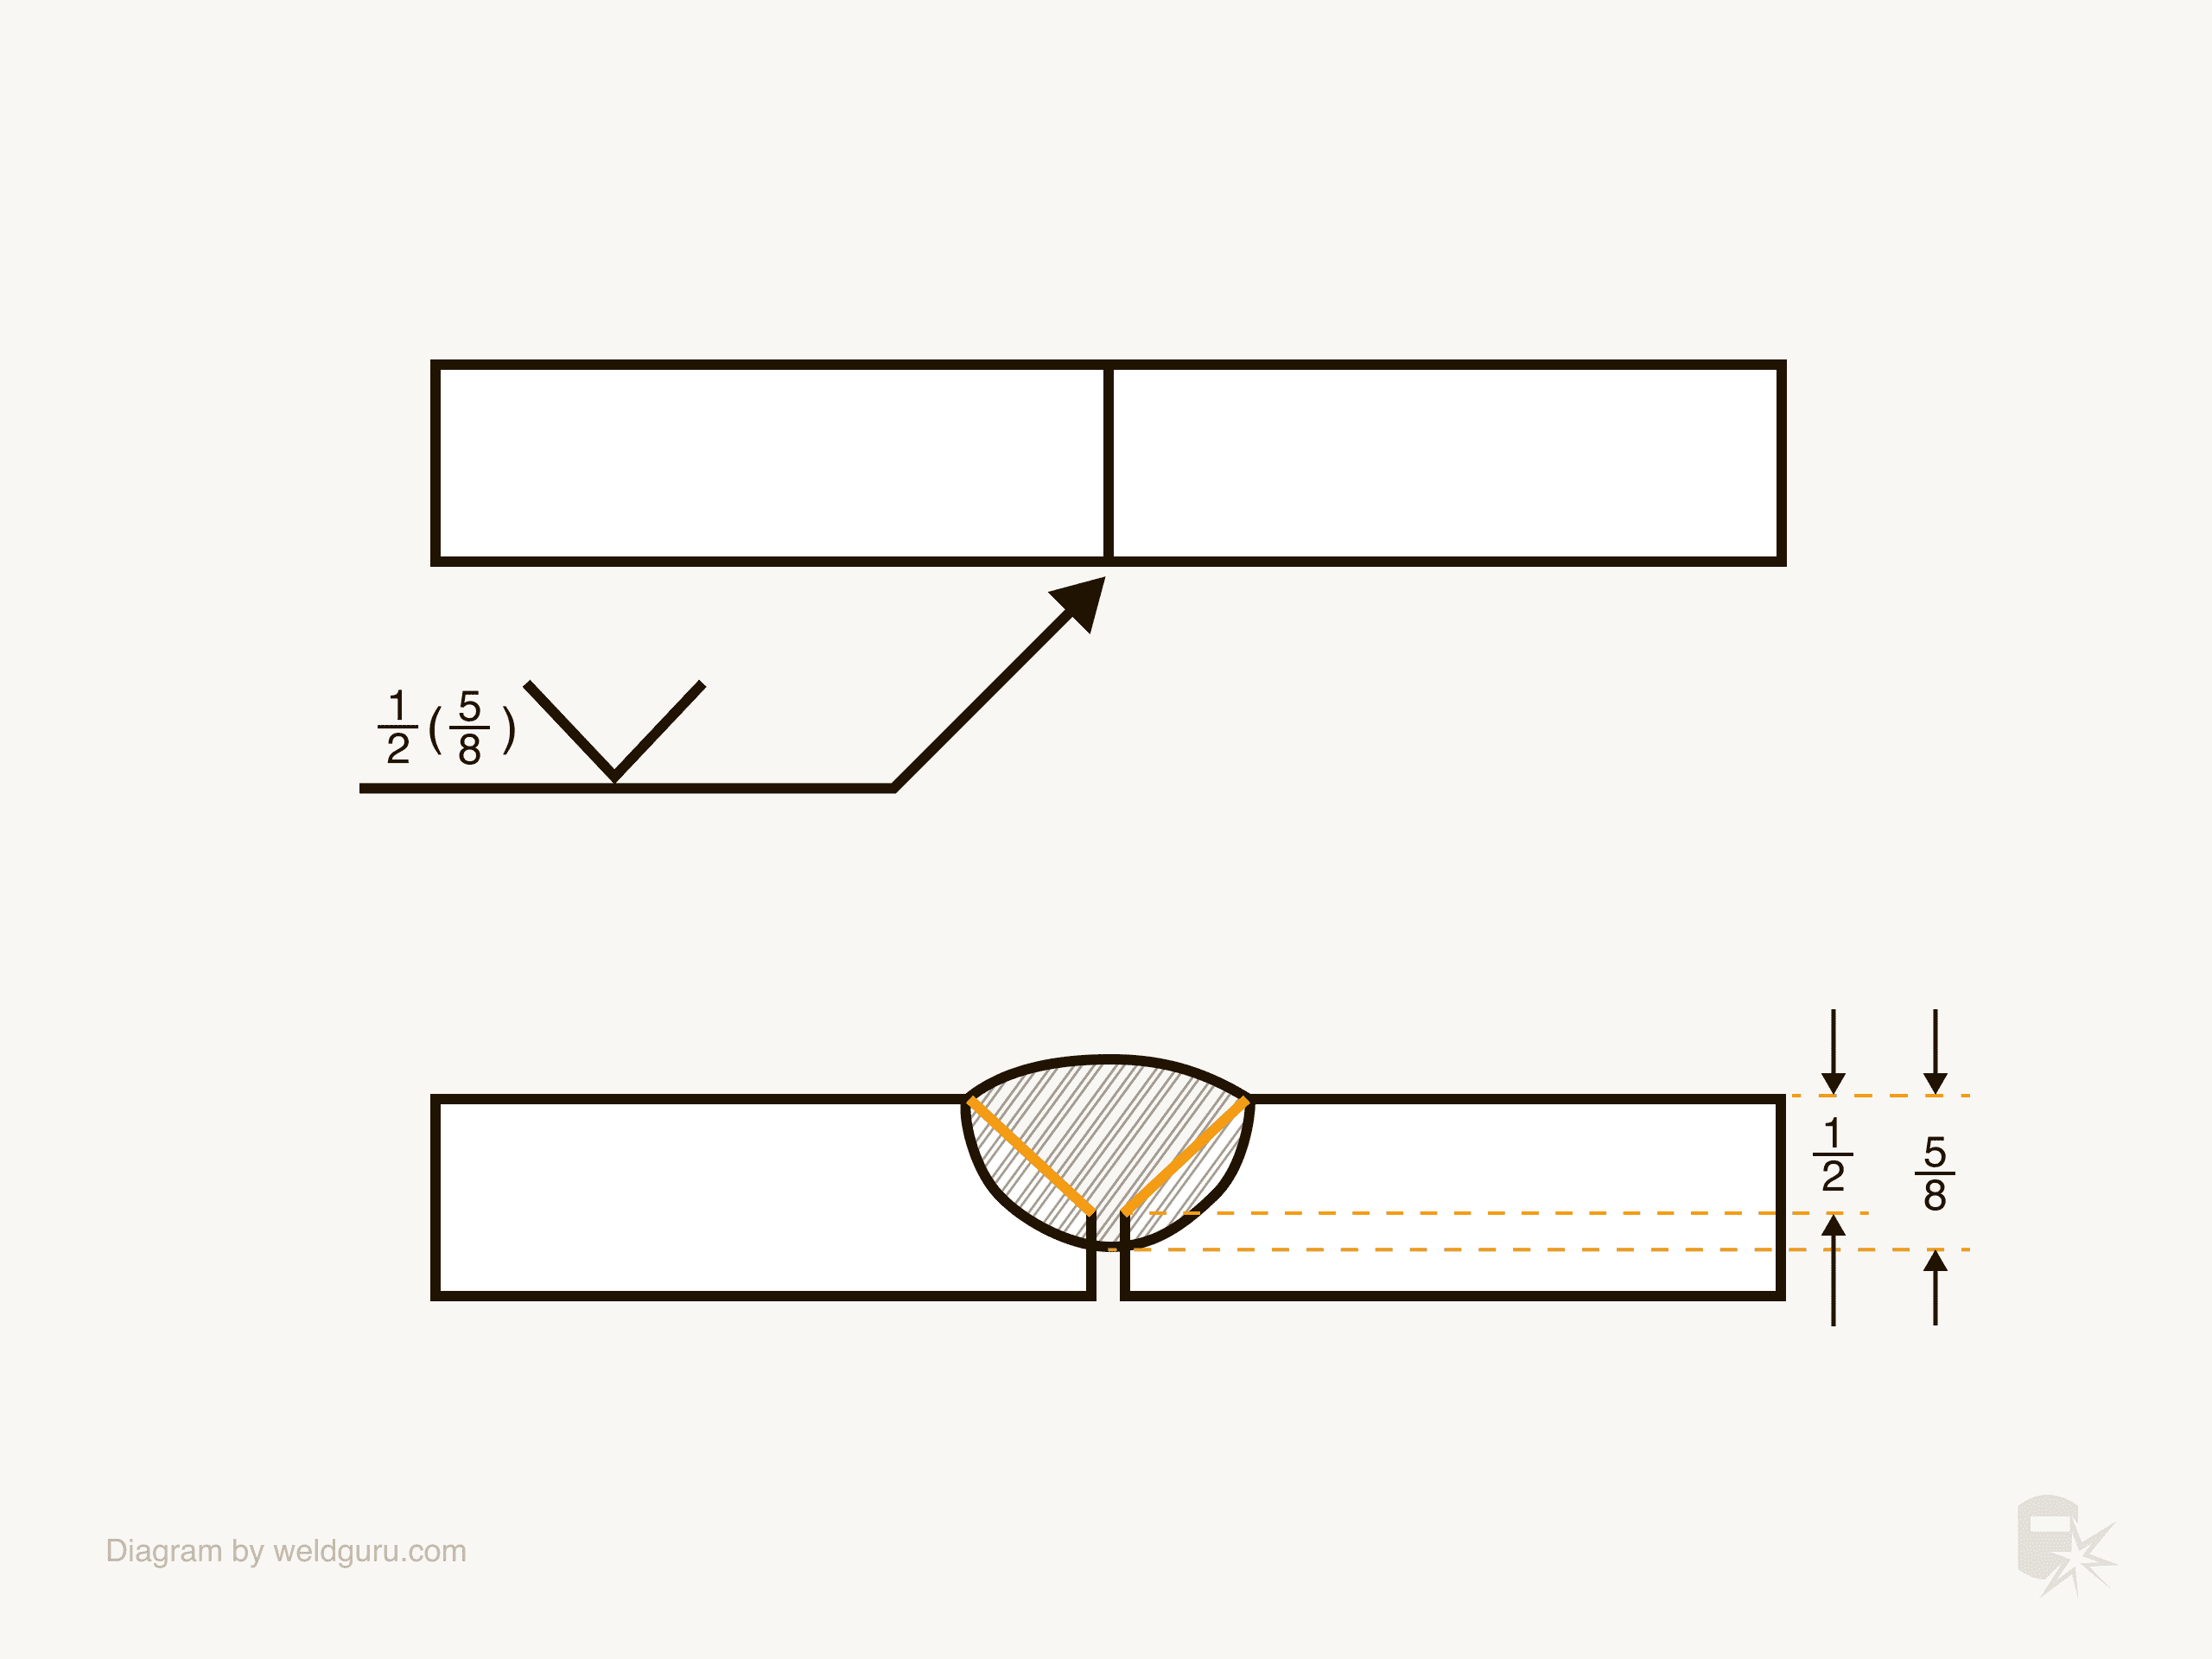
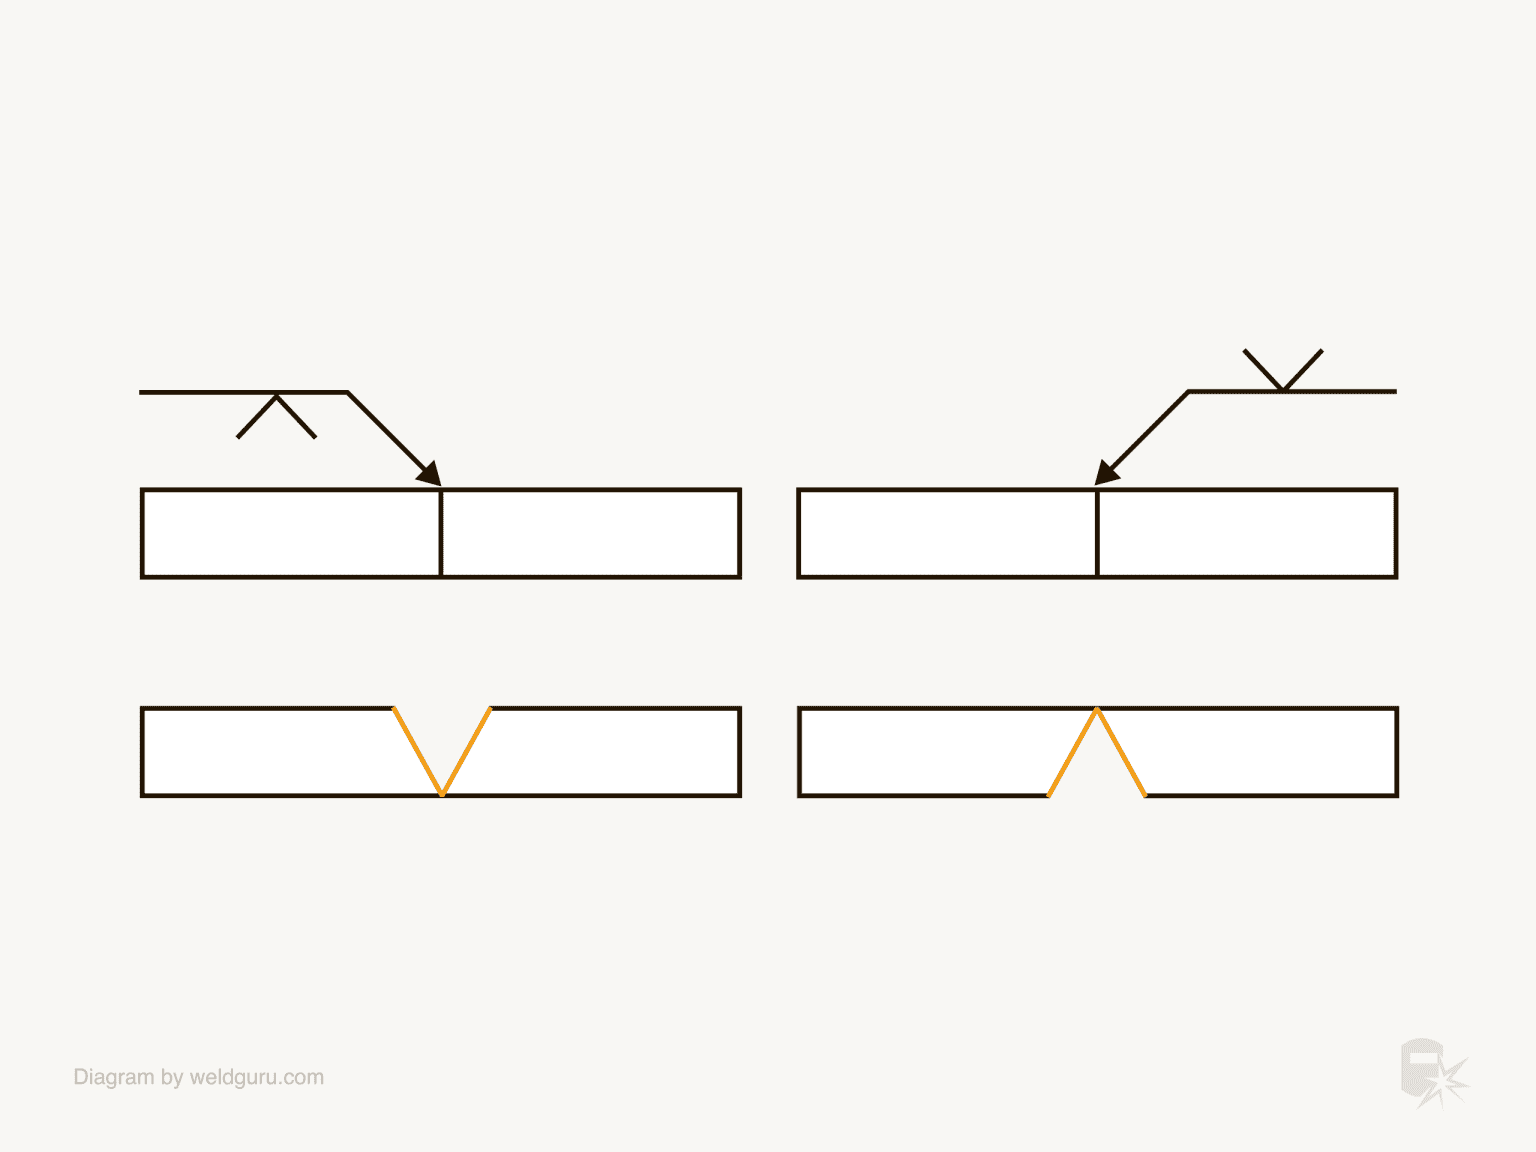
The V groove weld symbol looks like a simple V on the reference line of a welding symbol. It tells the welder that both pieces need to be beveled to form a V-shaped joint before welding. The symbol itself has a few parts that matter. There is the V shape attached to the reference line. There are numbers above and below that line. And there might be additional flags or tail notes that change everything. The basic symbol shows up on the reference line with the point of the V facing down when it goes on the arrow side and facing up when it goes on the other side. The arrow side rule is straightforward but people still get it backwards under pressure. If the V is below the reference line, you weld the side the arrow touches. If it is above, you weld the opposite side. That is it. Two lines of logic. But I have seen welders walk away from a job because they misread which side the symbol was on and then had to gouge out half the joint to redo it. The numbers tell you the gap and the angle. A typical callout might read something like a 60-degree included angle with a root opening of 3/16 inch and a root face of 1/8 inch. You do not weld blind on those numbers. You measure them with a go/no-go gauge or a protractor before you start. If the bevel is cut too shallow the filler metal cannot reach the root. If the root face is too wide you get lack of fusion every single time. These are not theoretical problems. They are the reasons rework budgets exist.
What the Symbol Does Not Tell You
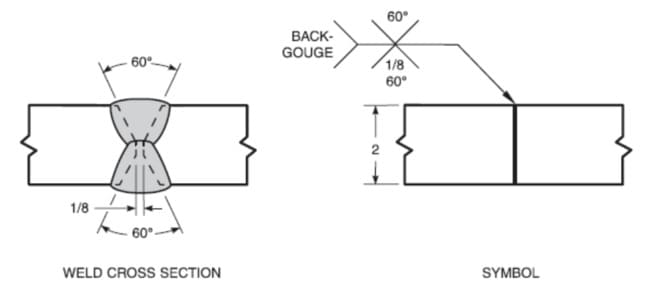
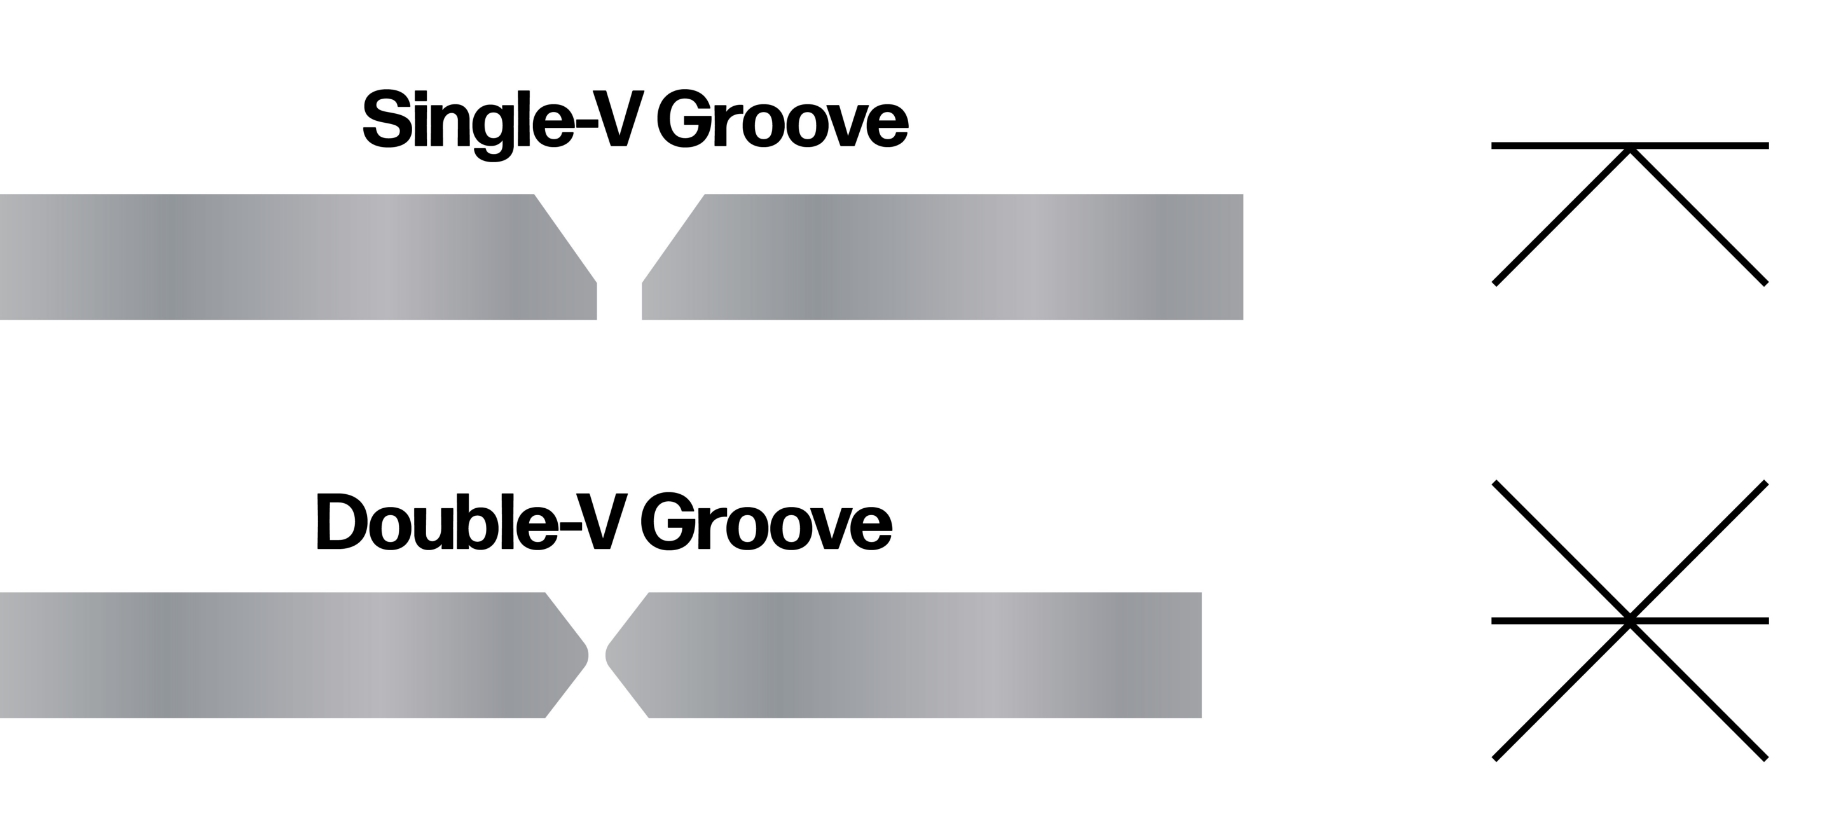
The welding symbol is a shorthand communication tool and it leaves out a lot of practical information. It will not tell you the welding process to use. It will not specify the electrode type or diameter. It will not indicate how many passes or what interpass temperature to maintain. That all lives in the procedure specification or the welder's qualifications, not on the symbol itself. A good welder reads the symbol and then checks the WPS. A careless one just starts moving the torch. Here is a nuance most beginners miss. The V groove symbol assumes a single-V joint. But when you are working with material thicker than about 1 inch, a single V is usually a bad call. The weld pool becomes too deep, the heat input balloons, and you are looking at significant distortion and possibly hydrogen cracking in higher carbon steels. The practical move is a double-V or J-groove instead. The symbol for that is two V shapes back to back on the reference line, one above and one below. It splits the weld passes between both sides and cuts the total filler metal volume nearly in half. That also means roughly half the distortion. I switched a fleet of my welders from single-V to double-V on 1-1/4 inch plate joints last year and our straightness tolerance pass rate went from about 62 percent to 94 percent within two weeks. That is not a small difference.
Get the Full Details
A Real Problem I Faced and How I Fixed It
About three years ago I was running a series of V-groove welds on 1-inch A36 plate with a 37.5-degree bevel angle per the drawing. Standard stuff. We were doing semi-automatic GMAW with 70S-6 wire. The first couple of joints looked fine visually. But when we took them for bend testing, three out of five failed on the tension side of the face bend. The fracture surface showed a thin band of incomplete fusion running right along the root. I spent two days chasing this. I checked the amperage. I checked the travel speed. I checked the shielding gas mix. Nothing was wrong. The problem was the root opening. The drawing called for a 5/16 inch root gap but the cutting process we were using — plasma arc — was leaving a slight rounded toe on each bevel edge. When the plates were brought together the actual contact point was somewhere in the middle of the V, not at the theoretical sharp root. The effective root opening was closer to 3/16 inch and the root face had effectively disappeared into a fillet of molten metal that never bonded to the base metal. It looked solid from the top. It was a ticking bomb underneath. The fix was embarrassingly simple. I switched from plasma cutting to machining the bevels on the plate edges. Machined edges have a true sharp root and a consistent root face. The first six joints from machined plate passed every test on the first try. Total cost increase per joint was about eight dollars in machining time. The rework cost per failed joint was closer to three hundred dollars when you factor in gouging, cleaning, repositioning, and repassing. The math writes itself.
Common Pitfalls with V Groove Weld Symbols
There are a few recurring mistakes I see over and over again in shop floors and field inspections. First, people ignore the back gauge dimension. The V groove symbol sometimes includes a dimension for the depth of the bevel or the total joint penetration. If you treat that as optional guidance instead of a hard requirement you will under-penetrate and the joint will be weaker than the base metal regardless of how pretty the weld bead looks on top. Penetration depth is measured after the fact with radiography or by sectioning and etching. You do not want to find out after the fact. Second, the flange condition of the bevel is routinely overlooked. A bevel that has been plasma or flame cut retains a hardened zone and possible micro-cracks along the edge. For critical structural work you need to grind that edge back until you see clean, bright metal. I have walked away from joints that were cut with oxy-fuel and had white specks of slag imbedded in the bevel face. Those specks become inclusions the moment you try to weld over them. Ten minutes with an grinding disc saves you from an entire day of rework.
Third, root opening variation. When you are fit-up welding multiple joints in sequence the first one sets the gap and then the subsequent ones change as the metal cools and contracts. I keep a set of tapered feeler gauges at my bench and check the root opening between every third joint. If it drifts more than 1/16 inch from spec I stop and adjust the fixture or the tack weld spacing. You can catch this in two minutes. You cannot catch it easily after the weld is done.
When a V Groove Is the Wrong Choice
Not every joint needs a V groove. If you are joining material under 3/8 inch thick a square groove with full penetration is often faster and just as strong. The V groove symbol would be unnecessary overhead in that case. If you are working with thin sheet metal the heat input from a V-groove weld will warp the assembly before you finish the first pass. A butt joint with a backing bar and a fillet weld on both sides is more appropriate and takes about a third of the time. Similarly, if the joint geometry makes access to one side impossible, a single-V from one side alone is risky. You will struggle to get proper root penetration without a back gouge procedure, and back gouging adds time and cost. In those cases a J-groove or a bevel-groove symbol on both sides with partial penetration might serve you better. The symbol changes accordingly and the procedure does too. Do not force a V groove where another groove type fits the geometry more naturally.
Quick Reference for the V Groove Weld Symbol
When you are standing at the print and need to make a decision fast, here is what the symbol is telling you in plain terms. The V shape on the reference line means bevel both pieces to form a V joint. The position relative to the reference line tells you which side to weld. The angle number is the included angle of the bevel. The root opening dimension is the gap between the plates at the root. The root face dimension is the flat portion at the very bottom of the bevel that should not be cut away. Any welding process symbol in the tail, like GMAW or SMAW, tells you how to deposit the filler. Length and quantity numbers to the left of the symbol tell you how long each weld should be and how many there are. Download a copy of AWS A2.4 if you need the official reference for symbol notation. It is the standard most shops in North America follow. You can find it through the American Welding Society website or many of the industrial supply sites. It is not free but it is worth keeping as a reference. The symbols change slightly between editions and having the current one prevents argument with inspectors.
The Bottom Line
The V groove weld symbol is not complicated once you stop treating it like decorative art on a blueprint. It is a set of instructions. Read the arrow side rule correctly. Verify the bevel angle and root dimensions before cutting. Machine the edges when precision matters. Check the root opening between joints. Know when not to use a V groove at all. The symbol does the heavy lifting for communication. Your job is to make sure the physical joint matches what the symbol promises.