Getting Value Analysis Right When Nobody's Watching
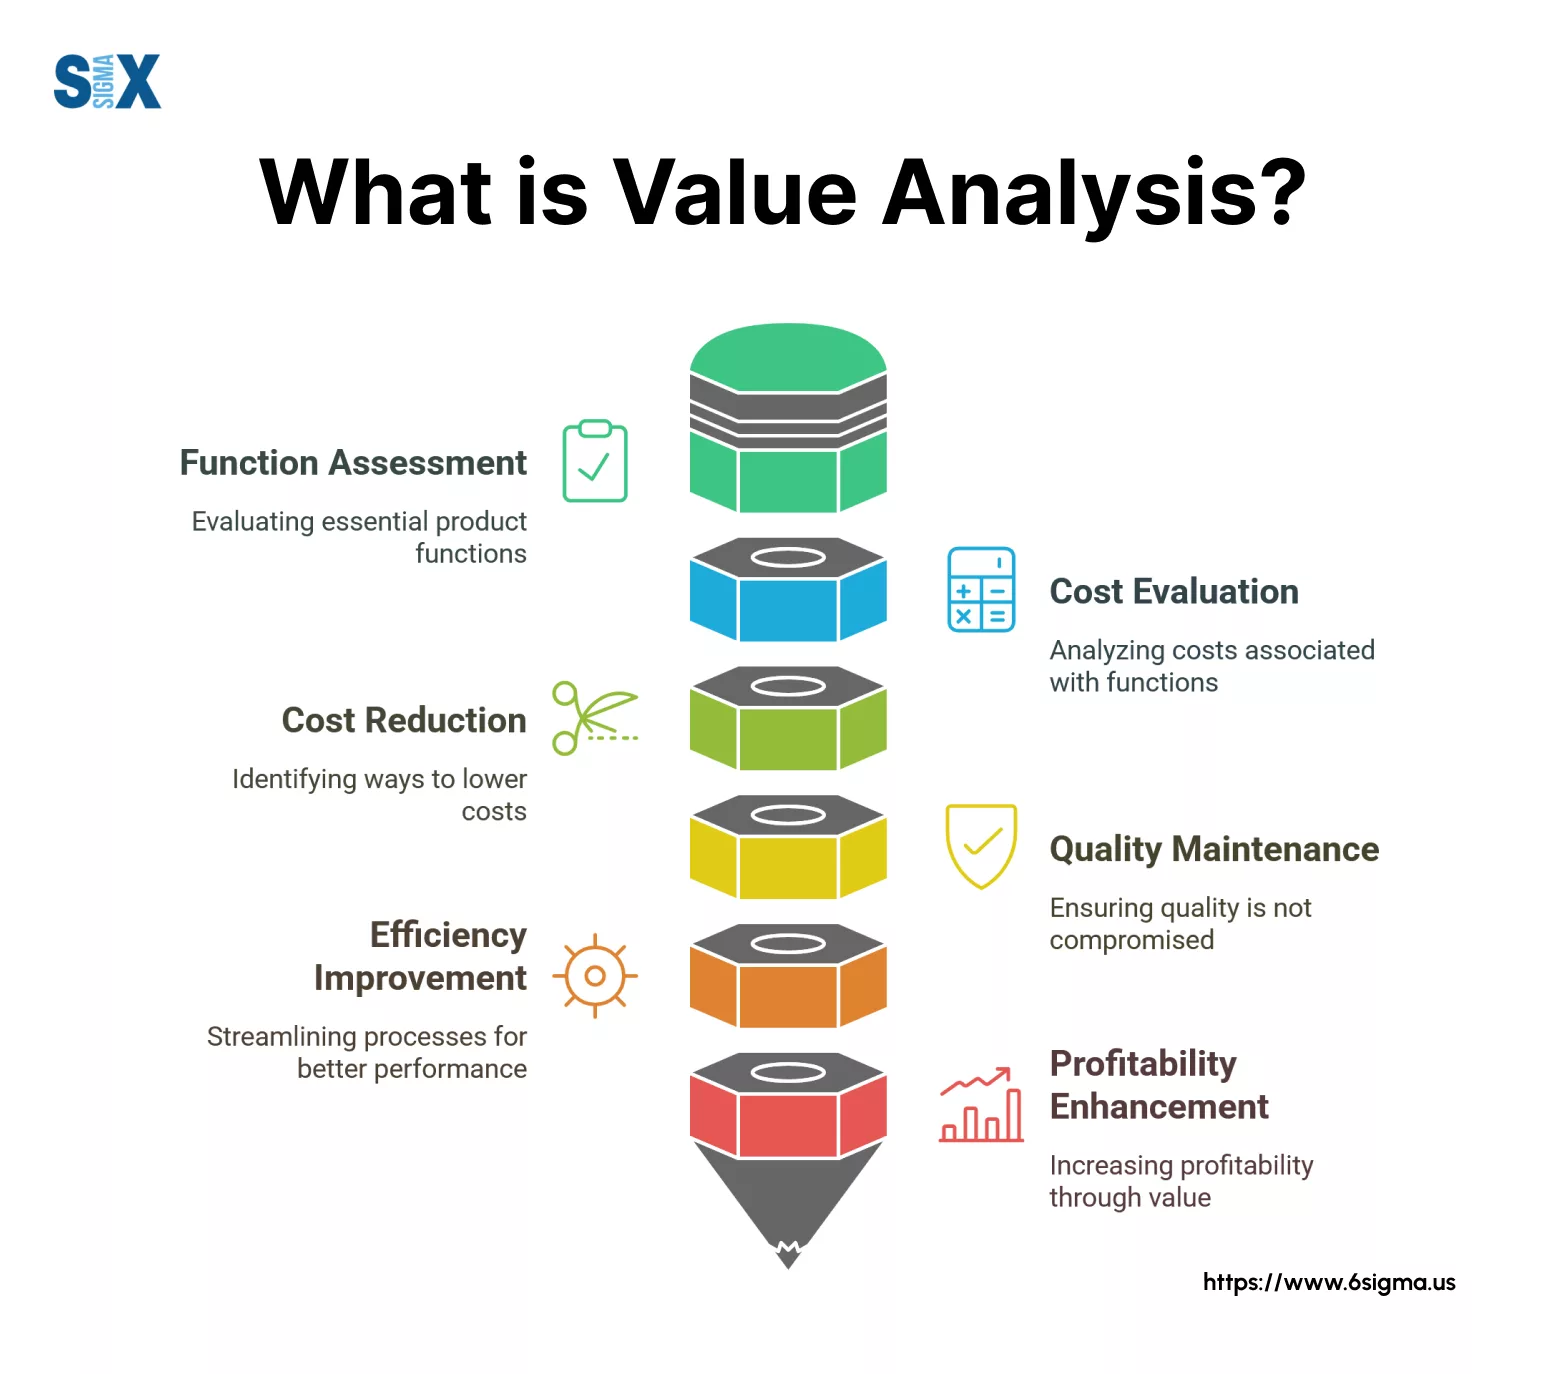
Most people treat value analysis like a checkbox exercise. They fill out a template, rank a few functions, and call it done. The ones who actually use it properly know it takes a specific approach that most guides don't cover. Value analysis isn't about cutting costs across the board. It's about function-by-function scrutiny of what a product or process actually does, then finding ways to deliver that function at lower cost without sacrificing performance. The core concept is simple enough, but the execution is where most teams stumble. I worked on a manufacturing line audit last year where we were tasked with reducing waste on a custom housing component. The initial instinct was to look at material costs, but that wasn't the lever. The real savings came from understanding that the housing had a secondary function nobody had written down. The part provided structural support for an internal bracket, and it also served as a thermal barrier. Most of the thickness specifications existed because they were copied from a previous generation design. When we stripped away the redundant thermal mass and kept only what the bracket needed, we cut material use by 34 percent without any requalification testing. The thermal analysis was unnecessary because the component never reached temperatures high enough to matter.
This kind of thing happens constantly. Functions get baked into designs through historical precedent rather than requirement. Value analysis is the tool that surfaces those assumptions.
How To Run A Value Analysis Properly
Start with function definition. Not feature definition, not specification definition. Function. Ask what the item actually does, not what it is. A washer doesn't distribute load. It maintains clamp force by compensating for surface irregularities. The distinction matters because it changes what you'd consider an acceptable alternative. Next, assign a cost to each function. This isn't the component's cost. This is how much of the total product cost exists to satisfy that specific function. If a single part delivers three functions, you need to split its cost across those functions based on measurable criteria. Weight, volume, or process time can work depending on what's available. I've used cycle time in production environments and mass in design environments because those are the metrics my teams already track. After that, build a function-cost matrix. Rows are functions. Columns are components or processes. Fill in the intersections with your allocated costs. The empty cells tell you something useful too. If a function shows zero cost allocation, it might mean nobody owns that function. Or it might mean it's being delivered for free by something else in the design. Either way, it deserves a second look.
Get the Full Details
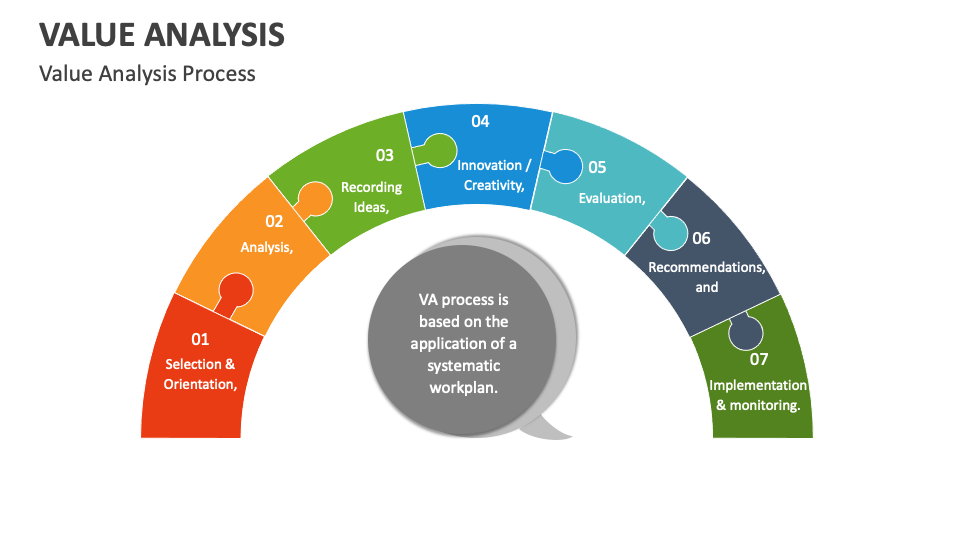
Then come up with alternatives. For each high-cost function, ask what else could deliver it. Standard off-the-shelf parts often beat custom solutions here, but don't jump to that conclusion blindly. I once saw a team replace a custom-machined aluminum bracket with a stamped steel one and save 60 percent on the part. It worked fine until we ran fatigue testing and found the stamped bracket failed at 8,000 cycles under a load profile that the original design handled at over 50,000. The function definition had been too narrow. We'd defined it as "hold the motor in place" when it should have been "hold the motor in place under vibration and thermal cycling." The broader definition would have ruled out the stamped bracket immediately. The alternatives phase is also where you evaluate maintainability, assembly sequence, and supplier risk. Value analysis isn't just about unit cost. A part that costs less but takes three times longer to install has consumed more value than it saved.
Pitfalls That Will Waste Your Time
One common mistake is starting with cost reduction as the goal instead of function optimization. When you lead with savings targets, you tend to find cheap versions of the same solution rather than better solutions. The output looks good on paper but delivers marginal improvement in practice. I've seen teams spend weeks chasing 5 percent cost reductions this way when a proper function-first review would have found 20 percent with less effort. Another issue is involving the right people late. Value analysis works best when the people who actually build and maintain the product are in the room from the start. Engineers sometimes run these exercises in isolation and come back with theoretically sound recommendations that nobody on the floor can implement. One analysis I reviewed proposed replacing a welded joint with a bolted connection to simplify assembly. The engineer hadn't consulted the welders, who pointed out that the proposed bolts would need access from both sides of the assembly, which wasn't possible in the final layout. The recommendation was technically valid but practically useless. Value Analysis Takes Place most effectively when cross-functional teams work through it together. Procurement knows supplier constraints. Manufacturing knows assembly realities. Quality knows failure modes. All three perspectives are necessary to avoid the blind spots that turn a promising analysis into an expensive misstep.
When Value Analysis Doesn't Work
There are situations where this method adds little value. Highly regulated products with fixed compliance requirements leave very little room for functional substitution. A medical device component that must meet a specific ISO standard often can't be redesigned without going through a lengthy recertification process that costs more than any material savings would offset. In those cases, value engineering through procurement negotiation or supplier consolidation makes more sense than redesign. Simplified products with two or three major functions also don't benefit much. There's not enough complexity to unpack. You're better off looking at economies of scale or process optimization instead. Value analysis shines in the middle ground. Products with moderate complexity, multiple functions, and reasonable scope for redesign. That's where the effort pays off. The methodology itself is tool-agnostic. You can run it on paper, in a spreadsheet, or with dedicated software. I've used both and found that the format matters less than the rigor of the function analysis. A well-executed exercise on a whiteboard beats a poorly executed one in an expensive platform every time.