Understanding the Process
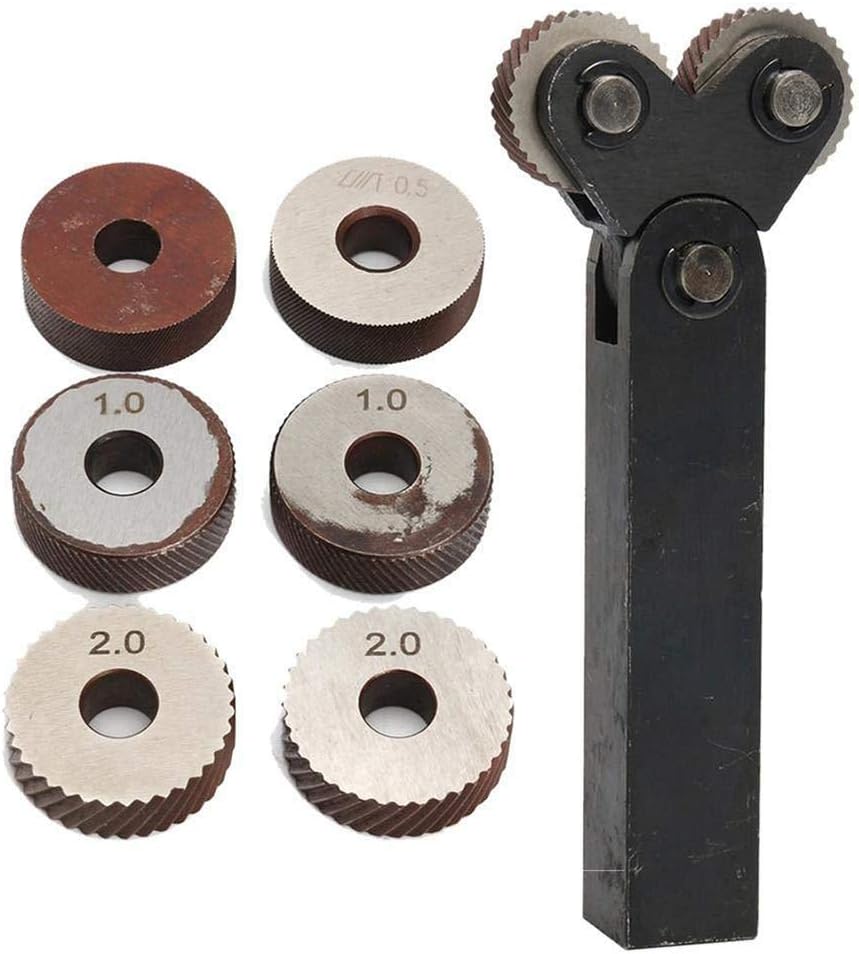
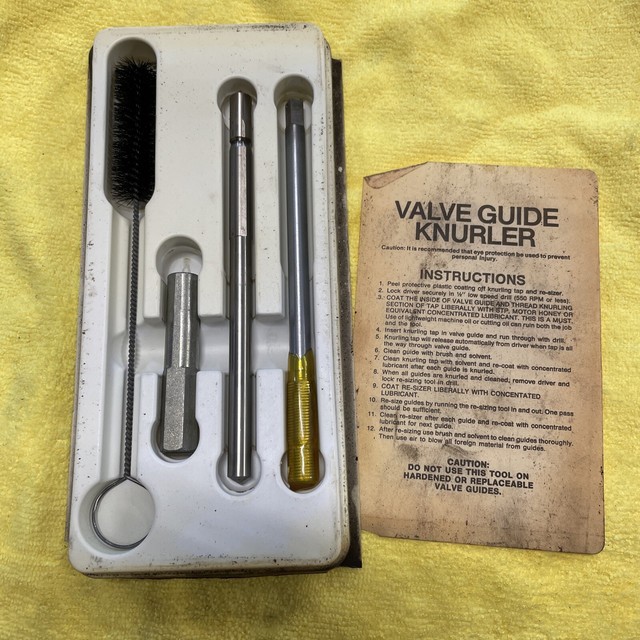
The outer surface of a valve guide gets a roughened pattern so it locks into the cylinder head bore when pressed in. A straight smooth guide can rotate or walk under thermal cycling, especially in high-output applications where the head sees repeated expansion and contraction. Knurling addresses that by creating a mechanical key between the guide OD and the head bore. You need a few things before you touch the head. A knurling tool itself, which is basically a handle with a small cutting wheel mounted on a pivoting arm. A micrometer or caliper capable of reading to .001 inches. The correct pilot for your guide ID so the cutter runs concentric. And obviously the valve guides you are installing. Here is how the actual job goes. Start by measuring the head bore. Record the diameter at three points along the bore to check for taper or out-of-round. That measurement determines what kind of interference fit you are trying to achieve. A standard cast iron head with a .492 inch bore and a .500 inch guide OD calls for roughly .008 inch interference. Aluminum heads expand more, so the calculation shifts. If you are installing in an alloy head that has been re-bored to .502, you need a larger guide or a different approach altogether.
Mount the pilot in the guide. Tighten it just enough to center the cutter. Set your depth stop. I usually set it to remove about .003 to .004 inch of material from the guide OD, which translates to a radial expansion of roughly .006 to .008 inch after the knurl forms. That is the range that works for most passenger car heads without over-stressing the alloy around the bore. Apply cutting oil. Do not skip this. The steel cutters work harden quickly if they run dry, and you end up tearing the bronze instead of shearing it cleanly. Engage the cutter against the guide and rotate the handle. Two to three light passes are better than one deep pass. You are forming teeth, not milling stock. The resistance should feel consistent. If the tool binds or the handle kicks back, you have gone too deep or your pilot is not centered. I learned this the hard way on a set of late-90s Honda B-series heads. The manufacturer specs called for a .003 to .005 interference fit on the intake side. I set my depth stop correctly, engaged the cutter, and immediately felt a grab. The guide jumped. I backed off, pulled the head, and found that the old guide had been installed with an anti-seize compound that had baked onto the OD. The knurling cutter was cutting through residue instead of metal, which threw off the interference calculation entirely. My workaround was to use a flexible abrasive stone on a die grinder, carefully clean the guide OD back to bare metal, re-measure, and start over. Took me another twenty minutes per guide, but the installs went smooth after that. Lesson: always inspect the guide OD before knurling, not after.
After the knurling is done, wipe the guide clean. Brush out any chips from the head bore with a rigid bristle brush and compressed air. A single fragment of bronze left in the bore will push the guide off-center when you press it in, and then you are dealing with a guide that is slightly crooked and has compromised flow through the valve train. Press the guide in. Use a proper sleeve that contacts the outer face of the guide, not the knurled surface itself. You want even pressure across the entire face. A socket and a slide hammer or a hydraulic press both work. The knurled teeth will bite into the bore material as they pass through, creating that mechanical lock. If the guide stops before it is fully seated, do not hammer it. Back it out, inspect the bore for debris, and try again.
Get the Full Details

Common Pitfalls and What Most People Miss
Beginners tend to over-knurl. More teeth does not mean a better seal. An overly aggressive knurl pattern creates thin fins of displaced metal that can fracture under thermal stress, leading to premature guide failure. Stick to a light, even pattern. The goal is uniform contact, not maximum texture. Another thing people overlook is pilot runout. If your pilot is worn or dirty, the cutter will trace an elliptical path instead of a circle. The resulting knurl pattern will be uneven around the circumference. One side ends up with heavy interference while the other side is loose. I once installed four guides on an LS head, perfectly confident in my setup, and after assembly noticed uneven valve train noise on one bank. Turned out the pilot on one of my knurling tools had a slight bend from a prior drop. Ran a dial indicator against a known-good guide, measured .003 runout at the cutter tip, and swapped it out. Everything else checked out fine after that. Also consider the material of your guides. Bronze knurls easily and gives predictable results. Sintered iron is harder on cutters and produces a finer, less pronounced pattern. Some aftermarket aluminum heads have thin-walled guide bores that can distort under the radial force of aggressive knurling. In those cases, a guide with a pressed-in interference fit without knurling, or even a sleeve-style guide, may be the safer route.
If the head bore is already worn past specification, knurling will not fix it. You need to either reinstall a sleeve, use oversized guides, or have the head professionally rebored. Knurling adds material engagement, not structural repair. It is a finishing technique, not a solution to a bad bore.
Tool Options and Cost Considerations
Knurling tools run anywhere from forty dollars for a basic manual unit to two hundred plus for a precision bench-mounted version with adjustable depth stops and replaceable cutter wheels. The cheap ones work if you are careful. The expensive ones reduce the guesswork, especially on depth setting and pilot alignment. Replacement cutters cost around fifteen to thirty dollars a piece. They wear out faster than you might expect if you are knurling sintered iron guides in volume. Keep spares on hand. A dull cutter produces ragged knurl teeth that do not seat properly and can loosen under heat cycling. Some shops skip knurling entirely and rely on a precision bore plus a tightly tolerated guide OD. That works if the head is in good shape and the parts are sourced correctly. But knurling remains useful when you are working with older heads that have some bore wear, or when you need a margin of safety against guide rotation in a high-stress application. It is a low-cost insurance policy on an otherwise expensive repair.

Bottom Line
Knurl a guide lightly, measure twice, keep your pilot clean, and never assume the head bore is perfect just because it looks okay. The tool is straightforward. The judgment calls are where mistakes happen.