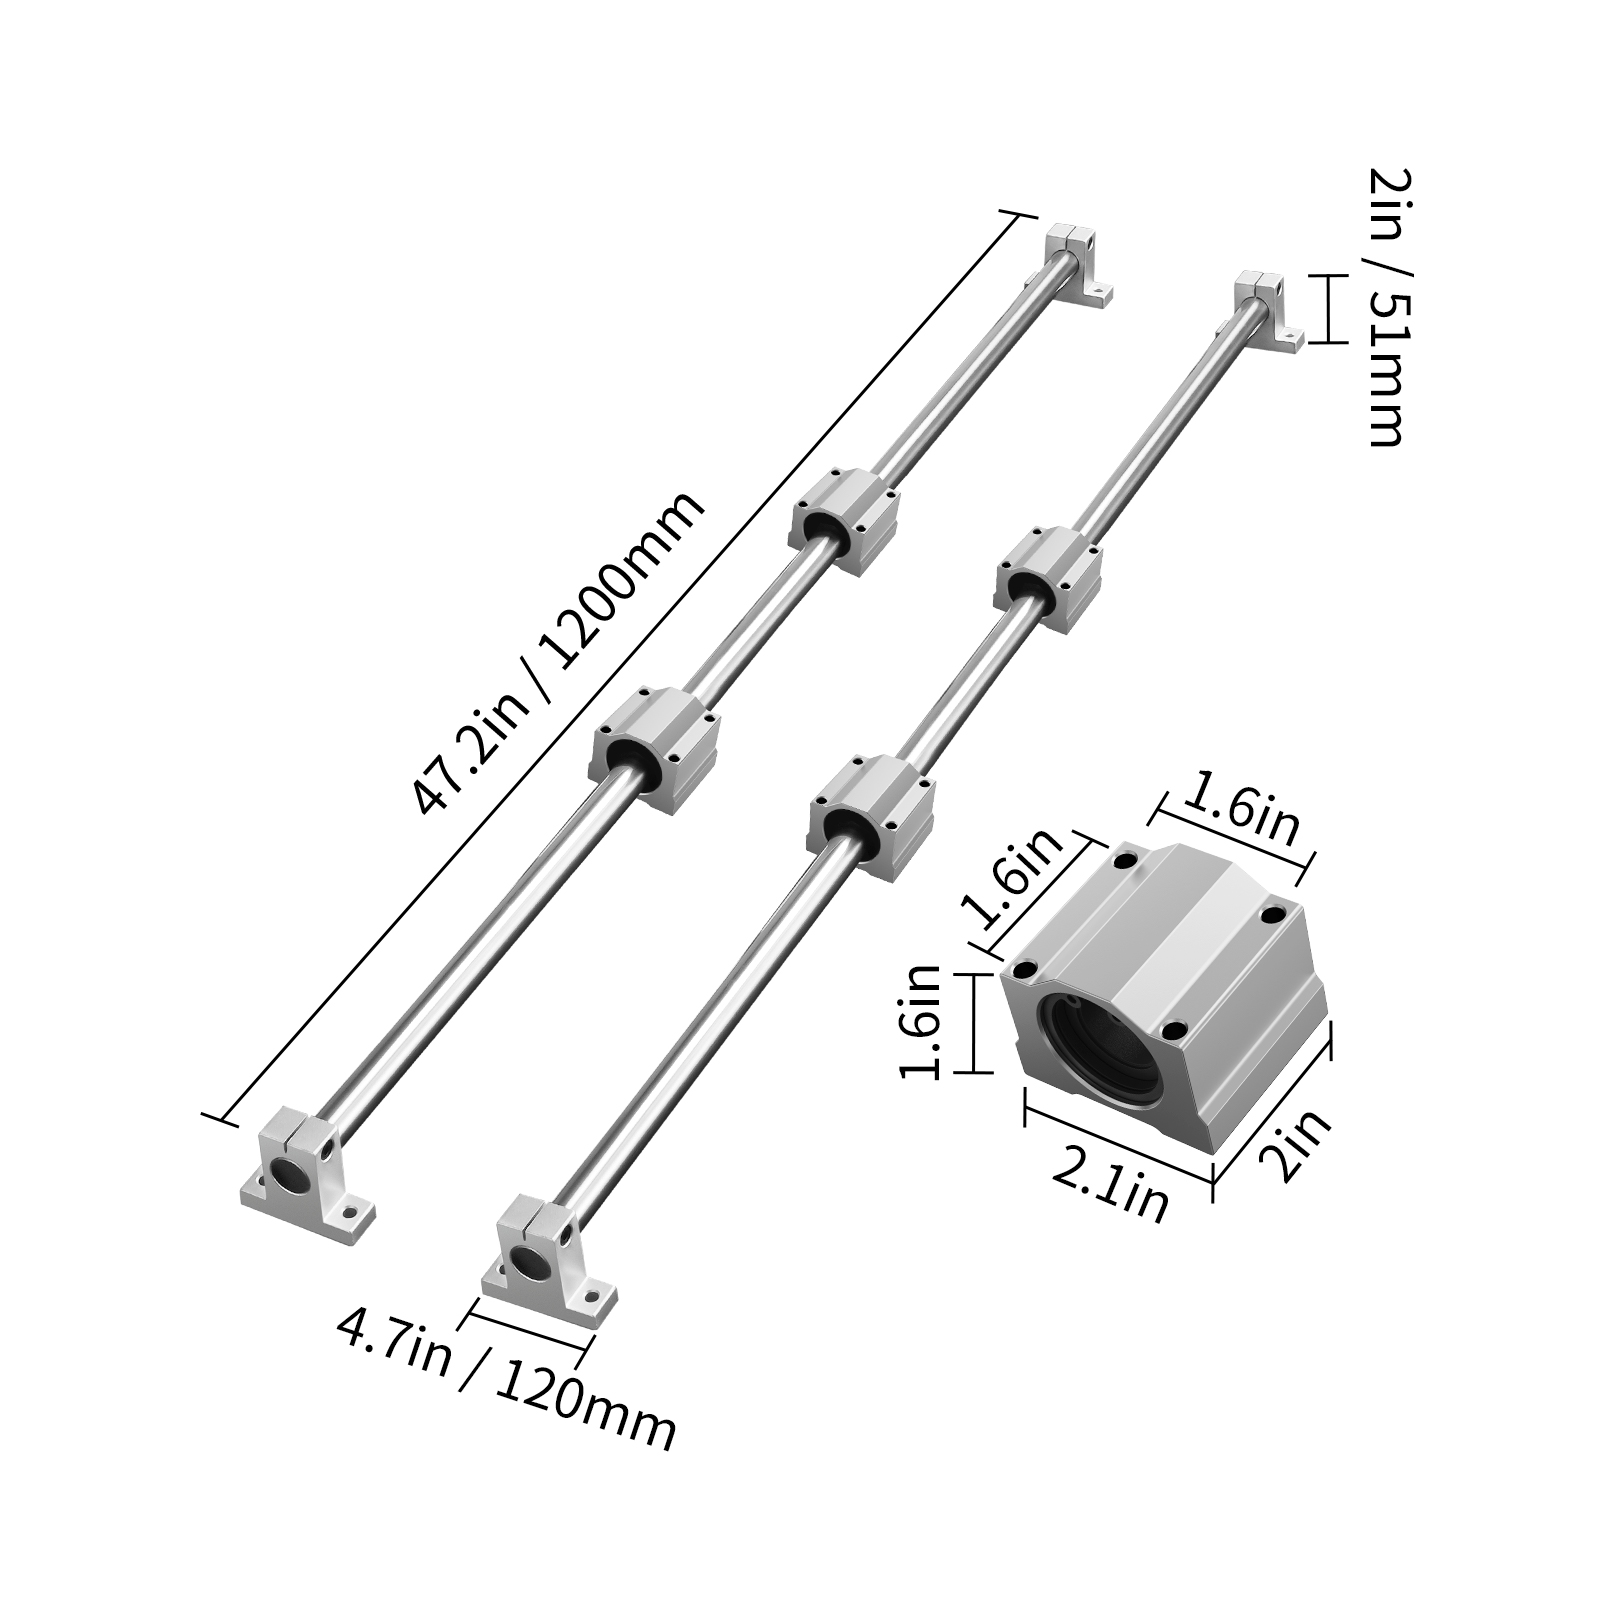
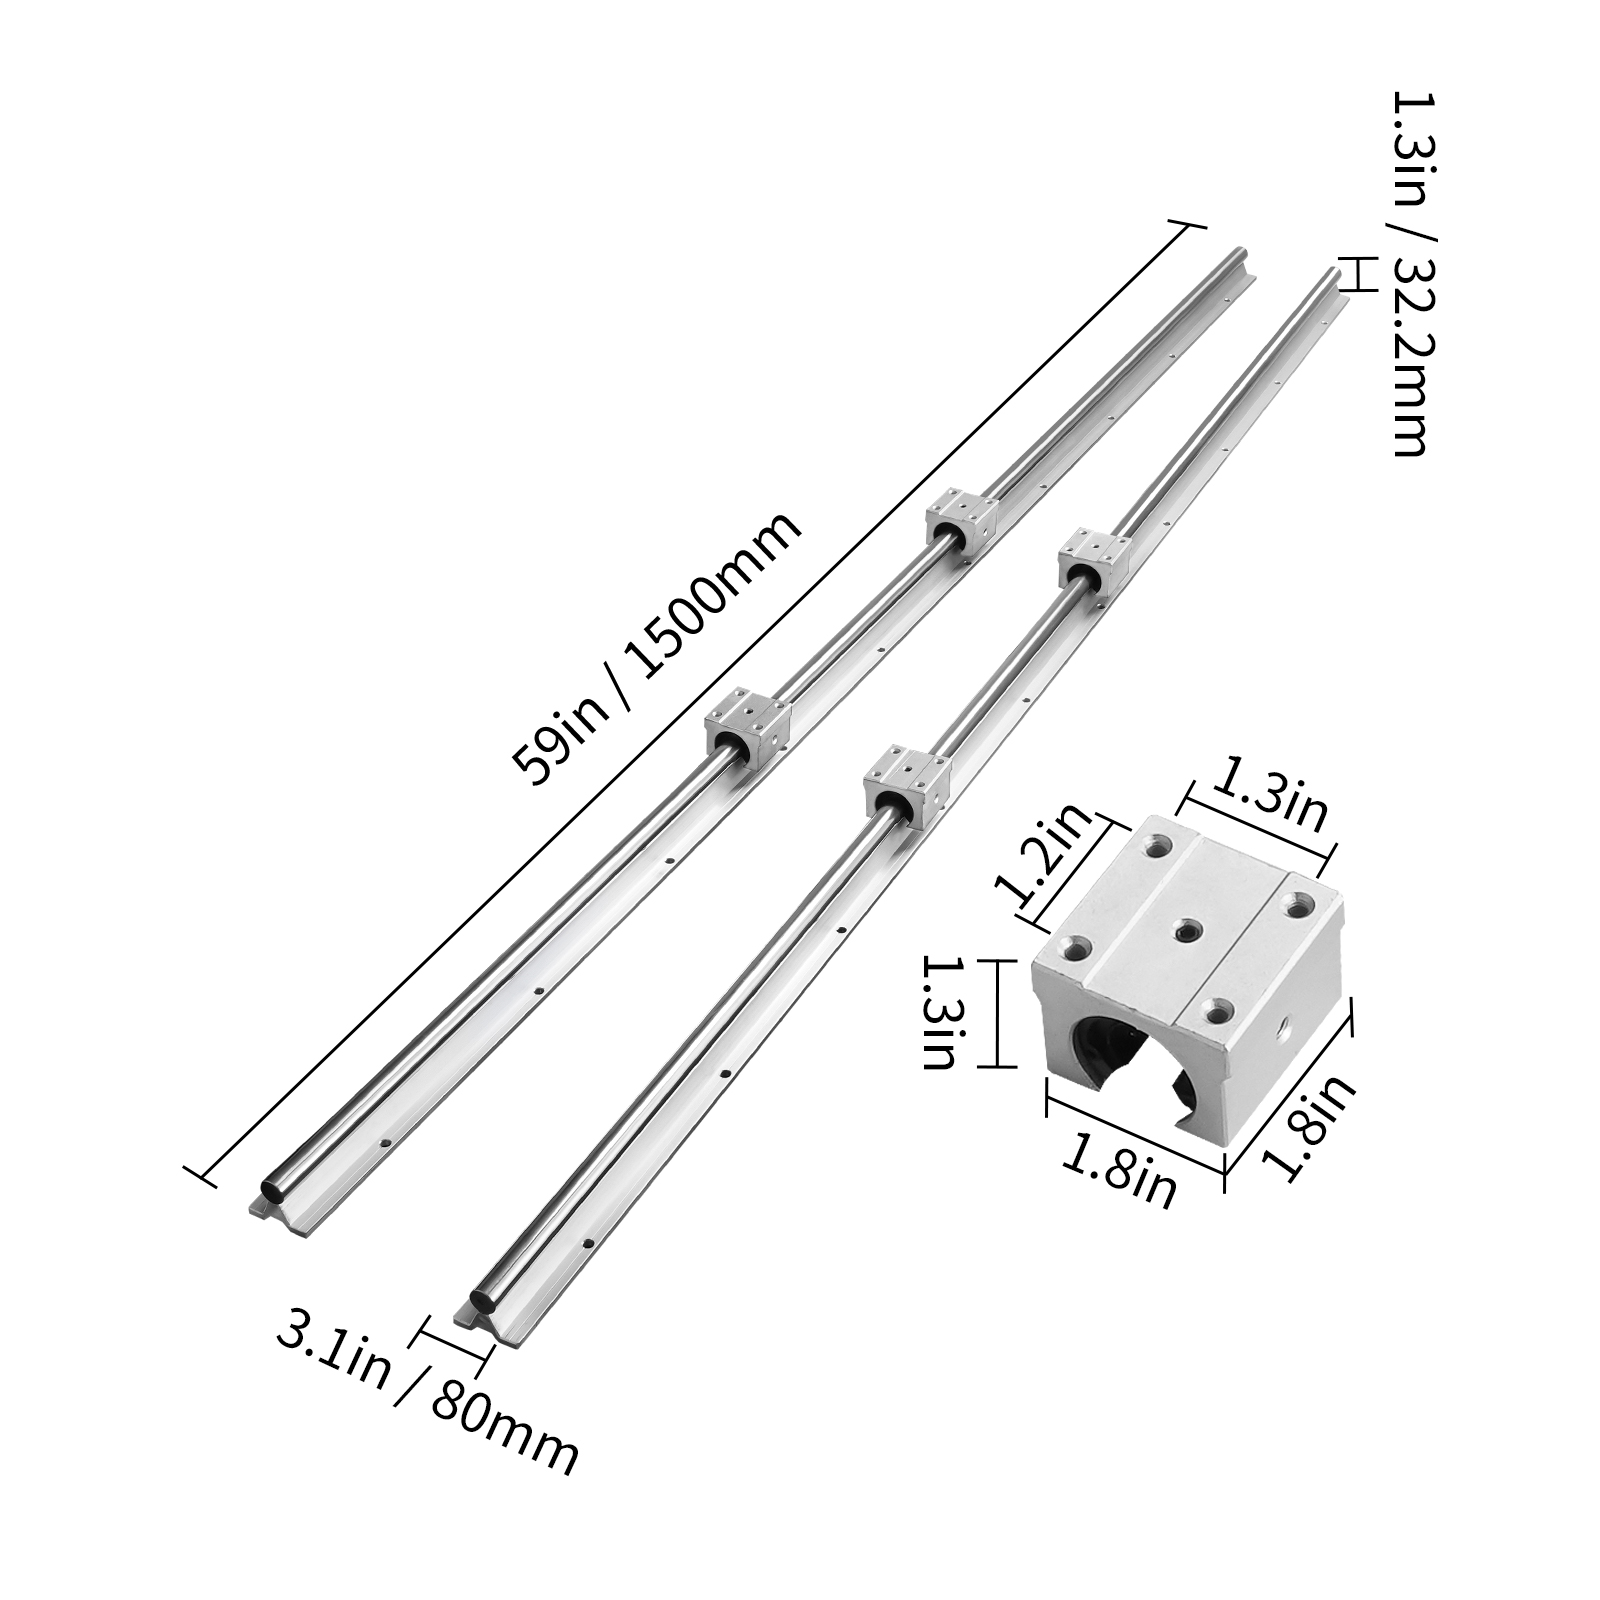
Mounting Vertical Linear Guide Rails: What Actually Works
Most people buying Linear Guide Rails for a vertical setup install them exactly the same way they would for a horizontal machine. That is a mistake. The first thing you need to do is check the mounting surface flatness before anything else, because gravity changes how the rail reacts under load in a way that horizontal mounts don't. I spent about three weeks on a project last year where we had Vertical Linear Guide Rails running in a 5-axis CNC modification. The rail kept drifting after 40,000 cycles. We replaced the rail three times before realizing the issue wasn't the rail itself. It was the aluminum extrusion we mounted it to. The T-slot plate was milled to 0.02mm flatness over a 600mm span. Fine for a horizontal mill. Terrible when your carriage is pushing down at 200kg and the mount flexes just slightly at the center. We ended up grinding the surface down and re-milling it to 0.01mm flatness, then used a torque wrench at exactly 4Nm per bolt in a cross pattern. The drift stopped immediately.
Vertical Linear Guide Rails: Mounting and Setup
Here is the actual process for getting this right the first time. Start with the mounting surface. Use a precision surface plate and a dial indicator if you can. Check flatness along the entire length, not just at the ends. A rail that looks straight to the naked eye can have a center sag of 0.05mm or more. That sag will cause uneven wear inside the recirculating ball blocks and dramatically shorten bearing life. Once your surface is acceptable, you mount the rail using a torque wrench. Do not hand-tighten bolts. Each fastener needs to be torqued to the manufacturer's specification, usually between 3Nm and 8Nm depending on the rail size. Tighten in a cross or star pattern, starting from the center and working outward. This seats the rail evenly against the mounting surface and prevents it from rocking once you apply load. After the rail is mounted, you need to check alignment with the mating rail or axis. Use a dial indicator mounted to the carriage and run it along the rail's reference surface while sliding the carriage the full travel distance. Any variation greater than 0.01mm over the total length means you have alignment issues. On a vertical setup, you also need to check for angularity error. The rail should not twist under its own weight. Mount a test block and measure deflection at both ends with the carriage at top and bottom positions. If the deflection differs by more than 0.02mm, your mounting surface is not rigid enough or the fastener pattern is insufficient.
Load calculation is the part most people skip. A Linear Guide Rail's dynamic load rating tells you how much weight it can handle when moving horizontally. When you mount it vertically, the effective load changes. The carriages are hanging, not pressing down. This means the ball tracks inside the blocks see different stress distribution. Calculate your required dynamic load rating by taking your total moving mass, adding the cutting or machining forces, and multiplying by a safety factor of at least 1.5. For vertical applications, I typically use 2.0 or higher because shock loads from direction changes are more severe than horizontal setups. Sealing matters more on vertical rails. Gravity pulls contaminants downward along the rail surface. A standard scraper seal works fine horizontally but lets fine dust migrate past it vertically. Use dual seals with a wiper on the outside and a contact seal on the inside. If your environment has coolant or chips, add a bellows cover or a full-length protective skirt. This extended maintenance interval from monthly to quarterly without significant contamination issues. Grease choice is another thing people get wrong. Standard lithium-based grease works in most horizontal applications. Vertical rails benefit from a heavier viscosity grade, preferably ISO VG 100 or 150, because the grease needs to resist dripping and maintain a lubricating film between the balls and raceways when the carriage is stationary for long periods. Re-grease intervals should be halved compared to horizontal use. If you are running at high speed, check the manufacturer's limit curves. Vertical operation often reduces maximum speed by 10 to 15 percent due to the added gravitational load on the bearing blocks.
Get the Full Details

If you are using Multiple Carriage setups on a single rail, the load distribution becomes non-linear. The carriage nearest the supported end carries significantly more load. A common rule of thumb is that the outer carriages take 60 to 70 percent of the total load in a two-carriage vertical arrangement. If you need even load distribution, add intermediate support brackets or use a dual-rail configuration with proper preload adjustment between them.
When Vertical Linear Guide Rails Are the Wrong Choice
These rails are not a universal solution for every vertical motion application. If your machine has a lot of side load or moment load, a linear guide rail will wear out quickly regardless of how well you mount it. In those cases, a cylindrical linear guide or a round shaft linear bearing system handles off-axis forces better and at lower cost. I have seen V-slot wheel systems outperform expensive Linear Guide Rails in dirty environments with heavy side loading, even though they look less precise on paper. Another limitation is speed. If you need travel speeds above 2 meters per second on a vertical axis, consider a ball screw with a counterbalance or a direct drive linear motor instead. The ball nut and recirculating blocks generate heat at those speeds, and thermal expansion in a vertical configuration causes positioning drift that is much harder to compensate for than in a horizontal setup. Cost is the final practical consideration. A quality preloaded Linear Guide Rail with matching carriages runs significantly more expensive than a simple guide pin and bushing arrangement. If your precision requirement is under 0.05mm repeatability and the load is under 50kg, a basic guide system is adequate. Don't overspecify because a catalog looks impressive.
The installation process itself takes longer than most estimators account for. A skilled technician needs about 45 to 60 minutes per meter of rail for proper mounting, alignment, and verification. Budget accordingly. Rushing the alignment step to save time costs you in maintenance and replacement down the line, and replacing a worn rail block in a completed machine is roughly five times more labor than doing it correctly during initial setup.