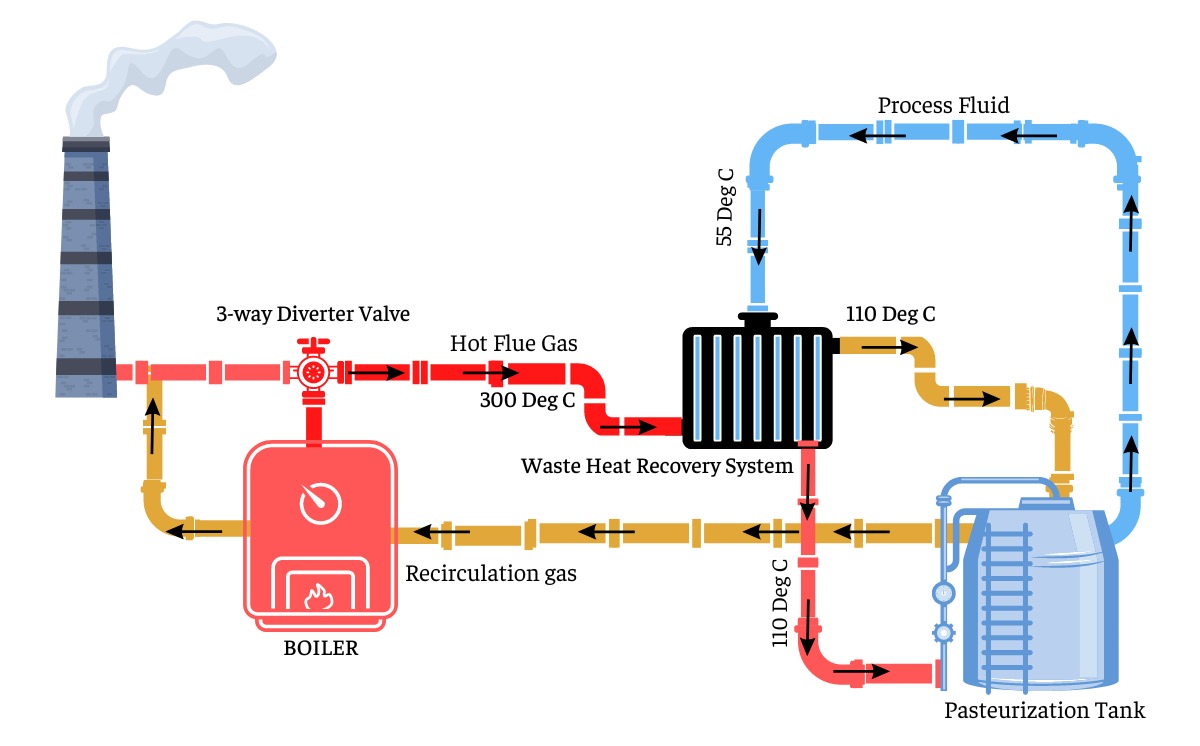
Getting Started With Waste Heat Recovery Technologies
Most people think waste heat recovery is just slapping a heat exchanger on an exhaust pipe and calling it a day. That's not how it actually works in practice. When I first got into this field, I assumed the engineering was straightforward—capture the heat, convert it, done. The reality is messier and more interesting than that.
Understanding Waste Heat Recovery Technologies at the Component Level
Before diving into systems, you need to understand what types of waste heat you're dealing with. The temperature range matters enormously. Low-grade waste heat (below 200°C) behaves completely differently from high-grade sources (above 500°C), and the recovery technology you choose should match the source characteristics, not the other way around. There are three main categories you'll encounter in real installations: direct heat exchange systems, thermoelectric generators, and organic Rankine cycle (ORC) systems. Each has its own sweet spot and each fails in predictable ways if you misapply them.
Direct heat exchange is what most people default to. You run a heat exchanger in the exhaust stream, capture thermal energy, and use it for space heating, domestic hot water, or preheating combustion air. It's simple, efficient, and underwhelming for anything requiring electricity generation. The efficiency numbers look good on paper—sometimes 80-90% thermal recovery—but that's because you're not converting to a different energy form. You're just moving heat around, and heat wants to flow downhill anyway.I once installed a shell-and-tube heat exchanger on a natural gas furnace exhaust at an industrial facility. The math said we'd recover about 15 kW of thermal energy. We did. The problem wasn't the exchanger; it was condensation. The exhaust gas dropped below the dew point, acidic condensate formed, and within six months the copper tubes developed pinhole leaks. The workaround was switching to a plate-and-frame exchanger with stainless steel plates and installing a condensation trap downstream. The recovered energy stayed the same, but the maintenance interval improved from quarterly to annual. Thermoelectric generators (TEGs) use the Seebeck effect to convert temperature differentials directly into electricity. No moving parts, no fluids, no maintenance in theory. In practice, the efficiency is abysmal—usually 3-8% depending on the temperature differential and the material quality. But there are scenarios where TEGs are genuinely the right choice, and those scenarios are often overlooked. The key insight most beginners miss is that TEG efficiency depends on the difference between hot and cold sides, not the absolute temperature of the hot side. A 300°C exhaust source with poor cooling might give you worse results than a 200°C source with aggressive cold-side heat rejection. I've seen engineers oversize the hot-side heat exchanger and undersize the cold side, then wonder why their TEG array produced half the predicted power. The solution was swapping to a liquid-cooled cold plate with a circulation pump. Power output doubled with the same heat source.
Get the Full Details

Another pitfall: TEG modules degrade when operated near their maximum temperature rating for extended periods. Most commercial Bismuth Telluride modules start losing performance after 1,000-2,000 hours at 250°C+ hot side temperatures. If you need longevity over peak output, derate the modules. Run them at 60-70% of their max temperature rating and they'll last ten times longer with acceptable power loss.
Organic Rankine Cycle Systems for Medium-Grade Heat Recovery
ORC systems bridge the gap between simple heat exchange and high-temperature steam cycles. They use organic working fluids with lower boiling points than water, allowing electricity generation from heat sources as low as 80-100°C. The trade-off is complexity and capital cost, but the electricity generation aspect makes them attractive for industrial applications where thermal loads don't justify a full steam cycle. The working fluid selection is critical and heavily influences system performance. Common choices include R245fa, R123, and siloxanes. Each has different critical temperatures, pressures, and environmental profiles. R245fa is widely available and well-characterized, but its global warming potential is 1,000+ times that of CO2. Siloxanes like MDm5 are ODP-zero and GWP-near-zero, but they decompose at high temperatures and can form solid deposits in the expander. I learned this the hard way when a facility using MDm5 in a retrofit installation spent $40,000 on expander rebuilds after the fluid broke down into siloxane polymers inside the scroll mechanism. The expander type matters enormously too. Scroll expanders work well for small-scale ORC (under 100 kW electrical) and handle the two-phase flow better than turbines, but they have limited capacity. Radial inflow turbines are more efficient at larger scales but require drier vapor entry and precise nozzle geometry. For most waste heat recovery applications under 50 kW, scroll expanders are the pragmatic choice despite lower isentropic efficiency.
Practical Design Considerations for Real Installations
When sizing a waste heat recovery system, the first thing to measure is the actual exhaust flow rate and temperature profile over a complete operating cycle. Nameplate values are meaningless. I once saw a facility specify a waste heat recovery system based on a furnace nameplate of 500°C exhaust at 2,000 Nm³/h. The actual operating condition was 320°C average with frequent dips to 180°C during load transients. The heat exchanger they ordered was oversized for the mean condition and couldn't maintain minimum gas velocity during low-load periods, leading to fouling from particulate deposition. Particle filtration upstream of any heat recovery equipment is non-negotiable for industrial exhaust streams. Even with what looks like clean combustion, fly ash, soot, and condensed hydrocarbons will accumulate on heat transfer surfaces. A simple bench filter or cyclone separator before the heat exchanger extends cleaning intervals by orders of magnitude. The capital cost is minimal compared to the downtime savings from avoided soot blowdowns. Control strategy is where most waste heat recovery systems fail operationally. The recovery system must never compromise the primary process. If your heat exchanger causes backpressure buildup in the exhaust stream, the furnace or boiler will respond negatively. I've seen control systems that modulated exhaust dampers to maintain heat recovery temperature, only to discover the upstream equipment was surging because the damper positioning was creating unstable flow conditions. The fix was implementing a constraint-based controller that treated the exhaust backpressure as a hard limit, not a control variable.

Common Pitfalls That Wipe Out Project Economics
One of the most common mistakes is neglecting the parasitic load of the recovery system itself. Pumps, fans, controls, and auxiliary heating all consume energy that reduces net recovery. A system that appears to recover 100 kW of thermal energy might only deliver 65 kW net after accounting for circulation pumps and control system power. This is especially relevant for ORC systems where the working fluid pump can consume 5-15% of gross electrical output. Another economic killer: assuming the recovered energy has the same value as the energy it replaces. Waste heat recovery economics depend heavily on what you do with the recovered energy. Electricity has higher value than thermal energy in most tariff structures. Thermal energy displaced from a gas furnace might save you $0.03/kWh in fuel, while electricity from an ORC system could displace $0.12/kWh in grid purchases. But if you can't sell the electricity at a favorable rate or the thermal energy isn't usable on-site, the project economics collapse regardless of technical feasibility. Corrosion assessment is frequently skipped during the feasibility phase. Acid dew point corrosion affects any system where exhaust gases cool below the condensation temperature of sulfuric or hydrochloric acids. Gas-fired equipment typically produces sulfuric acid condensation if exhaust drops below 130-150°C depending on fuel sulfur content. Material selection must account for this. 316L stainless steel handles mild acid condensation; duplex stainless steels or nickel alloys are needed for severe conditions. I've seen carbon steel heat exchangers fail within a year in applications where the designer assumed dry operation but never verified the actual exhaust composition.
When Waste Heat Recovery Doesn't Make Sense
Sometimes the numbers don't work, and you should walk away. Small temperature differentials (less than 50°C between source and sink) rarely justify the capital investment unless the waste heat source is essentially free and you have existing infrastructure to connect to. The Carnot efficiency limit means low-grade heat can only be converted to work with poor efficiency, and even direct thermal recovery faces diminishing returns as the temperature lift decreases. Highly variable or intermittent heat sources are another scenario where recovery systems underperform. A waste heat source that operates at full load for 2,000 hours per year versus 8,000 hours makes a massive difference to project payback. I've seen several installations that looked viable on paper but delivered mediocre results because the underlying equipment had seasonal operating patterns that left the recovery system idle for months at a time while the capital costs continued accumulating. Dirty or fouling-prone exhaust streams present a special challenge. If the exhaust contains sticky particulates, tar, or condensable organics, maintenance intervals shrink and availability drops. The recovery system might work perfectly for three months before fouling reduces heat transfer coefficients by 40%, requiring shutdown for cleaning. In these cases, the levelized cost of recovered energy rises significantly, and simpler recovery methods (or none at all) may be economically superior to a complex system that's constantly under maintenance.
Implementation Roadmap for a Typical Industrial Application
Start with a detailed energy audit. Measure actual operating conditions over multiple cycles, not single snapshots. Record temperature, flow rate, and composition data at representative points. This data drives every subsequent decision. Next, identify the recovery target. Are you trying to generate electricity, provide process heat, or preheat combustion air? Each target selects different technology pathways and changes the economic analysis substantially. Preheating combustion air is often the simplest and most economical option because it doesn't require conversion equipment—just a heat exchanger sized for the available temperature differential. For electricity generation, the decision tree branches based on heat source temperature and availability. Below 150°C with steady operation, ORC is the only practical conversion technology. Between 150-400°C, you might consider ORC or advanced TEG arrays depending on the required power output. Above 400°C, steam cycle recovery becomes viable and is often more efficient than organic cycles for large installations.

Once technology selection is complete, detailed design should address fouling mitigation, materials compatibility, control architecture, and maintenance access. These aren't optional extras—they're the factors that determine whether your recovery system operates reliably for five years or requires constant attention and frequent replacements. The final consideration is the economic model. Calculate net present value using realistic operating profiles, not nameplate conditions. Include parasitic loads, maintenance costs, and expected degradation in your analysis. A system that appears to pay for itself in three years under ideal conditions might have an eight-year payback when you account for real-world performance drift and operational interruptions. The gap between theoretical and actual performance is where most waste heat recovery projects find their true economics.