Reading Weld Symbols on Drawings
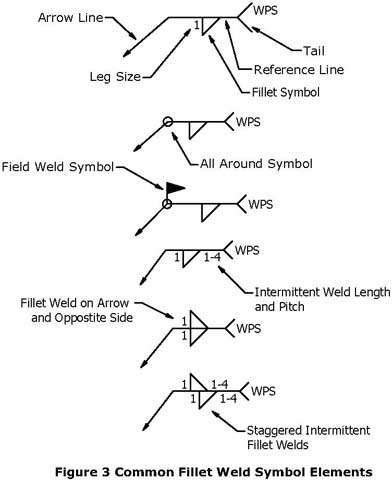
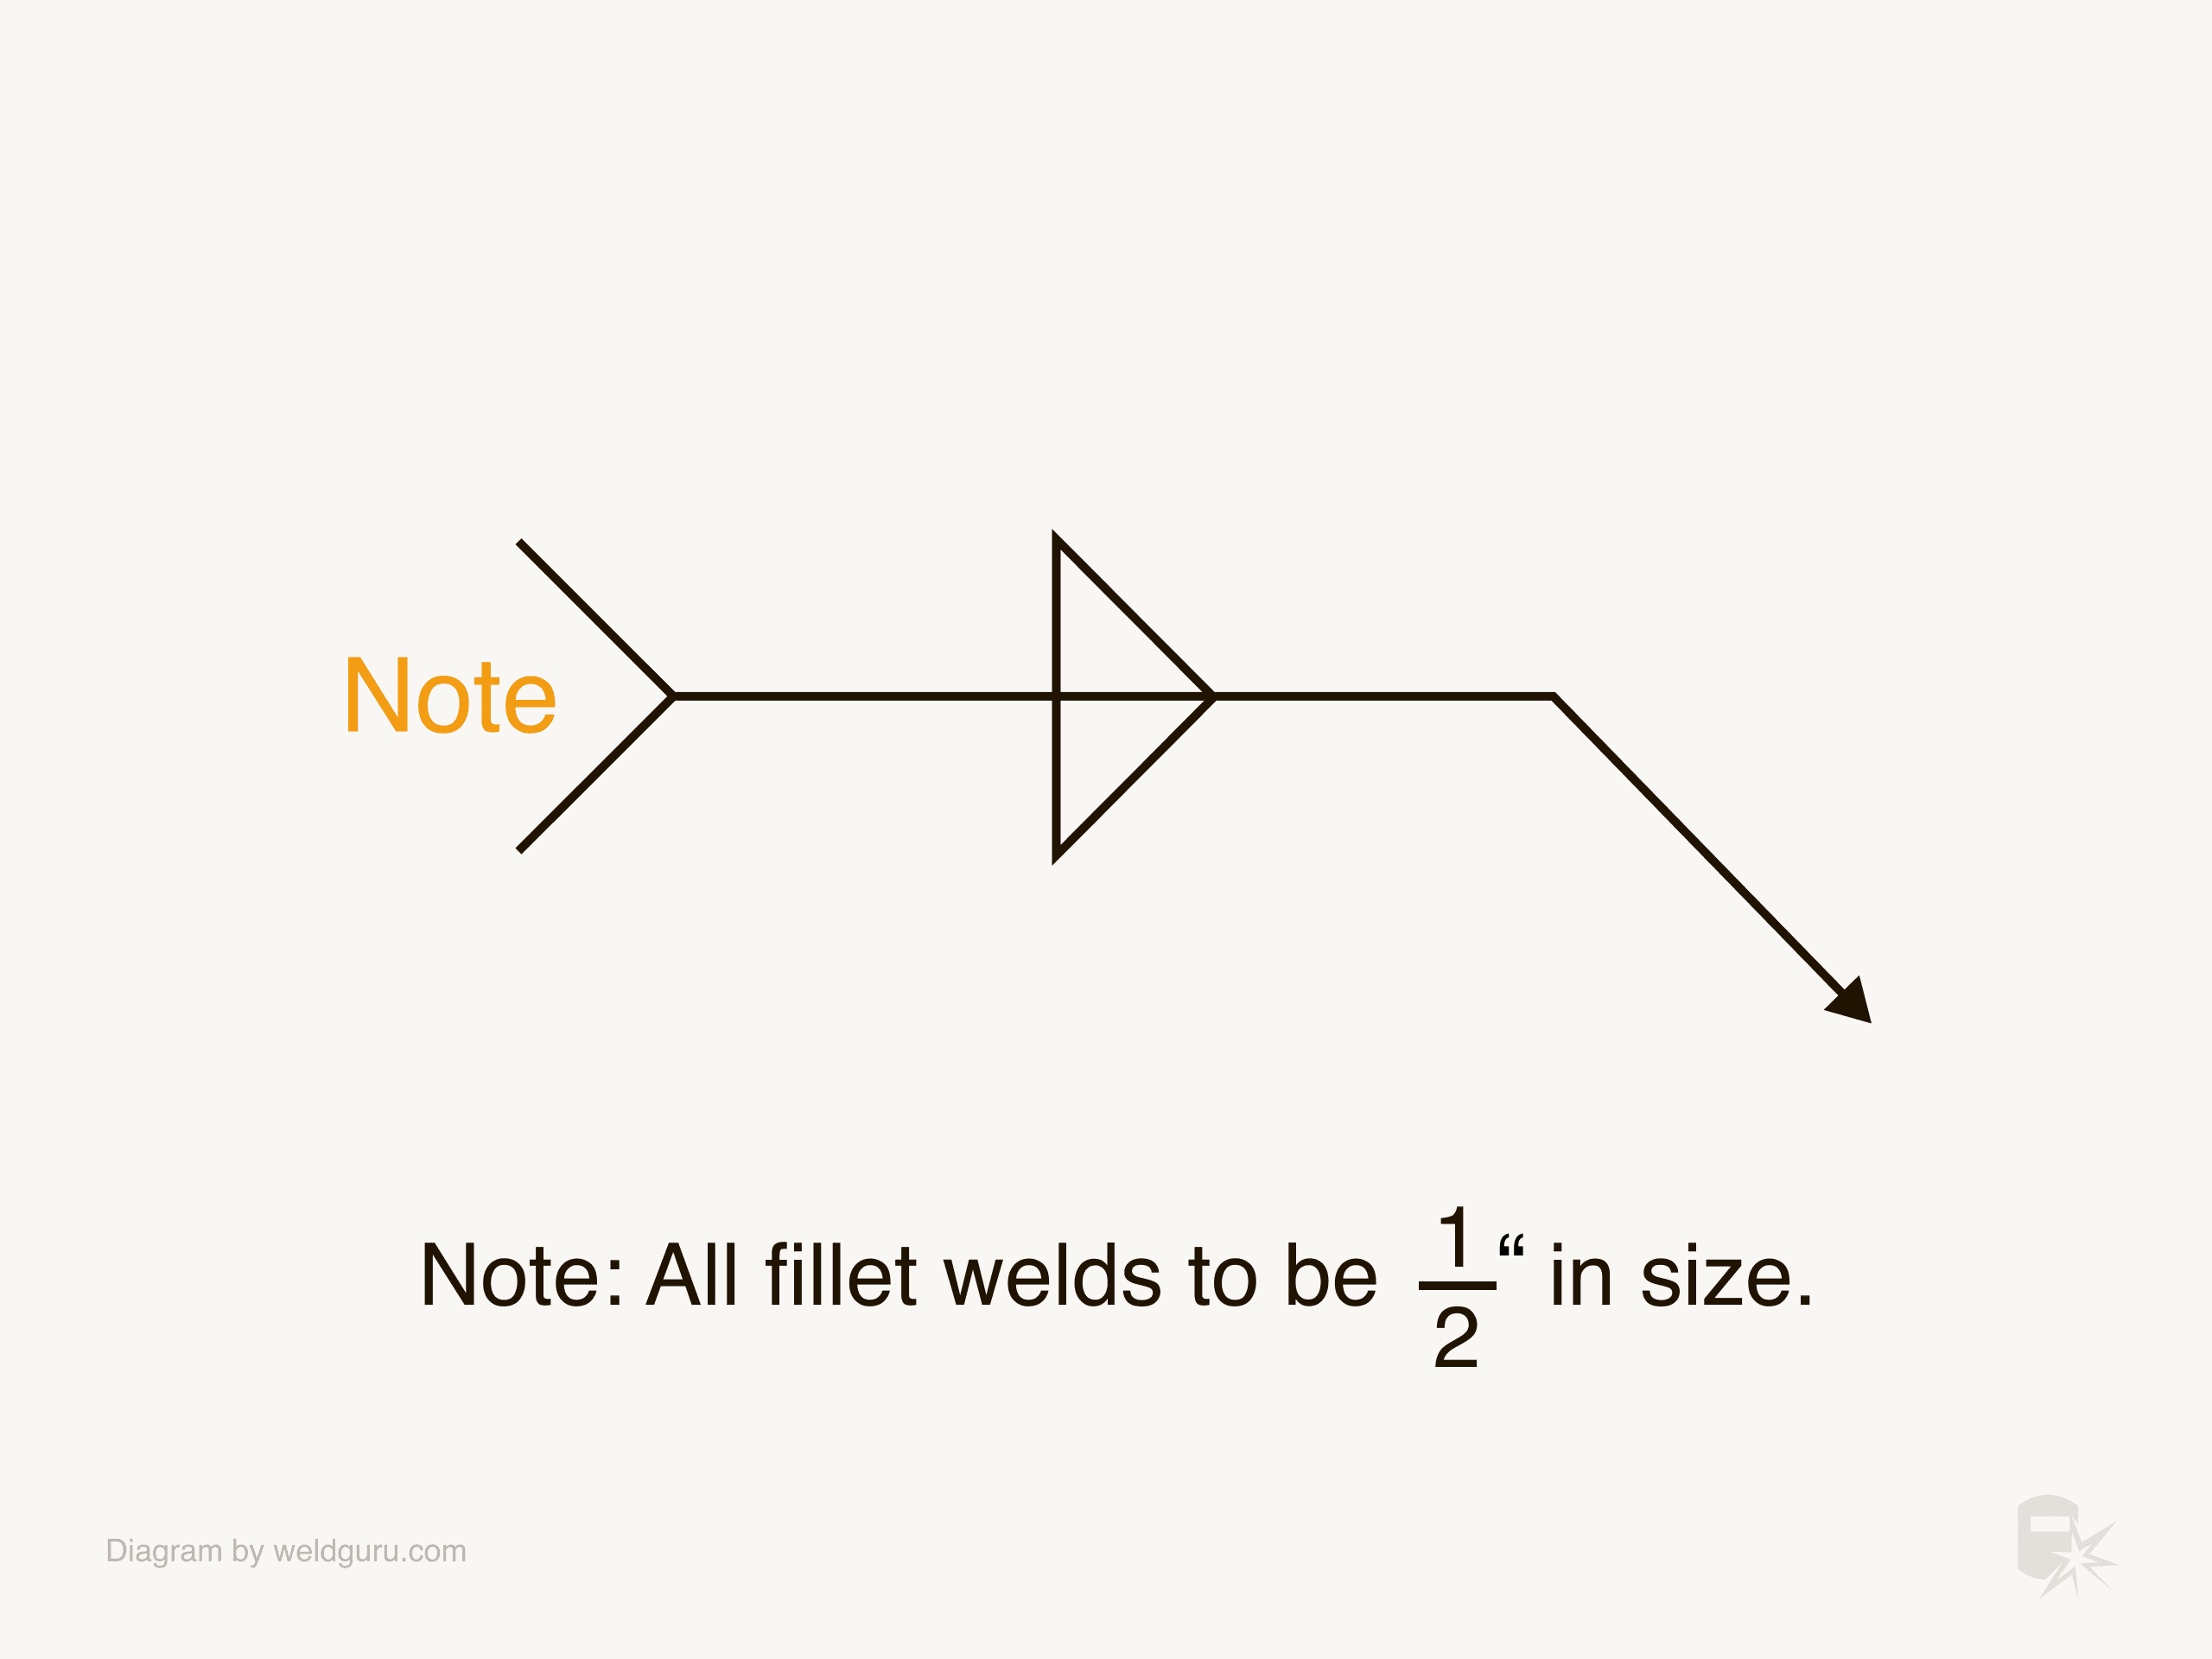
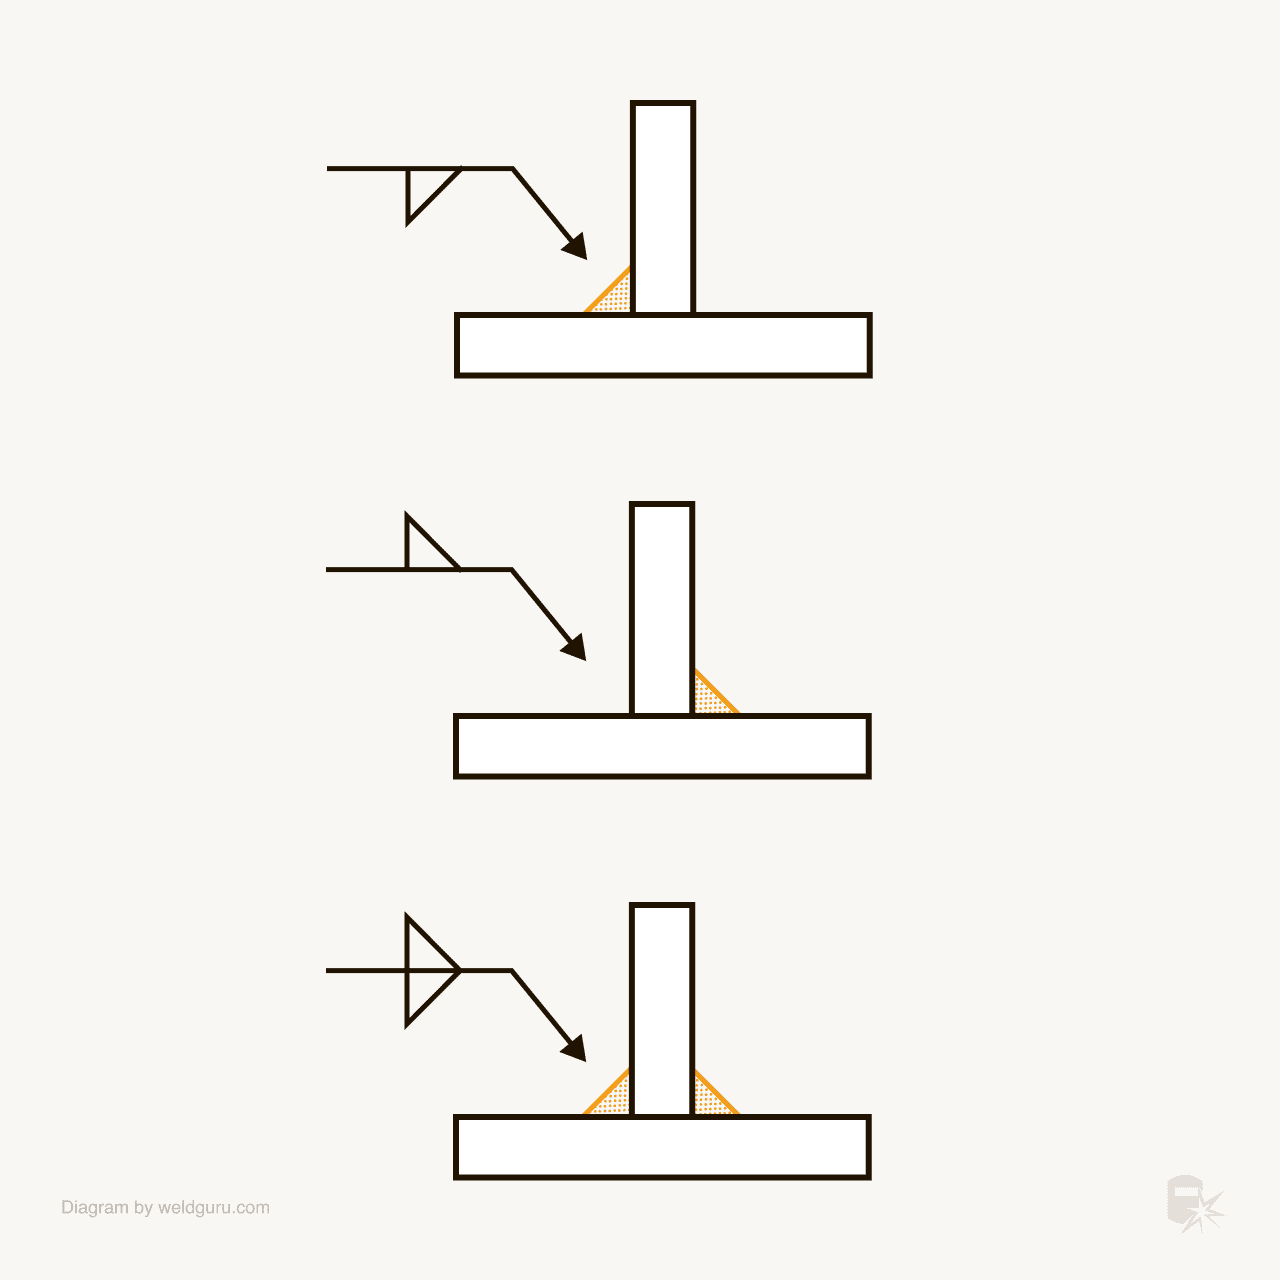
The welding symbol is a standardized shorthand that communicates what kind of joint to make, how big the weld should be, and where to place it. When you pick up a blueprint and see a weld symbol, you need to decode it quickly because misreading even one element can result in a welded assembly that doesn't meet the structural requirements. The American Welding Society standard AWS A2.4 governs these symbols, and most fabrication shops in the US follow it strictly. A fillet weld symbol looks like a right triangle with the vertical leg on the left and the horizontal leg on the bottom. That is the only shape you need to memorize for fillet welds. The size goes to the left of the triangle. A symbol reading 3/8 might look small, but it represents three-eighths of an inch. If you see 6, that is millimeters. Always check which system the drawing is using before you start welding. The length of the weld goes to the right of the triangle. A dash after the length number means the weld runs continuously along the entire joint. No dash means it is an intermittent weld, and you will see pitch values further to the right. The arrow side versus other side designation determines which leg of the joint the weld sits on. If the triangle sits below the reference line, the weld goes on the arrow side. If it sits above the reference line, the weld goes on the other side. Both sides means you see triangles above and below the line with the same specifications. This is where people make mistakes. I once had a joint called for a single fillet on the arrow side with a 1/4 inch size, and the welder read it as a double fillet because the symbol was smudged near a dimension line. The inspection report came back rejecting the joint. Redrawing the symbol with cleaner spacing and adding a note to verify arrow-side placement before beginning work was the fix. It cost us two days of rework on a custom structural frame.
The field weld symbol is a small flag at the junction where the arrow meets the reference line. That flag tells the welder this joint must be welded in the field, not in the shop. Skip it and you might deliver a piece that cannot fit together on site because the weld would interfere with alignment bolts or fit-up. The weld-all-around symbol is a circle at that same junction point. It means the weld continues around the entire perimeter of the joint. Using it instead of calling out individual sides saves time on complex shapes and reduces the chance of a welder missing a section. Here is a practical breakdown of the main elements:
| Element | What it tells you |
|---|---|
| Triangle shape | Fillet weld type |
| Number left of triangle | Weld size (leg length or throat) |
| Number right of triangle | Weld length |
| Dash after length | Continuous weld |
| Numbers after length | Pitch for intermittent welds |
| Flag symbol | Field weld required |
| Circle at junction | Weld all around |
| Position above/below line | Arrow side or other side |
The process designation goes in the tail of the symbol. MIG, TIG, SMAW, flux-cored — whatever the specification calls for appears there. If the tail is blank, the process is either specified elsewhere on the drawing or left to the welder's discretion. In most engineered drawings, the process will be defined in a general notes section rather than in every individual symbol tail. That is normal and not an oversight. The most frequent error I see is confusing the effective throat with the leg length. The leg length is the measurement of each side of the triangle. The effective throat is the shortest distance from the root to the face, roughly 0.707 times the leg length for an equal-leg fillet. Some engineers specify throat requirements directly. If the drawing says 5mm throat, you need a leg length of about 7mm, not 5mm. Welding to 5mm leg when 5mm throat was specified gives you a weld that is undersized by nearly thirty percent. That difference is the gap between passing inspection and having to cut out the joint and start over. Another issue is the misconception that a weld symbol covers the entire joint automatically. It does not. If the symbol shows a length of 3 inches with a pitch of 6 inches, that is a 3-inch weld every 6 inches on center, not a continuous weld. Running that as continuous will add unnecessary heat input, cause more distortion, and waste consumables. On a long beam-to-column connection, I once caught a team running intermittent fillet welds continuously because the pitch notation was written in a cramped corner and nearly unreadable. The extra weld metal changed the stress distribution in the connection. We ground out approximately forty percent of the welds and re-cut them to spec.
Get the Full Details
The weld contour symbol matters if the joint requires a flush finish or a convex profile. A flat contour is the default. A convex contour means the weld face bulges outward, which increases the leg length beyond the nominal size. A concave contour means the weld is ground or naturally flows inward, producing a smoother transition that reduces stress concentration. For fatigue-critical joints, a concave contour is often specified because the smoother geometry disperses stress better. If the drawing does not call for any contour, assume convex by default for a fillet weld, since that is the natural shape a weld bead takes. Prefabricated weld symbols can speed things up. Instead of repeating the same fillet specification on every joint in a truss, the engineer can put a note like "all fillets 3/8 x 6 on 12 unless noted otherwise" and then use local overrides where needed. This keeps the drawing cleaner and reduces symbol clutter. However, it also means the welder has to read the general notes carefully. A local override that says "1/4 all around" on one specific joint does not change the default for the rest of the drawing. Ignoring that hierarchy is another common source of field errors. The root gap and bevel angle are separate from the fillet weld symbol itself but are often shown nearby on the joint detail. A fillet weld on a square-edge butt joint is different from a fillet weld on a prepared groove joint. The symbol alone does not tell you the gap. If the joint requires a specific root opening for access or fusion, that dimension will be on the joint detail drawing, not inside the weld symbol. Mixing those two sources of information is why some welders end up with poor root penetration on joints they thought were straightforward fillets.
Practical Tips From the Shop Floor
When you are reading a symbol for the first time, go through it in order: process, location, size, length, pitch, contour, and any special notes. Skipping the tail or ignoring the flag is where most quick-read errors happen. If the drawing is in metric, verify whether the size numbers are in millimeters or if there is an explicit inch conversion noted. I have worked on projects where the architectural drawings were in feet and inches but the structural steel fabrication package switched to millimeters without updating the title block, and the resulting weld sizes were off by a factor of twenty-five. For intermittent fillet welds, the pitch measurement is center-to-center, not edge-to-edge. A 3-inch weld on 6-inch pitch means the center of each weld segment is 6 inches apart. The gap between weld segments is 3 inches. Confusing edge-to-edge with center-to-center pitch shortens the actual weld length and weakens the joint. On a simple lap joint with 4-inch welds on 8-inch pitch, using edge-to-edge spacing would leave you with only 2 inches of weld per 8-inch segment instead of 4 inches. The backing strip notation is worth noting if you encounter it. A small rectangle below the reference line indicates a permanent backing strip. Its absence does not necessarily mean no backing — it might mean the welder is expected to use a temporary backing method or single-side weld with proper melting. If the specification requires complete joint penetration on a groove weld, the fillet weld symbol alone does not communicate that requirement. You need the groove weld symbol with the appropriate preparation details alongside it.
One thing that does not get enough attention is the effect of welding position on the symbol interpretation. The symbol does not change based on position, but the allowable size and travel speed do. A 1/4 inch fillet weld overhead is harder to hold consistent than the same size on a flat position. If the drawing calls for tight tolerance on weld size across multiple positions, consider specifying a maximum leg length slightly below the nominal to account for positional variation. It is a small adjustment that prevents a lot of scrap. When dealing with multi-pass fillet welds, the symbol itself does not specify the number of passes. That information comes from the welding procedure specification and the welder's judgment based on material thickness and joint configuration. A 1/2 inch fillet on 3/4 inch plate might take three passes. The same size on 1/4 inch plate might be a single pass. The drawing will not tell you that. It will only give you the final size requirement. Understanding what that means in practice comes from experience, not from the symbol alone.