The Viscosity Thing That Nobody Gets Right
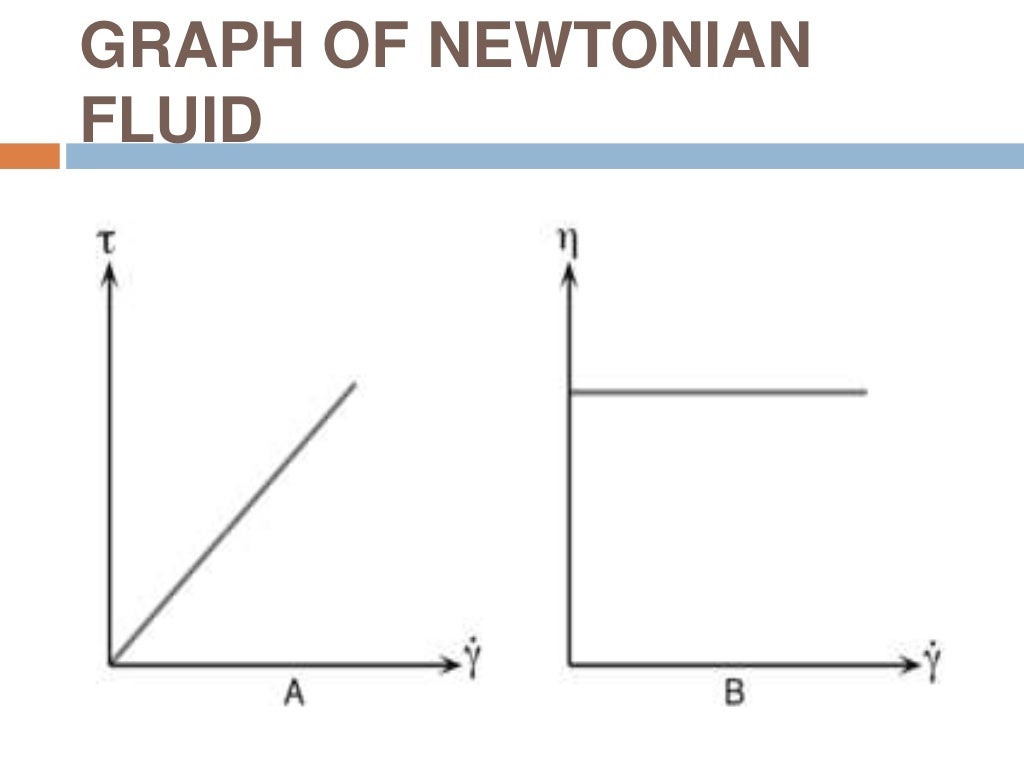
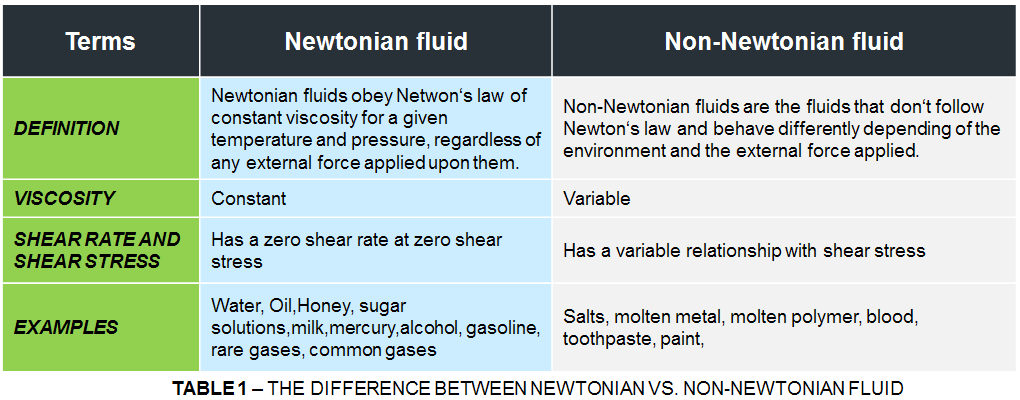
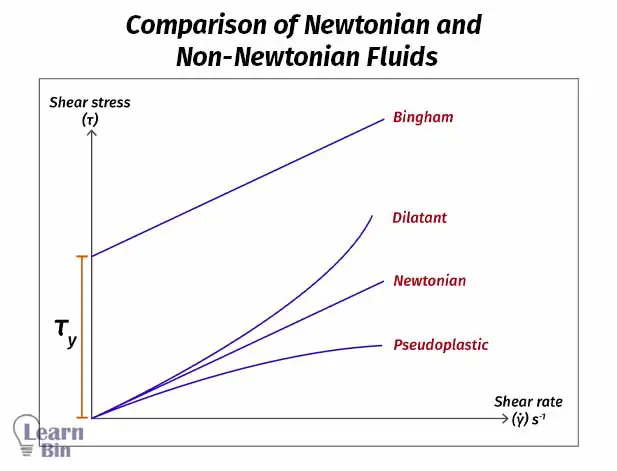
Most people think viscosity is just a number you look up in a table and move on with. It isn't. Viscosity is a behavior that changes depending on how hard you push it, how fast you push it, and sometimes how long you've been pushing it. Getting this wrong is why some processes fail at pilot scale and then look fine on paper. A Newtonian fluid is defined by having constant viscosity at a given temperature and pressure. Water, mineral oil, ethanol, and light hydraulic fluids all fall here. Double the shear rate, you get double the shear stress. The ratio stays fixed. That's it. There's nothing mystical about it. A Non Newtonian fluid breaks that rule. The viscosity changes with applied shear. Some thin out. Some thicken. Some need a minimum stress to start flowing at all. Oobleck is the party trick version, but the real industrial versions are a lot more complicated and a lot more expensive to get wrong.
Shear Thinning vs Shear Thickening vs Yield Stress
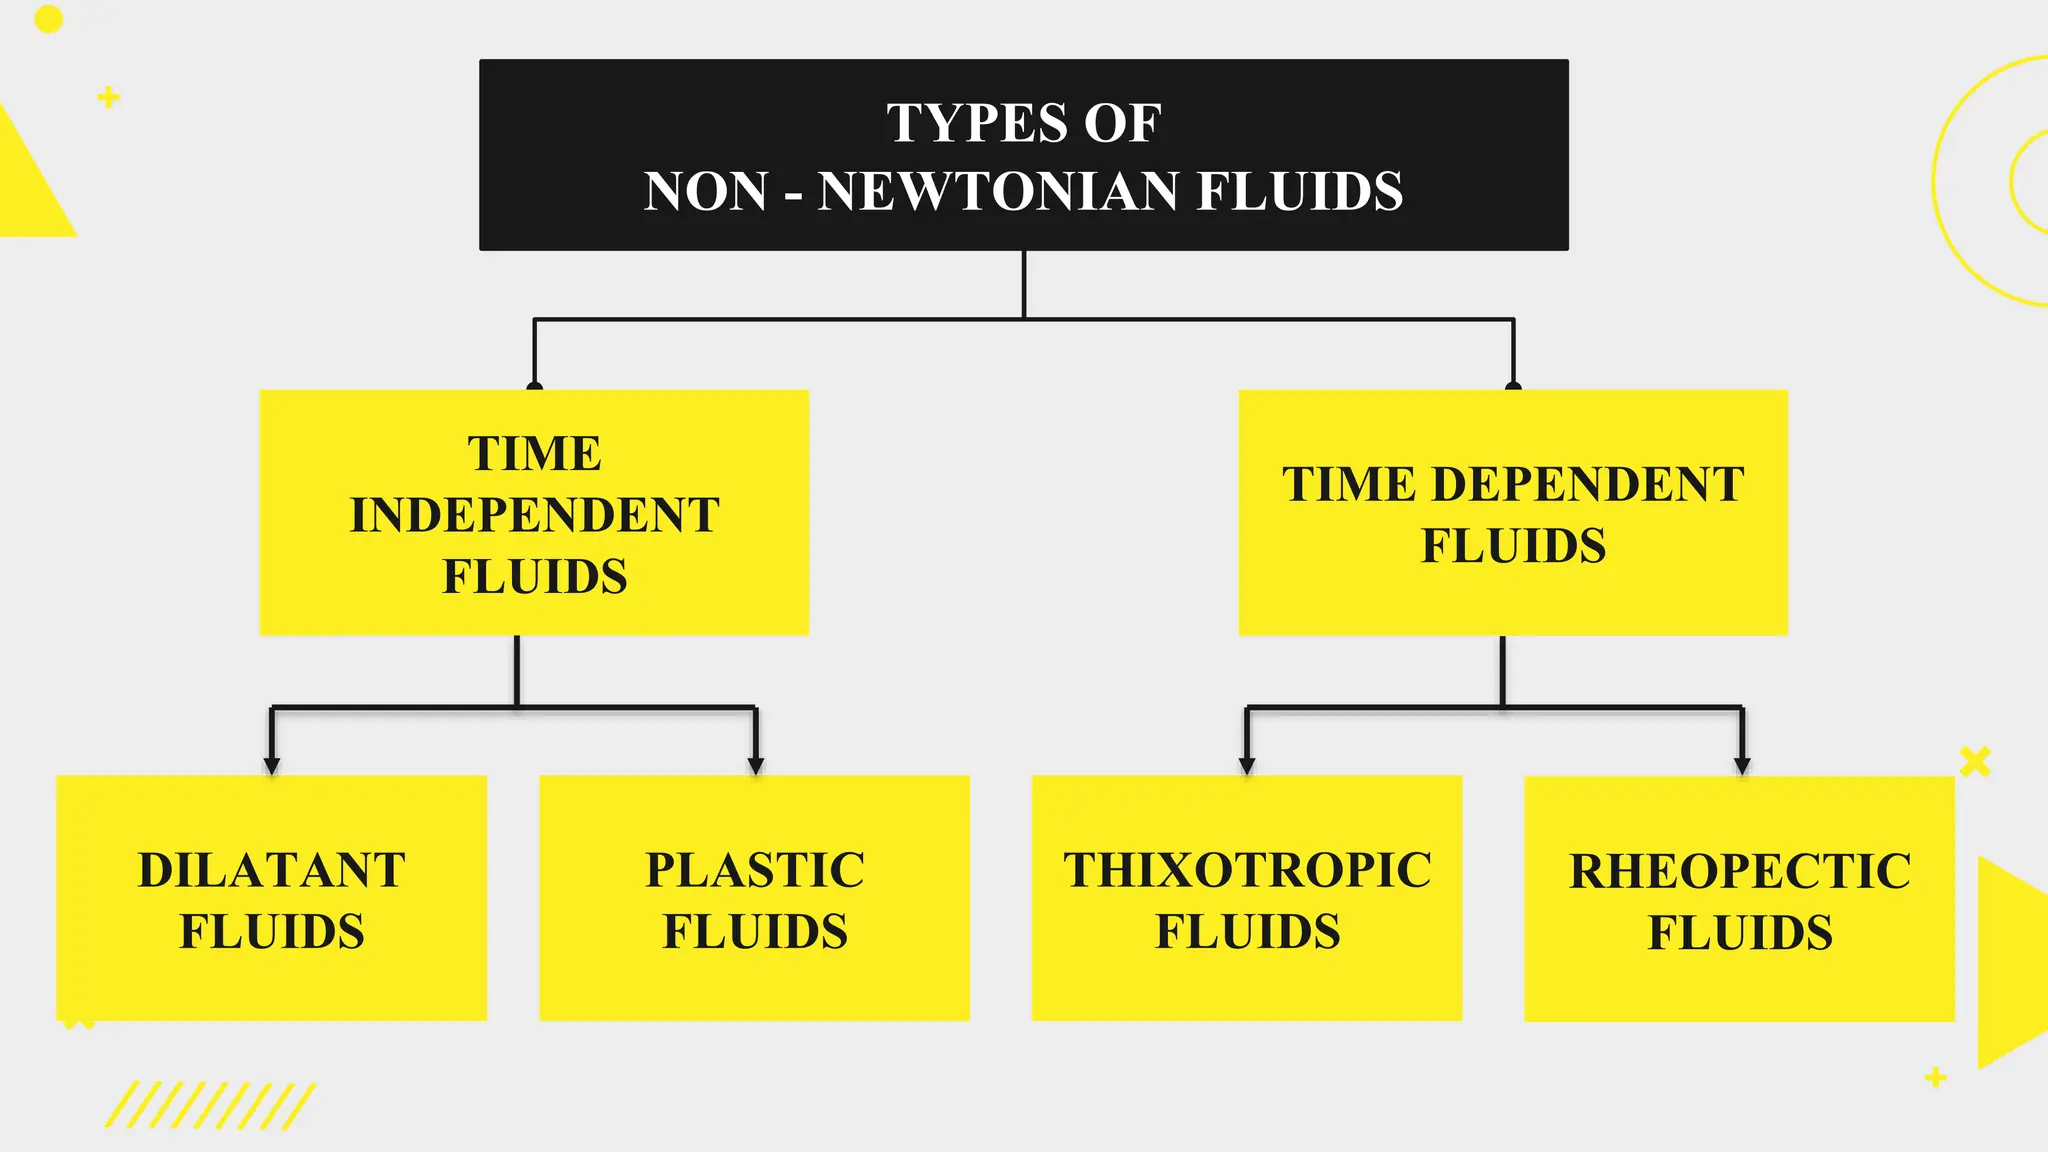
Shear thinning means the fluid gets less viscous as you increase shear rate. Paint is a classic example. It flows off the brush easily but sits on the wall without running. Ketchup works the same way. Polyacrylate-based thickeners, xanthan gum solutions, and most polymer melts behave like this. The viscosity can drop by one or two orders of magnitude across the typical processing range. You need a rheometer curve, not a single number, if you're doing any real calculation. Shear thickening is rarer but more destructive. A cornstarch suspension in water roughly doubles or triples its viscosity when you hit it hard enough. Dilatant powders in suspension, some silica dispersions, and certain concentrated particle systems do this. If you're pumping a shear thickening slurry through a narrow orifice, the pressure spike can be violent. I once watched a 2 inch diaphragm pump develop a pressure oscillation that sounded like gunfire because the slurry was transiently jamming the check valve. The fix wasn't more pump. It was lowering the solids loading and switching to a larger bore line with a slower stroke rate. The pump didn't change. The operating window did. Yield stress fluids need a minimum stress before they flow at all. Below that threshold they behave like a soft solid. Above it, they may shear thin, stay Newtonian, or even shear thicken after yielding. Toothpaste, bentonite mud, and many food suspensions sit here. The practical consequence is that a pump running below its yield point will just churn and heat the fluid without moving it. You'll burn the motor trying to push something that refuses to move. I learned that the hard way with a wax-based coating slurry at about 18 percent solids. The manufacturer's spec sheet listed a plastic viscosity and a yield value, but the yield value was temperature dependent and shifted by nearly 40 percent between 20°C and 35°C. We sized the heater tray for the lower bound. When ambient temperature crept up in summer, the yield stress dropped and the slurry started channeling instead of flowing uniformly. The product came out laminated and weak. The workaround was to add a small amount of a dispersant that stabilized the yield stress across that temperature band, then reverify with a vane spindles test at the actual operating temperature before committing to the next batch.
How to Actually Characterize These Materials
You don't characterize non Newtonian fluids with a viscosity cup. You need a controlled rate or controlled stress rheometer and you need to run a flow curve. Start with a steady shear sweep from low to high shear rate. Record the apparent viscosity at each point. Fit the data to a model. The Power Law model, also called the Ostwald de Waele equation, is the default for shear thinning systems where the log viscosity versus log shear rate plot is roughly linear. It has two parameters: the consistency index and the flow behavior index. When n equals 1 you are back to Newtonian. When n is below 1 you have shear thinning. When n is above 1 you have shear thickening. The model is simple, but it fails at very low and very high shear rates for most real fluids, so don't trust it outside the range you actually measured. The Carreau model adds a zero shear viscosity and an infinite shear viscosity plateaus with a time constant. It fits polymer melts and concentrated solutions much better over a wide range. The Cross model is similar and often preferred when you have a clear Newtonian plateau at low shear. If your material has a yield stress, the Herschel Bulkley model extends the Power Law by adding a yield term. That is the one you use for pastes, slurries, and food gels. Fitting these models by hand is tedious. Use the built-in fitting tools in common rheology software. Do not rely on a single point measurement to reverse engineer a model parameter. It won't work. Time dependent behavior is a separate problem. Some fluids are thixotropic, meaning their viscosity decreases over time under a constant shear and recovers when the shear stops. Bentonite clay, some gel bearings, and certain printed circuit board solders behave this way. Other fluids are rheopectic, which is basically the opposite and much rarer. A yogurt stabilizer system I worked with showed clear thixotropy on a three interval test. The breakdown recovery was incomplete after 60 seconds of rest, which meant that any process relying on quick filling and quick setting needed a different additive package or a longer dwell time between shear events. Measuring this requires a structured rheological test, not a quick check.
Get the Full Details

Pitfalls That Cost Real Money
The biggest mistake I see is treating a non Newtonian fluid as Newtonian for Reynolds number and pressure drop calculations. It screws up everything. A polymer solution that reads 100 centipoise on a viscometer at one shear rate might read 15 centipoise at the shear rate inside a pipe. Using the high number will massively overpredict pressure drop. Using the low number will underpredict it. The correct approach is to calculate an apparent viscosity at the wall shear rate for your specific geometry and flow regime, then iterate. For a Power Law fluid in a pipe, the wall shear rate is not 4Q divided by pi R cubed. It is 4Q times 3n plus 1 divided by 3n pi R cubed, where n is the flow behavior index from your fit. That correction factor alone can shift your calculated shear rate by 30 to 50 percent for typical shear thinning materials. Another mistake is ignoring normal stress differences. In polymer melts and concentrated solutions, the first normal stress difference drives die swell. If you extrude a shear thinning polymer through a die and measure the diameter of the extrudate, it will be larger than the die opening. The effect scales with shear rate and with elasticity. If you are doing any coating or extrusion process and ignore die swell, your product dimensions will be wrong. The fix is empirical. Run a die swell test at your target shear rates and build a correction curve into your process. No amount of theoretical calculation replaces that data. Temperature coupling is another trap. Viscosity is exponentially dependent on temperature for most fluids. A 10 degree Celsius change can shift viscosity by 20 to 50 percent depending on the fluid. If your process involves frictional heating, heat from downstream equipment, or ambient swings, your viscosity estimate from a lab measurement at 25°C will not hold. Measure at the actual processing temperature or use an Arrhenius-type temperature correction with experimentally determined activation energy for viscous flow.
When to Use What Measurement Method
Rotational rheometers are the workhorse. Use a cone and plate for small sample volumes and high precision. Use parallel plates for materials that might slip or have large particles. Use a vane geometry for yield stress materials and structured gels where wall slip would destroy your data. I have seen people use a standard spindle viscometer on a thixotropic paste and get completely wrong numbers because the spindle geometry imposed a shear history that destroyed the structure before the reading stabilized. Switching to a vane SP6 spindle and a controlled stress mode fixed it. The viscosity curve matched the rheometer data within 5 percent. Capillary rheometers are better for high shear rate data that rotational instruments cannot reach. If you need shear rates above about 10,000 per second, go capillary. You also need to correct for entrance pressure drop using the Bagley correction and for non Newtonian shear rate using the Rabinowitsch correction. Skipping either correction gives you systematic errors that compound quickly. For field work where a lab instrument is not available, a rotational viscosity meter with a suitable spindle can give you a quick check, but treat the result as a single point at a single shear rate. Do not extrapolate it to other conditions. I keep one of these in the shop for rough screening. It takes about 5 minutes to run a sample, and it catches gross failures like incomplete dispersion or unexpected phase separation before you waste time on a full rheological characterization.
Limitations You Need to Accept
No single model fits every fluid over every shear rate range. Power Law is convenient and widely cited, but it is mathematically incorrect at both extremes for most real materials. Carreau and Cross are more realistic but require more parameters and better data. Herschel Bulkley is essential when yield stress exists, but fitting all three parameters simultaneously from noisy data is unstable. You need good low shear data to pin down the yield stress, and good high shear data to pin down the flow index. Garbage in, garbage out applies harder here than in almost any other area of fluid mechanics. Wall slip is a real problem with concentrated suspensions and emulsions. The fluid near the wall moves faster than the bulk, making your measured viscosity artificially low. Roughened geometries, sandblasted plates, or vane tools reduce this effect. If your viscosity drops when you change the gap on a parallel plate test, you are probably seeing slip. Correct for it or change the geometry. Some fluids degrade under shear. Polymers break, emulsions break, particle networks collapse. Your viscosity curve will depend on how much shear history the sample has experienced. This is not a measurement error. It is a real material response, but it means your data is only valid for the shear history you imposed. If your process imposes a different shear history, your model parameters will not transfer. Test under conditions that match your process as closely as possible.
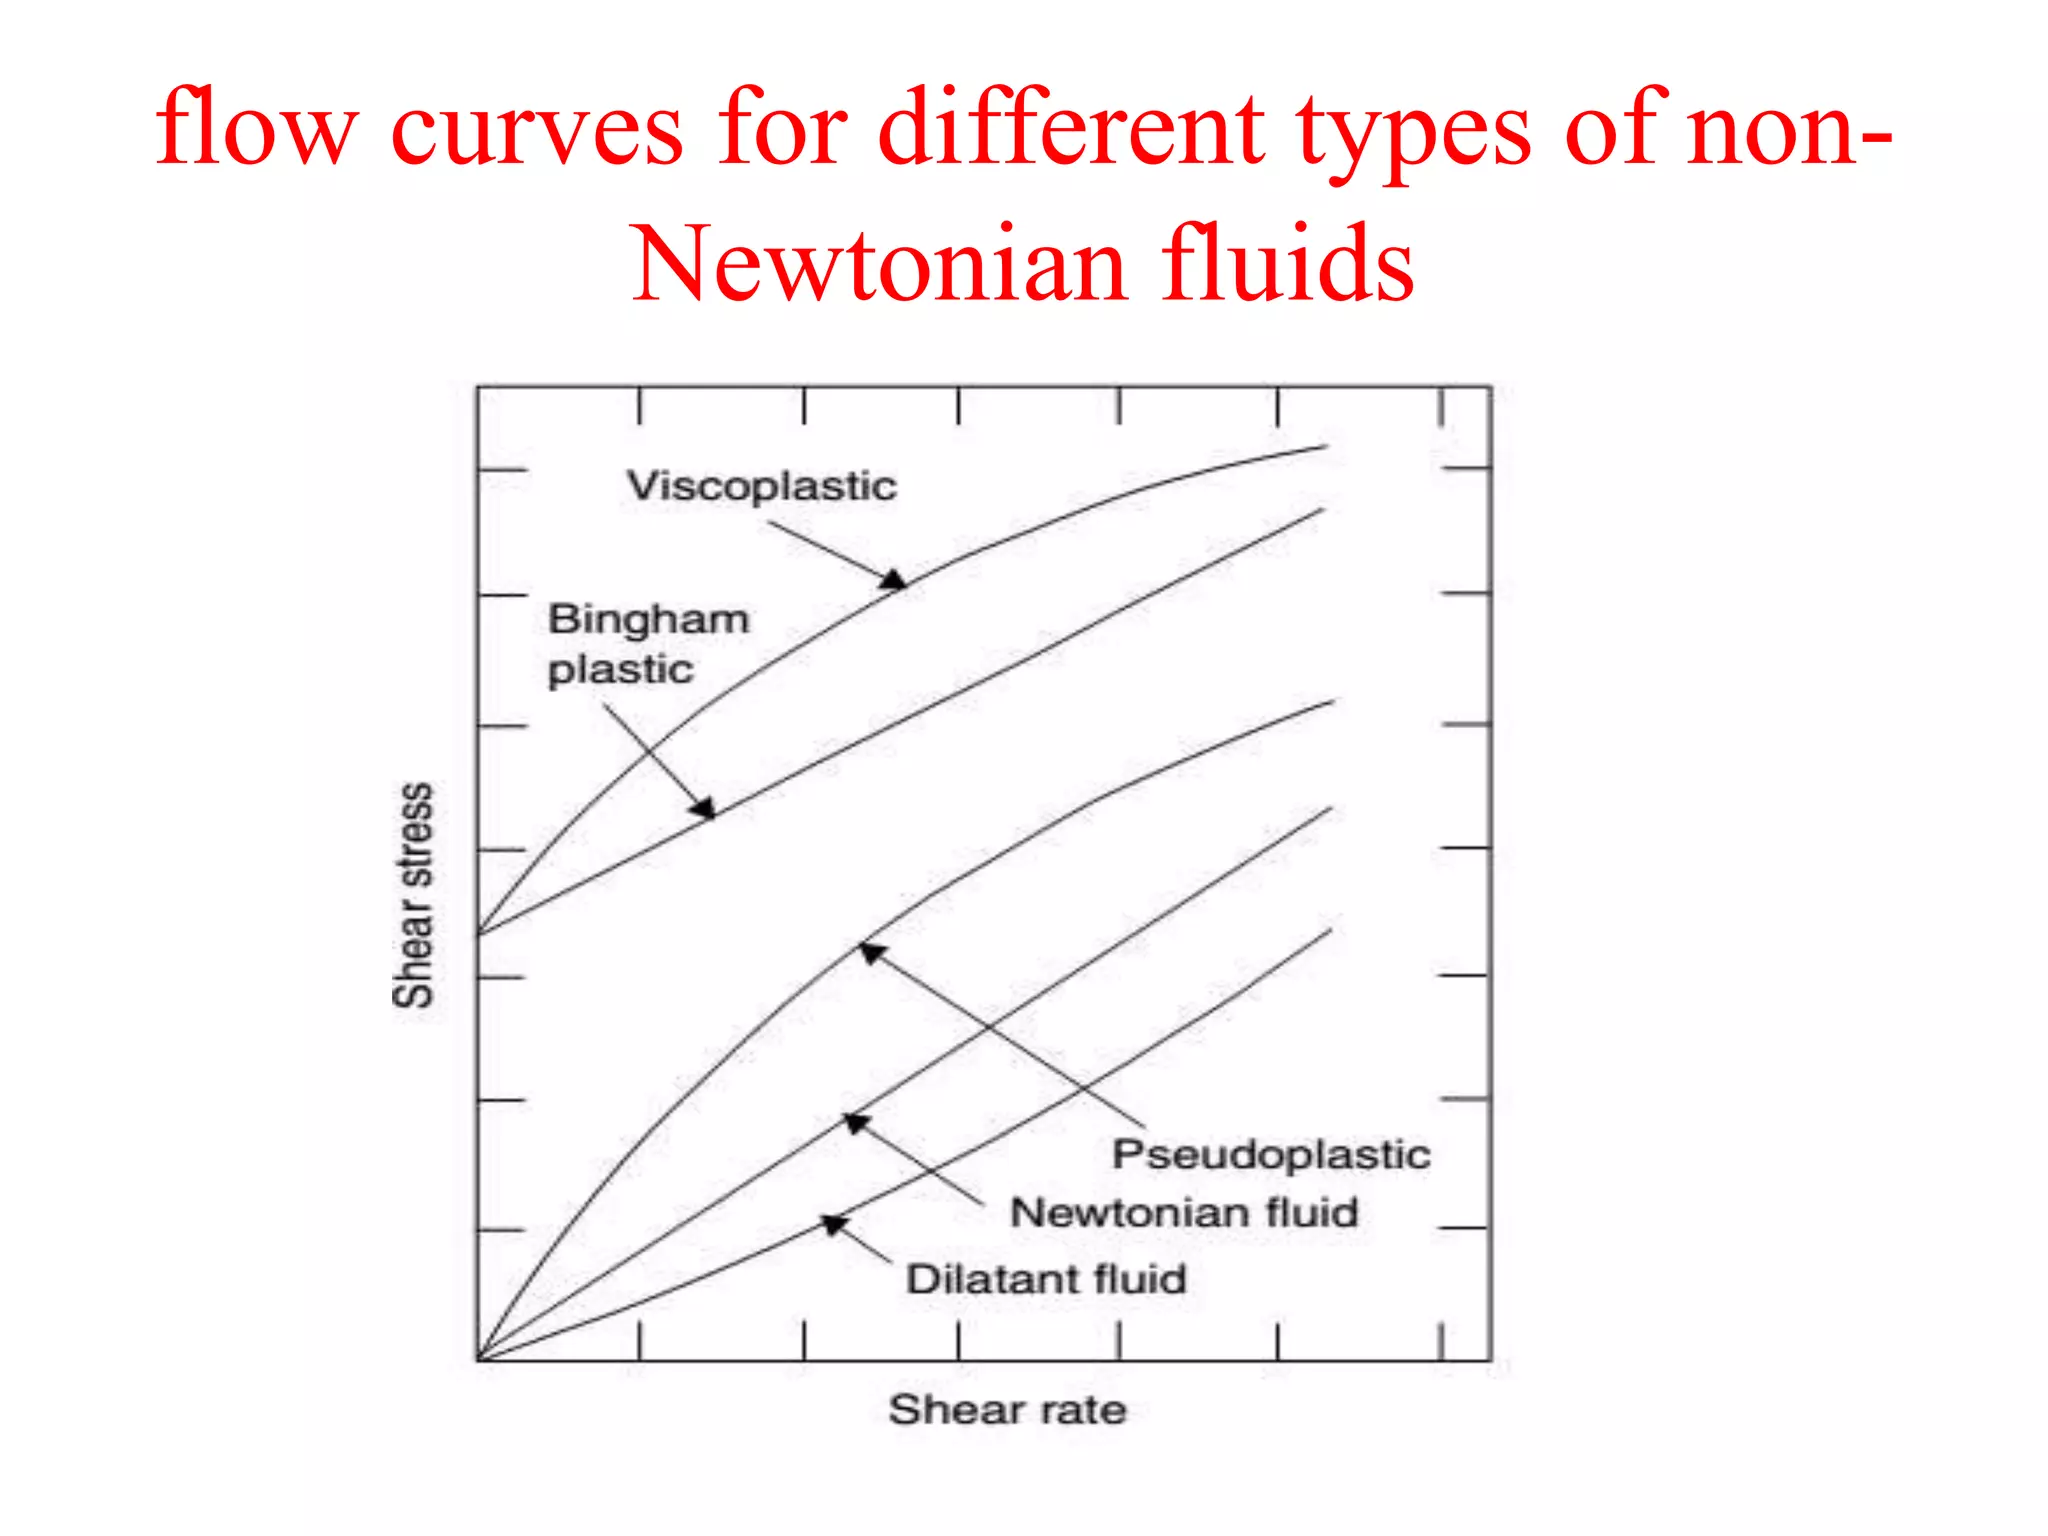
And yes, Bingham plastics are a subset of yield stress fluids, but they are rare in practice. Most real materials that behave like Bingham plastics are actually Herschel Bulkley with a flow index near 1. Calling everything a Bingham plastic makes your calculations simpler and your results less accurate. Use the right model.