Time Studies Explained
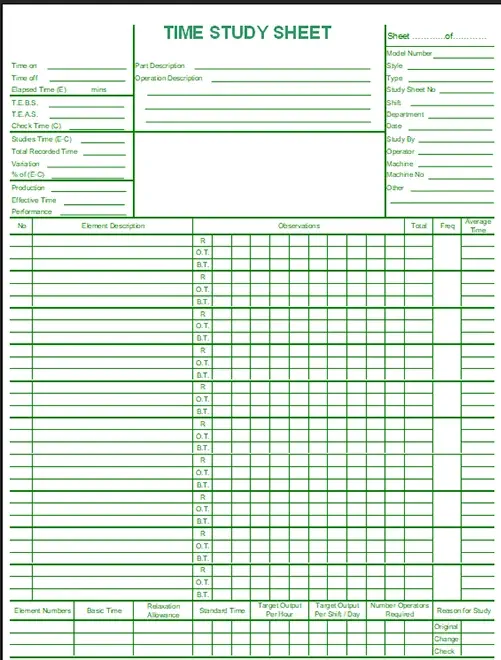
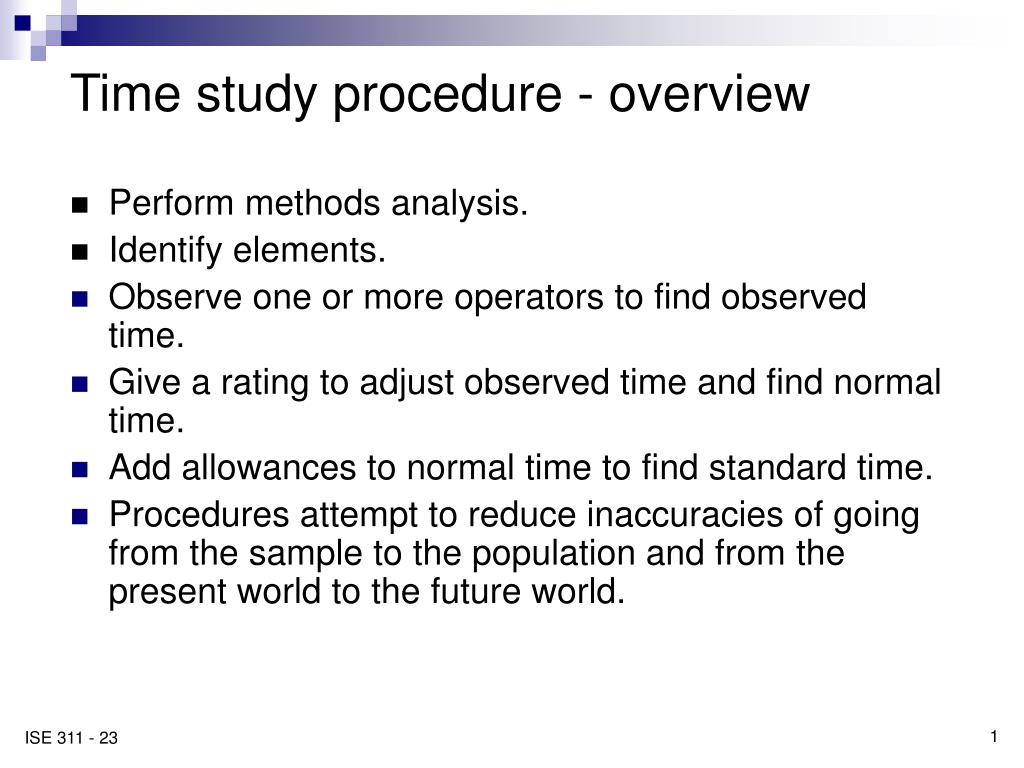
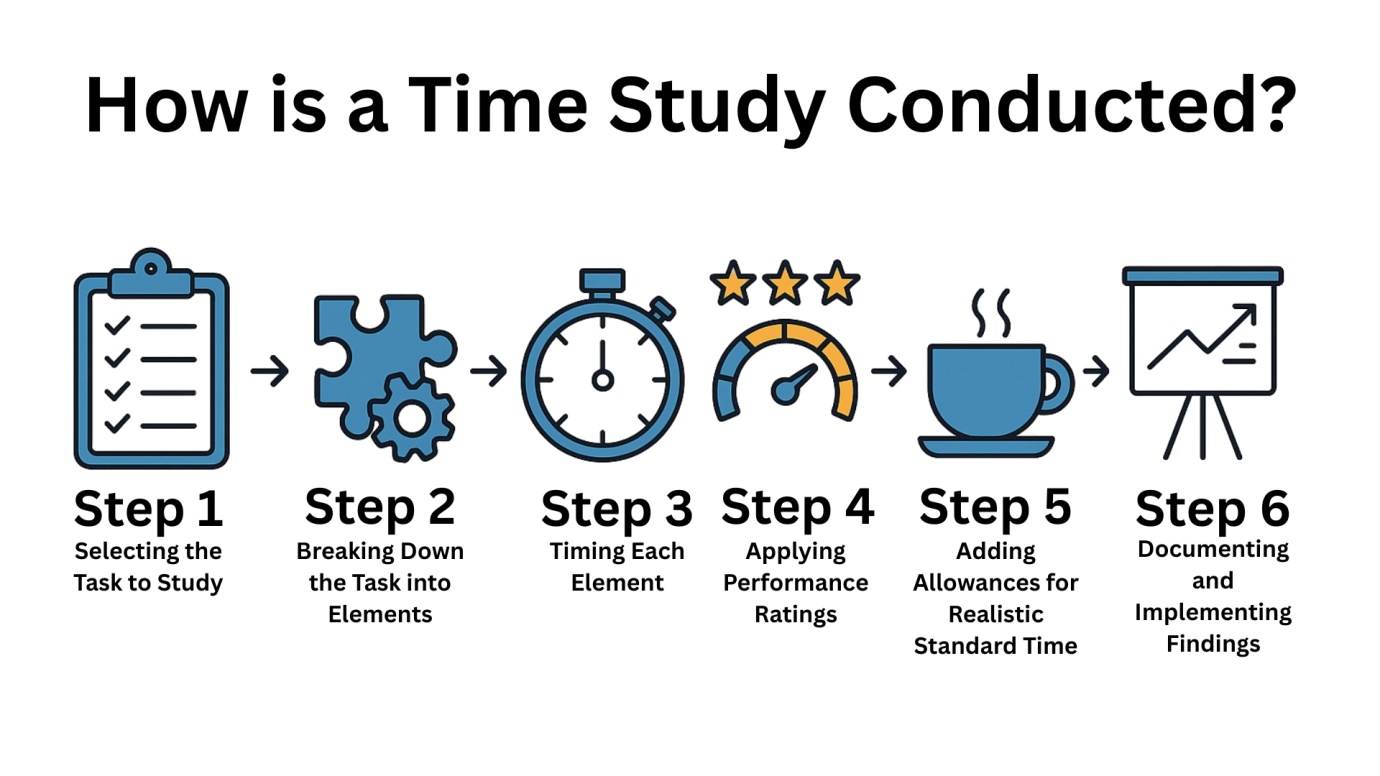
I've spent most of my career watching people struggle with time studies, usually because they treat it like a simple stopwatch exercise. It isn't. A time study is a structured method of observing and recording the time it takes to complete specific tasks or components of a process, then using that data to establish standards, identify bottlenecks, and improve efficiency. The basic premise is straightforward enough, but the execution is where most people mess it up. The method starts with selecting a task or process to observe, breaking it down into discrete elements, and then measuring how long each element takes. You can do this with a stopwatch, a digital timer app, or specialized time and motion software. In practice, I use a split-cycle technique where I record each element's time individually rather than trying to estimate segments after the fact. This reduces error significantly. Here's what actually happens. You observe a worker performing a task repeatedly. You record the time for each distinct element. You take enough samples to account for natural variation. Then you apply a normal rating factor to adjust for the worker's pace relative to a "normal" standard, and you add allowance factors for fatigue, personal needs, and unavoidable delays. The result is what's called the normal time, and when you add allowances you get the standard time.
The formula looks like this: Normal Time = Observed Time × Rating Factor. Standard Time = Normal Time × (1 + Allowance Percentage). That's the textbook version. In practice, the rating factor is where everything falls apart. I've seen analysts sit there and guess at a rating factor of 1.15 or 0.90 without any real basis. That's pure speculation dressed up as science. A proper rating requires a calibrated reference point. I use benchmark tasks that I've timed extensively across multiple operators before applying ratings to new observations. It takes more upfront work but it eliminates the biggest source of error in the entire process. Let me give you a concrete example from a job I worked last year. We were studying an assembly line for a small electronics manufacturer. The task was soldering components onto PCB boards. The claimed cycle time was 4.2 minutes per board. My measurements showed a consistent range from 3.1 to 5.8 minutes depending on the operator and the board complexity. The variance was massive. What we found was that 60% of the variation came from two factors: the time operators spent searching for the right component on a disorganized parts tray, and the rework cycle when a solder joint failed inspection. The actual soldering action took about 1.4 minutes on average. The rest was waiting, searching, and correcting mistakes.
That's the kind of thing time studies reveal when done properly. Most management teams only see the 4.2 minute number and assume the process is fine because it's close to target. The time study exposes the hidden waste. There are several types of time studies you should know about. Work sampling uses random observations to estimate the percentage of time spent on different activities. It's useful for jobs that can't be broken into clean repetitive elements, like maintenance or supervisory work. But it requires a large number of observations to achieve acceptable confidence levels. Cycle time studies measure complete repetitions of a task and work well for manufacturing or transactional processes with clear start and end points. Microtime studies break tasks down into the smallest possible elements, sometimes measured in seconds or fractions of seconds. These are common in high-volume call centers or warehouse picking operations. Predefined time systems like MTM (Methods-Time Measurement) or MOST (Maynard Operation Sequence Technique) don't rely on stopwatch observation at all. They use predetermined motion-time values from a database of standard motions. This is faster and more consistent than stopwatch methods but it requires training and the database has to match your specific industry. MTM-2 is commonly used in automotive and assembly environments. MODAPTS is popular in European manufacturing. These systems let you calculate standard times from process descriptions without ever standing on the floor with a stopwatch.
Get the Full Details

There's a major limitation that nobody talks about enough. Time studies measure what people actually do, not what they should do. If the process is broken, the time study will give you a reliable standard for a broken process. I once did a study for a hospital lab where the standard time for processing a blood sample came out to 23 minutes. When we redesigned the workflow and eliminated three unnecessary transport steps, the new standard dropped to 11 minutes. Same task, half the time, because the original process had accumulated years of redundant steps that the time study faithfully documented. Another pitfall is the Hawthorne effect. Workers change their behavior when they know they're being observed. This is especially pronounced in knowledge work where the act of measurement itself alters the process. I've learned to do a quiet observation period first, sometimes two or three full cycles, before I start recording data. This lets the operator settle back into their normal routine. You'll know when it's working because the measured times stop trending lower across consecutive observations. If they're still dropping, you're not measuring normal performance yet. For sample size, the rule of thumb is that you need enough observations to get within a desired accuracy band with reasonable confidence. A rough calculation: n = (z × s / e)² where z is the z-score for your confidence level (1.96 for 95%), s is the standard deviation of your measurements, and e is your desired error margin as a decimal of the mean. In practice this usually means somewhere between 20 and 60 observations per element for manufacturing tasks. For highly variable processes like customer service calls, you might need 100 or more. I always calculate the sample size before I start collecting data so I know when to stop.
If you want a tool to manage this, there are several options. StopWatch Pro is a desktop application that handles element timing, rating, and allowance calculations. TimeDox is a web-based platform that works well for remote or distributed teams. For mobile work, Seconds Pro on iOS is decent though the Android alternatives are weaker. Free options include Google Sheets with a custom time study template, which is honestly sufficient for most small-scale applications. The software matters less than the discipline of the person using it. One advanced nuance that separates competent analysts from the rest is understanding when NOT to use a time study. Tasks that are highly variable by nature, like creative problem-solving or strategic planning, don't yield useful standard times. The variance will be so large that any standard you produce will be meaningless. For these, work sampling or outcome-based metrics are more appropriate. Similarly, tasks that involve significant interpersonal coordination, like project management or cross-functional meetings, are too context-dependent for traditional stopwatch timing. You'll measure the wrong thing. The biggest mistake I see people make is treating time study results as absolute truth. They're not. They're a snapshot of a specific process, under specific conditions, performed by specific people, at a specific time. Processes change. People change. The standards need to be revisited regularly, ideally whenever there's a significant change in method, equipment, or materials. A standard that's more than two years old without validation is probably already wrong.
In my experience, the organizations that get the most value from time studies aren't the ones using them to set punitive production quotas. They're the ones using the data to redesign workflows, reduce variability, and train new employees against a realistic benchmark. The standard time becomes a reference point for continuous improvement rather than a stick to beat workers with. That shift in mindset makes the entire difference between a useful tool and a dysfunctional one.