Static Charge and Why It Matters in Real Work
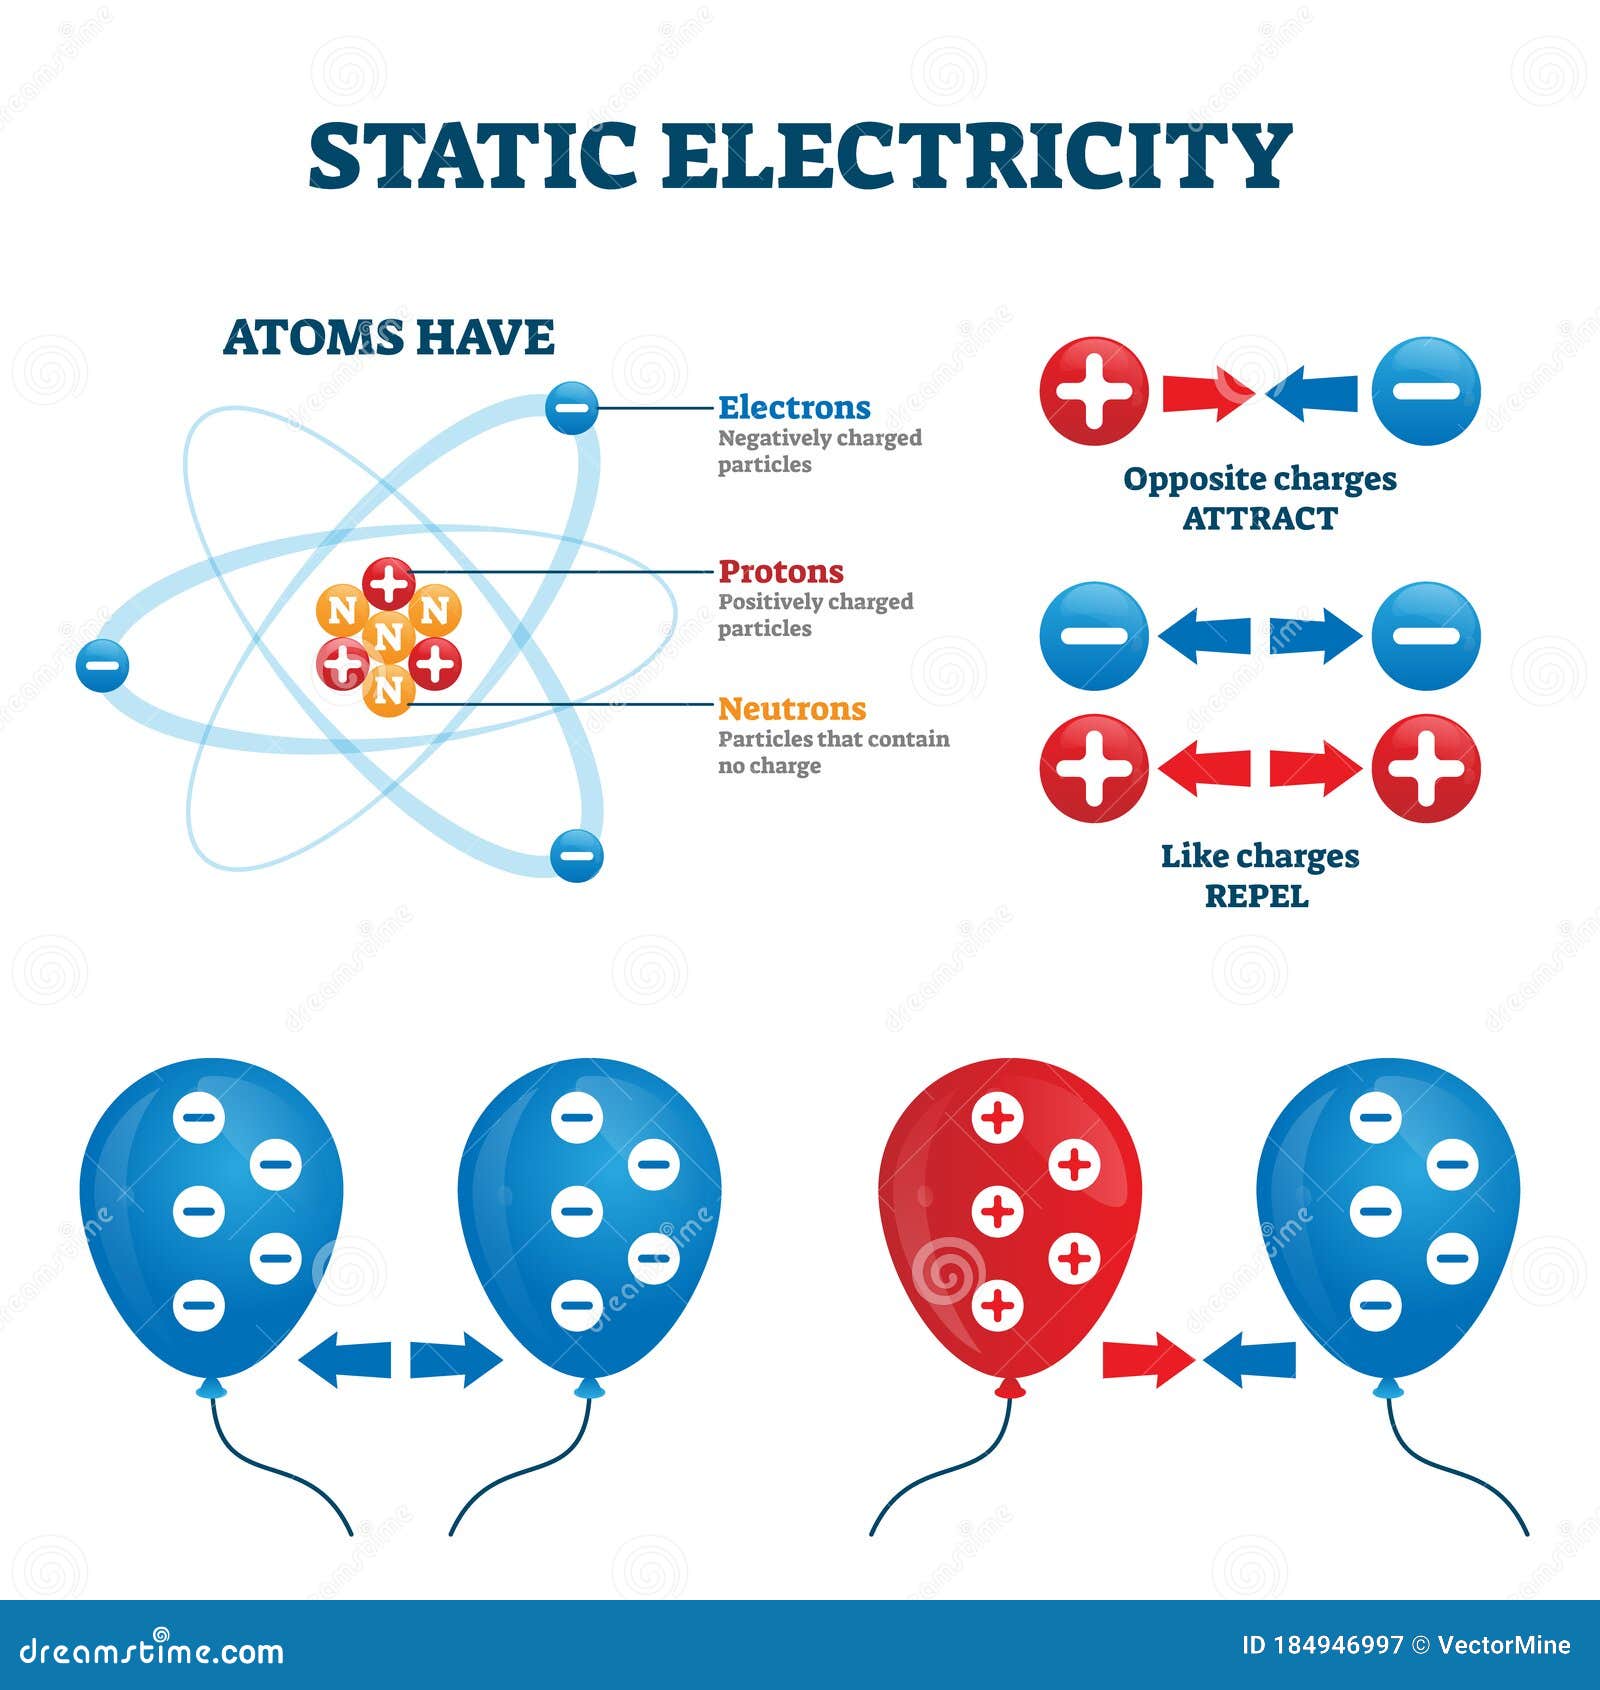
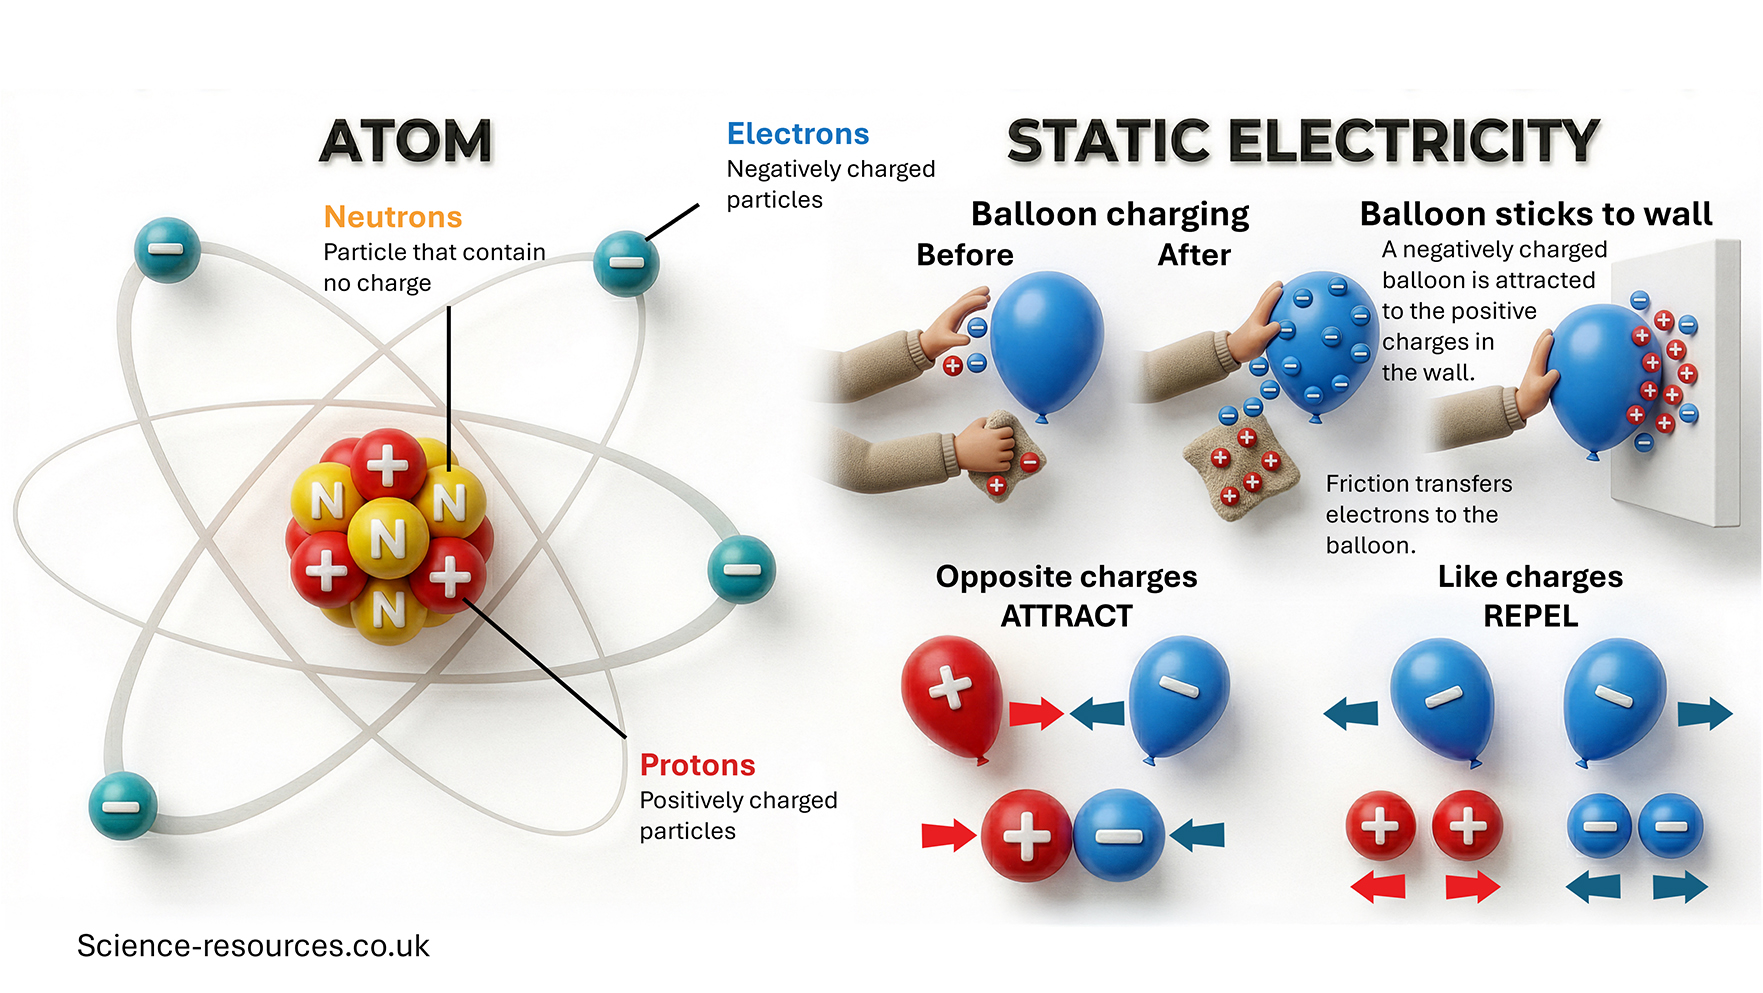
Electrostatic electricity is just charge buildup on a surface where the electrons have nowhere to go. You rub two materials together, one gives up electrons and the other takes them, and suddenly you have a voltage difference sitting there until something discharges it. That's it. In a lab it's a nuisance. On a production floor it can destroy entire batches. At its core, electrostatic electricity refers to stationary electric charges and the forces they produce. The charges aren't flowing through a conductor like in a circuit. They're sitting on an insulator or an isolated conductor, creating an electric field around them. When the field gets strong enough to break down the surrounding medium—usually air—you get a spark, a shock, or in industrial settings, a catastrophic failure of sensitive components. The triboelectric series is the practical starting point. It lists materials in order of their tendency to gain or lose electrons. Rubber and PTFE sit at the negative end and will aggressively grab electrons. Glass and human skin sit toward the positive end. If you're working with anything in between, you need to know where your materials fall on that list before you start assembling or handling components. I learned that the hard way.
Here's a specific situation I ran into about three years ago. We were assembling PCB assemblies in a cleanroom environment, and we kept getting intermittent failures on low-voltage analog circuits. The failure rate was maybe 4 percent, completely random, and it happened only on certain boards. We swapped out components, reflowed solder, checked every solder joint, ran diagnostics for days. Nothing. The boards would pass test, get boxed, and then fail in the customer's equipment two weeks later. The problem was electrostatic discharge happening during assembly. Not a dramatic spark you could see or feel. We were talking about micro-discharges from workers' clothing rubbing against the work surface, charging the PCB substrates to around 800 volts. That's below the threshold where humans feel a shock. Below the threshold where most ESD monitoring equipment flags an alert. But high enough to partially damage the gate oxides on MOSFETs and the input stages of op-amps. The damage wasn't always immediate. It created weakened pathways that failed after thermal cycling in the field. We ended up installing ionizing air bars at every workstation and switching to grounded conductive work surfaces. The failure rate dropped to zero within a week. We also started testing incoming bare boards for hidden ESD damage using curve-tracer analysis on sensitive components before they went into assembly. That last step caught about 6 percent of boards that looked fine on visual inspection but had already been compromised.
How the Physics Actually Plays Out
Charge separation happens through contact and separation. When two surfaces touch, electrons move across the interface depending on their work functions and surface conditions. When you pull them apart, one surface is left with excess electrons and the other is deficit. The voltage that results depends on the capacitance of the charged object. A small object with high charge has a very high voltage. That's why you can get a several thousand volt shock from walking across a carpet and touching a doorknob. Your body capacitance is roughly 100 to 200 picofarads. The energy is low, maybe a few millijoules, but the voltage is what causes the breakdown. For industrial purposes, the relevant metric isn't just voltage. It's the rate of charge generation and the ability of the charge to dissipate. A material might generate 500 volts per cycle of contact separation, but if it's conductive and properly grounded, the charge leaks away before it builds up to a dangerous level. An insulator holds that 500 volts for minutes or hours. That's the real distinction between safe static conditions and hazardous ones. Air humidity changes everything. At relative humidity below 30 percent, most common materials generate significantly higher static charges because the moisture layer on surfaces that normally helps bleed off charge is absent. I've seen static charge levels on polymer packaging materials drop by roughly 80 percent when humidity went from 20 percent to 55 percent. That's not a coincidence. Water molecules adsorbed on surfaces create a thin conductive path that allows charge to dissipate. But relying on humidity control is unreliable in many environments. Climate control systems drift, seasons change, and some processes require low-humidity conditions anyway. Ionization is the more consistent approach.
Get the Full Details
Practical Control Methods
Grounding is the first line of defense and it sounds obvious but it's where most facilities fail. I've walked into manufacturing areas with grounded wrist straps hanging unused on hooks, mats that look connected but aren't actually bonded to ground because the cord was damaged six months ago, and equipment racks that are plugged into grounded outlets but have no actual earth connection because the building wiring was done incorrectly. A continuity check between your work surface, your wrist strap, and the earth ground point takes about ten seconds and costs nothing in equipment. Do it weekly at minimum. I made a habit of checking with a simple multimeter and logging the results. It took me three months to find every single broken ground connection in a facility of about forty workstations. Ionizers are the standard tool for neutralizing charge on insulators. You can't ground a plastic housing. You can't bond it to earth. An ionizer blows a stream of positively and negatively charged ions onto the object, neutralizing the charge. The key specification to watch is the balance of positive to negative ions. A poorly balanced ionizer will neutralize a positive charge and then overshoot and create a negative charge, oscillating back and forth. Good ionizers get within plus or minus 35 volts of neutral and stay there. Cheap ones oscillate between plus and minus 200 volts, which is worse than doing nothing because you're actively charging the workpiece. Material selection matters more than people realize. If you're designing a workflow around ESD control, the first question should be whether you can eliminate the insulating material entirely. Replace a plastic tray with a grounded metal one. Use conductive tote boxes instead of polypropylene bins. Every insulating surface in your workspace is a potential charge reservoir. I've seen entire ESD programs fail because someone switched from one brand of antistatic mat to another that looked identical but had a surface resistance ten times higher. The new mat passed a basic static decay test but didn't dissipate charge fast enough for the process speed they were running at.
Workpiece handling technique is another area where small changes make a measurable difference. Pick parts by the edges, not the centers. Don't slide components across surfaces. Use proper grounding points when moving boards between stations. These feel like minor details until you've spent a week chasing a problem that turns out to be operator technique. I once saw a technician consistently charge a circuit board to over a thousand volts just by sliding it across an ungrounded mat to reposition it under a microscope. The board sat there at that voltage for the entire assembly process. Whatever happened next on that board was operating in a compromised state.
Measurement and Verification
You need to measure what you're dealing with. A simple electrostatic voltmeter or surface potential meter will tell you the voltage on a charged object. A current monitor can measure charge decay rates. For facility audits, I use a combination of a non-contact voltage sensor for quick checks and a grounded electrode method for more precise measurements of charge decay on materials. The key numbers to track are surface potential in volts, charge decay time to reach a safe level, and the ion balance of any neutralization equipment you're using. Safe levels depend on your application. For general electronics assembly, keeping surface potentials below 100 volts is a reasonable target. For high-density memory components, you might need below 25 volts. The milspec standards exist for a reason. ESDS-A64187 and ANSI/ESD S20.20 outline the requirements. They're not suggestions. One thing that catches people out is that static charge on a workpiece doesn't disappear just because you ionized it once. If you leave the workpiece sitting on an insulating surface after neutralization, triboelectric charging from air movement, nearby personnel, or even the settling of the material itself can rebuild charge over time. In a typical office environment with normal air movement, a neutralized plastic component can accumulate measurable charge within five to ten minutes. This is why ionization should be continuous in high-risk areas, not a one-time treatment applied before a task.

Where This Approach Falls Short
ESD control programs have real limitations. Ionizers require maintenance. The needles and emitters accumulate dust and need cleaning on a regular schedule. I've seen ionizers go months without service in busy facilities, becoming less effective over time without anyone noticing. You need to verify ionizer performance monthly at minimum using an ion balance tester. Grounding doesn't solve everything. It only works for conductive or dissipated materials. If your process involves handling molded plastics, glass, or ceramic components, grounding is irrelevant for those items. You need ionization or environmental control for those. Some facilities treat grounding as a complete solution and then wonder why they're still getting ESD failures on boards that include plastic connectors and ceramic capacitors. Human behavior is the biggest variable. All the equipment in the world won't help if workers remove their wrist straps to adjust equipment, walk around the facility with grounded shoes that have worn through the soles, or place boards directly on ungrounded surfaces. Training matters. Audit the training. I've found that the most effective ESD programs are the ones where compliance is checked casually and frequently, not the ones with the longest training documents. A supervisor walking by and asking someone to reattach their wrist strap is more effective than another mandatory training session that nobody remembers.
If you're dealing with extremely sensitive components like GaN devices or advanced CMOS processes, ESD control becomes more of a systematic engineering problem than a set of rules to follow. You need controlled environments, continuous monitoring, statistical process control on ESD-related parameters, and often dedicated cleanroom-level protocols. Standard office or light industrial ESD controls won't be sufficient in those cases. The investment is significant but the cost of failure is higher. The practical takeaway is that electrostatic electricity is manageable but it demands consistent attention to detail. Measure your conditions. Verify your controls actually work. Accept that some materials will always generate charge and plan for neutralization rather than prevention. And don't skip the maintenance.