The Materials That Actually Make Up Industrial and Laboratory Membranes
A lot of people asking about this just read a product sheet and see a laundry list of polymers they've never heard of. The reality is simpler than the marketing copy suggests, but also more finicky in practice. What Is Membrane Made Of depends entirely on which membrane type we're talking about. Reverse osmosis, ultrafiltration, dialysis, and gas separation membranes are all built differently and serve completely different purposes. Getting them mixed up is how you ruin a $4,000 membrane in a week. Reverse osmosis membranes, the kind you'd find in a water treatment plant or a residential reverse osmosis system, are almost always built from a thin-film composite. The active layer is polyamide — specifically cross-linked polyamide — deposited on top of a porous polysulfone support layer, which sits on a polyester nonwoven fabric for mechanical strength. The polyamide skin is where all the action happens. It's only about 100 to 200 nanometers thick. That's roughly one-thousandth the width of a human hair. Everything underneath it is just structural scaffolding keeping that thin layer from collapsing under pressure. Ultrafiltration membranes tend to be made from polysulfone, polyethersulfone, polyvinylidene fluoride, or cellulose acetate. These materials create a sponge-like pore structure rather than a dense selective barrier. The pores range from about 1 to 100 nanometers, which is big enough to let water and dissolved salts pass right through while trapping proteins, colloids, and larger organic molecules. Cellulose acetate has a longer track record in municipal applications because it's more tolerant of chlorine, but polymeric alternatives have largely replaced it in industrial settings due to better chemical resistance and higher flux rates.
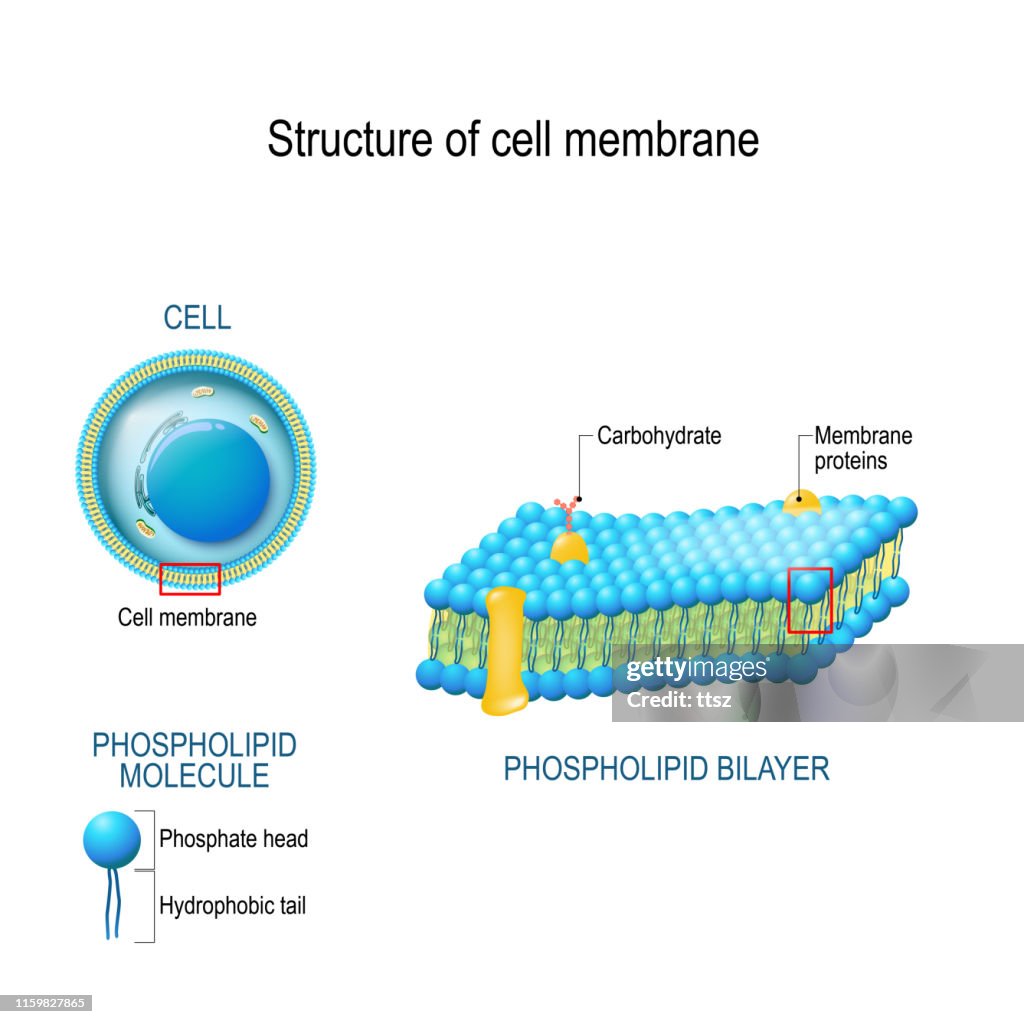
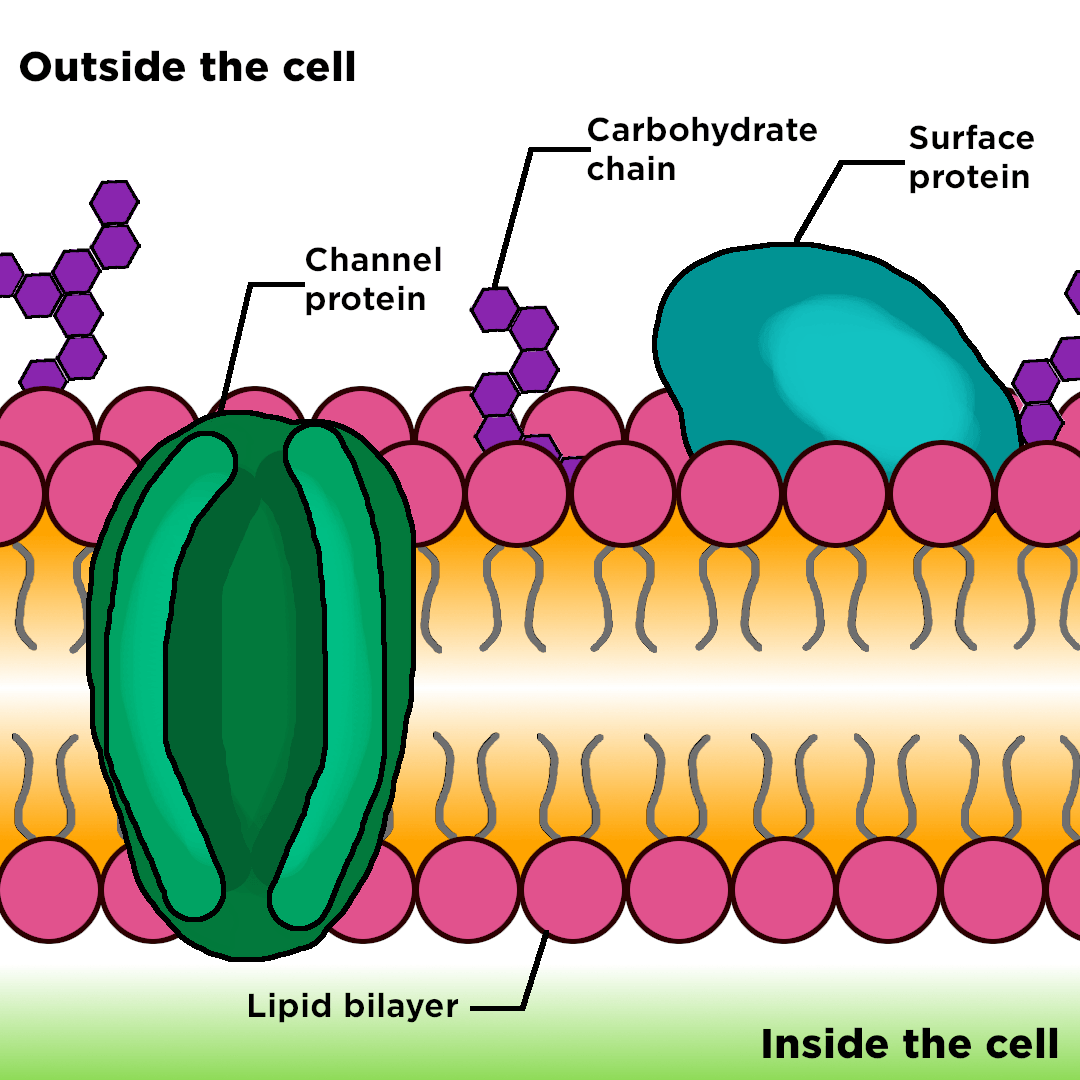
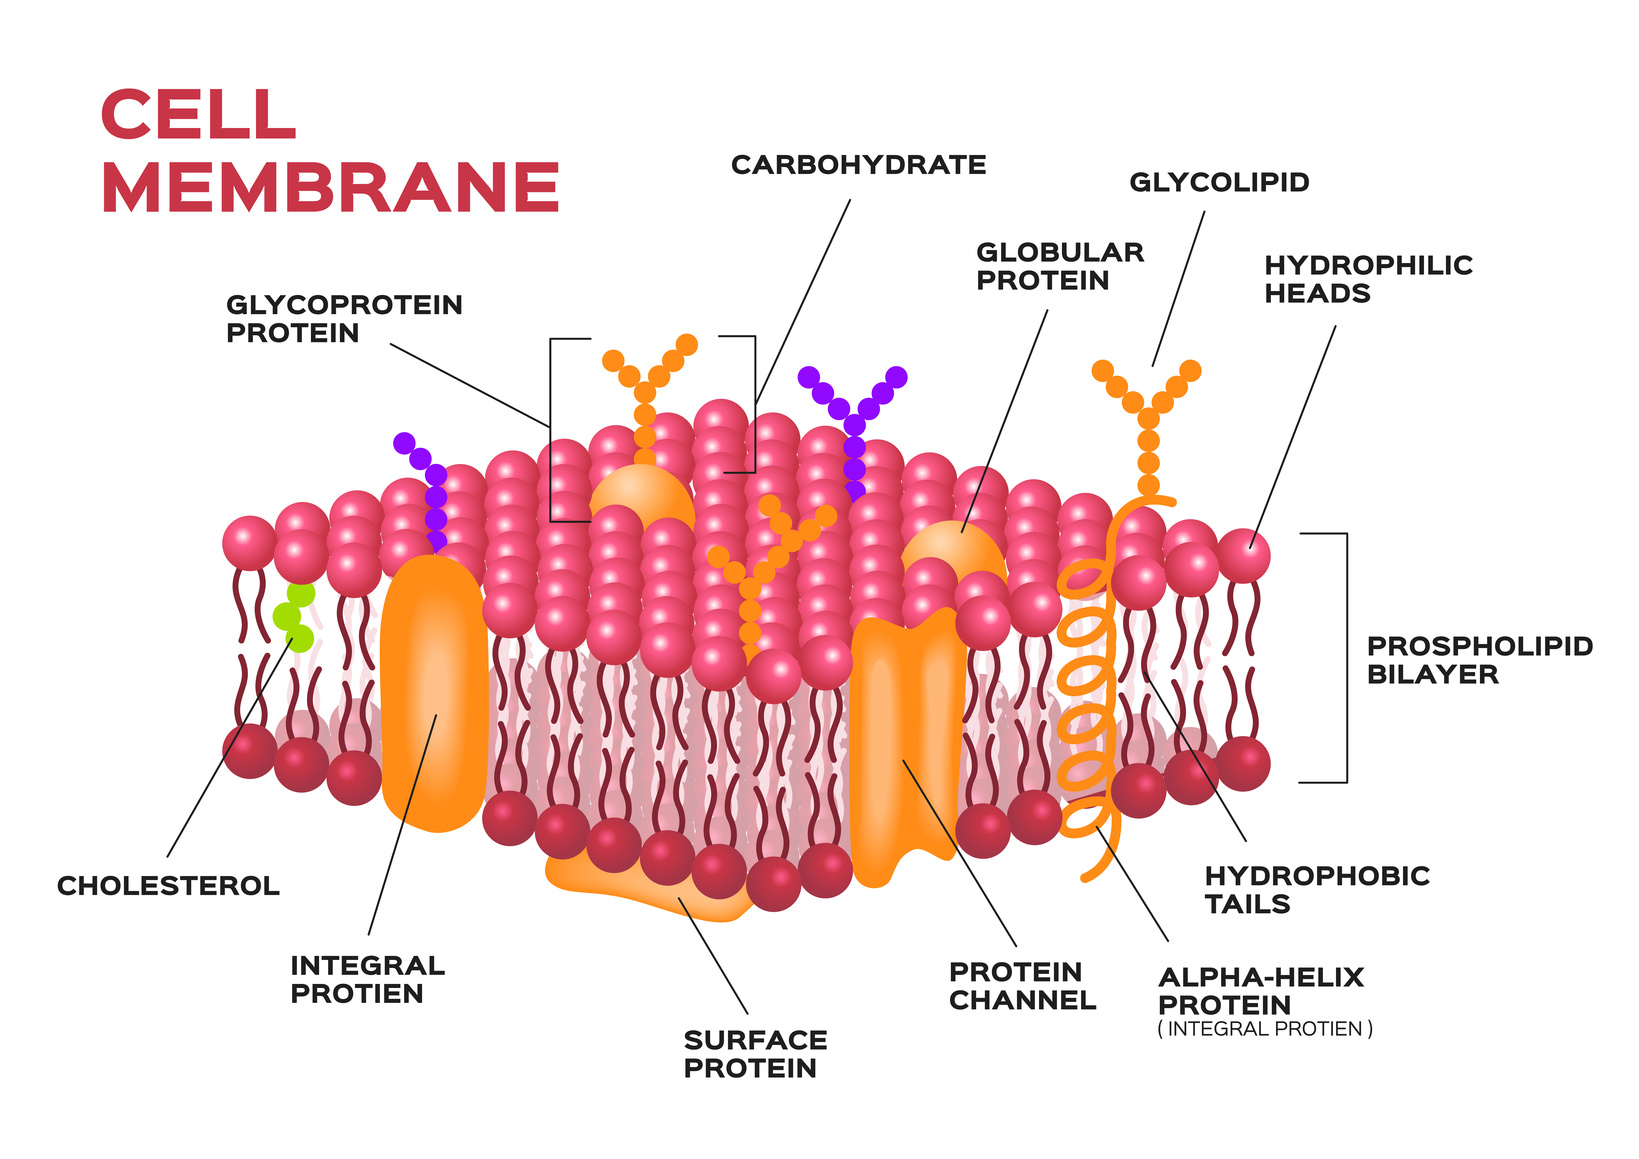
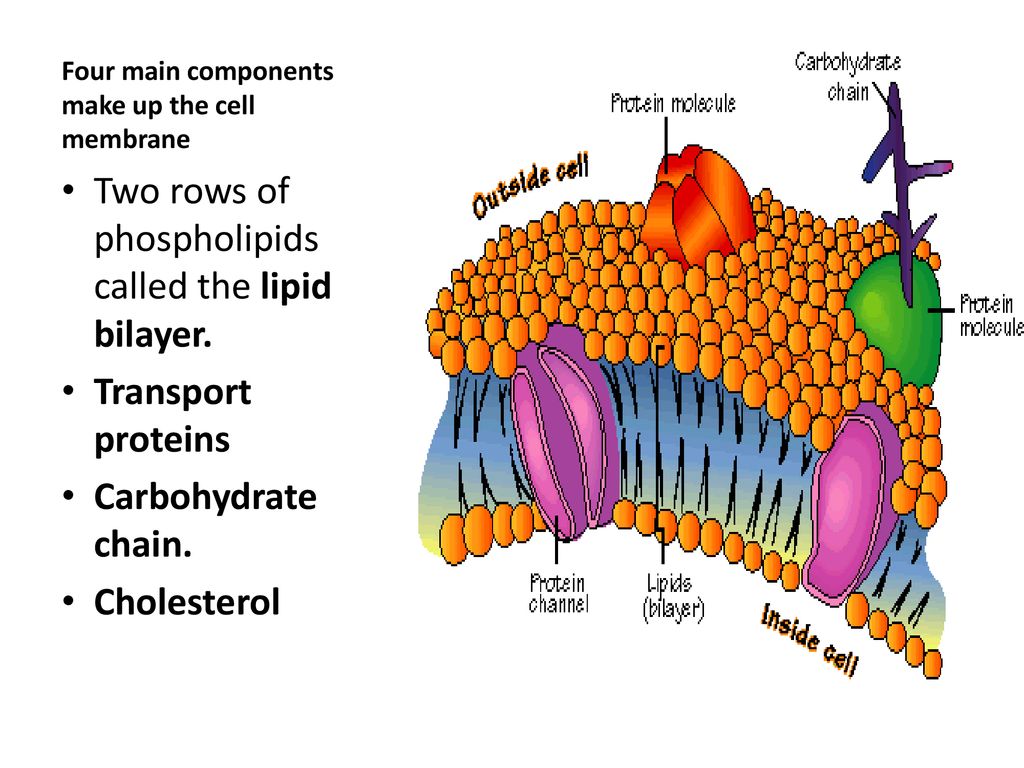
Biological membranes — cell membranes, to be precise — are made from a phospholipid bilayer with embedded proteins, cholesterol, and carbohydrates. That's a completely different scale and mechanism than the synthetic membranes used in filtration. The phospholipids have hydrophilic heads facing outward and hydrophobic tails oriented inward, creating a semi-permeable barrier that controls what enters and exits a cell. Ion channels and transport proteins handle the selective passage. This is osmosis at the cellular level, not pressure-driven filtration. Dialysis membranes for medical use are typically cellulose-based — regenerated cellulose, cellulose acetate, or modified cellulose like cuprophane. Synthetic polymers like polysulfone and polyethersulfone are increasingly common too. The key requirement here is biocompatibility. The membrane can't trigger an immune response or leach toxic compounds into the bloodstream. That's why you won't see standard industrial polysulfone in a hemodialyzer without significant surface modification.
The Polyamide Thin Film — Why It Matters and Where It Fails
The polyamide layer in RO membranes is formed through interfacial polymerization. You expose a polysulfone support to an aqueous solution containing m-phenylenediamine, then introduce an organic phase with trimesoyl chloride. The two solutions meet at the interface and polymerize almost instantly, forming that ultra-thin selective skin. The reaction takes seconds. The resulting membrane has a nodular surface morphology that you can see under SEM, and the cross-linking density determines salt rejection performance. Here's the thing most people don't understand about polyamide membranes: they are extremely sensitive to chlorine. Free chlorine concentrations above 0.1 ppm will oxidize the polyamide layer, breaking the amide bonds and degrading salt rejection. I spent three weeks troubleshooting a desalination unit that was losing 15% of its salt rejection over a two-month period. Turned out the pretreatment chlorination stage hadn't been properly dechlorinated before the water hit the RO membranes. The sodium bisulfite dosing pump had failed six months earlier and nobody had caught it. By the time I pulled the pressure vessels, the membranes were permanently damaged. The polysulfone support layer was still intact, but the active polyamide skin had been stripped away in patches. This is why free chlorine testing before RO entry is non-negotiable in any serious installation. The typical workaround is dual-stage dechlorination with activated carbon filtration backed by bisulfite dosing, with online ORP monitoring to verify complete chlorine removal. Even that isn't foolproof. Carbon filters can develop channeling if the flow rate exceeds design capacity, and bisulfite dosing needs regular calibration because the reagent degrades over time. I've seen facilities skip ORP monitoring entirely and just trust the dosing pump setting. That's a gamble that usually ends badly.
Get the Full Details
Ceramic and Inorganic Membranes — The Nuclear Option
When polyamide and standard polymer membranes can't handle the process conditions — extreme pH, high temperature, aggressive solvents, or severe fouling scenarios — you move to ceramic membranes. These are typically made from alumina, zirconia, titania, or silicon carbide. The separation layer is often a thin ceramic coating on a porous alumina support tube or plate. They can handle pH values from 0 to 14, temperatures up to 150°C or more, and are resistant to cleaning chemicals that would destroy polymer membranes. The trade-off is cost and fragility. A ceramic membrane element costs five to ten times more than a comparable polymeric one. They're also brittle — you can crack them with improper handling or rapid thermal cycling. I worked on a food processing plant that switched from polyether sulfone ultrafiltration to ceramic membranes for a whey protein recovery application. The feed stream had high fat content and required CIP cleaning at 85°C with caustic soda. The polymeric membranes lasted about four months before flux decline became unmanageable. The ceramic membranes have been running for over three years with routine chemical cleaning and no performance degradation. The payback period was roughly eight months given the replacement frequency of the old setup. But the initial capital outlay was substantial and the system required a different cleaning protocol — slower ramp-up and ramp-down rates to avoid thermal shock.
Common Misconceptions That Waste Money
One persistent myth is that higher material thickness equals better performance. In RO membranes, the polyamide layer is intentionally made as thin as possible because water flux is inversely proportional to the selective layer thickness. A thinner layer means higher permeate flow at the same operating pressure. The challenge isn't making it thicker — it's making it uniform. Pinhole defects in the polyamide layer are the number one cause of premature salt passage in otherwise well-maintained systems. Another misconception involves the support layer. People assume the polysulfone substrate does nothing for separation performance, and technically that's correct. But the support layer's pore structure and mechanical properties directly affect the polyamide formation process during manufacturing. An inconsistent support layer produces an inconsistent active layer. This is why membrane manufacturers are extremely protective of their substrate formulations and pore structure specifications. The most expensive mistake I see is using membranes outside their specified pH and temperature ranges and expecting longevity. A standard polyamide RO membrane operated at pH 11 for extended periods will experience irreversible hydrolysis of the polyamide network. The salt rejection drops gradually at first, then collapses rapidly once the degradation becomes severe enough. I've seen operators try to clean heavily fouled membranes with alkaline solutions at pH 12 for "deep cleaning." One extended clean-in-place at that pH can do more damage than months of normal operation with slightly elevated feed pH. The manufacturer's cleaning guidelines specify a maximum pH of 11.5 for short-duration alkaline cleaning, and even that should be limited to a few hours. Going beyond that is experimental at best and destructive at worst.
How to Read a Membrane Specification Sheet Like Someone Who's Actually Used These Things
Beyond the standard specs like nominal pore size, molecular weight cut-off, and material composition, look for the water permeability coefficient, salt rejection rate at specified conditions, and compaction rate. Compaction is the gradual reduction in flux that occurs during the first few hours of operation as the membrane structure consolidates under pressure. A high-quality polyamide RO membrane should stabilize within four to eight hours of continuous operation at design pressure. If flux keeps declining past that point, either the membrane is compacting excessively due to manufacturing issues or the operating pressure is too high for the membrane's design specification. The material compatibility chart in the datasheet is also important. Check not just the feed water chemistry but the cleaning chemicals you plan to use. Some membranes tolerate peracetic acid for biofouling control while others don't. Some accept citric acid for scale removal and others require specific chelating agents. I had a situation where a facility was using a generic citric acid cleaning solution on polyethersulfone ultrafiltration membranes, and the low pH combined with the chelating agents was causing progressive degradation of the membrane surface. Switching to a neutral-pH cleaning protocol extended membrane life from about eleven months to over twenty-two months with equivalent flux recovery. The bottom line is that membrane composition determines everything about how the membrane performs, what it can handle, and how long it will last. Picking the right material for your application and respecting the operational limits is the difference between getting three years of service out of a membrane and replacing it in three months. The chemistry is straightforward. The execution is where most people make mistakes.