Getting Your Head Around These Four Processes
These four terms come up together a lot because they all deal with shaping metal without heating it up. That distinction matters more than people think. Hot working changes the grain structure entirely. Cold working refines it, increases strength through strain hardening, but also introduces residual stress you need to manage. I learned that the hard way on a batch of 304 stainless tension rods back in 2018. We pushed the draw reduction too aggressive in a single pass and got micro-cracking at the surface. Took us three days to figure out what happened. The processes overlap more than textbooks suggest. Wire drawing feeds into cold forming when you need consistent feed stock. Rolling produces the sheet that then goes into forming operations. Understanding where one ends and another begins helps you plan tooling and material flow correctly.
Wire Drawing Cold Forming Sheet Metal Forming Rolling
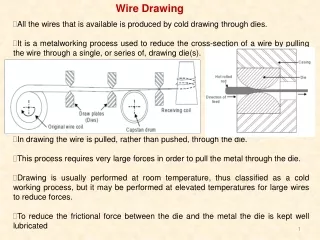
Here is how each one actually works in practice, and where the real problems show up. Wire drawing pulls metal through a die to reduce diameter. Simple in concept. The die is typically tungsten carbide or diamond for finer gauges. You lubricate heavily—usually a phosphate and soap coating on steel wire, or an oil-based compound for aluminum. The reduction per pass matters a lot. Rule of thumb for most steels is somewhere between 15 and 35 percent area reduction per pass. Go beyond that and you risk die failure or workpiece fracture. Aluminum can handle slightly more reduction per pass but galls easily if your lubrication is insufficient. The draw bench speed varies by material and gauge. Steel wire under two millimeters might run at sixty to ninety meters per minute on a modern multi-wire line. Larger diameters on a single-die bench crawl along at twenty to thirty meters per minute. Tension between stands is critical. Too much tension and you elongate or neck the wire. Too little and you get coil formation inside the die, which ruins the surface finish and can snap the wire.
Strain hardening is the main consequence you deal with. Every pass increases tensile strength while reducing ductility. If you need to draw a wire down from eight millimeters to two millimeters, you cannot do it in one pass on most equipment. You need intermediate anneals. A typical 304 stainless wire going from eight millimeters to two millimeters might need three to four draws with anneals between passes two and three, and again before the final pass. The anneal temperature for 304 is roughly 1040 Celsius, held long enough to restore full ductility, then quenched or air-cooled depending on the grade and required properties. I had a problem once where the final diameter was coming out consistent but the ovality was terrible. Turned out the die entry angle was worn unevenly on one side. We were pulling six millimeter brass wire and the die had seen about 40,000 meters of run time. Replacing the die brought ovality back under two percent. Checking die wear regularly saves a lot of scrap. A dial indicator at the exit check station catches diameter drift before it becomes a batch rejection.
Get the Full Details
Cold Forming
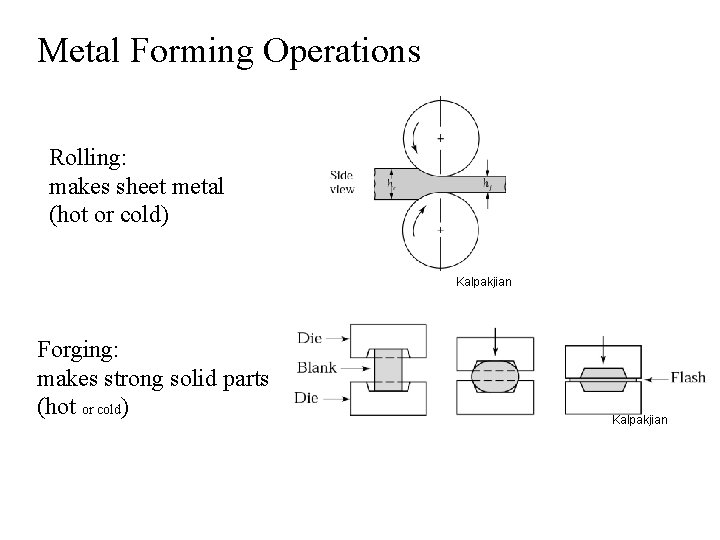
Cold forming covers a wide range of operations. Heading, extrusion, bending, roll forming—all of it falls under this umbrella. The common thread is deforming metal at or near room temperature to achieve a shape closer to final dimensions than casting or machining would provide. Fastener production is the classic application. Cold heading machines can produce thousands of bolts per hour from coiled wire feed. The material flows into a die cavity under high pressure. Multi-impact headers do successive blows to fill the die. The material must have adequate ductility, which is why soft tempers or annealed stock are standard inputs. Work hardening happens during the form, which is usually desirable for the finished fastener. The bigger challenge with cold forming is springback. Not in the same way as bending, but the elastic recovery after the load is released can change dimensions slightly. For precision components, you factor this into the die design. A typical allowance is anywhere from five to fifteen micrometers depending on the material and geometry. For high-volume runs, the die gets made to compensate. For prototype work, you end up tweaking with trial parts and measuring.
Lubrication in cold forming is not optional. Zinc stearate, phosphate coatings, or specialized synthetic compounds reduce friction and prevent galling. Without it, you damage the die surface quickly and part quality degrades. I once ran a batch of aluminum housing components without sufficient lubricant and took out a $12,000 die in under four hours. The aluminum welded itself to the die steel. That was a costly lesson in not skipping the prep steps. For complex geometries, incremental forming—multiple stations or operations—gives better results than trying to form everything in one stroke. The trade-off is cycle time. A single-hit process is faster but limited in complexity. A multi-station transfer line produces better detail but costs significantly more in tooling and setup time.
Sheet Metal Forming
This is pressing, stamping, bending, and deep drawing of sheet stock. The press tonnage you need depends on the material, thickness, and geometry. A rough calculation for blanking or punching is shear strength times perimeter times thickness. For forming operations, it is more complex because you are dealing with bending moments and material flow, not just shearing. Material choice drives everything. Mild steel forms easily with standard tool steel dies. Stainless requires more tonnage and more careful surface management. Aluminum is forgiving on tonnage but springs back more and galls on steel tooling. You often coat aluminum tooling or use nitrided dies to extend life. Engineering plastics like UHMW can work as counterfaces for aluminum forming when you are doing low-volume runs. Deep drawing is where sheet metal forming gets interesting. You are pulling flat blank material into a die cavity with a punch. The material at the flange undergoes compressive hoop stress while the wall undergoes tensile stress. If the ratio of blank diameter to punch diameter is too large, the flange wrinkles. If the wall stress exceeds the material strength, it tears. The limiting drawing ratio for most steels is around 2.0 to 2.2 for a first draw. Anything beyond that requires intermediate anneals or multiple draws with decreasing die openings.
Bend allowance calculations matter more than people give them credit for. The K-factor, which represents the neutral axis shift during bending, is not a fixed constant. It varies with material, bend radius, and sheet thickness. For mild steel with a bend radius equal to the sheet thickness, a K-factor around 0.4 to 0.5 is typical. For harder materials or tighter radii, it shifts. Using a generic table value will get you within a millimeter or two on simple parts. For precision assemblies with multiple bent features accumulating tolerance, you need to measure and calibrate for your specific material lot. I spent a week chasing a tolerance issue on a stamped enclosure. The bend lines kept drifting by about 0.8 millimeters between first article and production runs. The problem was inconsistent blanking lubricant buildup on the die. Every other shift, the operator cleaned the die surfaces, and the parts came back to spec. Standardizing a cleaning schedule and using a thinner film lubricant solved it. The moral is basic shop discipline often matters more than fancy tooling design.
Rolling
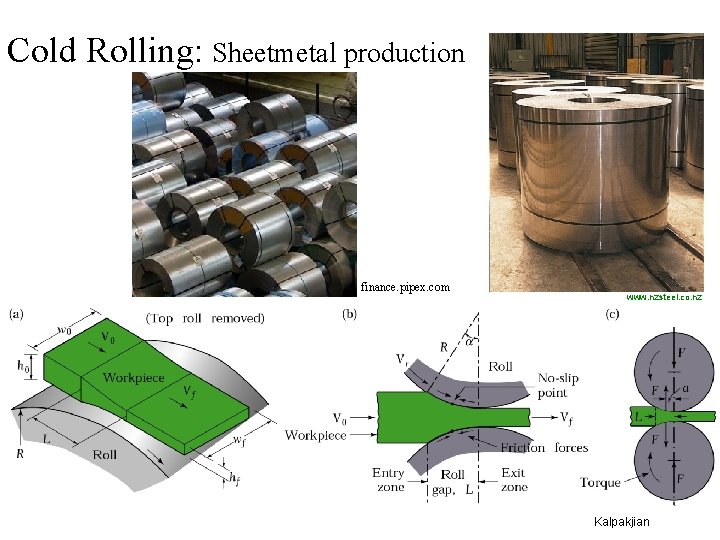
Metal rolling reduces thickness or shapes cross-sections by passing material between rotating rolls. Sheet and plate rolling uses flat rolls. Shape rolling uses contour rolls for beams, channels, and rails. Wire rod mills use a series of stand reductions to go from ingot to final diameter. Hot rolling breaks up the as-cast structure and refines the grain. The material enters the rolls at elevated temperature, typically above the recrystallization point, so strain hardening does not accumulate. This means you can take large reductions in a single pass. A steel slab might go from 200 millimeters thick down to 20 millimeters in a multi-stand hot strip mill in a continuous pass. Cold rolling follows hot rolling to achieve tighter tolerances and better surface finish. The reductions per pass are smaller, maybe five to fifteen percent per stand in a tandem mill. The work hardening from cold rolling is significant. Cold rolled sheet might go from yield strength of 200 MPa in the annealed state to over 400 MPa after two passes with intermediate reductions. That strength increase is why cold rolled stock is specified for precision applications where form stability matters.
Flatness control in rolling is a constant battle. Crown—the tendency for the roll to deflect in the center under load—creates thickness variation across the width. Work roll bending, roll shifting, and hydraulic crown control systems mitigate this on modern mills. For a small shop with a two-high cold mill, you manage crown by selecting the right roll diameter and monitoring gauge with X-ray or beta gauges. If you are producing thin gauge material under half a millimeter, even minor roll deflection shows up immediately in the product. Shape rolling for structural sections requires a series of stand passes, each one progressively forming the final cross-section. The first few passes break down the bloom or billet into a rough shape. Intermediate passes refine it. The finishing stands bring it to final dimensions with tight tolerances. Roll design for shape rolling is specialized work. Each groove needs to account for spread, elongation, and the natural flow of the metal. Get the pass schedule wrong and you end up with edge cracks, incomplete fills, or excessive roll wear. A limitation worth noting upfront: cold working has a hard ceiling on how much reduction you can achieve before the material becomes too brittle to continue. Some high-strength alloys can only be cold worked a small percentage before requiring annealing. Titanium alloys are particularly restrictive. You cannot run them through the same reduction schedules as mild steel. Push too hard and you get cracking or even catastrophic die failure from workpiece fracture.

Another practical limitation: residual stress from cold working can cause parts to distort over time or during subsequent machining. Stress relieving at moderate temperatures—around 590 to 650 Celsius for most steels, held for about one hour per inch of thickness—reduces this risk. If you are making precision machined components from cold-worked stock, skipping the stress relief is a common source of later headaches.
How These Processes Connect in Practice
A typical production flow might start with a wire rod that goes through descaling and drawing to the required diameter. That drawn wire feeds a cold heading machine to produce fastener blanks. Or the rod goes through a rolling mill to produce sheet, which then enters a press line for stamping and bending operations. The same material might pass through multiple processes depending on the final part geometry. Planning the sequence matters for cost and quality. Annealing between operations adds time and equipment cost but is often necessary. Surface preparation between draws or forms affects tool life significantly. A clean, properly coated surface extends die life by factors of two or three compared to running raw stock through the same tooling. Quality control across these processes relies on dimensional measurement, surface inspection, and mechanical testing. Tensile tests verify that strain hardening is within spec. Bend tests check ductility after cold working. Hardness testing gives a quick indication of the work hardening state. For production environments, in-line gauging at key points catches drift before it becomes scrap.
The main pitfalls I see people encounter are underestimating the strain hardening effect, skipping adequate lubrication, and not accounting for springback in forming operations. All three are fixable with proper process planning and documentation. The stuff that causes real losses is die wear management and material consistency. Always verify your incoming stock properties and track die life per batch. The data you collect early saves you from surprises later.


