Production floor paperwork nobody wants to read, but everyone needs
The thing about work instructions for production that trips people up isn't the writing itself. It's the gap between what you type on paper and what actually happens when a machine breaks at 2:47 AM and three new operators are standing around watching a supervisor try to remember the torque sequence by heart. I spent seven years in automotive assembly before moving into process documentation, and the hardest part was never explaining a step clearly. It was figuring out which steps operators already knew so well they'd never mention them out loud. When I worked on the line at Ford's plant in Oakville, we had work instructions that were technically perfect and practically useless. The engineering team wrote them like procedure manuals for astronauts. Real operators needed something different. They needed the version that accounted for the fact that the right-hand tool cart only had two sockets instead of three, and the floor mat in Bay 4 always got greasy if it rained.
Work Instruction For Production: What Actually Gets Used
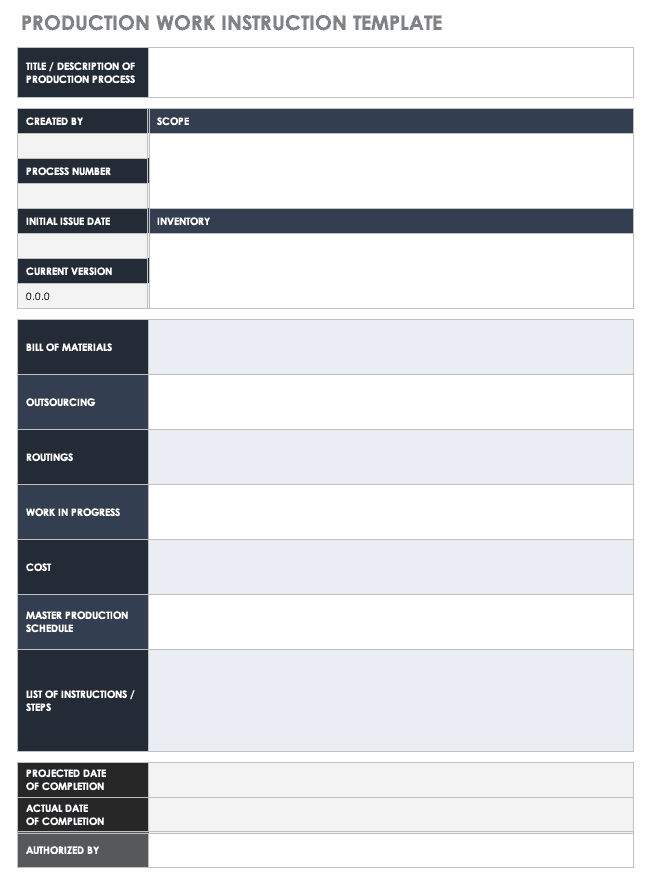
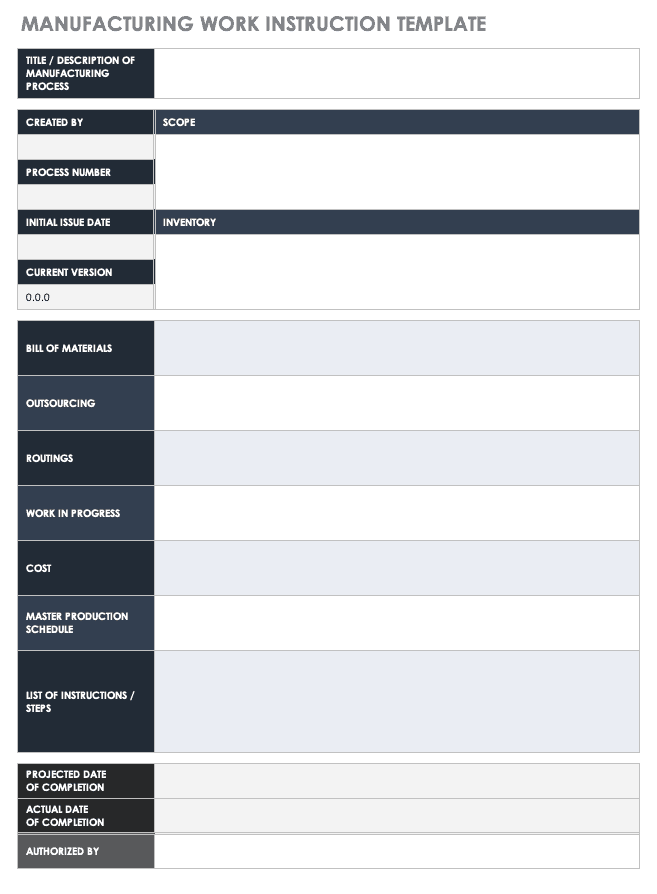
A work instruction for production isn't a legal document. It's a communication tool between the person who designed the process and the person who's trying to execute it while standing on concrete for eight hours. The difference matters because one audience reads it once and files it. The other reads it forty-seven times over six months until the words disappear and muscle memory takes over. Your instruction has to survive both uses. The structural elements are standard. You need a header with part number, revision level, effective date, and safety warnings that actually matter. You need numbered steps in imperative mood. You need diagrams where words fail. But the content that makes or breaks these documents comes down to one question: what happens when the operator encounters the exception case that wasn't in the original design spec? I learned this the hard way during a recall investigation. A supplier had changed a washer material without updating the work instruction. The instruction said to torque to 12 Nm. It didn't say what to do if the bolt backed out past the thread engagement mark because the new composite washer compressed differently. Thirty thousand vehicles rolled off the line with under-engineered connections. The fix took six weeks and cost the plant about $2 million in rework. That's the kind of gap that lives in these documents whether you intend it to or not.
How to write these things without wasting everyone's time
Start with the actual process, not the idealized version from the engineering drawing. Go to the gemba. Watch an experienced operator run the cycle at least three times before you write a single word. Pay attention to what they don't say out loud. The hand positioning, the way they check the gauge without looking, the sigh they make when they hit that one stubborn fastener. Those are the details that separate an instruction manual from an actual work instruction for production. Use active voice. Keep sentences under twenty words when possible. One action per step. If a step contains two verbs, split it. The operators reading this at the end of a shift don't have patience for grammatical gymnastics. They need to know whether to pull or push, tighten or loosen, and what color indicator means stop versus proceed. Include the tools and materials section at the top. Not buried in the body text. Not as an appendix. Right after the safety warnings. An operator at 6 AM needs to verify they have the right socket size before they start, not mid-cycle when they discover they've been using the wrong one for twenty parts.
Get the Full Details

Photographs beat diagrams every time. A diagram shows a bolt in isolation. A photograph shows the bolt in context, next to the housing, with the lighting and glare that actually exists on the shop floor. I started using iPhone photos on my phone rather than CAD renderings, and the acceptance rate from floor supervisors jumped from 40 percent to 85 percent. The photos don't need to be pretty. They need to be accurate. Lighting inconsistencies, slight blur, the occasional finger in the frame. That's real. That's what operators recognize.
The version control problem nobody talks about
This is where most documentation programs fail. You write a clean work instruction for production. Six months later, engineering changes a material spec. The machine gets modified. The process drifts. Your document is now wrong, but the revision log says otherwise because someone updated the date field without verifying the content. I've seen revision histories where three different versions claimed to be the latest, and the only way to know was to open each one and compare. The workaround is brutal but simple. Every change request must include the old document and the new document side by side. Not a summary. Not a bullet list of modifications. The actual pages. Someone has to read both and confirm the difference is what they expected. This adds about four minutes to each change request, but it eliminates the class action lawsuit scenario where a plant runs a process for six months based on outdated torque values. Also remove the revision history table. Nobody reads it. Put the change description inline with the step it affects. If you changed the torque spec in step 14, annotate step 14 directly. Don't hide that information in a footer that describes what happened three versions ago. Operators don't care about version 2.3. They care about whether the value in front of them is correct right now.
When these documents fail completely
Here's what nobody wants to admit. Work instructions for production don't solve training problems. They don't replace supervision. They don't prevent mistakes when the operator is rushed, distracted, or working a process they haven't performed in three weeks. A document is a reference tool, not a guarantee. The people who treat it as a silver bullet end up with binders full of perfectly written instructions sitting unused on shelves while operators develop their own shorthand methods. The bottleneck usually appears during peak production. When you're hitting quota and the shift supervisor is yelling about throughput, nobody reads the work instruction. They've memorized the critical steps or they're winging it based on what they did yesterday. The document only matters during the quiet moments, and those are exactly when people don't feel like reading. If your plant runs 24/7 with high turnover, consider pairing work instructions with visual management systems. Shadow boards for tools. Color-coded safety zones. Andon lights that force a stop when something deviates. The work instruction becomes the detailed reference for the lead operator rather than the primary communication channel for every person on the line. This isn't a failure of the document. It's an acknowledgment that one tool can't solve all the problems.
I switched some of our work instructions to video format last year. Not as replacements. As supplements. A thirty-second clip showing the correct hand position and motion flow, posted at the workstation on a loop. The operators who watched the videos made fewer errors in the first two weeks than the group that only read the printed instructions. The ones who didn't watch the videos performed identically to the control group. The video doesn't help everyone. It helps the people who need to see it. There's also the language barrier problem. If your floor has operators who read at a ninth-grade level or operate in a second language, your work instruction is effectively invisible to them regardless of how well you write it. The solution isn't better writing. It's reducing the reading load entirely. More pictures. Fewer words. Universal symbols where they exist. And for the critical steps, a verified translation by someone who actually speaks the language, not a translation app that turned "torque to specification" into "turn until it feels right" in our first attempt.
What to measure instead of how many you write
The standard metric is document count. How many work instructions for production exist in the system. This is the wrong metric. It measures activity, not effectiveness. A better metric is the first-time-right rate on the operations that have documented instructions versus the ones that don't. Or the cycle time variance for steps that include visual aids versus text-only steps. Or the number of deviations reported within the first thirty days of a process change, tracked against whether the updated instruction was actually distributed and acknowledged. I stopped reporting document count to senior management and started reporting the error rate delta. Within six months, the budget for documentation improvements doubled. Not because writing better instructions became more important. Because the numbers showed it mattered.