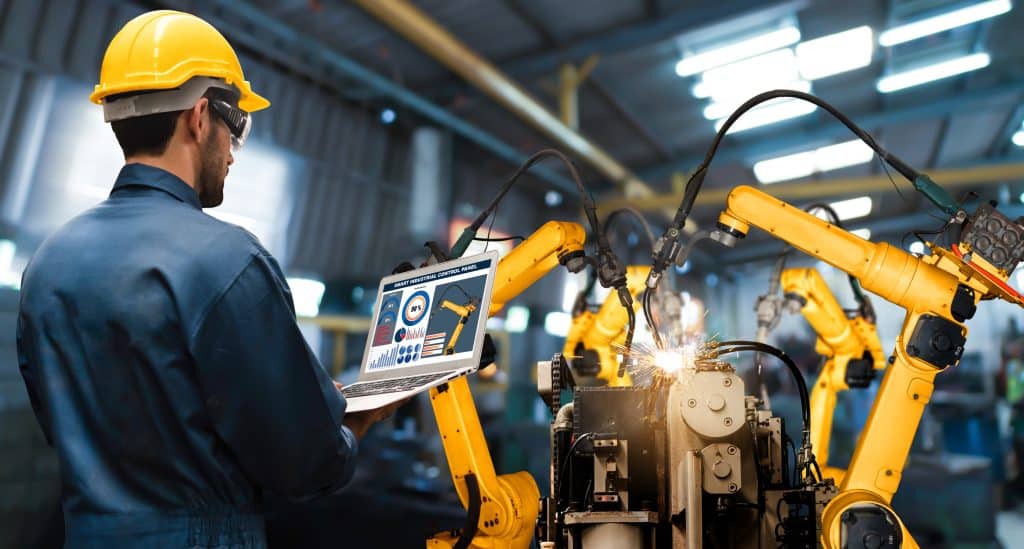
What actually moves the needle on the shop floor
Most people think advanced manufacturing is all robots and shiny displays. The reality is messier. You get machines that either run like clockwork or eat your tooling budget in a week. The difference usually comes down to how the technology is integrated, not the technology itself. I spent three years working with additive and hybrid systems on the production side before moving into process engineering. What I learned is that the technology most plants adopt successfully is the one they treat as a regular tool, not a miracle worker. Digital twins, robotic welding cells, CNC turning centers with live tooling, laser cladding, and in-line metrology are all part of what falls under Advanced Manufacturing Technology Examples, but some of them earn their keep faster than others.
Advanced Manufacturing Technology Examples that actually pay off
Let me walk through the ones I've seen work and the ones that became expensive paperweights. Hybrid additive-subtractive machining combines metal 3D printing with CNC milling in a single setup. You build up near-net-shape geometry, then machine the critical surfaces. A typical use case is restoring or modifying turbine blades. We ran one cell for overhauling Inconel 718 components. Instead of ordering a new blade from a 12-week lead time supplier, we printed a repair layer and finished it to tolerance on the same machine. Cut cycle time from weeks to days on parts that normally sat in a procurement queue. The catch is post-process heat treatment. Most hybrid cells don't have an integrated stress relief step. We had to shuttle parts to a separate furnace, which added about six hours per batch and introduced alignment risk. The workaround was building a custom pallet fixture that held both the printed part and a sacrificial calibration coupon. That way we could track residual stress through the coupon instead of relying on manufacturer specs. It added roughly twenty minutes of machining time but eliminated part rejection later.
CNC turning centers with live tooling and Y-axis are another category that gets underestimated. A standard lathe does rotation and longitudinal cuts. Add live tooling and you get milling, drilling, and tapping off-center without a second setup. For a component like a hydraulic manifold block, this can eliminate an entire machining step. One shop I knew reduced a five-operation workflow to two by switching from a mill to a multitask lathe. They didn't replace the mill entirely, but about sixty percent of the parts moved to the lathe permanently. The pitfall here is rigidity. Live tooling introduces off-center cutting forces that standard lathe spindles aren't always designed to handle at full load. If you're cutting titanium or hardened steel with a live tool, tool life drops significantly compared to a proper mill. We found that switching to ceramic inserts on the live tools and reducing feed rates by about thirty percent kept deflection within acceptable limits for most of our aluminum and steel work. Hardened materials still needed the mill. In-line metrology and SPC integration is less flashy but probably the highest ROI upgrade most plants can make. The concept is simple: measure parts during machining, not after. A probe on the machine tool checks dimensions, feeds the data back to the CNC offset, and adjusts the next cut automatically. One of our presses did this for a bearing seat diameter. Instead of waiting for a CMM check after the part was already done, the system caught a tool wear drift at about hour two of a run and compensated before scrap accumulated.
Get the Full Details

The limitation nobody mentions upfront is that in-line metrology only helps when the process is stable enough to be predictable. If your fixture is loose, your material batch varies wildly, or your thermal growth isn't controlled, the probe will compensate for errors that should actually be stopped at the source. We wasted about four weeks chasing offset adjustments on a process that really needed better fixturing. Once we upgraded to a precision tombstone fixture, the SPC data became actually useful instead of just masking symptoms. Robotic arc and laser welding cells are everywhere now, but the ones that deliver consistent quality follow a specific setup pattern. The robot program isn't the hard part. Getting consistent weld penetration across part variations is. We worked with a series of cast aluminum housings where the gap between mating surfaces varied by up to two millimeters due to casting tolerance. A standard programmed path would produce undercut on the wide gaps and burn-through on the tight ones. The solution was a laser welding cell with a seam tracking sensor, not just a standard MIG setup. The sensor mapped the joint gap in real time and adjusted travel speed and power on the fly. For the same part, weld defect rate dropped from about eight percent to under two percent. The initial investment was significant, but the scrap savings paid for the cell in roughly fourteen months at our production volume.
Digital twin and simulation-driven process planning deserves mention because the gap between marketing claims and actual utility is widest here. A proper digital twin of your machining process can predict cycle time, tool wear, and potential collisions before a single cut. The problem is that these models require accurate material data, real tool geometry inputs, and calibrated machine dynamics. If your CAM setup doesn't reflect actual cutting conditions, the simulation is just a nice-looking visualization. One project I led used simulation to optimize a multi-pass milling strategy for a large aerospace bracket. The software recommended a stepover reduction from twelve percent to seven percent of tool diameter, along with a climb-to-conventional switch on certain passes. Actual cycle time came in at about ninety-two percent of the simulated prediction, which is well within acceptable range. Tool life improved noticeably too. But getting there required calibrating the simulation model against real cuts first. Without that calibration step, the numbers are decorative at best.
Where these technologies commonly fail
The biggest failure mode across all of this isn't the technology itself. It's the expectation that it will work the way the vendor demonstrated it on a reference part. Shop floor reality introduces variability that demos don't show. Material batch differences, operator habits, ambient temperature swings, and fixture wear all accumulate. Another common failure is trying to automate inspection instead of preventing defects. SPC and in-process measurement are only valuable if you have a response plan. We installed a vision system on a stamping line that flagged dimensional drift, but the shift supervisor had no authority to adjust press tonnage without a manager present. The system would alarm, the part would keep running out of spec for forty-five minutes, and by the time someone authorized a stop, we had two hundred bad parts. The technology worked fine. The process around it didn't. If you're evaluating Advanced Manufacturing Technology Examples for your own operation, start by mapping where your current bottlenecks and scrap sources actually are. Then pick the technology that addresses those specific points rather than whatever has the best demo video. The cell that sits unused for six months because it solved a problem you didn't have is the most common outcome I've seen, and it's entirely preventable if you anchor the decision to measured pain points first.