Working with the Altendorf F45 When It Throws Errors
The F45 is a solid saw. It’s been on my shop floor for about six years now and honestly it rarely causes problems. When it does though, the error codes aren’t always intuitive. The manual covers the obvious ones but there are a few that show up on occasion and don’t get much attention in the documentation. I’m going to walk through the ones I actually deal with rather than just repeating what’s in the manual. Most of the time you’re looking at a few core errors that stem from the same handful of issues.
Understanding Altendorf F45 Error Codes
The control panel uses a combination of letters and numbers. E-codes generally indicate electrical or sensor faults, while P-codes relate to positioning and servo issues. There’s also the occasional Alarms group that’s more procedural, like guard open or material clamp errors. The most common one is the servo fault on the X-axis. It usually shows as E-Servo-X or something similar. What’s interesting is that this doesn’t always mean the servo drive itself is bad. I had this happen last year after a power fluctuation in the building. The error would come up on startup, the saw wouldn’t move, and everything looked terrible. Turned out the ground strap on the main electrical cabinet had loosened somewhere between the distribution board and the machine. Tightening that fixed it. I spent about two hours tracking down a loose lug that a multimeter could barely confirm was an issue. Another one worth mentioning is the Y-axis encoder fault. This shows up when the machine loses its reference position. Happens more often than I’d like after a complete power outage when everything comes back on simultaneously. The fix is usually a full machine rehome procedure, which you find in the service menu. Sometimes it’s as simple as running the homing cycle twice. Other times one of the encoder strips on the rail has accumulated chips or dust and needs cleaning. I keep a can of isopropyl and a lint-free rag near the machine specifically for this. Takes about five minutes if you know where the strips are located.
The clamp pressure error is another recurring one. It’ll flag when the material isn’t holding firm enough during the cut. Usually this is just worn clamp pads or compressed air dropping below the required threshold. Check your air pressure at the regulator first before you assume anything mechanical is wrong. My shop runs at around 7 bar and the clamp needs minimum 5.5 to hold properly. If your compressor is marginal the clamp error will show up intermittently, especially during longer cutting sequences when the tank pressure sags. Blade protection faults come up less frequently but they’re annoying when they do. The system monitors blade deflection during the cut and if it detects too much resistance or deviation it stops and throws an error. I’ve seen this caused by a slightly worn bearing in the blade housing, but also by using a blade that’s too narrow for the material thickness you’re cutting. There’s a minimum blade width requirement relative to kerf depth and if you’re running thin kerf blades in thick stock you’ll get false trips. The workaround is either switching to a proper blade or adjusting the sensitivity in the machine parameters, though I wouldn’t recommend lowering the threshold too far. It’s there for a reason. When you’re searching for specific Altendorf F45 Error Codes and their meanings, the best resource is still the service manual. You can get a copy through Altendorf directly or through their authorized distributors. There isn’t a great public database for these. Some third-party sites have uploaded scanned versions but they’re often incomplete or from older firmware revisions. The error code lists changed slightly between firmware versions 3.x and 4.x, so make sure you’re looking at the right one for your machine.
Get the Full Details
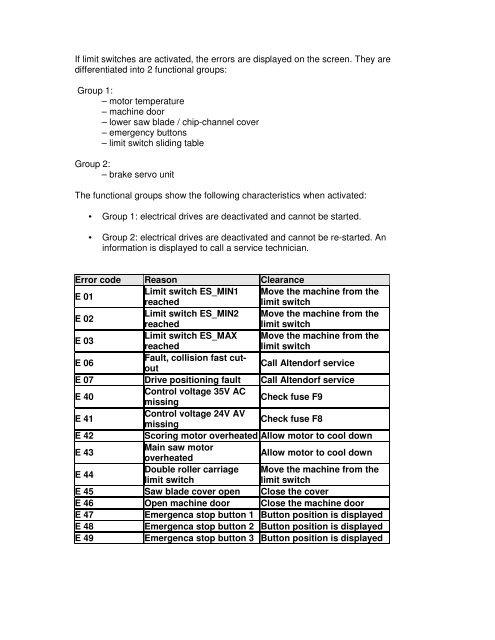
One thing the manual doesn’t make clear is that some errors are latched and some are self-clearing. Latched errors require a reset after the underlying issue is resolved. Self-clearing ones will just go away once the sensor reads normal again. The display will usually indicate which type you’re dealing with but it’s not always obvious. If you’re stuck on an error that seems like it should have cleared, try cycling the main power. Hold the off switch for ten seconds before turning it back on. I’ve seen this resolve ghost errors that wouldn’t clear through the normal reset procedure. The thermistor warnings on the servo motors are another category worth understanding. These show up as temperature-related errors and they’re legitimate concerns. If a servo motor is running hot enough to trigger a fault, there’s usually a mechanical issue behind it. Binding guides, insufficient lubrication on the rack and pinion, or a failing bearing will all cause the motor to work harder and heat up. I once had a persistent E-Temp-Y error that traced back to a dried-out grease fitting on the Y-axis rack. Lubed it up and the error never came back. The motor temperature had been climbing gradually over several weeks before it finally triggered the fault. If you’re dealing with communication errors between the PLC and the motion controller, that’s a different beast entirely. These tend to manifest as random freezes or the display going blank. Usually it’s a loose connector somewhere in the D-sub cable runs inside the control cabinet. Check the connectors on both ends first. Then check the earth bonding. I’ve seen this happen after routine maintenance when someone opened the cabinet and didn’t reseat everything properly. Always double-check those connections after any service work.
The good news is that the vast majority of errors on this machine are straightforward. The F45 is well-built and the electronics are generally reliable. Bad errors usually trace back to one of three things: power quality, maintenance neglect, or a single failing component. Work through those in order and you’ll save yourself a lot of time calling for service.