Amada Press Brake NC9 Controller: What It Is and How to Actually Use It
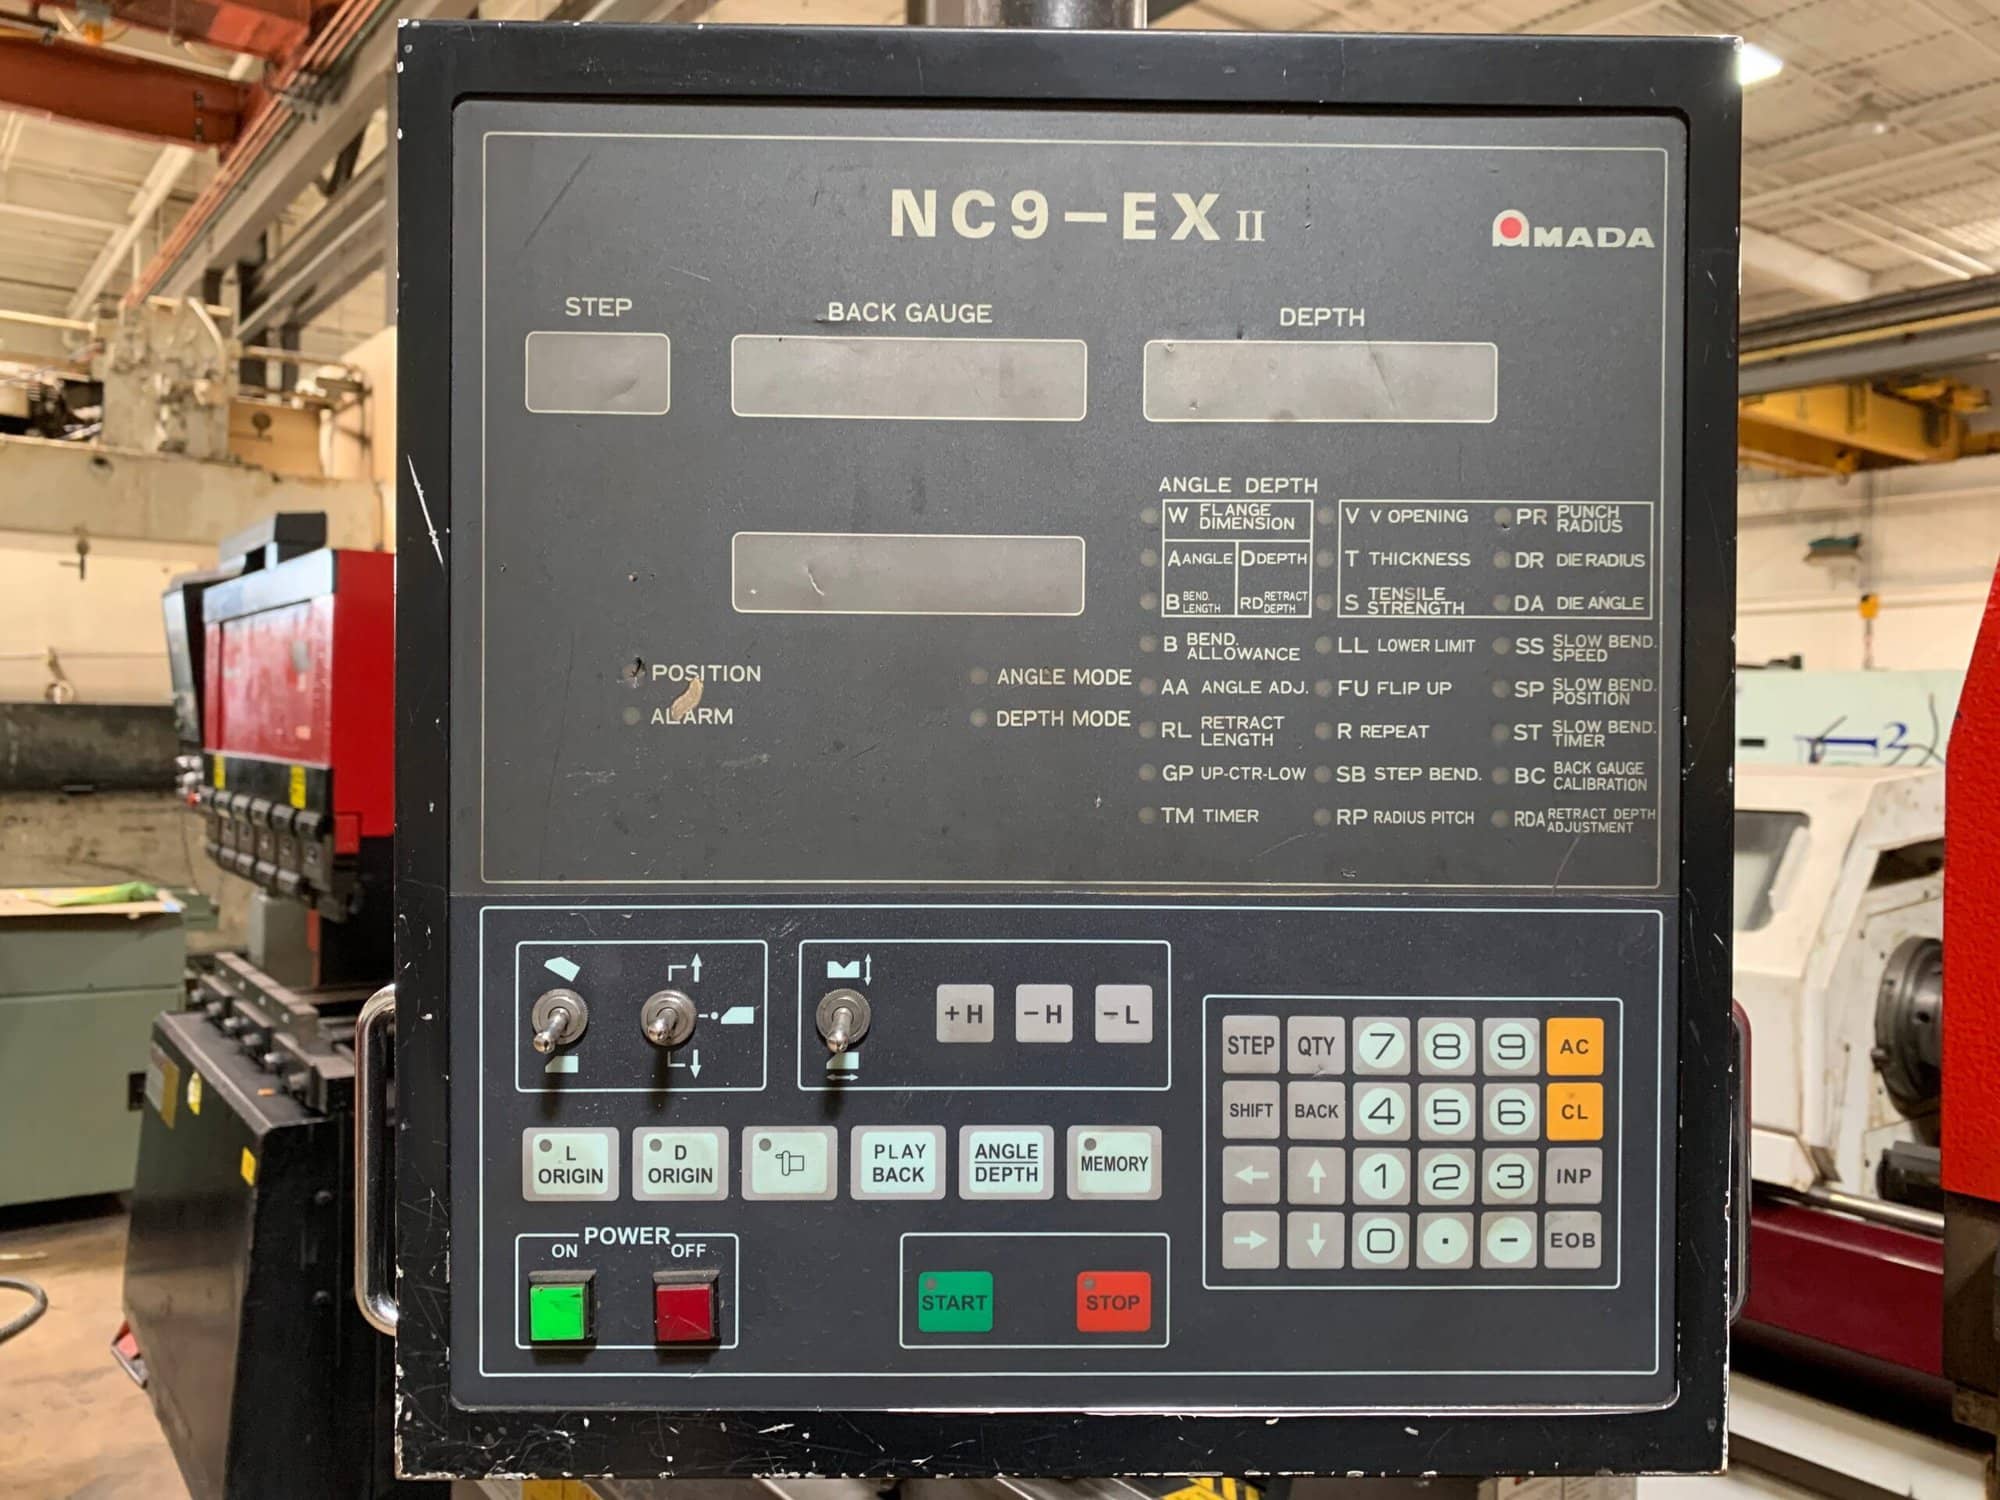
The NC9 is Amada's numeric control system for press brakes. It handles angle compensation, backgauge positioning, and tooling setup calculations in real time. If you're running an Amada press brake, you'll interact with this controller daily. The manual that comes with it is dense and not written for beginners. I've spent more hours than I care to count working through its sections, and there are details most operators miss. Most people treat the NC9 manual like a reference book you only open when something breaks. That's backwards. You need to understand the relationship between the machine's kinematics and the software's assumptions before you ever attempt a complex bend sequence. The NC9 does a lot of math behind the screen, and if you feed it bad input, the output will look right until your parts don't match.
Amada Bending Nc9 Control Manual
I recommend keeping a physical copy or a PDF on a tablet near the machine. The touchscreen interface is responsive but awkward to navigate when you're wearing gloves in a cold shop. The printed manual lets you flip pages quickly between sections without fighting through menus. Here's a practical walkthrough of what matters most when you're actually programming bends. Setting Up a New Bend Program
Navigate to Program mode. You'll see a list of existing programs and an option to create a new one. Enter the material type, thickness, and bend angle. The NC9 will calculate the required tonnage and press brake closing height automatically. Most operators just accept these numbers without question. That's where problems start. The tonnage calculation assumes standard V-die widths relative to material thickness. If you're using a narrow die or a specialty tooling setup, the calculation will be off. I had a situation last year where the controller was calling for 80 tons on a job that clearly needed closer to 120 tons. The operator had selected a 6mm V-die for 10mm material instead of the usual 80mm opening. Once I corrected the die width in the program, the tonnage reading adjusted properly. Check your tooling inputs every single time before hitting cycle start. Backgauge Positioning
Get the Full Details
The backgauge on Amada machines with NC9 control typically has X, R, and T axes. X is the main positioning axis. R tilts the fingers. T raises and lowers them. You program positions for each bend step, and the controller moves the backgauge through them automatically during the cycle. One thing the manual doesn't emphasize enough: the backgauge has a repeatability limit around 0.02mm under normal conditions. If your parts are consistently out of tolerance by a fraction, check the backgauge fingers and the guide rails for wear. I replaced worn guide blocks on a BR-4020 that had been accumulating maybe 0.15mm of play over three years. First article after the fix measured within spec on every station. Angle Compensation and Crowning
The NC9 has automatic crown control that adjusts the deflection compensation based on your program parameters. It reads the ram position and applies hydraulic correction to keep the bend angle consistent across the entire workpiece length. This is useful but not infallible. When bending very short pieces relative to the bed length, the crowning system can overcorrect. I learned this the hard way on a batch of 300mm flange bends on a 4-meter machine. The ends were coming out two degrees different from the center because the automatic crown was assuming a full-length load distribution. Switching to manual crown override for that job and programming a static offset fixed it immediately. The manual covers this scenario in section 7.3 but buries the explanation among dozens of other parameters. Common Pitfalls Beginners Miss
The NC9 stores tooling libraries. Operators sometimes populate these with incorrect offsets or wrong bend radius values. When you're building a new program from a different machine's tooling library, don't just copy and paste. Verify each tool entry against the physical tool on the machine. A single wrong radius in the library throws off the entire bend calculation, and the screen won't warn you about it. Another issue: backup battery failure. The NC9 uses a battery to retain program data and parameters. I once found a machine at a customer site where the battery had died approximately eight months prior. No alarm was triggered because the system only displays a warning light, not a message. Twenty-three programs had been lost. Replace the battery annually on a schedule. Don't wait for the warning to appear. Downloading the Manual

The official NC9 control manual is available through Amada's support portal. You'll need your machine serial number to access the correct document version. Amada releases updates periodically, so make sure you're downloading the version that matches your controller firmware. Using a mismatched manual with an updated system causes confusion, especially around the programming syntax sections which changed between firmware revisions. If you don't have portal access, contact your local Amada representative. They can email you a copy or direct you to a dealer who stocks printed versions. Third-party PDFs circulating online are often outdated or incomplete, missing revision notes that address known issues. When the NC9 Falls Short
The controller works fine for standard operations. It struggles with highly customized or multi-material setups where tooling changes frequently between shifts. Program setup time increases noticeably when you're swapping tooling more than twice per hour. In those environments, some shops run pre-setup tooling carts with labeled positions and program the NC9 for fewer changes per shift, batching similar tooling together. It's not elegant but it cuts changeover time significantly. For machines older than ten years, the NC9 hardware can become sluggish. Response time between keypress and screen update degrades. If your controller feels unresponsive, a firmware reload sometimes helps, but hardware replacement of the control unit is often the only real fix. Amada doesn't publicly disclose the hardware specifications, so diagnosing whether it's a software or hardware issue requires trial and error. The NC9 manual is adequate but not particularly user-friendly. It assumes you already understand press brake fundamentals. The best approach is to read it once thoroughly, then keep it nearby for reference as you build experience. The specific sections on tonnage calculation, crowning parameters, and backgauge programming will save you more headaches than anything else in there.