Welding Qualification Tests for Boilermakers
The boilermaker test isn't one single exam. It's a combination of practical welding performance and written questions covering codes, safety, and metallurgy. Most people looking this up are trying to prepare for a certification under ASME Section IX or AWS D1.1. Here's what you actually need to know going in. Written portions cover things like joint designation, welding positions, shielded metal arc welding (SMAW) parameters, gas metal arc welding (GMAW) settings, and basic metallurgy. You'll see questions about what E7018 versus E6010 electrode means, how to calculate travel speed, and when preheat is required. The practical side is usually a coupon weld evaluated for bend tests, visual acceptance, and sometimes radiography depending on the employer or jurisdiction. I once watched a guy fail his written section because he didn't know the difference between a backstep stringer and a standard stringer bead. He could weld all day, nailed every practical coupon, but missed three questions on welding symbols. That cost him the journeyperson spot at a refinery turnaroun. Don't let that happen to you. Go through a welding symbol reference sheet until the arrows, dimensions, and supplementary symbols are automatic.
How to Prepare for the Written Exam
Grab a copy of ASCA QW-400 through QW-490. That's the variable section of ASME Section IX. You don't need to memorize it, but you do need to know how to look things up fast. Test centers usually allow an open-book code reference, so bring yours marked up. Practice finding answers under time pressure. When I run study sessions for apprentice groups, I time them on locating a single parameter in the code book. Most can't do it in under 45 seconds on the first try. After two weeks of daily practice, they're consistently under 15 seconds. Here are sample questions you should be able to answer without hesitation: Question: What does an E7018 electrode designation mean?
Answer: 70 indicates tensile strength in ksi. 1 means all-position welding. 8 means low-hydrogen potassium coating with AC or DC reverse polarity. Question: When is preheat required for carbon steel according to Table 3.1 of ASME Section IX? Answer: It depends on material thickness, carbon equivalent, and hydrogen content of the filler. For A516 Grade 70 above 1.5 inches, preheat is typically required at 50-100°F minimum depending on the exact composition and procedure qualification record.
Get the Full Details
Question: What is the minimum branch-to-run diameter ratio for a 45-degree branch connection per ASME B31.3? Answer: The ratio should not be less than 0.5 unless specific design calculations justify a smaller ratio. This comes up constantly in boiler and pressure piping work.
The Practical Welding Test
Most employers have you weld a coupon in specific positions. For boilermaker work, 6G (pipe at a fixed 45-degree angle) is the gold standard. If you can pass a 6G SMAW or GTAW test, you're generally considered competent for structural and pressure boundary work. Plate tests in the 3G and 4G positions are also common for vessel fabrication roles. Key point nobody mentions enough: clean your bevels properly. I've seen coupons rejected for slag entrapment in the root pass, and the root cause wasn't technique. It was dirty base material. Oil, mill scale, or residual flux from fit-up grinding ruins root penetration consistency. Take five extra minutes to grind or wire-brush the joint before striking an arc. This alone fixed my own reject rate when I was testing for a nuclear plant contract — went from one rejection in six attempts down to zero rejections on the last twelve.
Common Pitfalls That Fail People
Travel speed variation is the biggest silent killer. Your arc length might look stable but if you're accelerating through the root on one side and dragging on the other, your penetration will be asymmetric. The bend test will crack on the slow side because of coarse grain structure from excess heat input. I learned this the hard way during a NDE-assisted qualification where a face bend failed at 18 degrees on one side and passed at 22 on the other. Fixed it by using a backing bar with a consistent pause at each root side instead of continuous travel. Another issue is ignoring the WPS being tested against. Some candidates auto-pilot through the weld using their personal habits instead of following the qualified procedure's amperage, voltage, and technique specifications. If the WPS calls for 140 amps on root passes and you run 170, you're technically not welding per a qualified procedure. The inspector doesn't care how good the weld looks if it doesn't match the PQR.
Resources That Actually Help
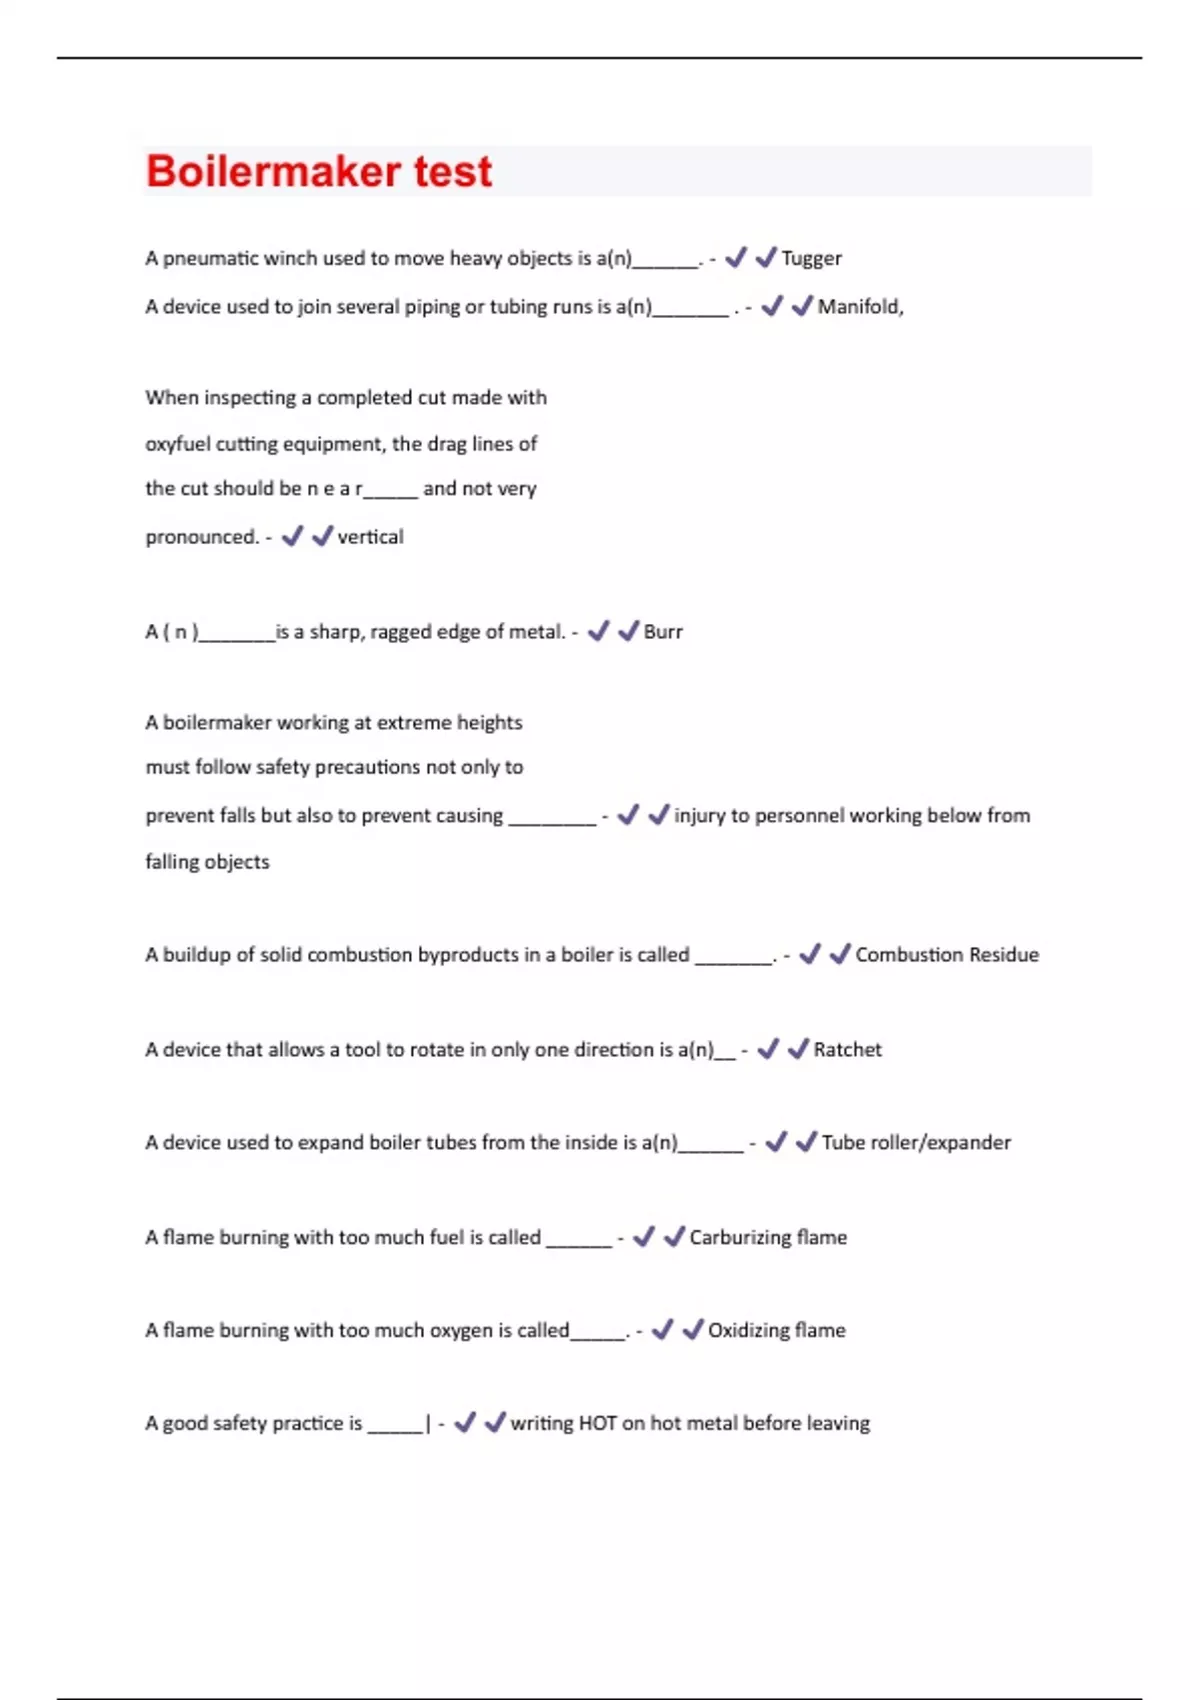
Stick with the official codes. The AWS Welding Handbook Volume 2 has solid review material. Lincoln Electric's procedure manuals are free online and worth reading even if you don't use their equipment. YouTube channels like TheWeldingGeek and Ben Koerner walk through test preparations but don't rely on them as your primary study source. They're supplementary at best. For actual Boilermaker Test Questions And Answers, the best approach is building your own question bank from past tests and code cross-references. Many trade shops keep old exam packets from previous hires. Ask your foreman or union local if they have copies. The questions recycle across industries because the code doesn't change that often.
When the Code Route Isn't Enough
Sometimes you'll encounter employers who want NBIC (National Board Inspection Code) or API 1104 specific qualifications beyond ASME Section IX. Those have their own question sets covering pipeline welding, repair and replacement rules, and field welding conditions. If you're targeting power plant or petrochemical work, budget extra time for API 1104 prep. It's a separate exam with its own practical — single-wall or double-wall technique questions plus written coverage of fracture-critical weld criteria. The written portion for API 1104 is shorter but more practical than ASME. Expect questions about cold shut detection, nickel alloy considerations, and field welding wind protection requirements. Bring your code book, keep it organized with tabs, and pace yourself on the written section so you have time to verify answers rather than guessing on the last five questions.