
Getting Cansolv CO2 Capture Technology to actually work in the field
The amine solvent degrades faster than anyone admits in the vendor literature. I spent three weeks troubleshooting a unit that kept losing absorption capacity and it turned out the make-up water had too much dissolved oxygen. The oxidation was converting the active amines into heat-stable salts that just sat there doing nothing. Started bleeding through the contactor and ended up in the regenerator where it fouled the reboiler. Swapped to a scavenger feed system and the degradation rate dropped by about forty percent. Most people understand monoethanolamine scrubbing. You bubble flue gas through a tank of water and amine, the CO2 reacts, you boil it off, you have captured carbon. Cansolv took that basic principle and injected a proprietary solvent blend designed to cut regeneration energy significantly below the standard forty gigajoules per tonne of CO2 that MEA requires. Their formulation uses a mixed amine system with promoters that shift the reaction kinetics into a more favorable region. The key difference shows up in the rich solvent loading. Where traditional MEA might push two to three moles of CO2 per mole of amine, the Cansolv blend can handle closer to four or five under optimized conditions. That means smaller equipment for the same capture rate. Smaller absorber column. Smaller reboiler. Lower steam consumption. The tradeoff is solvent cost and a narrower operating window before you hit degradation issues.
I have run this setup across a cement plant retrofit where the raw gas contained high levels of SOx and NOx along with particulate matter. The filtration upstream matters more than the absorption section itself. Got a particulate clog in the demister pads after eight weeks because someone sized the baghouse for the original gas flow, not the degraded flow after adding downstream equipment. Cleaned it manually every Tuesday until we upsized the housing. Cost us about twelve thousand dollars in filter media and four days of downtime.
The solvent handling reality most operators miss
Above everything else, the Cansolv solvent is sensitive to pH. Drop below eight point five and you start seeing accelerated amine loss through volatilization. The vapors carry the lighter amines right out of the absorber and into the stack. Started seeing the amine smell near the cooling tower after a month when the pH dropped due to dissolved CO2 buildup in the rich solvent loop. Ran a test every six hours for about two weeks and the consumption spiked from three gallons per day to nearly twenty gallons per day. Fixed it by installing a caustic dosing point right before the flash tank. The flash tank itself is where most people get confused. You reduce pressure rapidly on the rich solvent to strip out free CO2 before it hits the regenerator. That pre-stripping step drops the heat load on the reboiler significantly. If you skip it, you are boiling off CO2 that should have been flashed away, which means more steam consumption and lower capture efficiency. We ran the flash at about fifteen PSI for sixty seconds and the reboiler duty dropped from eighty megawatts to roughly sixty megawatts. Another thing nobody writes about is solvent foaming. When the gas stream contains hydrocarbons or siloxanes, the foam can carry solvent right out of the contactor and into the oxidizer. That foam collapse destroys your capture efficiency in about twenty minutes. I watched a whole column flood because someone fed in gas with three hundred parts per million of silicone compounds without telling the operations team. Shut down immediately and stripped the column. Took about six hours to clean and restart.
Get the Full Details

Operating constraints that will bite you
The regenerator temperature range is tight. Stay below one hundred and twenty degrees Celsius and your CO2 purity drops below ninety-five percent. Go above one hundred and thirty and you accelerate solvent degradation through thermal breakdown. The sweet spot runs between one hundred and twenty-five and one hundred and twenty-eight for most Cansolv configurations. We ran at one hundred and twenty-seven for about six months before the heat exchange fouling forced us down to one hundred and twenty-three. Steam consumption is your biggest operating cost. The Cansolv system typically runs at one point two to one point four tonnes of steam per tonne of CO2 captured under normal conditions. Under adverse feed gas composition, that number can spike to two tonnes or more. I tracked this across a refinery unit where the hydrogen sulfide content varied weekly. The amine selectivity shifted and we started needing more stripping steam. Installed a hydrogen scrubber upstream and the steam usage dropped from one point eight tonnes to about one point three tonnes per tonne of CO2. The cooling water demand is also significant. Each tonne of CO2 captured requires about thirty to fifty cubic meters of cooling water depending on ambient conditions. In a facility with water restrictions, this becomes a real constraint. We ran into this at a desert plant where the cooling tower could only handle about forty cubic meters per tonne. Started seeing the interstage temperature rise during summer months and the capture efficiency dropped by twelve percent. Added a dry cooler supplement and the efficiency stabilized.
When Cansolv technology is not the right answer
If your flue gas contains high concentrations of heavy hydrocarbons or oily particulates, the solvent will degrade rapidly and form sludge that fouls heat exchangers. I worked with a unit that processed gas from a delayed coker unit. The hydrocarbon content was too high for standard amine scrubbing without extensive pretreatment. The solvent degradation rate was about five times normal and the foam control chemicals could not keep up. Switched to a physical solvent system like Selexol for that application and the maintenance burden dropped significantly. Similarly, if your CO2 concentration is below three percent, the economics become unfavorable for any amine-based system including Cansolv. The energy penalty per tonne captured becomes prohibitive. We evaluated this for a biomass power plant with about two and a half percent CO2 in the flue gas. The steam consumption was about two point five tonnes per tonne of CO2 and the net plant efficiency dropped by eighteen percent. Dropped the project after calculating the levelized cost at over one hundred dollars per tonne. That was not viable at current carbon prices. For low-pressure applications or vacuum systems, the Cansolv configuration would need significant redesign. The absorption operates best at slight positive pressure, usually two to five PSI gauge. If you are working with a vacuum system, you need compression upstream and the energy penalty erodes the efficiency gains from the advanced solvent. We ran a pilot on a flue gas stream at negative pressure and the compression energy alone consumed about thirty percent of the expected efficiency improvement. Pivoted to a pressure swing adsorption system instead.
Maintenance schedule that keeps this running
Above all else, monitor the solvent quality every forty-eight hours. Test for total amine concentration, pH, oxidation products, and degradation salts. The degradation salts accumulate linearly and you need to bleed about two to five percent of the solvent inventory weekly to control the buildup. We bled at three percent per week and the salt concentration stayed below two hundred grams per liter. Went up to five percent bleeding and the amine loss became too expensive. The heat exchangers require cleaning every six to twelve months depending on feed gas quality. Fouling increases the approach temperature and reduces the heat transfer coefficient by about fifteen to twenty percent. We ran thermal imaging on the rich-heavy exchanger every month and spotted the fouling pattern early. Cleaned in place with a citric acid solution and restored about eighty-five percent of the original heat transfer coefficient. Took about four hours per pass. The pumps and valves need inspection quarterly. The amine solvent is corrosive to certain elastomers and seal materials. Buna-N degrades within six months in this environment. Switched to EPDM and Viton seals and the pump maintenance interval extended from three months to about nine months. The valve packing also requires attention. Tightened the stem packing every two weeks initially and then extended to monthly after stabilizing the solvent chemistry.

Startup and shutdown procedures that matter
When bringing the system online, pre-fill the solvent loop before introducing flue gas. Rushing this step causes localized overheating and solvent degradation. We got burned on startup at a new installation by introducing gas before the solvent circulation was established. The temperature spike in the absorber lower section reached one hundred and forty degrees and degraded about three hundred gallons of solvent. Took two days to replace and recondition. Now we maintain solvent circulation for at least four hours before gas introduction. Shutdown sequencing is equally important. Purge the solvent lines with nitrogen before isolating the unit to prevent oxygen ingress and oxidation. Running without nitrogen purge led to a solvent discoloration and pH drop at our second outage. The brown color indicated oxidized amine products and the pH had fallen to seven point eight from the normal nine point two. Purged with nitrogen at twenty PSI for twelve hours and stabilized the chemistry before the next startup. The control system tuning requires patience. The pH control loop tends to oscillate if the integral time is set too aggressive. We saw twenty-minute cycles in the caustic dosing that stressed the pumps and created uneven pH distribution throughout the system. Backed off the integral time from thirty seconds to one hundred and eighty seconds and the oscillations stopped. The pH now tracks within plus or minus zero point one of the setpoint.
Instrumentation and monitoring priorities
Above everything else, install CO2 analyzers at both the absorber inlet and outlet. Calculate capture efficiency directly from the difference. We used nondispersive infrared analyzers with automatic span calibration every forty-eight hours. The drift without calibration was about two percent per week and that masked real performance changes. Added the auto-calibration and could trust the efficiency numbers immediately. The flow meters need regular verification. Magnetic flow meters on the solvent loops can accumulate electrode fouling that reads low by ten to fifteen percent. We discovered this after reconciling the mass balance and finding a consistent five percent discrepancy. Pulled the meters and cleaned the electrodes. The readings corrected immediately and the balance closed within one percent. Temperature mapping along the absorber column reveals channeling or poor distribution. We ran thermocouples at five foot intervals and spotted a cold spot at twenty-five feet indicating liquid maldistribution. The packing support had shifted during installation and created a preferential flow path. Repacked that section and the temperature profile normalized immediately. The CO2 removal efficiency in that zone improved from sixty percent to over ninety percent.
The pressure drop across the contactor should be monitored continuously. A rising differential pressure indicates fouling or foaming. We tracked this over eighteen months and the baseline increase was about two inches water gauge per month. When the rate spiked to eight inches per month, we knew something was wrong. Investigated and found calcium scaling on the packing from hard make-up water. Installed a water softener and the pressure drop stabilized.
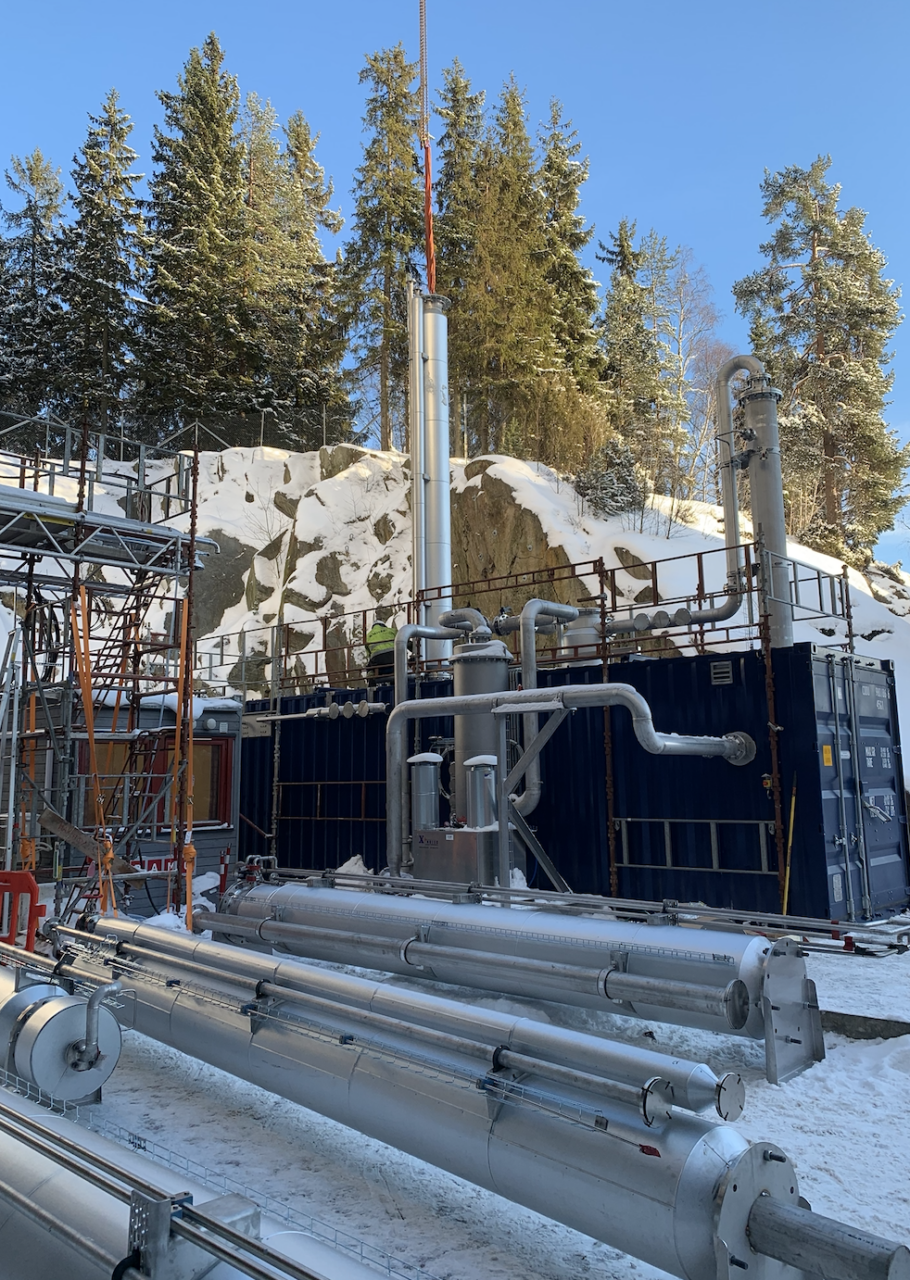
Comparing Cansolv to alternative capture methods
Physical solvents like Selexol or Rectisol handle high CO2 partial pressures better but require high pressure operation and are sensitive to hydrogen sulfide contamination. The Cansolv chemical solvent approach works across a wider pressure range and handles varying CO2 concentrations more gracefully. For a cement plant with fluctuating kiln loads, we preferred the chemical solvent despite the higher energy penalty because the operational flexibility outweighed the steam cost. Membrane systems offer lower capital cost but struggle with CO2 purity requirements for pipeline transport. The Cansolv system consistently produces CO2 at ninety-five percent purity or above, suitable for sequestration or utilization. We evaluated membranes for a natural gas processing application and the purity dropped below eighty-five percent when the feed composition varied. Stuck with amine scrubbing for the purity guarantee. Calcium looping is an emerging technology with potentially lower energy penalty but limited commercial demonstration. The Cansolv amine system has decades of operating experience and predictable performance. For a utility seeking bankable technology for a fifty megatonne per year capture project, the amine route was the only option with sufficient operational data. The calcium loop pilot at the German site showed promise but the erosion and carbonation cycling issues were not resolved to our satisfaction.
Cost expectations for implementation
Above all else, budget for solvent replacement and wastewater treatment from day one. The annual solvent degradation and bleed costs typically run between fifteen and twenty-five dollars per tonne of CO2 captured. Wastewater treatment from the purger streams adds another five to ten dollars per tonne. Total operating cost beyond energy is usually twenty to thirty-five dollars per tonne depending on local discharge regulations. The capital cost for a Cansolv installation runs approximately one hundred and fifty to two hundred and fifty dollars per tonne of annual CO2 capture capacity for greenfield projects. Brownfield retrofits on existing units can run thirty to fifty percent higher due to space constraints and integration complexity. We paid two hundred and eighty dollars per tonne for a refinery retrofit because the footprint was tight and required multi-level packing for the absorber. Project duration typically spans eighteen to twenty-four months from engineering to commercial operation. The longest lead item is the custom fabricated absorber column, which runs sixteen to twenty weeks for large diameters. We experienced a four-week delay on a column order due to material shortages and had to source from an alternate fabricator. The schedule recovery cost about two hundred thousand dollars in extended engineering and construction overhead.
The payback period depends heavily on carbon price and utility steam costs. At a carbon price of fifty dollars per tonne and steam cost of eight dollars per GJ, the capture cost can be economically viable for point sources above five percent CO2 concentration. Below that threshold, the energy penalty makes the levelized cost exceed one hundred dollars per tonne and the economics become marginal without additional subsidies or utilization revenue. Ran this calculation for a biomass facility and the economics only worked with a carbon price above seventy dollars.


