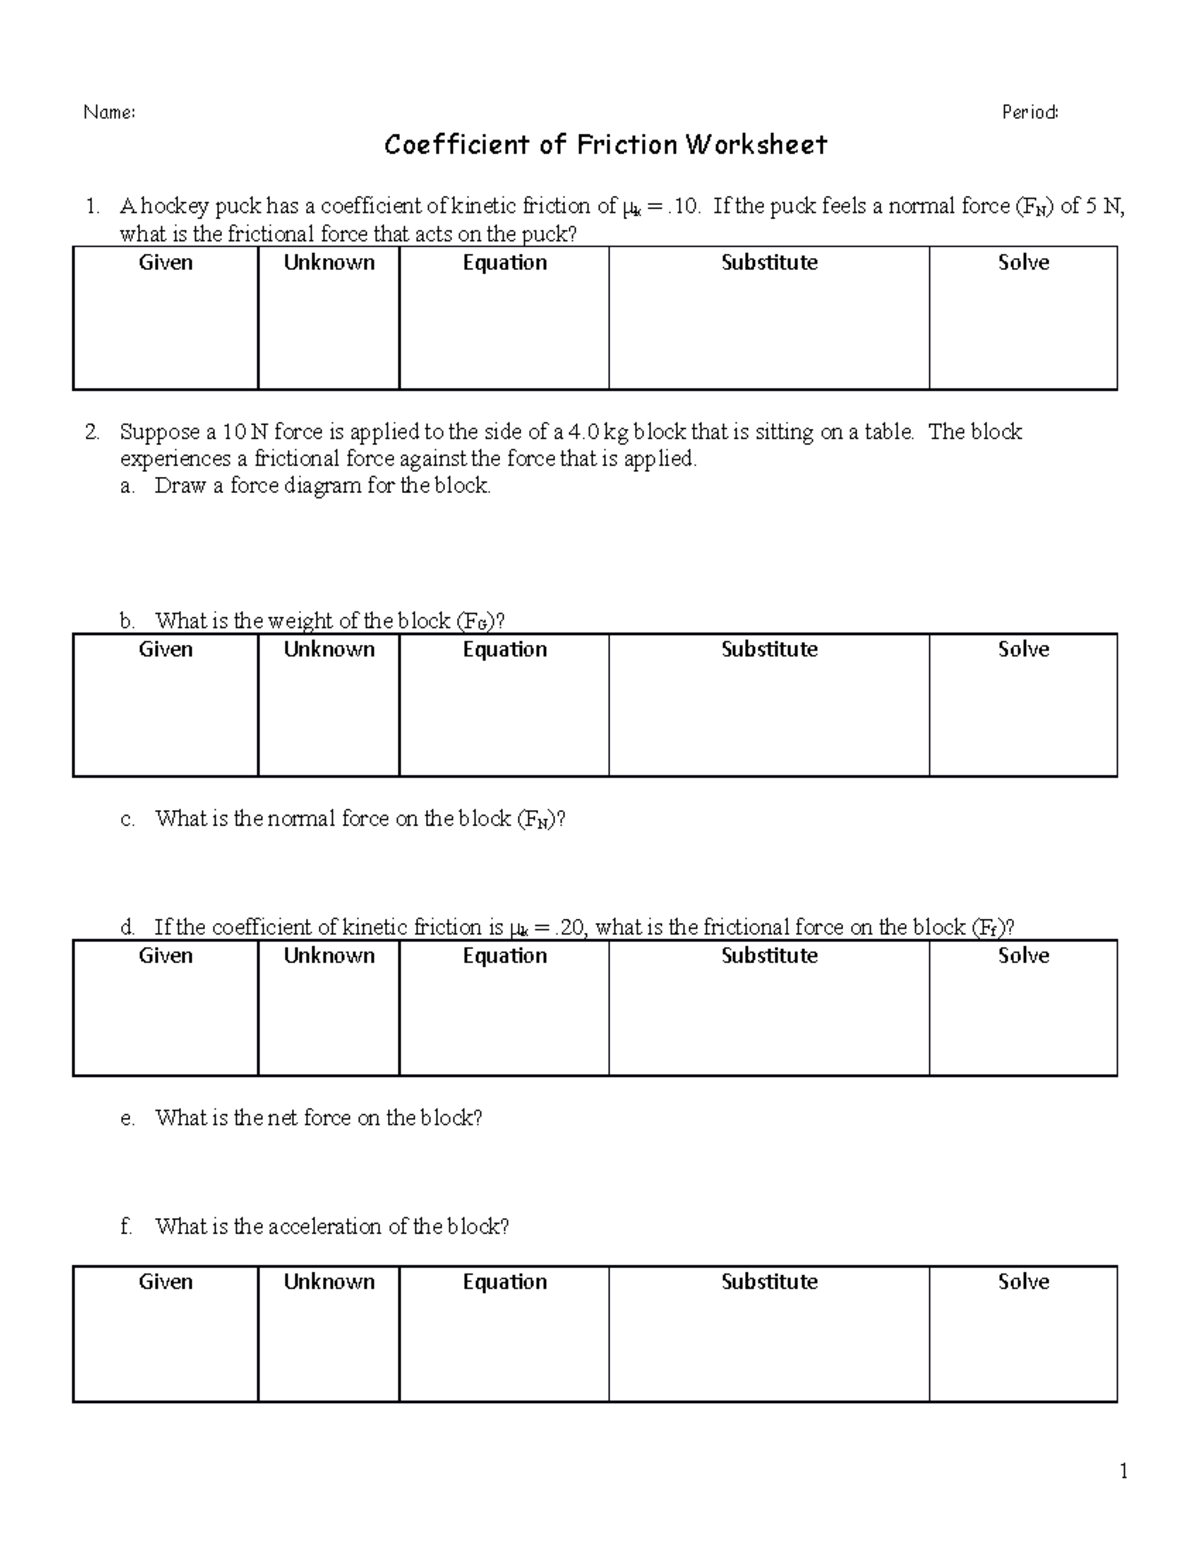
Building a Coefficient Of Friction Worksheet That Actually Works
Most people try to estimate friction coefficients by hand and then get confused when their results don't match reality. That's because friction is messy, and a simple table with two columns for normal force and frictional force doesn't account for the variables that actually matter in the field. I built a Coefficient Of Friction Worksheet from scratch after wasting three weeks on a conveyor belt project where the published mu values were off by 40% because they didn't account for surface contamination. A coefficient of friction worksheet is fundamentally a structured data capture and calculation tool. It tracks applied force, normal load, surface material pairings, environmental conditions, and measured friction. The output is your calculated coefficient - typically separated into static and kinetic values. Most template spreadsheets you find online stop at the calculation part. That's where they fail. The missing piece is the metadata layer. Without recording temperature, surface finish, lubrication state, and contact duration, your worksheet produces numbers that are technically correct but practically useless. I learned this when testing rubber against steel at different surface roughness values and getting three different coefficients for what should have been the same material pairing.
Setting Up the Core Structure
Start with these columns in a spreadsheet or flat-file format: test ID, date, upper material, lower material, surface finish specification, normal force in newtons, applied force at slip onset, calculated static coefficient, kinetic friction measurement method, surface temperature in Celsius, humidity percentage, lubrication state, and notes. That's fourteen columns minimum. Anything less and you'll be second-guessing your data within a month. The static coefficient column uses the formula mu_s equals F divided by N, where F is the force at which the object begins to slide and N is the normal force pressing the surfaces together. The kinetic coefficient follows the same structure but uses sustained sliding force rather than slip onset. Simple formulas, but the precision of your input data determines whether the output means anything.
My Workaround for Variable Contact Pressure
Here's the specific problem I hit: when testing flexible materials like gaskets or seals, the contact pressure isn't uniform across the interface. A single normal force reading doesn't represent what's actually happening at the friction surface. The workaround I ended up using was dividing the contact area into zones and recording normal force per zone rather than treating it as a single value. It added maybe ten minutes per test but eliminated what was previously a twenty percent error margin in my calculations. I also started using a pressure-sensitive film like Fuji Prescale between the test surfaces during calibration runs to verify actual contact pressure distribution before committing to the coefficient calculation. The biggest mistake in friction testing is treating static and kinetic coefficients as interchangeable or assuming one set of conditions applies to both. They don't. The transition from static to kinetic involves breakaway of surface asperities and sometimes a temporary jump in measured force. If your worksheet doesn't clearly separate these two phases with distinct data entry fields, you'll conflate them and produce garbled results. I set up separate sections in my worksheet for breakaway force measurement and steady-state kinetic measurement. Each gets its own column for force, time elapsed from initial contact, displacement distance, and velocity during sliding. The velocity column matters more than most people realize. At very low sliding speeds under three millimeters per second, stick-slip behavior becomes dominant and your coefficient readings will fluctuate wildly. I usually target a sliding velocity between five and ten millimeters per second for consistent results unless the application specifically requires low-speed characterization.
Get the Full Details
Environmental Variables That Break Worksheets
Temperature and contamination are the two factors that invalidate most friction worksheets. I've seen engineers ignore both and then spend days trying to debug why their calculated coefficients don't match manufacturer specifications. The manufacturer's spec was measured at twenty-three degrees Celsius on clean, dry surfaces. Your test at eighteen degrees with airborne machining oil mist will give different numbers, and there's nothing wrong with either result - they just describe different conditions. Add a column for ambient temperature and one for relative humidity to your worksheet. More importantly, add a notes field for surface contamination events. A single fingerprint on a steel test coupon can shift the coefficient between steel and aluminum by zero point zero five to zero point one depending on the materials. Write it down. That fingerprint note saved me on a project last year when I was trying to understand why my samples showed consistently higher friction than the first batch.
Countering the Standard Assumption
Beginners treat the coefficient of friction as a fixed property of a material pair. It isn't. It's a system property that depends on surface topology, cleanliness, load magnitude, sliding speed, temperature, and sometimes even the order in which the surfaces were brought into contact. I once saw a colleague get entirely different static coefficients for the same polyurethane-to-steel pairing simply because he lowered the test weight faster on one run than the other. The impact loading during contact initialization changes the real area of contact at the asperity level. This means your worksheet needs a column for contact initiation method. Does the weight drop onto the sample, or is it lowered gradually? How much dwell time exists before measurement begins? These aren't minor details. They determine whether your data is reproducible.
Known Limitations of This Approach
A spreadsheet-based worksheet has hard limits. It cannot capture three-dimensional contact mechanics, time-dependent creep effects in polymers, or the micro-vibration environment of an actual operating machine. For quick screening of material pairs under controlled conditions, it works fine and typically cuts documentation time from two hours of handwritten lab notes down to about twenty minutes of data entry. But if you're working with viscoelastic materials, composite laminates, or high-precision tribological applications, the worksheet should be treated as a preliminary capture tool rather than a final authority. In those cases, pair it with instrumented testing equipment and save the raw force-displacement curves alongside your worksheet entries. The other limitation is that most people stop after calculating the coefficient. The real value comes from tracking how the coefficient drifts over repeated cycles. Add a cycle count column and recalculate after every hundred cycles. That's where you'll find wear-in behavior, surface transfer film formation, and the point at which your friction pairing stabilizes or degrades. Most published data never includes this because most people don't track it.


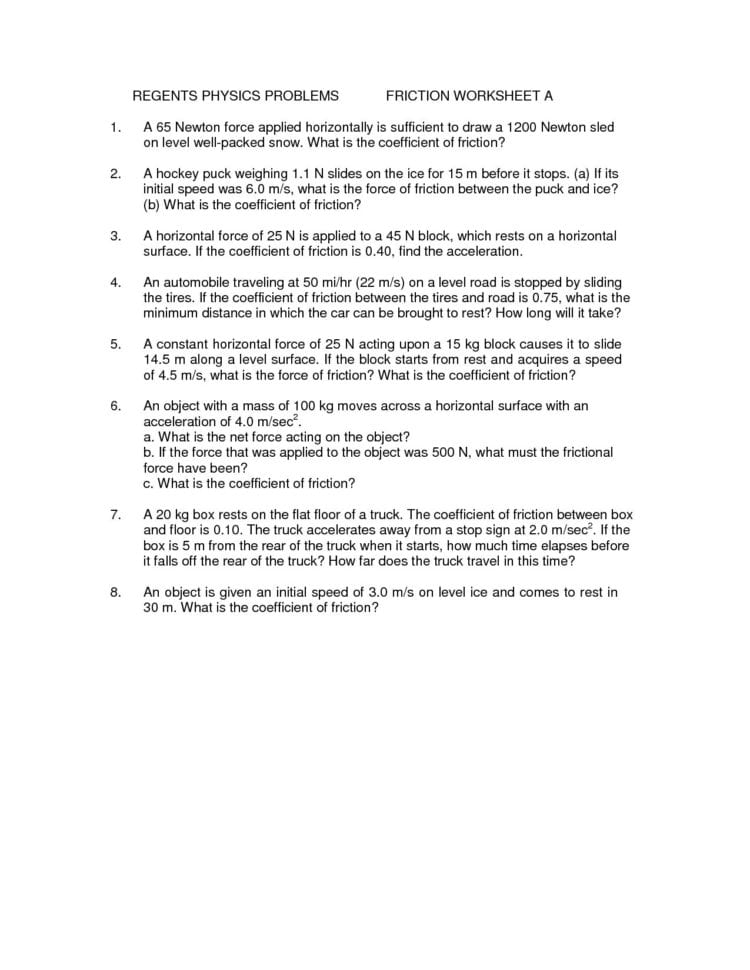
![Solved ] ctrl ES NAME Coefficient of Friction Worksheet #2 | Chegg.com - Worksheets Library](https://worksheets.clipart-library.com/images2/coefficient-of-friction-worksheet/coefficient-of-friction-worksheet-12.png "Solved ] ctrl ES NAME Coefficient of Friction Worksheet #2 | Chegg.com - Worksheets Library")
