
Resin color pours are not complicated if you stop overthinking them
I have made hundreds of resin pieces, and the ones that actually look good are the ones where I stopped trying to force the colors to do something dramatic and just let the chemistry do what it does. People obsess over the pour technique like it is some ancient secret, but the real difference between a cloudy mess and a clean pour comes down to two things: temperature control and timing. Everything else is noise. Before you mix anything, you need to understand the working window. Most epoxy resins give you about 20 to 45 minutes of workable time at room temperature before the viscosity climbs past the point where colors will flow and blend. If your shop runs cold, that window shrinks. I keep mine at roughly 72 degrees Fahrenheit because anything lower and I am fighting the material the entire time. The pour technique matters less than you think. The basic method goes like this. You mix your resin and hardener according to the manufacturer ratios, which most people skip reading and then wonder why their piece stays tacky for three weeks. Once mixed, divide it into separate cups. Add your pigments. Silicone resin dyes, alcohol inks, and mica powders all behave differently. Dyes tint clear. Mica adds opacity and shimmer but thickens the resin faster. I usually stick to a combination of dye for base color and a touch of white opaque for depth.
Pouring itself is straightforward enough that I barely think about it anymore. You can do a stacked pour by layering colors directly into the mold, or a flip cup where you pour each color into a single cup in layers and then flip it onto the mold. The flip cup tends to produce more organic, cell-like patterns because the colors migrate as they hit the surface. I prefer that look for most of my work. One thing nobody mentions until they ruin a batch: air bubbles. If you mix aggressively, you are trapping air. Let the mixed resin sit for about two minutes before adding pigment so bubbles rise. When you pour, pour from a low height, maybe six inches above the mold. A heat gun or torch passed quickly over the surface pops remaining bubbles. I use a butane torch, but a heat gun works if you keep it moving. One second over one spot and you get craters or scorching. I learned that the hard way on a large tray piece that ended up looking like the surface of the moon. Cover the mold. Dust gets in and ruins the finish, and I have spent hours sanding out embedded particles that a simple cover would have prevented. Use a cardboard box or a proper dust cover. Do not skip it.
Demold timing depends on the resin and the thickness of your pour. Thin pours under a quarter inch cure faster, often ready within 24 hours. Anything thicker needs longer. I typically wait 48 to 72 hours before demolding, and another few days before I do any sanding or finishing. Resin continues to harden past the initial cure, and pulling it out too early risks cracking or deformation. Patience is the cheapest tool in this process. If you are new to this, start small. A 4x6 inch mold teaches you more than a giant pouring board because mistakes are cheaper and you learn the behavior faster. Mix your resin properly. Measure twice. Keep your workspace stable temperature-wise. And stop watching YouTube tutorials about fancy techniques before you have made five basic pours. The fancy stuff is irrelevant until the basics feel automatic. There is no universal Color Pour Resin Mold Maker Instructions document you can download and follow perfectly because every resin brand, every pigment, and every environment behaves slightly different. What works in a humid Florida garage will not work the same way in a dry Colorado studio. The instructions on the bottle are a starting point, not a guarantee. You develop intuition from making the same pour ten times and noticing what changed each time. That is where the actual knowledge lives.
Get the Full Details

If you want a reliable reference point, most resin manufacturers publish detailed pouring guides on their websites. West System, River Road, and ArtResin all have thorough documentation. But those are general guidelines. The specifics of your pigments, your mold material, and your climate will dictate the adjustments you need to make. No single PDF covers that. You figure it out by doing the work. I once tried pouring with a new brand of mica powder I had never used before and the resin gelled completely inside the cup after only fifteen minutes. Turns out that particular pigment accelerates the cure significantly. I had already mixed two cups and watched both go to waste. The workaround was simple in retrospect: test a small amount of any new pigment in a separate cup before committing your full batch. Ten minutes of testing saves an hour of frustration and a lot of expensive resin. Mold selection matters too. Silicone molds are the standard for a reason. They flex, they release clean, and they handle reasonable complexity in shape. Cheap silicone can tear during demolding, especially on pieces with sharp edges or deep relief. I buy mid-range to high-grade silicone and avoid the cheapest options on marketplaces. The price difference is maybe twenty dollars and it prevents a lot of ruined pieces.
Surface preparation of the mold itself is worth mentioning. A light dusting of talcum powder or a spray of mold release can help with stubborn pieces, though most good silicone molds do not need it. I only use release agents when a piece has intricate detail or when the resin seems to be gripping. Overusing release agent creates a hazy film on the finished surface that requires extra sanding to remove, so I apply it sparingly when I do use it. Ventilation is non-negotiable. Epoxy fumes are not something to breathe deeply over extended periods. Work in a space with active airflow. An exhaust fan or an open window with a box fan blowing out is sufficient for most home studios. I keep a small fan running near my work area during mixing and pouring. It keeps the air moving without creating drafts that mess up the pour surface. Temperature swings after pouring can cause issues too. I had a batch where the nighttime temperature dropped fifteen degrees while the resin was curing and the top surface developed condensation that turned into a cloudy patch. It was unsalvageable. Covering the mold and keeping the environment stable prevents that kind of problem. If you pour in a space with significant temperature variation, consider a heated enclosure or at least a thermometer to monitor conditions over the cure period.
The final finish often separates beginners from people who produce acceptable work consistently. Sanding starts at 220 grit and progresses through 400, 600, 800, 1000, 1500, and finally 2000 or higher. Between each stage, clean the surface thoroughly to remove dust before moving to the next grit. Skipping grits leaves scratches that become obvious in the final polish. I wet sand with water and a bit of dish soap to keep the paper from clogging. It takes longer than dry sanding but the results are noticeably smoother. For the highest clarity finish, a polishing compound like Novus #2 followed by Novus #3 brings resin to a glass-like shine without the hassle of a additional resin coat. Some people pour a thin glossy top coat to achieve that effect, but that introduces another layer where bubbles and dust can cause problems. Polishing is more work upfront but it is more predictable. If your pours consistently come out cloudy, check your resin-to-hardener ratio first. Imbalanced mixing is the most common cause of cloudy or soft cured resin. Second check is temperature. Pouring in a cold environment slows the chemical reaction and can leave the resin in a partially cured state longer, during which moisture from the air can cause cloudiness. Third is contamination. Wiping down your mold with isopropyl alcohol before pouring removes oils and debris that interfere with the surface cure.
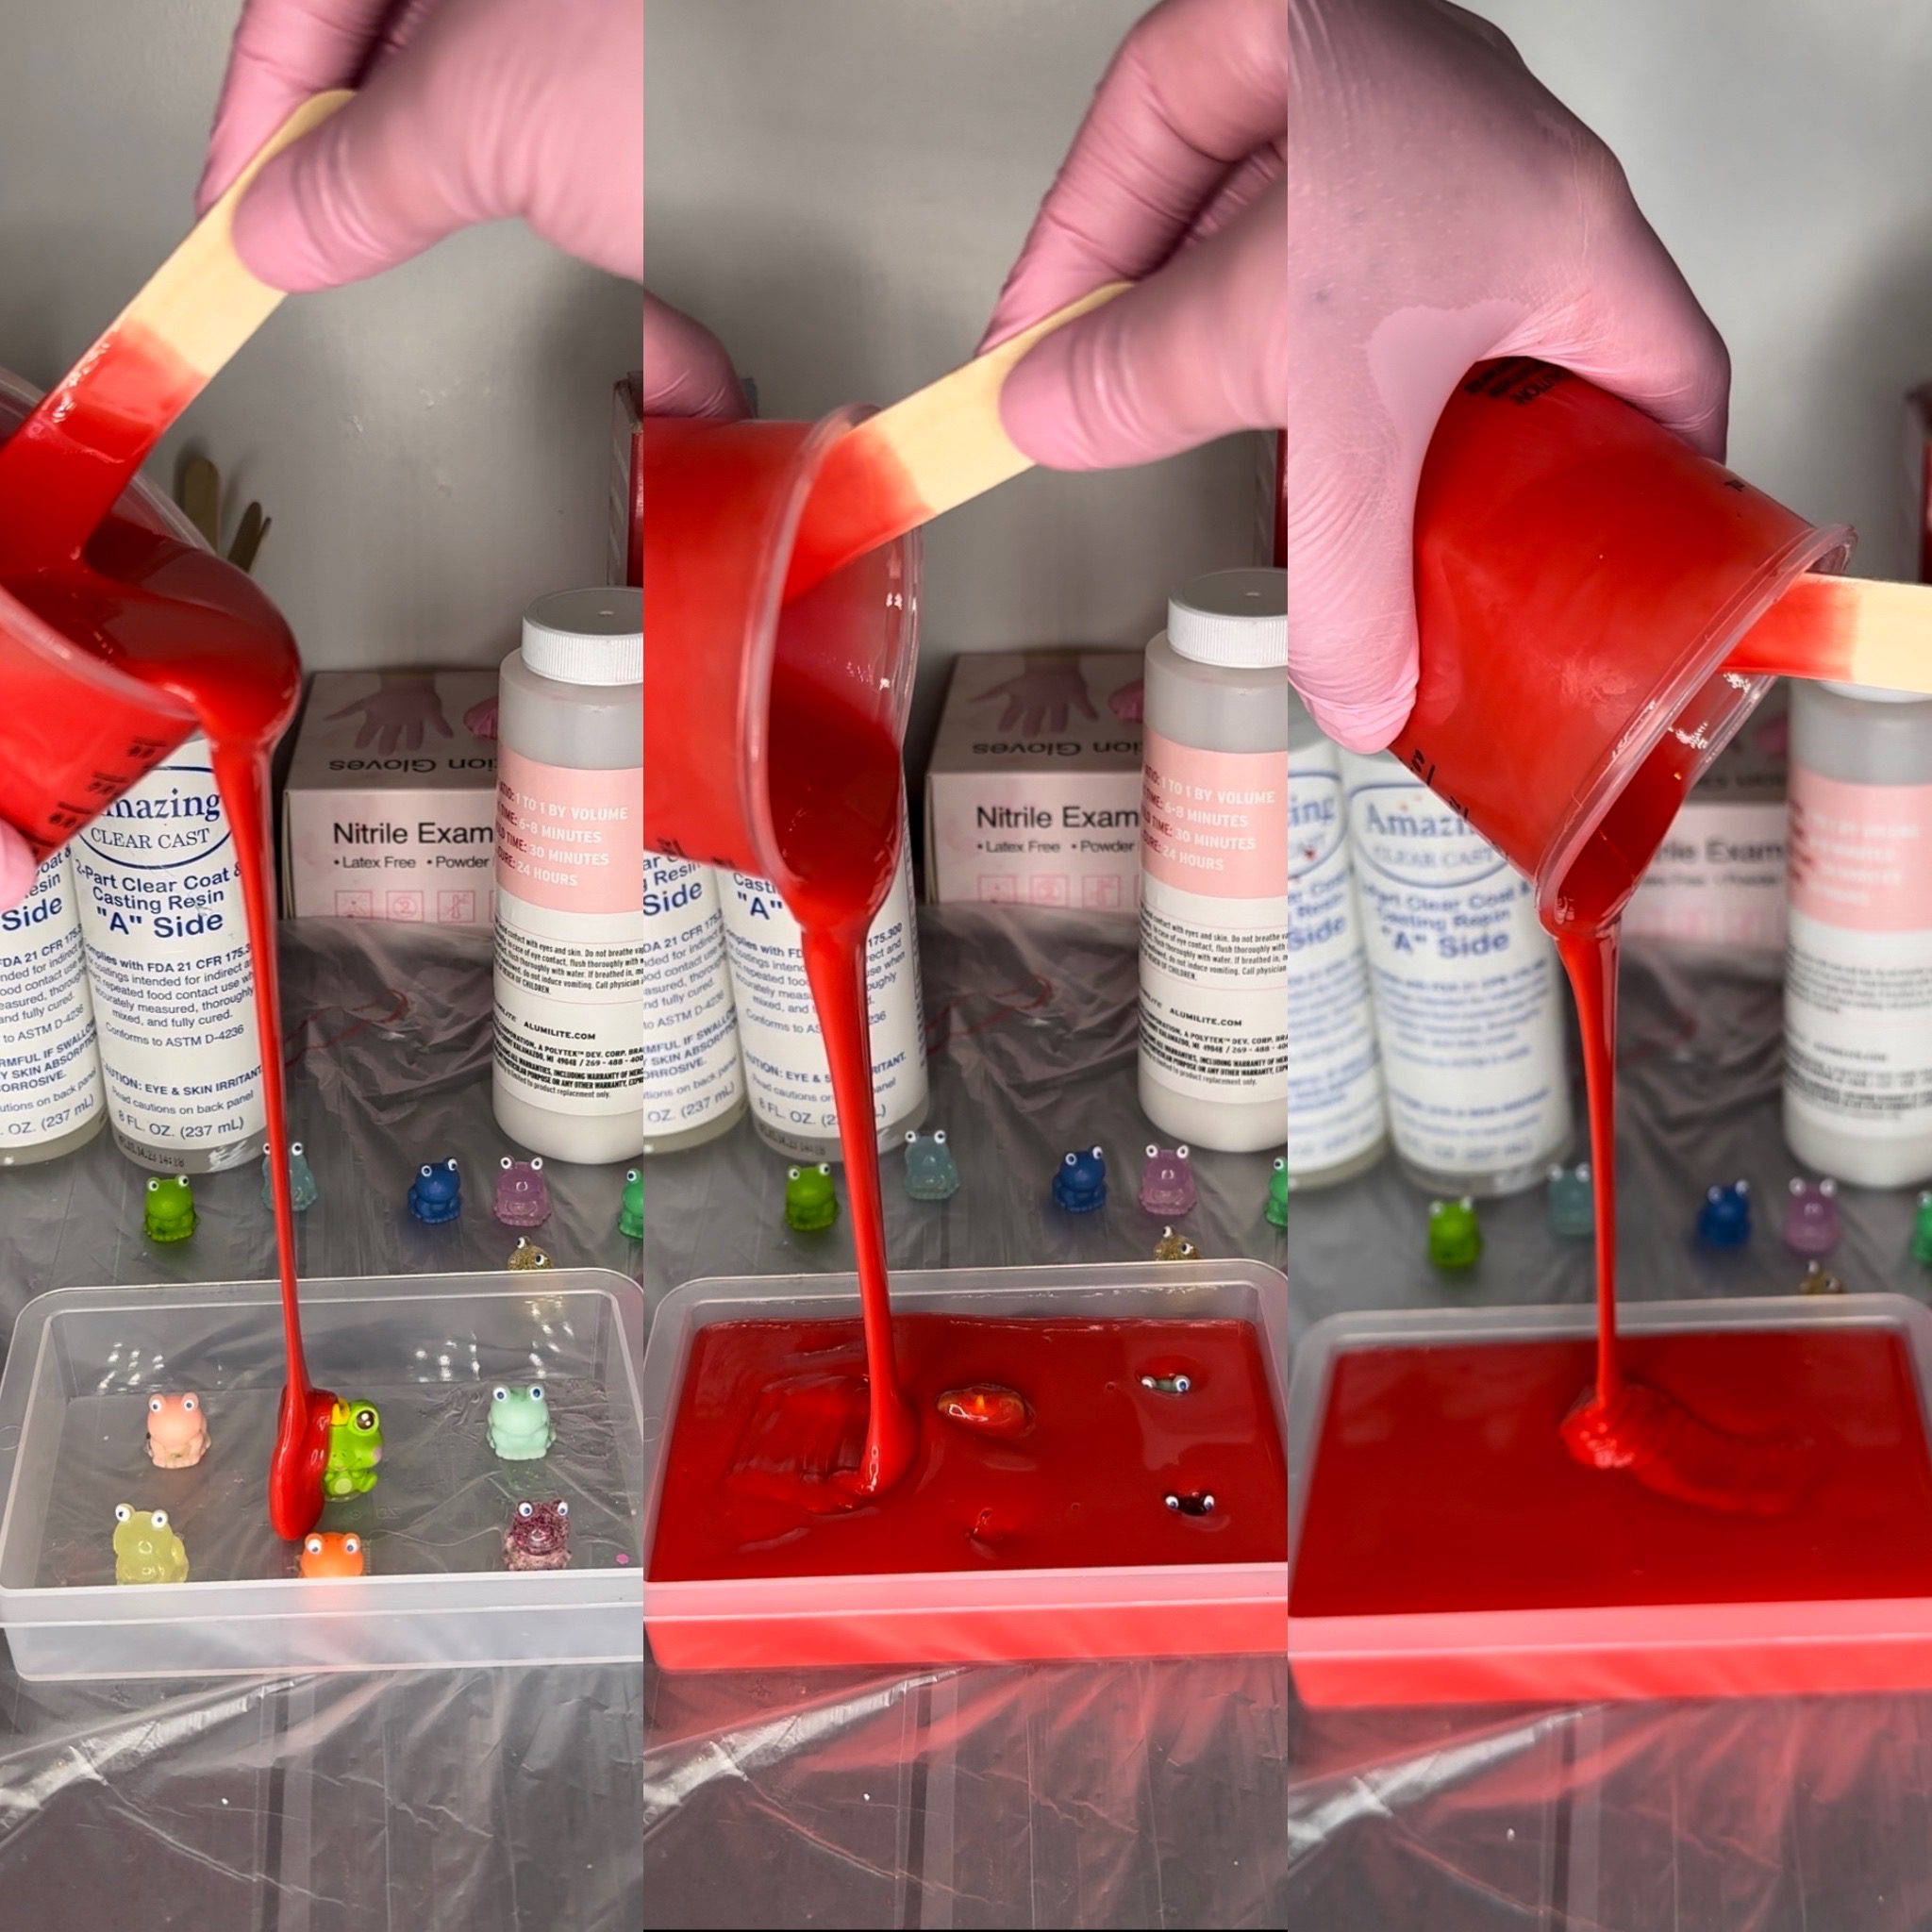
Titanium dioxide opaque white is useful but it thickens resin faster than most other pigments. If your formula includes a high percentage of white, expect a shorter working time and adjust your pour speed accordingly. I mix my whites separately and add them to the main batch right before pouring rather than mixing them in early, which helps manage the accelerated gel time. There is no shortcut that replaces practice. The Color Pour Resin Mold Maker Instructions you find online are useful frameworks, but the actual skill comes from repeated execution and observation. I have poured the same design dozens of times and still get different results each time because subtle variables shift. That variability is what makes this process interesting, even if it is frustrating when you are trying to reproduce a specific look consistently. Keep your records. Note the resin brand, the ambient temperature, the pigment types and amounts, and the pour method for each piece. A simple notebook or a spreadsheet on your phone works fine. After a dozen pours, you will start seeing patterns in what works and what does not for your particular setup. Those patterns are more valuable than any generic instruction guide.
Resin is inexpensive enough that you will waste some material while you learn. Accept that upfront. The first five pieces will probably not be great, and that is normal. Each one teaches you something specific about how your materials behave. By the tenth or fifteenth piece, you should have a feel for what adjustments to make before you even start mixing. The core principle is simple: control what you can control, accept what you cannot, and measure your results honestly. Most of the problems people encounter with color pour resin are preventable with basic attention to mixing accuracy, temperature, and timing. Everything beyond that is refinement, and refinement comes from doing the work repeatedly over time.


