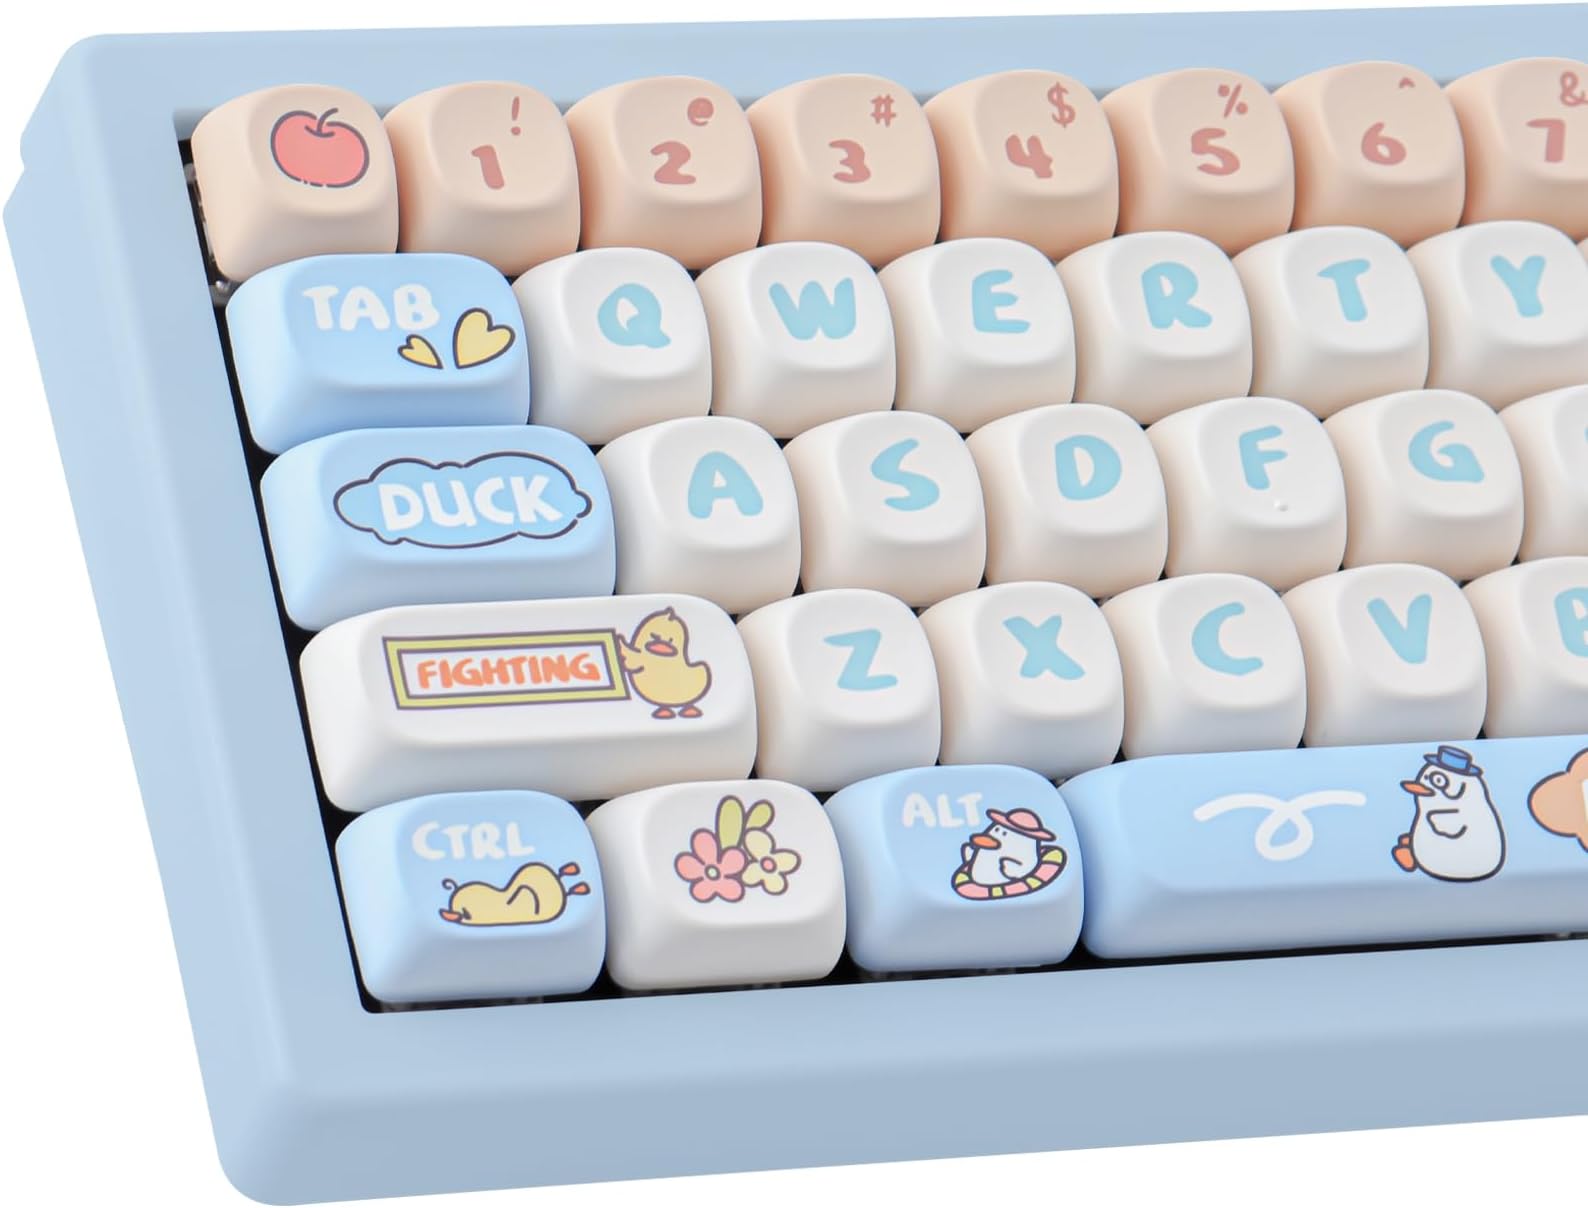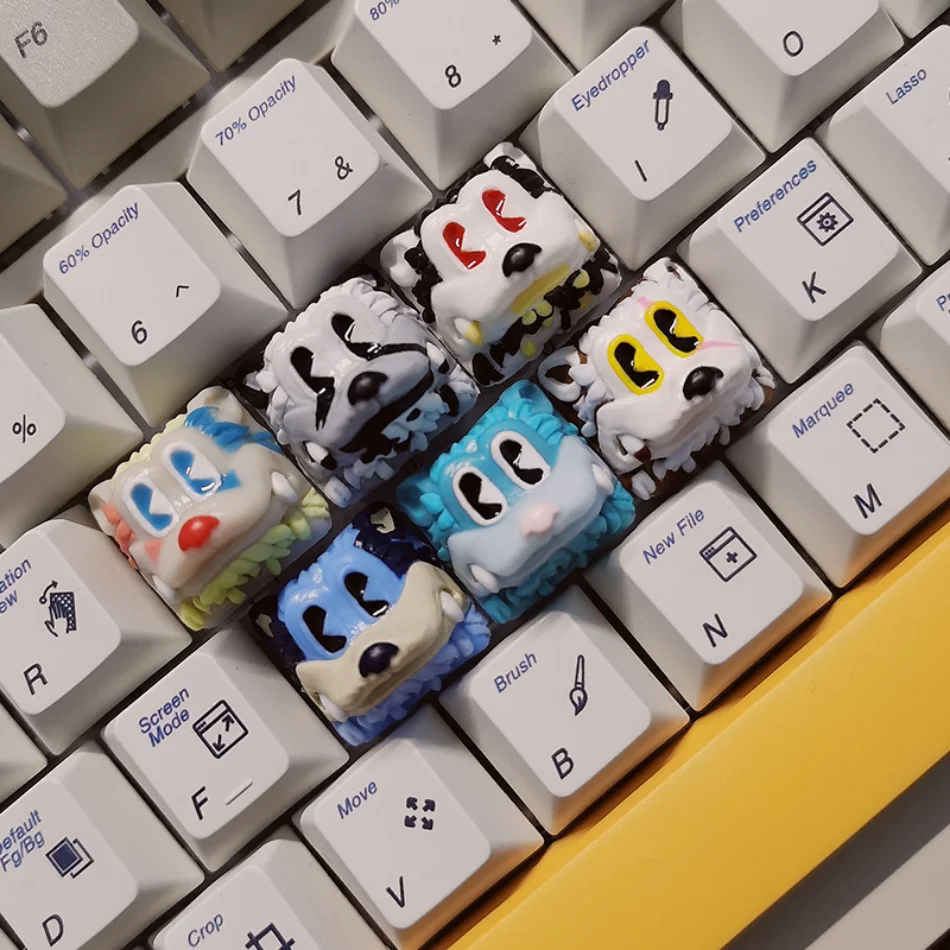
Custom keycap design takes more than picking a cute font and hitting export.
I spent three years messing with PBT double-shot profiles before I figured out why my custom sets looked fine on screen but terrible on my desk. Most people skip the part where actual keycap geometry matters. They download some free designer file, slap it on a 60% board, and wonder why their spacebar looks warped or their modifiers don't align properly. Let me walk you through how this actually works when you want something that looks good and functions correctly. There is a manual process, and once you get it, you can make any cute custom design without paying a premium to someone else.
Cute Custom Keycaps Manual
Start by picking your base profile first. Don't go chasing a character design and then try to fit it later. That is how you end up with a daisy chain of problems. Cherry MX profile, SA, MT3, XDA — these are the standards. Look at the actual cap height, the wall thickness, the bottom curve. I learned this the hard way after spending $80 on a set where the legends were unreadable because the designer hadn't accounted for the key radius. The tool you need is a CAD program. KeyShot is the industry standard for rendering, but for actually designing the files, use something like Rhino or even FreeCAD if you are on a budget. You will model each key individually. This takes time, but it is the only way to get proper legibility across different key sizes. When you are building your cute aesthetic, keep the wall thickness between 1.2 and 1.8 millimeters. Anything thinner and the resin or plastic will fail during production. Anything thicker and you lose the detail you are trying to add. I once had a designer who used 0.8mm walls on a custom Pokémon set. The keys cracked within a week. Do not repeat that mistake.
Setting up your 3D model correctly
Export your models as STL files with the right units. Millimeters. Inches will cause proportion issues that are nearly impossible to fix later. Make sure the stem area is perfectly aligned with the switch mounting point. This is where most people mess up. I have seen multiple designs where the cross shape was offset by two millimeters, making the keycap feel loose or completely unusable with certain mechanical switches. If you are going the resin casting route instead of injection molding, you need to account for shrinkage. Resin shrinks about 0.5 to 2 percent depending on the mix and cure conditions. I scale my designs up by 1.5 percent as a standard practice. It saves me from having to reprint half a keycap set after the first batch comes out smaller than expected. For those doing their own silicone molds, here is a detail nobody talks about: the draft angle. Your vertical walls need at least a 2-degree taper toward the stem side. Without it, the keycap sticks in the mold and you either damage it during removal or waste hours sanding out flash. I wasted three days on a Zelda-themed set because I skipped this step. You do not want that.
Get the Full Details
Design details that make or break the final product
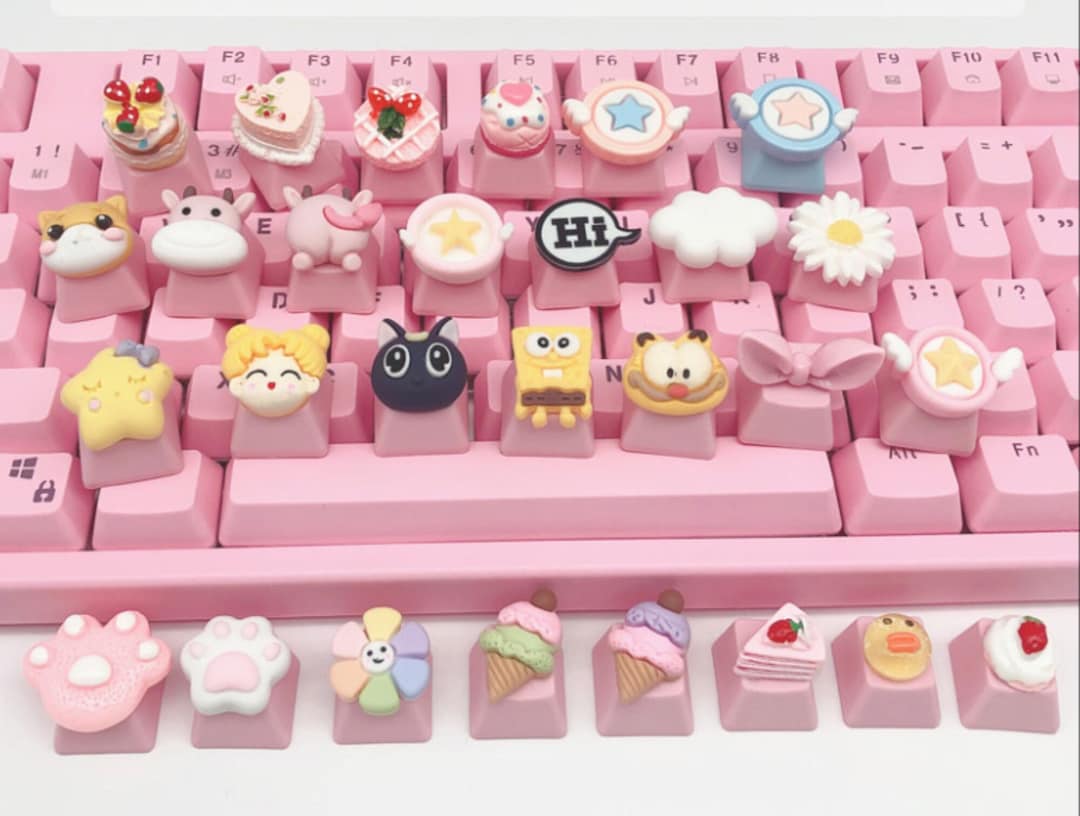
Keep your cute elements raised or recessed by no more than 0.5 millimeters from the main surface. Anything deeper and the resin or plastic flows unevenly. The detail will either fill in completely or create air pockets that become weak spots. I use a simple test method: print a small section of the design at 50 percent scale before committing to a full run. It catches about 80 percent of the potential production issues. Legibility is non-negotiable, even with cute themed keys. If you are putting characters or patterns on modifier keys, make sure there is enough contrast between the design and the background color. I recommend testing your color combinations in grayscale mode. What looks clear in RGB often disappears completely when rendered in your chosen plastic material. Here is a specific problem I ran into recently: designing a full set with rounded character illustrations. The corners of certain keycaps, especially the wider ones like the spacebar and shift keys, had these tiny unrendered gaps. It turned out the curvature of the keycap meant my design file had overlapping geometry that some slicers couldn't handle. The workaround was simpler than expected. I modeled each key separately with its own curvature rather than trying to project a flat design onto curved surfaces. It took about twenty minutes longer per key but eliminated all the rendering errors.
Material selection matters more than you think
PBT plastic is the baseline. It feels better, lasts longer, and handles heat without warping. ABS is cheaper but will shine and deform faster. For cute custom designs, I usually recommend PBT because the texture shows detail better. If you are doing translucent keys for RGB backlighting, you will need to order separate layers or use a dual-color injection process, which costs significantly more. Silicone keys exist as an option for extreme customization, but they have a major downside: they attract dust and lint like nothing else. They also have a distinct rubbery feel that some people love and others find unbearable. My recommendation is to stick with hard plastic unless you have a specific reason to go softer. The production quality is more consistent and they age better.
Working with manufacturers
If you are sending files to a production house, ask for their exact file format requirements upfront. Some prefer STEP files, others want IGES. Sending the wrong format causes conversion errors that introduce tiny geometry flaws. I always include a rendered image alongside the technical files so the production team can reference the intended look while working with the CAD data. Get a physical prototype before approving the full run. Digital renders lie. They show clean lines and perfect colors. A real printed or molded sample reveals warping, color inconsistencies, and fitment issues. I have paid for multiple runs where the prototype would have caught the problem if I had just waited for it before committing to fifty sets. Communication with manufacturers also requires specificity. Telling someone a keycap needs to be "pink" is useless. Use Pantone color codes or provide a physical color reference if possible. Same with texture. "Smooth" means something different to everyone. Specify roughness values if the manufacturer supports that level of detail.
Common failures and how to avoid them
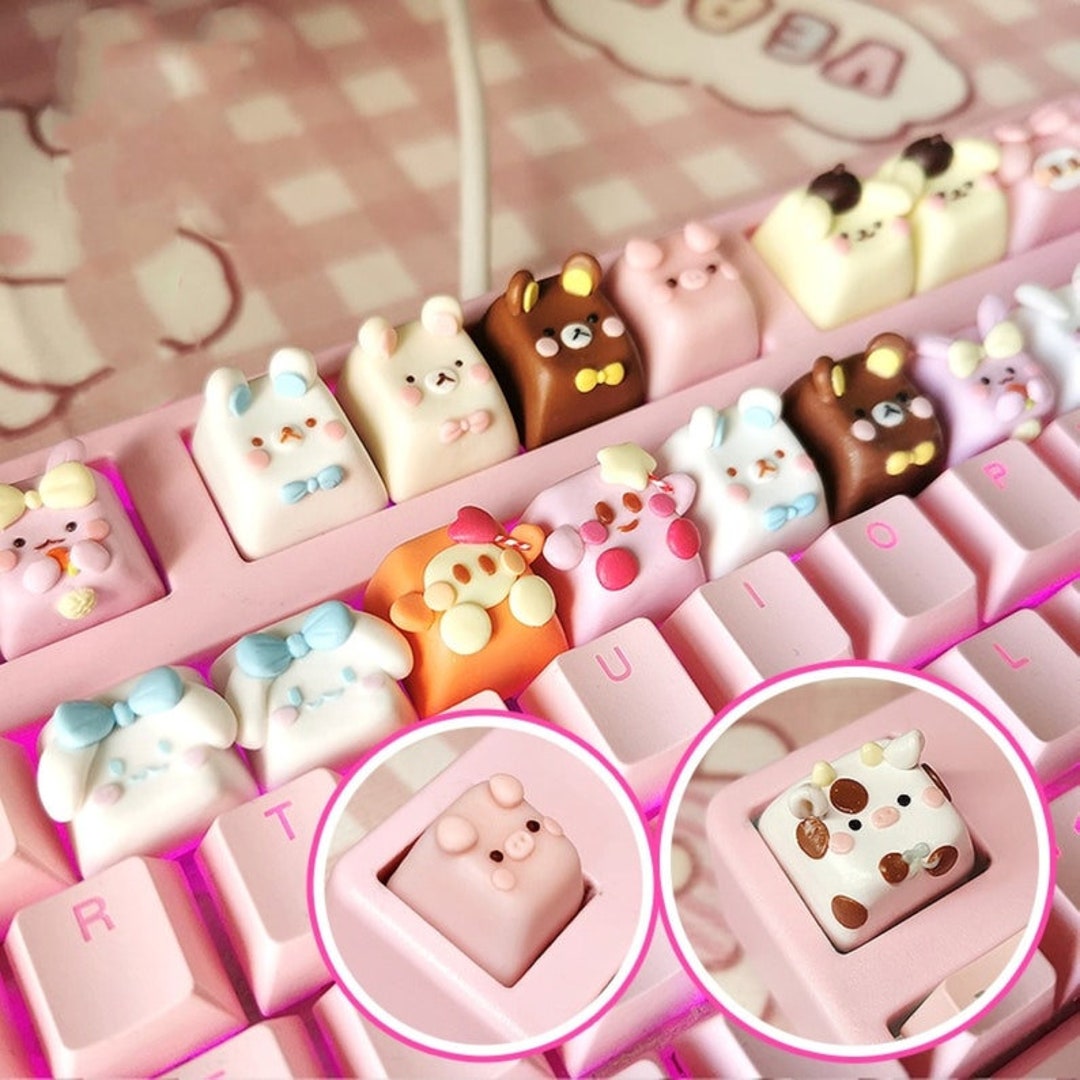
Keycap flex is the most common issue with custom designs. If you are doing intricate patterns or thin walls, the keys will flex under normal typing pressure. This causes uneven wear and eventually cracking. Reinforce your design by adding subtle structural ribs on the underside. They will not be visible during normal use but they add significant rigidity. Stem misalignment happens frequently with non-standard key layouts. If you are designing for a 65 percent or tenkeyless layout, measure your actual keyboard spacing before modeling. Different board makers have slightly different stem positions. A keycap designed for one brand may not seat properly on another even if the switch type is identical. Color bleeding is another production issue. When you use multiple colors in a single keycap, the boundaries between colors can blur if the manufacturing tolerances are loose. High-quality producers keep this to less than 0.1mm of bleed. Cheaper ones may exceed half a millimeter, which destroys the crispness of your cute design. Check reviews and sample galleries before placing an order.
The manual approach to custom keycaps is tedious but it gives you full control over the final product. You learn exactly what works and what does not through trial and error. The alternative is paying someone else to make the same mistakes with your money. Start with one or two keys as a test. See how your design translates from screen to physical object. Adjust based on what you learn. Then scale up from there.