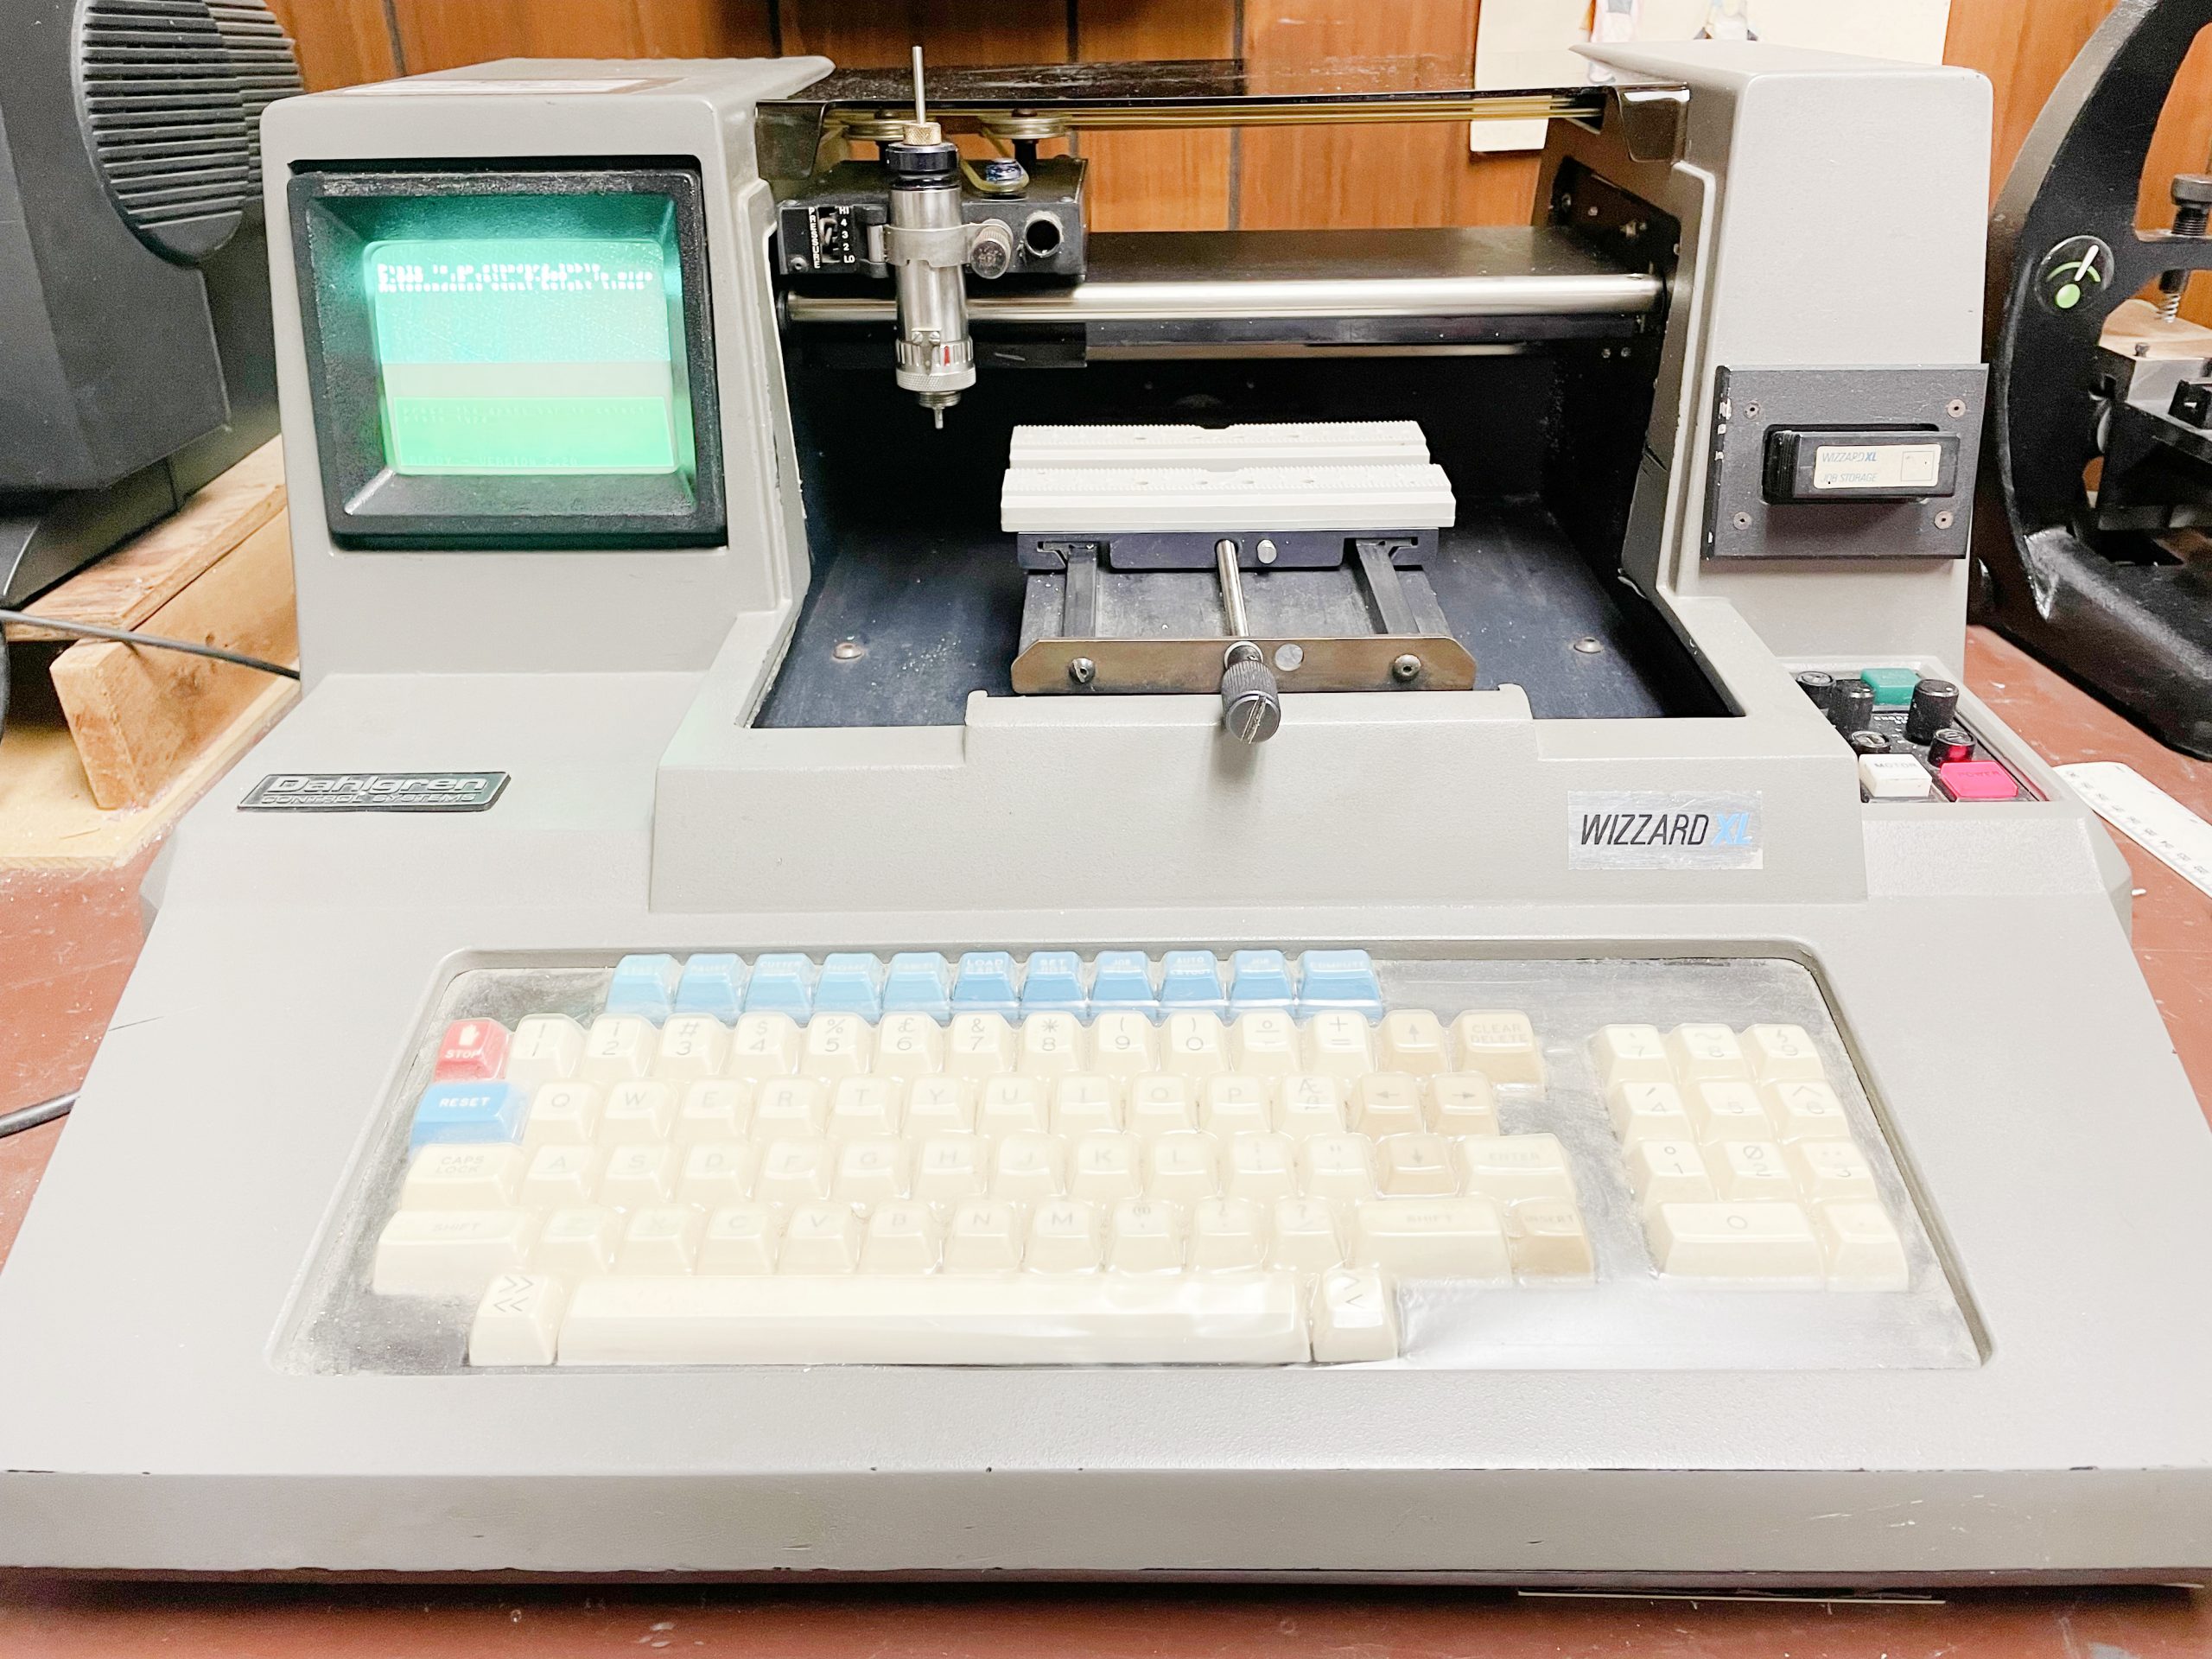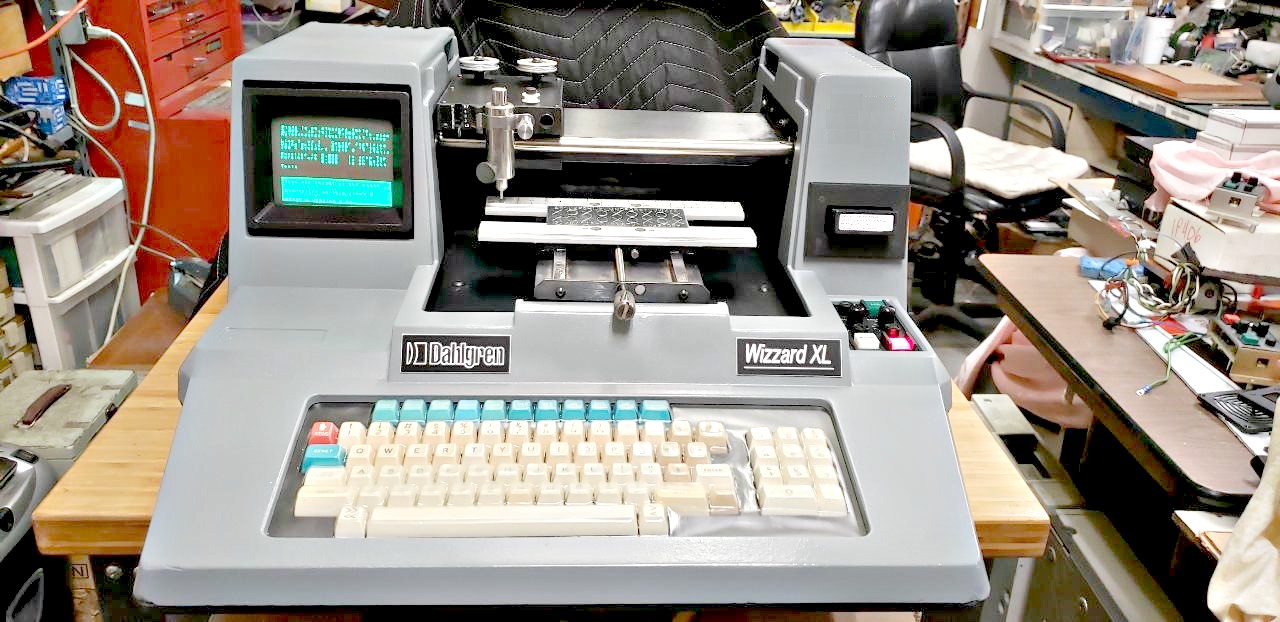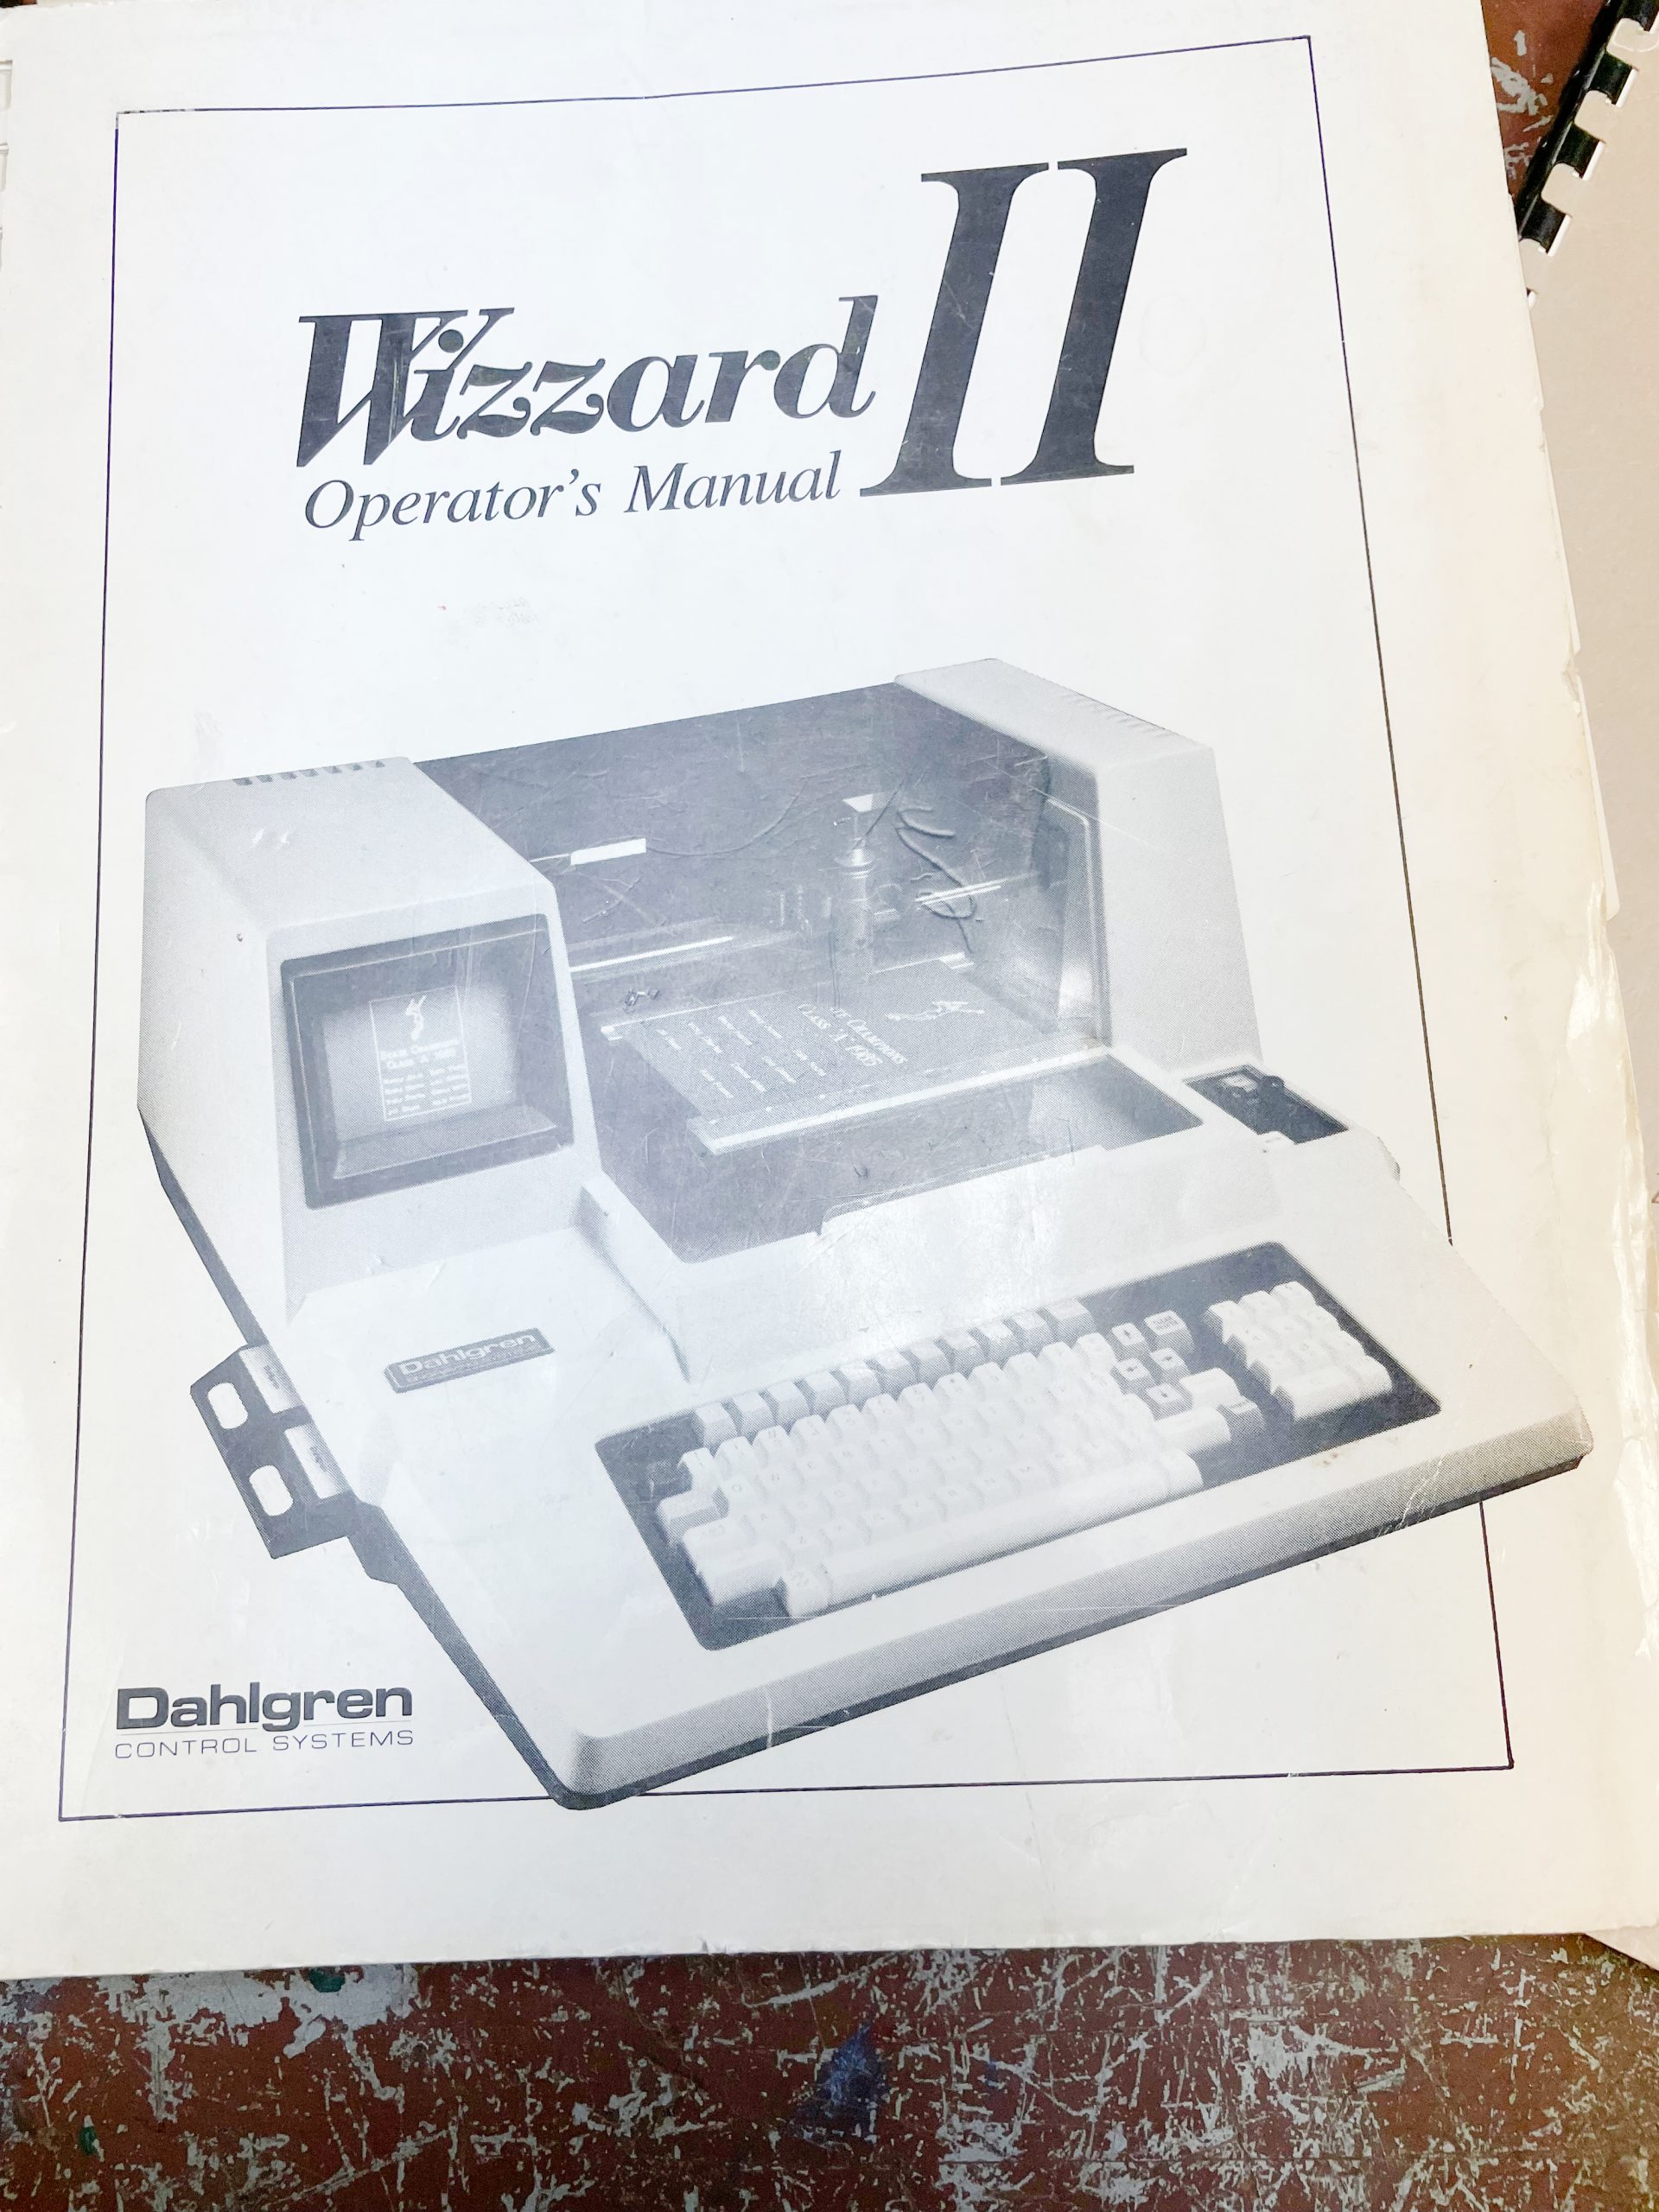
Getting Started With the Dahlgren Wizzard Xl Engraver Manual
The manual is scattered across a few different places on the web now, which is annoying but not uncommon for older industrial equipment. The official Dahlgren documentation server still hosts the main pdf, though the URL structure has changed enough times that a quick search through the Wayback Machine or the Dahlgren support portal usually turns it up. Search for "Dahlgren Wizzard Xl Engraver Manual" and you will find the primary 84-page document that covers the core operations. There is also a separate quick-start leaflet that some users prefer for daily reference, since the full manual buries the basic calibration steps under pages of technical specs you will rarely need after week one. I have run these machines for years, and the first thing I always tell people is that the manual is necessary but not sufficient. It describes the machine as if it will be used in ideal conditions, which is generous. The real knowledge is in the margins and in the things the manual does not warn you about.
Where to Find the Dahlgren Wizzard Xl Engraver Manual
The main manual is available as a pdf from Dahlgren's technical documentation section. If the link is broken, try searching by the serial number format on the machine's data plate. Second-hand listings on auction sites sometimes include a physical copy, which are actually more useful than the digital one because people who owned these machines tended to annotate theirs heavily with adjustments they found over time. I have a paper copy with about forty marginal notes that has saved me more than once. Before you fire up the laser head for the first job, the X and Y axes need to be squared. The manual gives you the procedure, but it assumes you have a reasonable square and a feeler gauge. Use both. What I found after three weeks of running a second-hand unit was that the belt tension on the Y-axis had drifted enough to cause a registration error of about 0.8mm per meter. That does not sound like much until you are engraving fine detail on a batch of thirty items and every piece is slightly off register. The workaround was straightforward. Loosen the idler pulley bolts just enough to take slack out of the belt while the carriage is centered on the axis, then retighten in a cross pattern. Re-check the axis square after. Do this every few months if the machine sees regular use, and definitely after any significant move or vibration event. The manual mentions belt tension but does not explain how to judge when it is right, so finger-pressure testing is your best practical guide. It should deflect about five millimeters under moderate thumb pressure at the midpoint of the span.
Understanding the Control Interface
The control panel is straightforward once you stop treating it like a computer interface. It is a dedicated controller with limited memory and a small character display. The key thing beginners get wrong is assuming they can load large vector files directly into the machine's buffer. They cannot. Files larger than about two megabytes will either fail to transfer or cause the controller to behave unpredictably during longer jobs. Keep your design files as lean as possible. Remove unnecessary nodes from vector paths. Simplify fills where you can. I usually run a pre-flight check on any file before sending it, looking specifically for duplicate lines, stray points, and overly dense hatching patterns that will make the controller choke. This habit alone cut my job failures from roughly one in eight to maybe one in forty. Another counter-intuitive point: the manual recommends starting your raster jobs at lower power and increasing gradually. In practice, I have found the opposite works better for consistency. Start at your target power and adjust speed instead. Changing speed affects how the head moves and how the laser interacts with the material more predictably than tweaking power, which tends to create hot spots and inconsistent depth, especially on materials like acrylic or wood veneer.
Get the Full Details
Material-Specific Settings
The manual includes a material settings table, and it is useful as a starting point. But it was written for a different era of laser tube condition and assist gas setups. A fresh tube and an older one will perform very differently at the same settings, so treat the table as a baseline rather than a rule. For example, the manual lists a certain power and speed combination for engraving stainless steel. That setting will work when the tube is new, but six months into the tube's life you may need to reduce speed by thirty percent or increase passes to get the same mark. Tracking your tube hours and adjusting settings accordingly is more reliable than trying to hit a static setting from a document. A specific edge-case that caught me out: when engraving anodized aluminum, the manual does not mention that the power settings it provides assume a clean, flat anodized surface. If the surface has any scratches or uneven anodization, the laser will follow those variations and produce inconsistent results. The fix is to sand the surface lightly with 400-grit paper before engraving, or to accept that the surface irregularities will show up in the final mark. There is no software workaround for this one.
Maintenance That the Manual Underplays
Filter replacement is the most critical maintenance task, and the manual treats it almost as an afterthought. The air filter on the optical path needs cleaning every two weeks with moderate use, and replacement every three months depending on what you are cutting. Cutting MDF or particle board without frequent filter changes will foul the lens within weeks. I learned this the hard way when a lens coated in sawdust-related residue caused a beam deviation that ruined a batch of pieces before I realized what was happening. Water cooling is another area where the manual is optimistic. The recommended water change interval assumes you are using distilled water and a clean reservoir. Tap water will deposit minerals in the block within a month, reducing cooling efficiency and putting stress on the laser tube over time. Use distilled water. Check the water level weekly. If the temperature probe reads more than four degrees above ambient, something is wrong and the machine should not be run until you find it.
Limitations and When to Walk Away
The Wizard XL is a solid machine for general-purpose engraving and light cutting work, but it has real limitations that the marketing materials do not emphasize. The working area is generous, but the Z-axis clearance is tight if you are working with thicker materials. Anything over about seventy millimeters in height and you will struggle to get the lens focused properly, especially toward the edges of the bed. The manual mentions this in the specifications section but does not make it clear how constraining it is for practical work. The laser tube life is another factor. At twenty thousand hours, which is the rated lifespan, output degrades significantly. You will notice it as a gradual need to slow down jobs or accept shallower engraves. Replacing the tube is not cheap, and compatibility with older control systems can be finicky. If your tube is already near the end of its life and you are doing production work, a machine upgrade may make more financial sense than managing an aging unit. Finally, the software ecosystem around this machine is limited. The native software is functional but dated, and third-party integration is not straightforward. If you need to tie the engraver into a workflow that involves automated job scheduling or remote monitoring, you will be building that yourself. There is no plug-and-play solution here.
If you are buying one second-hand, check the tube hours logged in the service menu, inspect the lens for coating damage, and run a test job on material you know well before committing. The manual will tell you what the machine should do. It will not tell you what to look for when it is starting to go sideways.