How to Actually Prepare for Quality Engineer Interviews
Most people treat quality engineer interview prep like a memorization task. They pull together flashcards for Six Sigma belt definitions and practice reciting the PDCA cycle. That approach works in academic settings and it fails completely in technical interviews. The difference is that interviewers are trying to see how you think when you don't know the answer, not whether you memorized a textbook chapter. I spent years sitting on both sides of these tables. Early in my career I ran into a candidate who could quote the entire ANSI/ASQ QIR standard from memory but couldn't tell me what he would do if his first audit revealed that half the measurement systems in a production line had Gage R&R values above 30 percent. He froze. The real question wasn't about the standard. It was about whether he understood what the numbers actually meant on the floor.
Common Quality Engineer Interview Questions and How to Approach Them
Here are the questions that actually come up, grouped by what they're really testing. I've included the specific angle interviewers are usually looking for and a brief note on how experienced candidates handle the harder versions. Statistical and measurement questions: You will get asked about control charts, process capability, and measurement systems analysis. Not just definitions. You'll be given a scenario where a Cp of 1.67 looks great but the process is drifting out of specification, and you need to explain the gap between potential and actual capability. Or they'll show you a Gage R&R result and ask whether the instrument is the problem or the operator variation. I've seen people correctly identify a Type 1 study failure but miss that the sample set didn't represent the full process tolerance band, which made the whole assessment meaningless. The trick is to ask about the sampling plan before answering about the pass/fail result. Root cause and corrective action questions: Expect a case study where something failed in production and you have to walk through your investigation. Five Whys comes up constantly. Ishikawa diagrams too. The trap here is stopping at a human error conclusion. If your root cause ends with "the operator made a mistake," the interviewer will push back because human error is never a root cause. It's a symptom. The actual root cause is usually a missing mistake-proofing feature, ambiguous work instructions, or inadequate training verification. I once handled a situation where a recurring assembly defect kept getting attributed to operator negligence. We ended up discovering that two different torque specs were being used on the same workstation because the previous engineer had updated the product without updating the work instruction revision. The fix wasn't retraining. It was a revision lockout procedure on the document management system.
Systems and audit questions: You need to demonstrate familiarity with ISO 9001, IATF 16949, AS9100, or 21 CFR Part 820 depending on the industry. But the deeper question is always about audit methodology. How do you decide what to audit? How do you handle a nonconformance that the auditee disagrees with? What's your approach to follow-up? A strong answer describes a risk-based auditing strategy rather than a rote checklist approach. I've interviewed people who couldn't explain the difference between a major and minor nonconformance in a way that showed they'd actually done the work. Quality tool proficiency: FMEA, SPC, MSA, PPAP, CAPA, 8D — these are the standard toolkit. The interview will probe whether you understand when to use each tool and when not to. A common mistake is recommending a full FMEA for every small change request. That's not how it works in practice. You scope the FMEA to the risk level. I worked on a line where someone had tried to apply a comprehensive AIAG FMEA to a minor fixture modification that touched zero failure modes. It took three weeks to complete and identified nothing useful. A quick risk assessment and a controlled trial run would have solved the problem in two days. Behavioral and situational questions: These matter more than most candidates realize. Tell me about a time you had to enforce a quality standard that slowed down production. Tell me about a disagreement with engineering over a release decision. The structure they want is specific: describe the context, what you did, what the outcome was, and what you'd do differently now. Vague answers get filtered out. I've sat through interviews where candidates gave five-minute responses that contained zero concrete details about their actual role in the situation.
Get the Full Details

Where Most Candidates Go Wrong
The biggest mistake is treating quality engineering as purely a documentation exercise. The second biggest is confusing testing with quality engineering. Testing catches defects. Quality engineering builds the systems that prevent defects from reaching the test stage in the first place. If your answers focus only on inspection and sampling plans, you're describing a quality inspector role, not a quality engineer role. Another issue is over-reliance on methodology without understanding the underlying statistics. You can know every step of a hypothesis test but still apply it wrong if you don't check assumptions like normality or equal variance first. I had a colleague who once recommended a full ANOVA to compare three suppliers on a dimension that was clearly non-normal and had highly unequal variances. The analysis was technically correct based on the inputs but the conclusions were garbage. The right move was a non-parametric test or a data transformation first. Some companies also ask about cost of quality calculations. Don't brush these off. They want to know you can translate quality problems into financial terms. Prevention cost, appraisal cost, internal failure cost, external failure cost. If you can't explain the difference between prevention and appraisal, you won't pass the screening round at any serious organization.
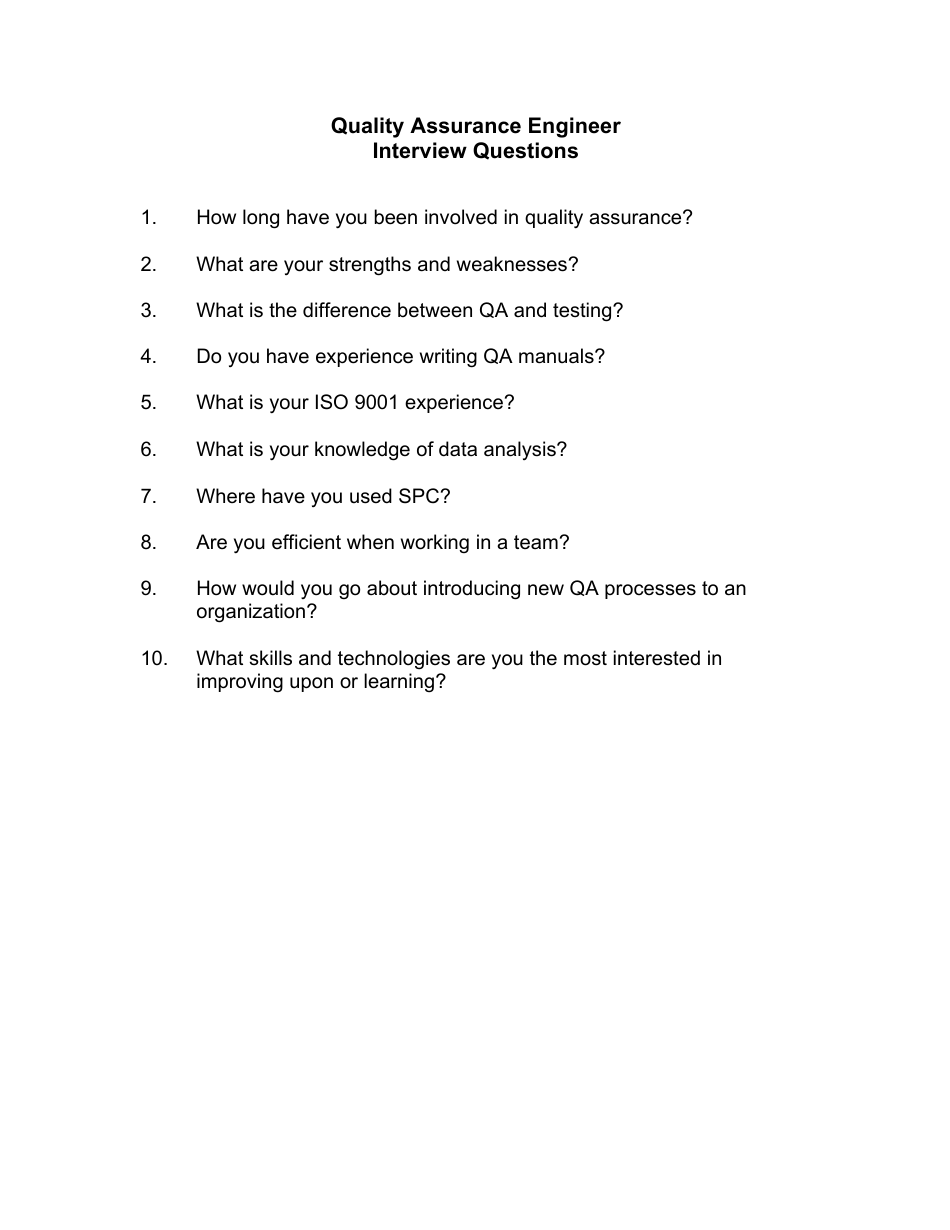
If you want a more structured set of practice questions to work through before an interview, there are curated collections available online that cover the standard domains. Look for ones that include scenario-based questions rather than just definition dumps.
What I Wish I'd Known Before My First Few
You will get questions about tools you haven't used directly. That's intentional. They want to see how you handle uncertainty. The honest answer is better than a fabricated one. Say you haven't used that particular software but explain the concept behind it and how you'd approach learning it. I once was asked about Minitab specifically and I admitted I mostly used JMP. The interviewer moved on quickly. She cared about whether I understood the statistical concepts, not the interface. Also, bring examples. Not resume bullet points. Actual examples. A process improvement you led. A CAPA you wrote that got accepted. A measurement system study you designed. If you can describe one project in enough detail to answer follow-up questions about why you made each decision, you've already passed half the interview. One thing no one tells you: the hardest questions come from the people who will actually be your peers, not the hiring manager. Panel interviews often include a mix of quality, manufacturing, and engineering leads. Each group tests a different dimension. Manufacturing wants to know you won't be impractical. Engineering wants to know you understand design constraints. Quality wants to know you won't cut corners. Prepare for all three angles.