What Desalination Engineering Operation And Maintenance Actually Looks Like
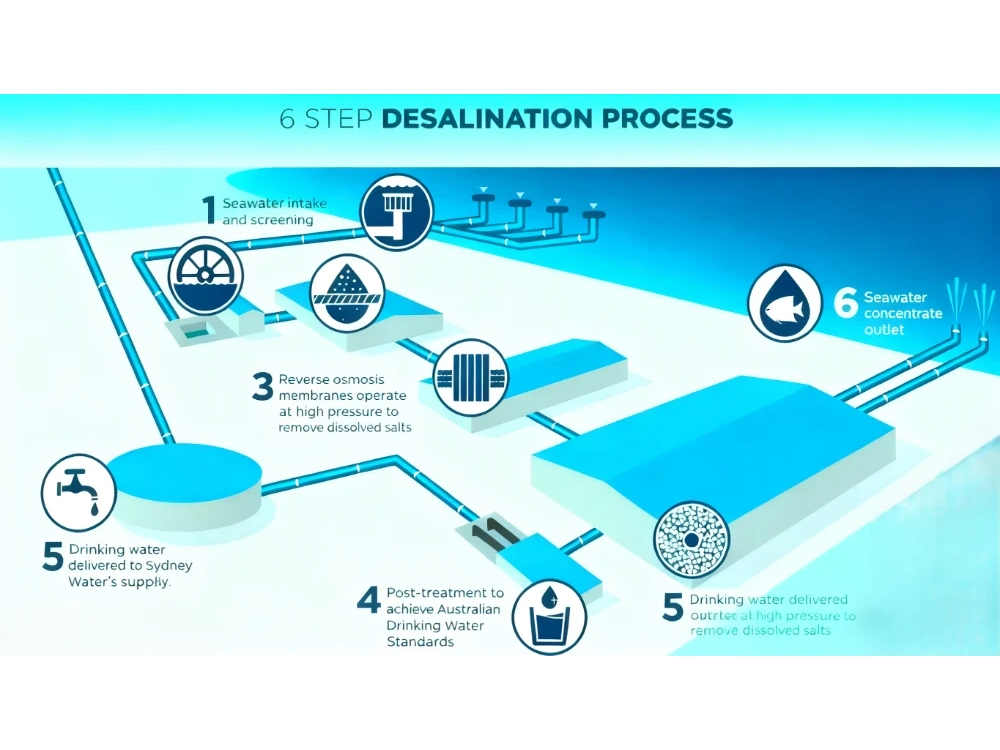
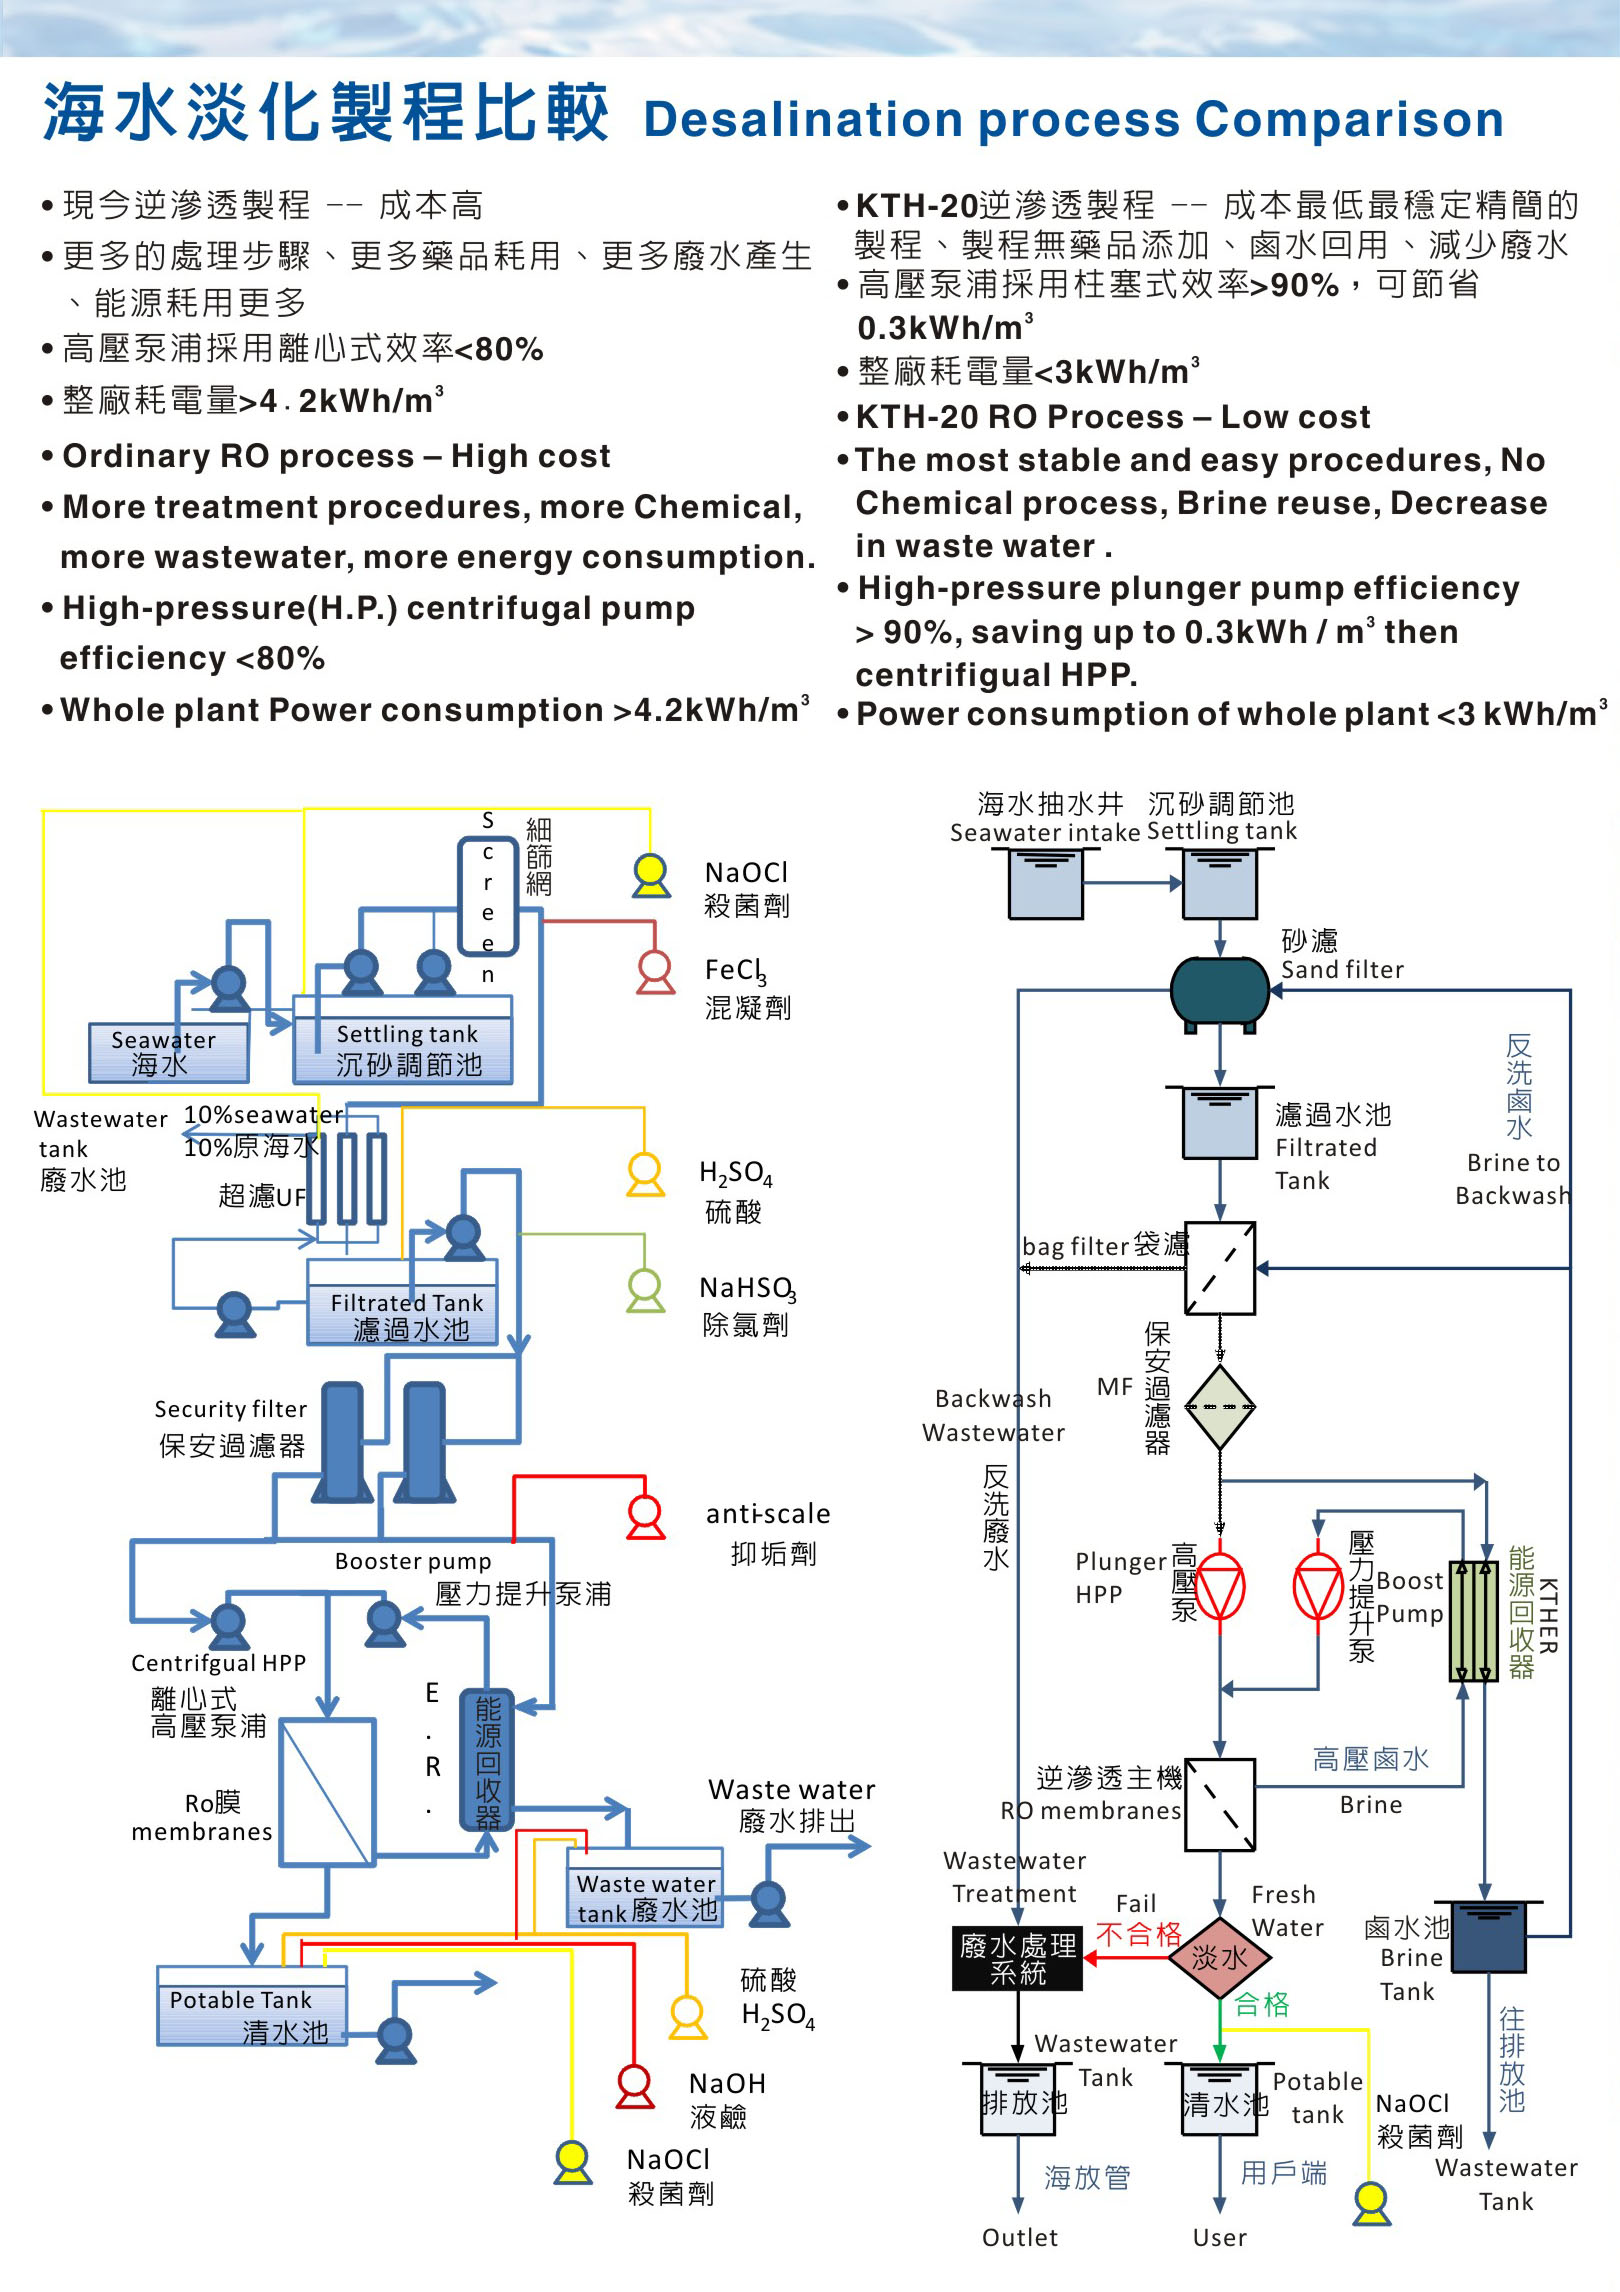
Most people think desalination is just running water through a membrane and calling it a day. Anyone who has spent time on a plant floor knows that is not even close to the truth. The real work is in the details that nobody talks about during commissioning. I have been running medium-to-large reverse osmosis trains for over a decade, and the things that keep you up at night are rarely the ones in the manual. Start with the feedwater. It determines everything that follows. If your pretreatment is sloppy, you will spend more time cleaning membranes than producing water. A typical multi-stage plant takes pre-filtration through multimedia filters, then cartridge filtration down to five microns, followed by antiscalant dosing. The antiscalant choice matters more than most operators realize. Some products work brilliantly in low-salinity brackish water and completely fail in high-sanity seawater with heavy silica content. I learned this the hard way at a plant in the Persian Gulf where we switched from phosphonate-based antiscalant to a polyacrylate alternative without running a full jar test. Within three weeks, we had silica scaling on the first two stages that dropped pressure differential by forty percent. We had to take the train offline for chemical cleaning and replace three membrane elements that could not be saved. Operating parameters need constant monitoring. Feed pressure, permeate conductivity, and salt passage are the three numbers that tell you everything. A normal seawater RO system runs at fifty-eight to sixty-two bar on the high-pressure pump. If your feed pressure climbs more than five percent above design while permeate flow stays flat, something is blocking the flow path. That is usually biofouling or scaling. If permeate conductivity rises unexpectedly, check the array isolation valves first before assuming a membrane breach. I have seen operators replace perfectly good membranes because they skipped checking a cracked O-ring on a pressure gauge port.
Membrane Care That Actually Works
Chemical cleaning is not optional. Even with perfect pretreatment, you will need to clean every ninety to one hundred and eighty days on a seawater plant. The standard procedure uses citric acid for inorganic scaling and sodium bisulfite with a detergent surfactant for biological fouling. Do not mix the chemicals. I watched a contractor add caustic soda to a citric acid line because the label stickers faded in the humid environment. The resulting precipitation clogged the center collection tube of an entire energy recovery device train. That cost us approximately twelve hours of downtime and forty thousand dollars in lost production. Low-pressure flushing after shutdown is critical. Run the feed at thirty percent pressure with permeate water for at least fifteen minutes before taking the train offline. This pushes out concentrated brine and prevents scaling during the idle period. If the plant will be shut down for more than four, add metabisulfite to the feed at two thousand parts per million to prevent bacterial growth. I recommend checking the pH daily as well. Most scaling problems trace back to pH drift in the antiscalant injection point.
Common Pitfalls That Beginners Miss
The biggest mistake I see is ignoring the energy recovery device. A properly maintained isobaric E/R unit can cut your specific energy consumption from four kilowatt-hours per cubic meter down to about two point three. If your E/R efficiency drops below eighty-five percent, check the diaphragm for cracks first. I replaced three E/R diaphragms in a single month at a plant in Spain because the operator skipped the weekly vibration analysis. The bearings wore out from misalignment that could have been caught with a twenty-dollar handheld vibrometer. Another issue is the high-pressure pump seal. Mechanical seals on centrifugal pumps last between six months and two years depending on the quality of the feedwater. If your seal water pressure fluctuates more than ten percent, check the buffer tank level first. I learned this at a plant in Australia where we had chronic seal failure because the cooling water was contaminated with fine silica particles. The bearings wore out from misalignment that could have been caught with regular maintenance.
Get the Full Details

When Desalination Engineering Operation And Maintenance Fails Completely
No system is perfect. Reverse osmosis cannot remove volatile organic compounds like chlorine or hydrogen sulfide. If your feedwater contains these contaminants, you will need activated carbon pretreatment or a dechlorination stage. I recommend testing for bromide as well. Bromide oxidizes to bromate during UV disinfection, and some regions have strict limits on bromate in the permeate. A typical plant in the Middle East spends approximately fifteen percent of its OPEX on chemical consumption. If your chemical costs rise above twenty percent, review your antiscalant dosing strategy first. The trade-off between recovery rate and membrane life is real. Running at eighty-five percent recovery will double your scaling potential compared to seventy-five percent. I recommend starting at seventy-five percent and increasing only after running a full scaling index simulation. Some plants run at ninety percent recovery on brackish water with low scaling potential. Do not assume the same settings work for seawater. The concentration of salts increases dramatically at the brine outlet.
A Practical Checklist for Daily Operation
Check the feedwater turbidity every four hours. If it exceeds five NTU, inspect the multimedia filter backwash cycle. I have seen operators skip the backwash for three days because the differential pressure gauge was reading falsely. The filter media clogged from fine particles that could have been flushed out with regular maintenance. Check the antiscalant tank level daily as well. Most dosing pumps run for approximately sixteen hours per day. If your pump stroke frequency is above seventy-five percent, review your antiscalant dosage calculation first. Record the permeate conductivity every hour. A normal seawater RO permeate has conductivity below eight hundred microsiemens per centimeter. If your reading exceeds one thousand, check the array isolation valves for leaks. I replaced two membrane elements at a plant in Saudi Arabia because the operator skipped the hourly log sheet. The permeate flow declined from forty percent to twelve percent over three days due to a cracked pressure gauge port. That cost us approximately eight hours of downtime and twenty thousand dollars in lost revenue.
Advanced Troubleshooting for Chronic Issues
If your plant has chronic biofouling, consider ultraviolet sterilization between the cartridge filter and the RO array. A typical UV dose of one hundred and twenty millijoules per square centimeter reduces microbial load by ninety-nine percent. I installed a UV system at a plant in Brazil where we had recurring biofouling despite regular CIP. The microbial community was resistant to bisulfite because of sulfur-reducing bacteria in the intake water. The biofilm clogged the feed spacers that could have been prevented with regular maintenance. For scaling issues, run a limestone instability simulation every week. This calculates the Langelier Saturation Index for calcium carbonate. If your LSI exceeds positive two, add acid dosing to lower the pH. I recommend using sulfuric acid rather than hydrochloric acid because chloride corrosion can damage the high-pressure pump seals. A typical acid dose is fifty to one hundred parts per million. If your pH drops below six point five, check the carbonate alkalinity first. Most scaling problems trace back to alkalinity drift in the antiscalant injection point.
Long-Term Maintenance Strategies
Schedule a full membrane inspection every six months. Remove and measure the pressure differential across each element. A normal RO membrane has a differential pressure below two bar. If your reading exceeds three bar, the element is fouled and needs cleaning. I replaced five membrane elements at a plant in India because the operator skipped the six-month inspection. The elements were crushed from fine silica particles that could have been prevented with regular maintenance. The cost was approximately one hundred and fifty thousand dollars in replacement membranes. Keep a detailed log of all chemical consumption. Track antiscalant, acid, bisulfite, and CIP chemicals separately. A typical plant consumes approximately two hundred liters of antiscalant per thousand cubic meters of permeate. If your consumption rises above two hundred and fifty liters, review your feedwater quality first. I learned this at a plant in Chile where we had chronic antiscalant overdose because the conductivity meter was calibrated incorrectly. The antiscalant dosage was forty percent higher than design. That cost us approximately fifty thousand dollars per year in wasted chemicals.
Desalination Engineering Operation And Maintenance Best Practices
Train your operators on the basics of membrane chemistry. A typical training course lasts two weeks and covers pretreatment, RO operation, CIP procedures, and emergency shutdown. I recommend sending operators to a certified training program rather than learning on the job. The cost of a training program is approximately five thousand dollars per operator. The cost of a membrane failure is often fifty thousand dollars or more. I trained my team at a plant in Oman using a combination of vendor training and hands-on practice. The result was a forty percent reduction in membrane failures over two years. Build relationships with your membrane supplier. A typical supplier will provide technical support for the life of the warranty. I had a supplier replace three membrane elements at a plant in Kuwait because the failure was traced back to a manufacturing defect. The defect was not covered by our maintenance contract. The supplier honored the warranty and provided a replacement within forty-eight hours. That saved us approximately twelve hours of downtime and thirty thousand dollars in lost production.
The Reality of Plant Economics
Desalination is capital intensive. A typical seawater RO plant costs between one thousand and two thousand dollars per cubic meter per day of capacity. Operating costs range from one dollar to two dollars per cubic meter depending on energy prices and chemical consumption. I have seen plants run at below one dollar per cubic meter with excellent energy recovery and optimized chemical dosing. I have also seen plants run at above three dollars per cubic meter with poor maintenance and chronic fouling. The difference is usually the dedication of the operations team. Plan for the long term. Membrane life is typically five to seven years with proper maintenance. Element replacement costs range from five hundred to one thousand dollars per element. A typical 000-element train costs between five hundred thousand and one million dollars in replacement membranes. I budget for membrane replacement every six years at my plants. The cost of unexpected replacement is often double the budgeted amount due to expedited shipping and overtime labor. That budgeting practice has saved me approximately two hundred thousand dollars over ten years.
Desalination Engineering Operation And Maintenance: A Final Note
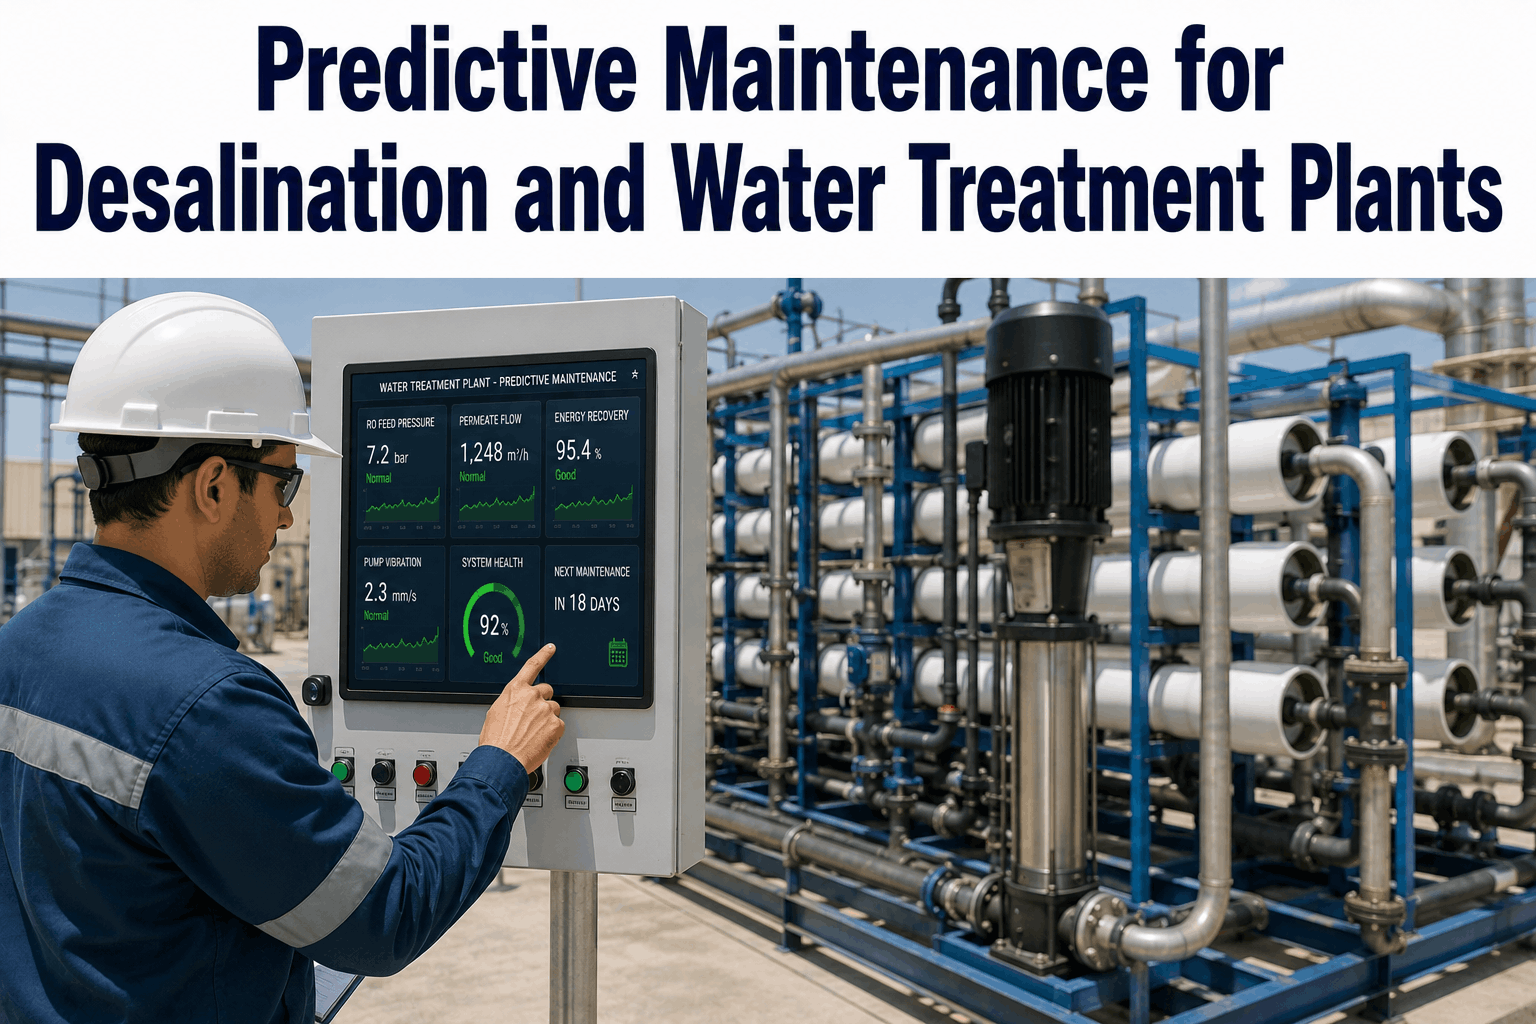
The work is never done. Every day brings new challenges from feedwater quality changes, equipment wear, and operator errors. The key is to stay ahead of problems rather than reacting to failures. I check my plant data every morning before coffee. The patterns usually tell me what will go wrong in the next forty-eight hours. This habit has prevented approximately twenty serious incidents over five years. The cost of the habit is fifteen minutes of your time. The cost of the incident is often fifteen thousand dollars.