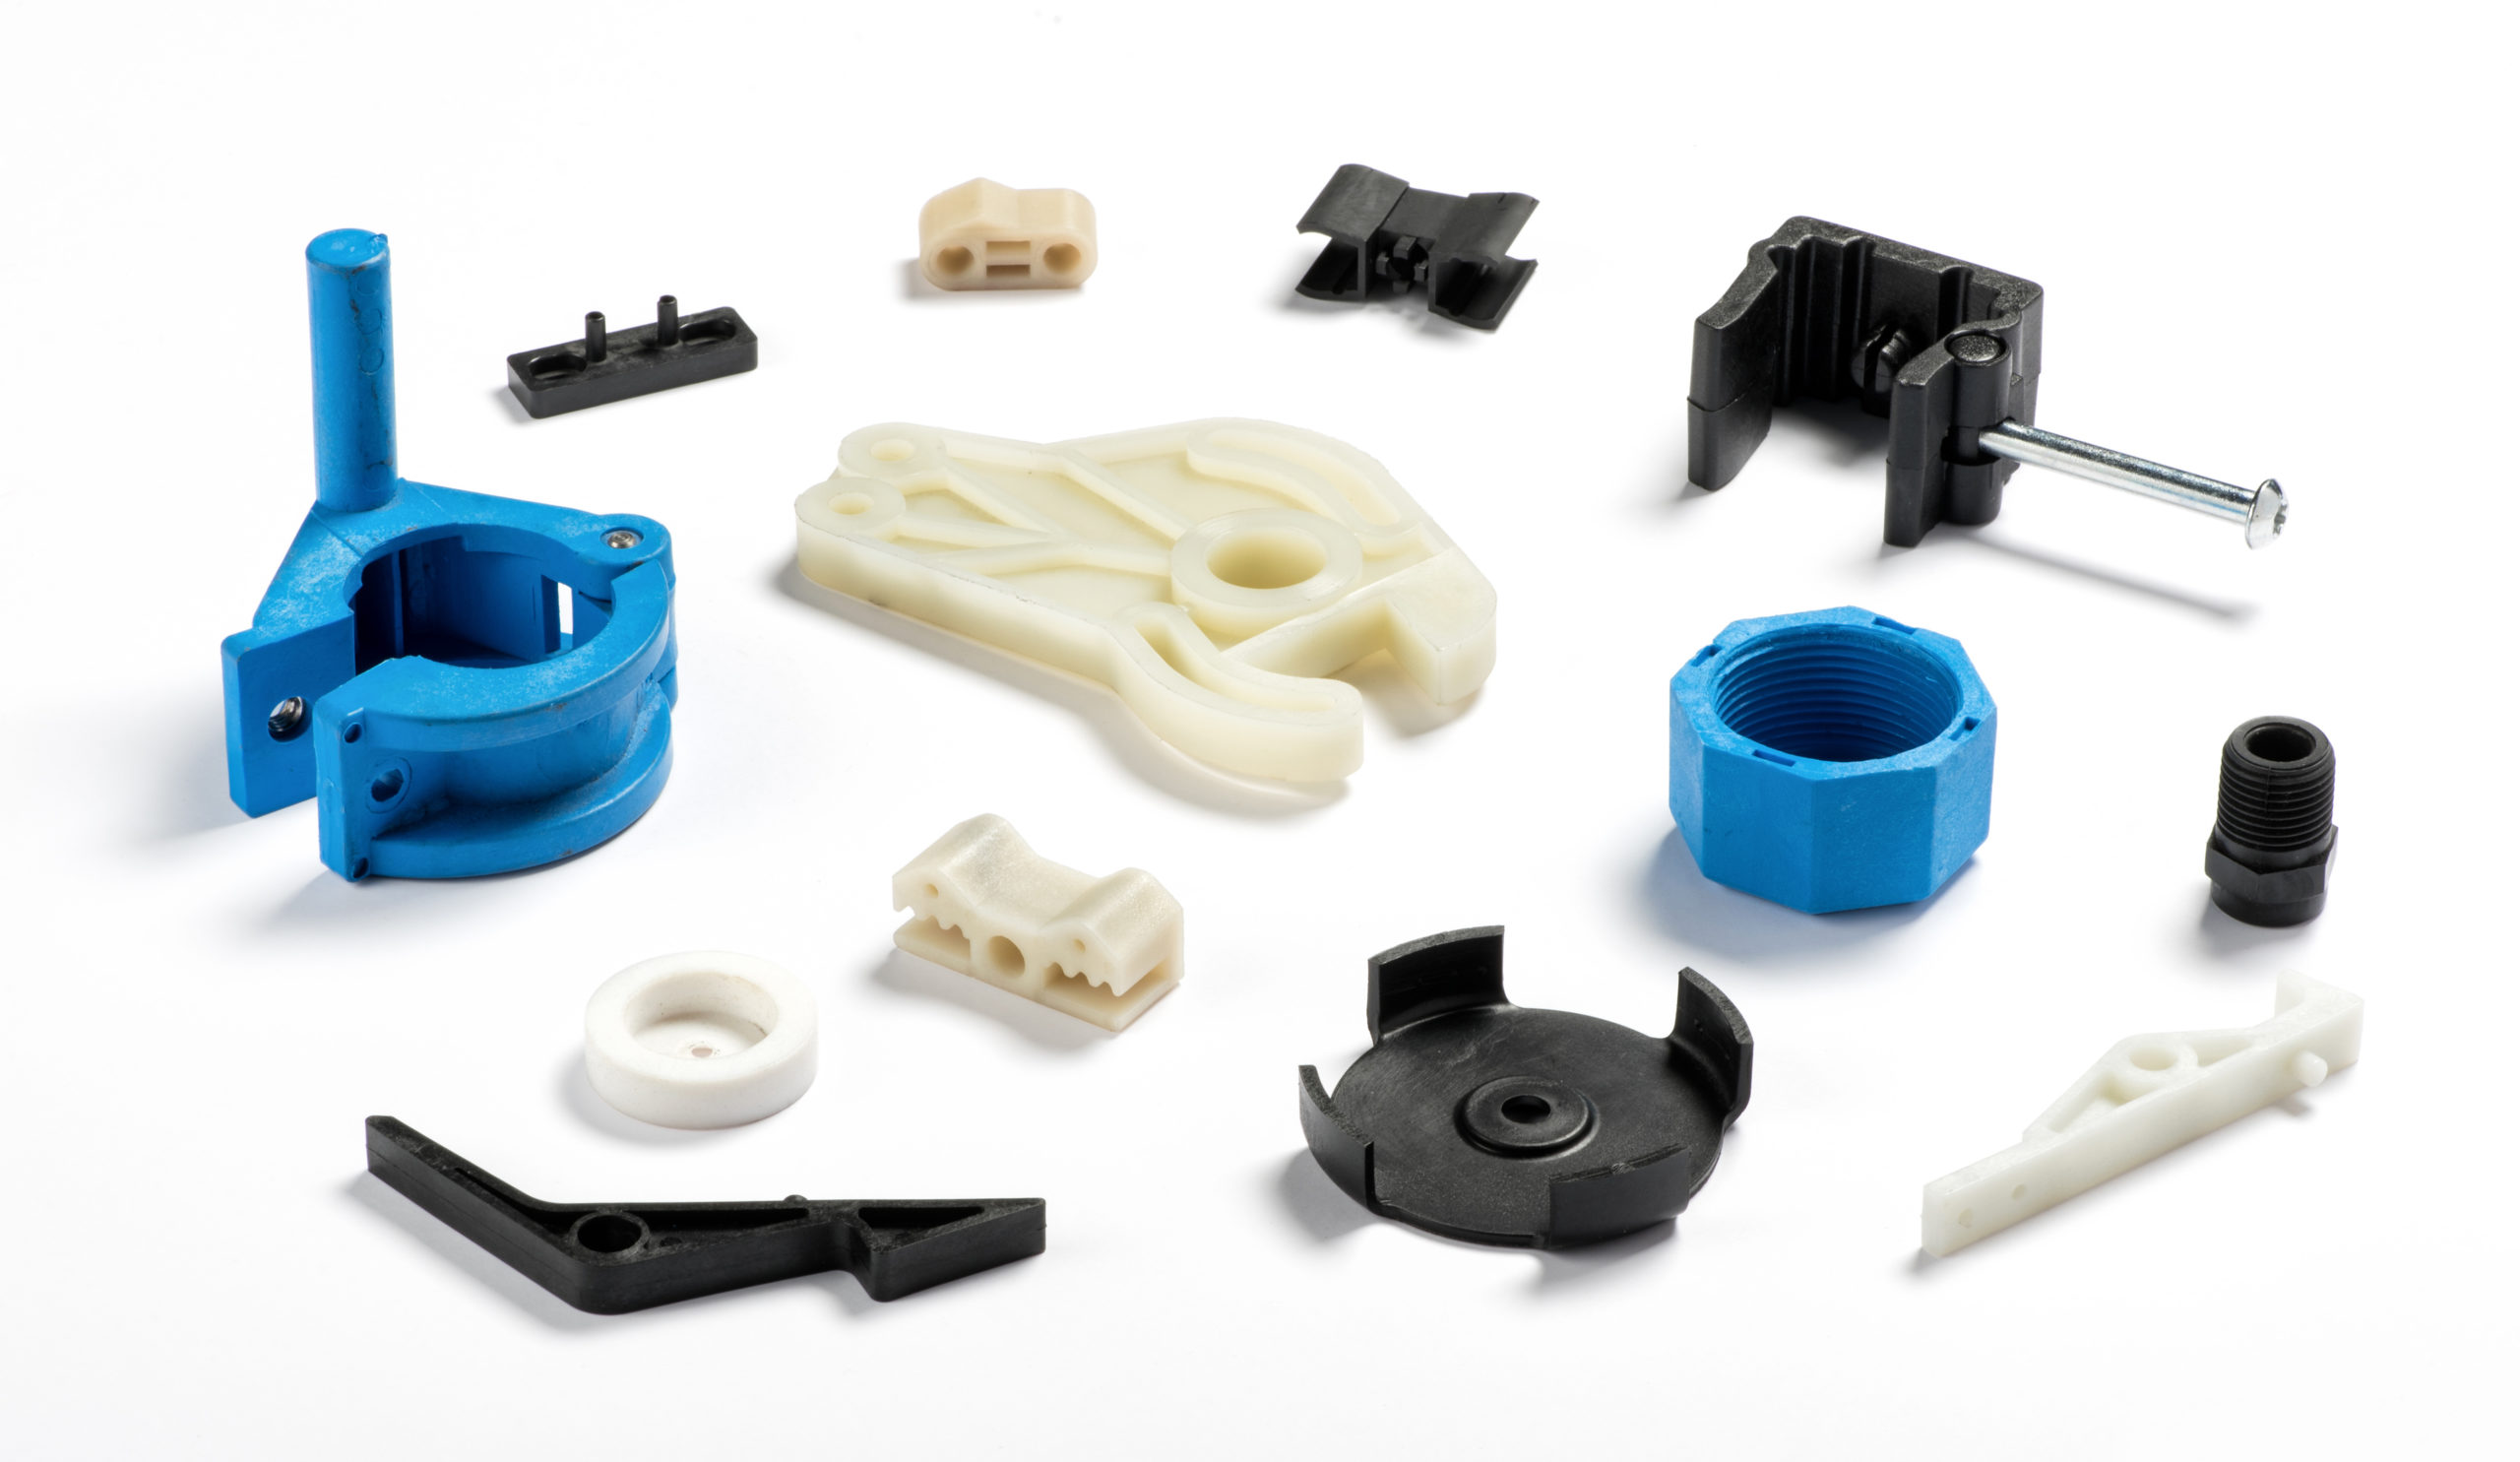
Snaps, Bosses, and the Things That Go Wrong
I spent three weeks last year debugging a two-part enclosure that refused to close past the halfway point. Both halves measured within tolerance. The CAD looked clean. The snaps kept popping back out. The culprit was a 0.003-inch undercut I'd specified on a PA66-GF30 part, paired with an ejection angle that made the snap arm deflect just enough to bind against the opposing wall before it seated. It only took me about eight prototype iterations and a dial indicator to prove it. Most people design snaps once and hope for the best. It rarely works. Assembly-friendly plastic design is mostly about managing forces during mating and release while accounting for the material behaving like plastic under load. You pick your joining method first. Snap-fits, press fits, thermal staking, ultrasonic welding, screw posts, or adhesives. Each one has a completely different set of constraints on wall thickness, draft, and surface finish. Mixing methods in a single enclosure is common, but it compounds the risk of warpage-induced misalignment later. A cantilever snap works because the arm deflects during insertion and springs back to lock behind a shoulder. The math is straightforward if you respect the limits. Deflection stress should stay below the yield strength of the material in use, usually with a safety factor around 1.5 for cyclic loading. For nylon 6/6, that often means keeping deflection strain under about 2 percent unless you are designing for a single-use assembly where the snap never gets taken apart. Acetal handles more strain, somewhere near 3 to 4 percent safely, which is why it shows up in latches that get opened and closed repeatedly. Polycarbonate and ABS are fine for one-time snaps, but they creep and relax over time, which means your retention force drops.
The beam length matters as much as the undercut. A short stubby snap needs aggressive deflection and will either fail on insertion or strip the housing shoulder. A longer beam lets you use a smaller undercut for the same retention. The undercut itself is usually between 0.5 and 1.5 millimeters for typical consumer enclosures. Go below 0.5 and the part feels loose. Go above 1.5 and insertion force spikes, especially with stiff materials. I use roughly 0.75 mm as my default for polycarbonate and 1.0 mm for acetal, then validate with a quick FEA run before committing to tooling. Lead-in angle is where most people get it wrong. A 30-degree lead angle gives smooth engagement but weak retention. A 60-degree angle locks well but requires serious insertion force. The sweet spot for manual assembly is usually around 45 degrees. If you need a tool-assisted press fit, you can push higher. Don't try to use a snap-fit for structural load-bearing. It is a positioning and light retention feature, not a way to replace screws in a bracket application.
Press Fits and Interference Joints
Interference fits are deceptively simple on paper. You specify a shaft diameter larger than the hole, press it in, and hope it stays. In practice, the interference value depends entirely on material, temperature at assembly, and how long you need the joint to hold. A 0.1 mm interference on a 10 mm boss in acetal at room temperature might hold for years. The same interference on a 10 mm boss in polypropylene might relax to near-zero retention within a month because polypropylene creeps under constant strain. If you are designing press fits for long-term assembly, stick with acetal or glass-filled nylons. If you need a removable press fit, you should add a slight taper, usually 0.5 degrees per side, so the part can be pried out without damaging the boss. One thing beginners miss is that press-fit bosses on thin walls will split if you push too hard. A boss on a 1.5 mm wall in polycarbonate can survive a small interference, but the same boss in a 0.8 mm wall will crack during insertion almost every time. The workaround is to thicken the wall locally around the boss or switch to a snap-fit design instead of fighting the material.
Get the Full Details
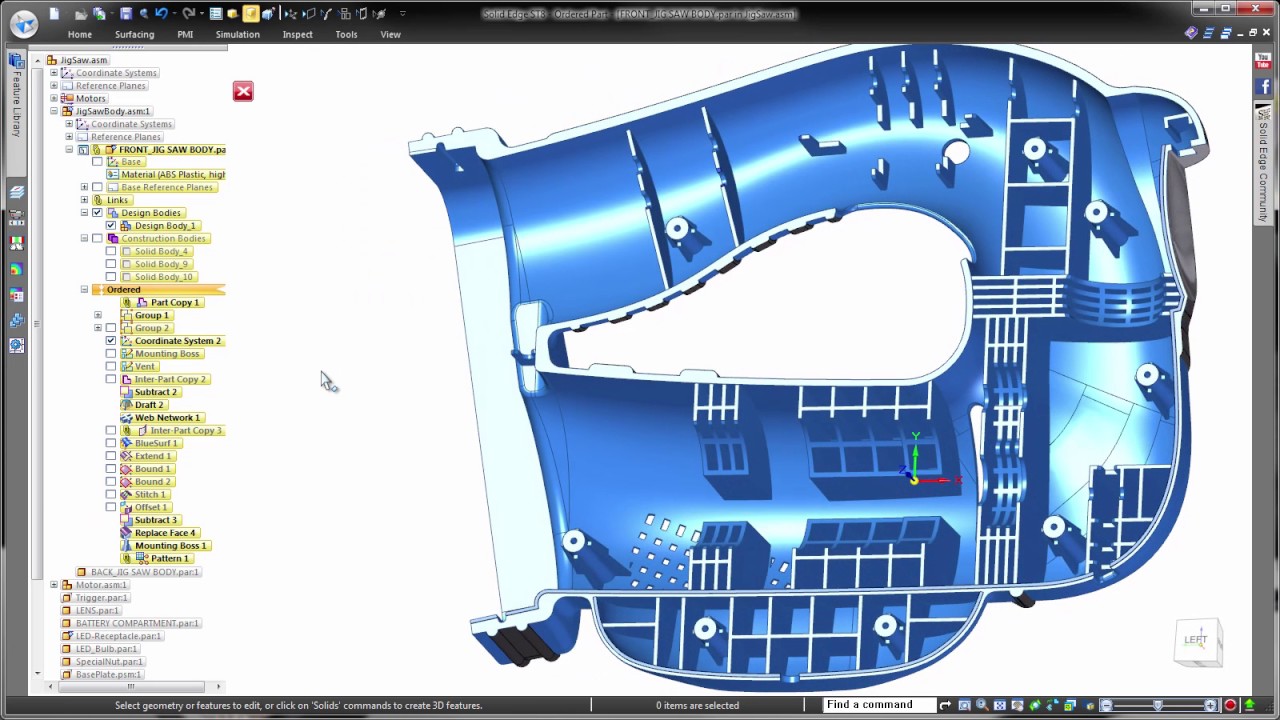
Tolerances and Stack-Ups in Designing Plastic Parts For Assembly
Stack-up analysis is non-negotiable. Every plastic part drifts during molding. Shrinkage varies by flow direction, especially with glass-filled grades. A PA66-GF30 part shrinks about 0.3 percent parallel to flow and 0.08 percent across flow. If your snap undercut is specified in the across-flow direction, you get nearly a 4x difference in dimensional stability compared to the flow direction. I always orient critical snap features parallel to flow when possible, and I call it out explicitly in the drawing notes so the mold maker knows which direction matters. Cumulative tolerance on an enclosure with five snapping features can easily add up to 0.5 mm or more in worst case. That means a snap that should engage cleanly might miss the receiving feature entirely if the parts land on opposite ends of their tolerance ranges. The fix is usually to design self-aligning features, such as conical lead-ins on pilot pins, and to put the loosest tolerances on secondary alignment features. Put the tightest tolerance on the primary locating feature and let the rest float.
Boss Design and Screw Threads
Heat-set inserts are the standard for durable threaded connections in plastic housings. You melt the seat into the plastic, press the insert in, and you get a metal thread that survives repeated mating. The common mistake is specifying a boss diameter that is too tight around the insert OD. If the boss is within 0.2 mm of the insert outer diameter, you risk cracking the plastic during installation, especially in brittle materials like GPPS. A clearance of 0.3 to 0.5 mm around the insert is usually safe. The boss should also have a downward-facing counterbore to support the insert head and prevent it from sinking through during torquing. For lower-volume or one-time assembly, tapped threads in the plastic itself work fine in nylon or acetal. Do not tap threads in polycarbonate unless you plan to never remove the screw. PC cracks under radial clamping stress from a tapped thread almost without exception. Acetal handles it well. Nylon is acceptable for moderate cycles. Anything brittle is a bad candidate. Wall thickness around screw bosses should be at least 1.5 times the screw diameter for torque resistance. A M3 screw in a 1.5 mm thick boss wall is risky. A 2.25 mm wall gives you margin for warpage and reduces the chance of the boss shearing off during assembly. I prefer specifying boss wall thickness as a separate dimension from the nominal part wall so the mold can thicken locally without changing the rest of the geometry.
Draft and Surface Finish
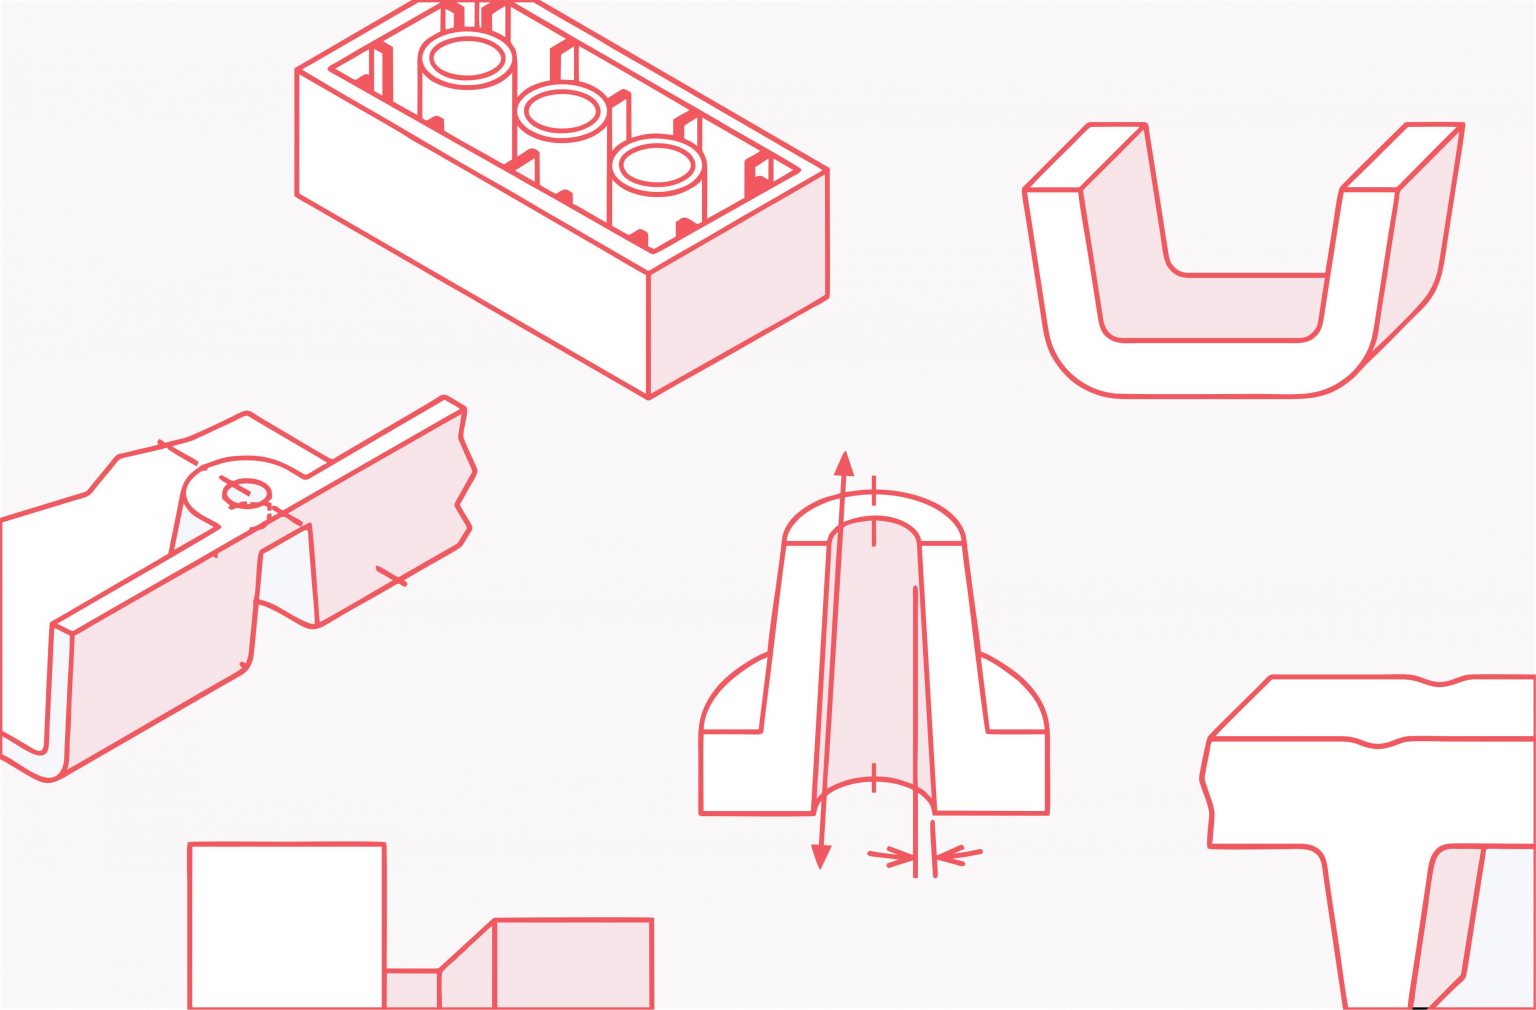
Draft is not optional. No draft means the part sticks in the mold, ejection forces increase, and surfaces scratch. Standard draft is about 1 degree per side for textured surfaces and 0.5 degrees for polished finishes. Textured surfaces grip the mold more aggressively, so you need more draft to pull free. If your part has deep ribs or gussets, add an extra 0.5 degrees on those features. Ribs also need thin walls. A rib that is thicker than 60 percent of the adjacent wall will sink and create visible deformation on the opposite surface. Keep ribs at 0.5 to 0.6 times the nominal wall thickness and terminate them with a radius, not a square corner, to reduce stress concentration. Ultrasonic weld joints require energy directors and shear joints designed specifically for the process. An energy director is a 60-degree triangular ridge, typically 0.5 to 0.8 mm tall, placed at the weld interface. It concentrates friction at a small contact area so the plastic melts quickly and uniformly. Without one, the weld takes longer, generates more flash, and often fails peel tests. Shear joints are another option where the lower part has a vertical surface that contacts the upper part first, melting from the bottom up. Shear joints produce cleaner welds with less flash but require tighter tolerances between the mating faces. If your part has large flat areas at the weld line, a shear joint is usually the better choice, assuming your mold can hold the tolerance. Amorphous plastics like PC, ABS, and PS weld better than semicrystalline plastics like nylon, POM, and PEEK. Semicrystalline materials absorb ultrasonic energy differently and often need modified joint designs or longer weld times. If you are choosing a material partly based on weldability, amorphous resins are easier to work with. If you must weld a semicrystalline part, consider adding a weld aid additive or switching to laser welding, which penetrates clearer materials and melts the joint more consistently.
Parting Lines and Flash Management
Flash at the parting line is inevitable in injection molding. The question is how much and where. Flash near a snap engagement surface or a weld joint can prevent proper closure or weaken the bond. I usually specify a parting line location away from functional features and add a small break-off allowance in the design, typically 0.1 to 0.2 mm of excess material that gets trimmed later. Automated trimming is fast and cheap for high volume. Manual trimming adds labor cost and inconsistency, so design around automation whenever possible. The enclosure I mentioned earlier had four snap features and two screw bosses. The snaps were designed correctly in the CAD model, with proper lead angles, undercut depth, and beam length. The issue was warpage. The molded parts bowed about 0.8 mm across the face due to uneven cooling and residual stress from the thick boss features next to thin walls. When I assembled the parts flat on the bench, the snaps misaligned by roughly 0.6 mm at the tips, which is enough to cause binding. The solution was not to change the snap geometry. It was to add locating pins with radial clearance on one side so the housing could float into alignment before the snaps engaged, and to redistribute rib thickness to reduce the warpage at the source. The revised parts assembled cleanly on the first try after the mold modification. Adding locating pins cost almost nothing in tooling. Redistributing wall thickness required a small change to the rib layout and a rerun of the molding cycle. The result saved about three weeks of debugging that would have happened on the production line. Some designs cannot be fixed with geometry alone. Thin-walled, large-area parts in amorphous materials warp predictably under thermal cycling. If your product ships from a warm warehouse to a cold car trunk and back, the dimensional shift can exceed your assembly tolerance by a significant amount. Polypropylene is particularly bad for this because of its high coefficient of thermal expansion. If your enclosure uses PP and has tight snap tolerances, you should expect seasonal fit issues unless you redesign for compliance or move to a material with lower expansion, such as a glass-filled nylon or acetal. No amount of tweaking snap angles will fix a material that expands and contracts enough to lose engagement.
Another scenario where plastic assembly design hits a wall is high-cycle latching under load. A snap that survives 500 cycles in a lab might fail at 200 in the field if the housing is under constant tension from a cable or a mounted component. Plastic relaxes under sustained strain. Over time, the retention force drops. If the application requires permanent, high-force retention, metal hinges or screw-fastened covers are the reliable choice. Snaps are fine for access panels that open occasionally. They are not fine for structural latches on heavy lids.
Material Selection Tradeoffs
Material choice affects everything: shrinkage, creep, weldability, chemical resistance, UV stability, and cost. Acetal is excellent for snaps and press fits because it has low moisture absorption and good fatigue resistance. It also has a low friction coefficient, which helps with sliding assembly. Nylon is strong and tough but absorbs water, which changes its dimensions and mechanical properties over time. If your part is used in a humid environment, design for the wet condition, not the dry one. A nylon snap that passes acceptance testing at 50 percent relative humidity may feel loose at 90 percent because the absorbed moisture plasticizes the material. Polycarbonate offers high impact resistance and clarity but tends to craze under solvent exposure and can stress-crack near sharp corners. Round all internal corners with a radius of at least 0.5 mm, preferably more. Stress concentration at sharp corners is where PC parts fail unpredictably in the field. ABS is a good all-around choice for consumer enclosures. It machines well, welds easily, and is inexpensive. It degrades under UV light, so outdoor use requires a stabilized grade or a paint/coating step.
Fast Validation Before Tooling
3D printed prototypes do not replicate injection-molded part behavior. FDM prints have anisotropic strength, different surface friction, and dimensional inaccuracies that make snap engagement testing misleading. SLA prints are closer in surface finish but still differ in material stiffness. The fastest reliable validation route is soft tooling, typically aluminum molds produced in a few weeks, or silicone molding for small batches. These methods give you injection-molded-quality parts in the right material at a reasonable cost. I recommend running at least 50 assemblies through the snap or press-fit features before approving hard tooling. It costs a fraction of a late change order and catches the issues that only appear after repeated mating cycles. If budget is tight and you must validate early, use CNC-machined parts in the actual production material for functional testing. They will not match molded surface finish or dimensional drift exactly, but they will reveal gross assembly issues like insufficient lead angle or interference that is too large. It is not a substitute for molded prototypes, but it is better than guessing.
Documentation That Actually Helps the Factory
Drawing notes matter more than most designers realize. Specifying the material grade, shrinkage factor, draft angles, critical tolerances, and preferred ejection side prevents the mold shop from making assumptions that ruin the assembly. Include a simple assembly diagram showing insertion direction, mating sequence, and expected force range if possible. Even a rough estimate like "insertion force approximately 15 N per snap" helps the assembly line engineer select the right tooling or fixture. I have seen multiple projects delayed because the factory assumed a different material shrinkage rate and the snaps were 0.3 mm too tight across all units. A single note on the drawing with the expected shrinkage range would have prevented it.