What Most People Miss About TPS Outside Of Manufacturing
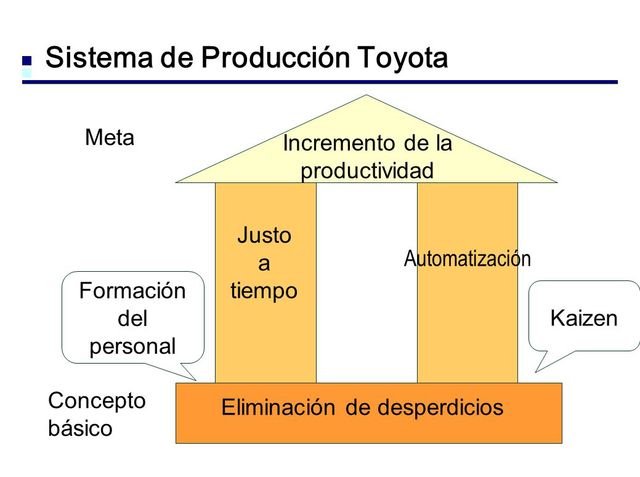
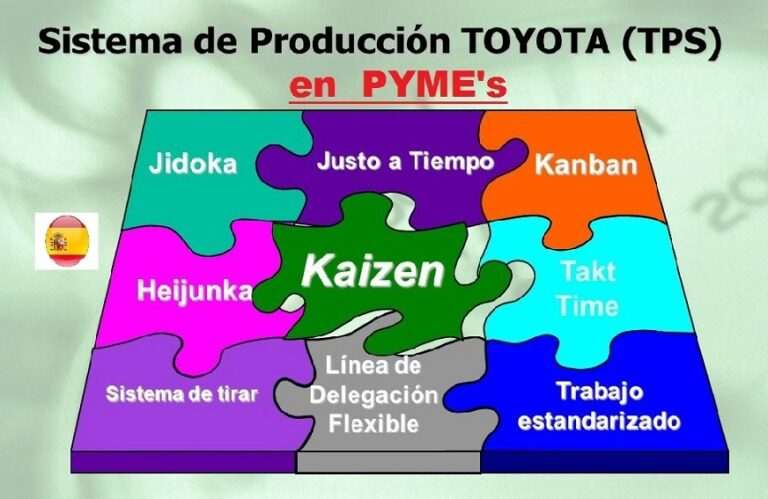
The Toyota Production System is not a methodology you can read about and implement next Tuesday. It is a decades-long accumulation of small corrections made by people who were genuinely frustrated with how work actually happened versus how it was supposed to happen. The original focus was vehicle assembly lines in post-war Japan, where resources were scarce and waste was a survival risk, not a management talking point. But the system extends well past the factory floor into service operations, healthcare, software, construction, and basically anything that involves a repeatable process with input, transformation, and output. I spent several years helping a mid-size logistics company try to adapt these principles to their warehouse operation. The standard TPS toolkit included just-in-time delivery, jidoka (automation with a human touch), andkaizen (continuous improvement), but none of that mattered until we stopped treating them as separate concepts and started treating them as a single interdependent system. That was the first counter-intuitive thing most teams miss: TPS components fail in isolation because they were never designed to work in isolation. The system only functions when all elements reinforce each other simultaneously.
El Sistema De Produccion Toyota Mas Alla De La Produccion A Gran Escala
Below is a practical breakdown of how the system translates outside of high-volume manufacturing, along with specific implementation steps and the things that tend to go wrong. Just-In-Time production is widely misunderstood as simply reducing inventory. It is not. It is about establishing a pull-based flow where each downstream step signals exactly what it needs, when it needs it, and in what quantity. In a manufacturing context this looks like kanban cards or electronic signal triggers. In a service context, like a hospital outpatient department I worked with briefly, it translates to patient appointment intervals being synchronized with room turnover times and staffing levels rather than scheduling patients into a static time grid that creates bottlenecks at the front desk. The practical implementation starts with mapping your value stream from raw input to finished output. You need to identify every step, measure cycle time at each node, and calculate the actual versus theoretical throughput. Most organizations find that only 5 to 15 percent of total process time is value-added work. The rest is waiting, transportation, over-processing, or correction. This number is not a goal to hit. It is a baseline measurement that tells you where to focus.
Jidoka in a non-manufacturing setting means building in the ability to detect abnormalities immediately and stop the process before a defect propagates. In software development this might look like automated test suites that halt a deployment pipeline the moment a regression is detected. In administrative work it means a checklist or validation rule that prevents a form from being submitted until critical fields are complete, rather than catching the error three days later during review. The principle is the same: catch problems at the source instead of catching them downstream where correction is expensive. Kaizen is the continuous improvement loop, but it is not about annual improvement initiatives or quarterly goal-setting sessions. It is about small, daily adjustments made by the people doing the work. One team I supported implemented a five-minute end-of-shift reflection where workers noted one thing that caused friction that day and one suggestion for fixing it. Within six months, they had compiled over four hundred micro-improvements that collectively reduced average order processing time from forty-seven minutes to twenty-two minutes. Most of these improvements were trivial in isolation. They were powerful because they accumulated without requiring budget approval or executive sponsorship.
Get the Full Details
A Specific Problem And The Workaround That Actually Worked
During my time with that logistics company, we hit a wall implementing andon-style visual signaling for their warehouse team. The problem was that the warehouse had three distinct shift patterns with different supervisory oversight levels, and the visual board system we set up was designed for a single shift with a consistent team. By the second week, the morning shift was updating the board correctly, the afternoon shift was partially ignoring it, and the night shift had stopped looking at it entirely. Defect rates started climbing again within a month because the signal-to-stop mechanism was inconsistent across shifts. The workaround was to replace the single visual board with a shift-specific digital ticketing system that auto-escalated issues based on severity and time elapsed. Instead of one board everyone checked at different levels of engagement, each shift had a streamlined interface showing only issues relevant to their operating parameters. We also reduced the escalation threshold from thirty minutes to ten minutes for critical defects. This brought consistency back across shifts without adding management overhead. It also revealed that the real problem was not worker engagement but a design that assumed uniform operating conditions that did not exist on the floor.
Implementation Steps That Do Not Require A Complete Overhaul
You do not need to transform an entire organization to start applying TPS principles. Begin with a single value stream that is clearly defined and has measurable outputs. A single product line, a single service workflow, or a single departmental process is sufficient. Map the current state, identify the largest source of waste, and address it before moving to the next constraint. Do not try to optimize multiple streams simultaneously. That is how projects stall and get abandoned. Standardize work before attempting to improve it. This sounds contradictory to kaizen philosophy but it is not. You cannot identify meaningful variation if there is no documented standard to compare against. Create a basic work instruction document for the process you are studying. It does not need to be exhaustive. It needs to capture the current best-known method so that improvements can be measured against a consistent baseline rather than against whatever each person does differently. Build feedback loops that close within hours, not weeks. TPS thrives on rapid feedback because problems are cheapest to fix when they are fresh. A weekly report on defect rates is too late. A daily dashboard updated in real time or near real time is more useful. An immediate stop-the-line signal is ideal but not always feasible outside of physical production environments. Even a simple shared document that flags issues as they occur and gets reviewed the same business day is a significant improvement over monthly reporting cycles.
Where TPS Actually Fails And What To Do Instead
TPS assumes a level of process stability and repeatability that simply does not exist in creative or exploratory work. Software architecture design, product strategy, research and development, and any work where the output is genuinely novel cannot be optimized using lean manufacturing principles without stripping the work of the very flexibility that makes it valuable. Trying to apply kanban systems and takt time calculations to a research team is a reliable way to destroy innovation velocity while creating the illusion of productivity. The system also struggles in environments with highly variable demand where pull-based production would require either excessive capacity buffering or frequent process disruptions. A custom furniture maker handling unique orders for each client will find JIT principles frustrating because every order is essentially a different product with different material sourcing, tooling requirements, and labor skills. In these cases, a hybrid approach that borrows lean thinking for the repetitive elements (material procurement, finishing processes, quality inspection) while allowing flexibility for the variable elements is more effective than a pure TPS implementation. Another significant limitation is the cultural requirement. TPS depends on a workforce that feels empowered to stop production and that trusts the system will not punish them for surfacing problems. In organizations with punitive management cultures, blame-oriented performance reviews, or high turnover rates, the system will not function regardless of how well you implement the tools. Workers will hide defects rather than signal them. They will follow standards mechanically without engaging in kaizen. The tools will look correct on paper while the underlying behavior remains unchanged. In these situations, addressing organizational culture and leadership behavior is a prerequisite, not an optional enhancement.

Measuring Whether It Is Actually Working
The most reliable indicators are lead time reduction, first-pass yield improvement, and inventory or work-in-process reduction on the specific value stream you are targeting. If your lead times are not decreasing within the first ninety days of focused implementation, something is wrong with the approach or the baseline measurement. Cycle time variability should also decrease as standardization improves. If average cycle time stays the same but variability increases, you are likely optimizing for throughput at the expense of flow consistency, which is a common mistake. Employee engagement metrics tied to kaizen participation are another useful signal. If fewer than five percent of frontline workers are submitting improvement suggestions after three months of implementation, the system is being treated as a management initiative rather than a worker-driven practice. This is not a failure of TPS. It is a failure of the implementation approach that is actually quite common. The system was never designed as a plug-and-play solution. It was designed as a learning system, a way of thinking about work that evolves as conditions change. The principles are stable. The applications are not. Understanding that distinction makes the difference between a brief implementation that produces temporary results and a sustained practice that adapts to whatever comes next.