What Deposition Actually Means In A Lab Context
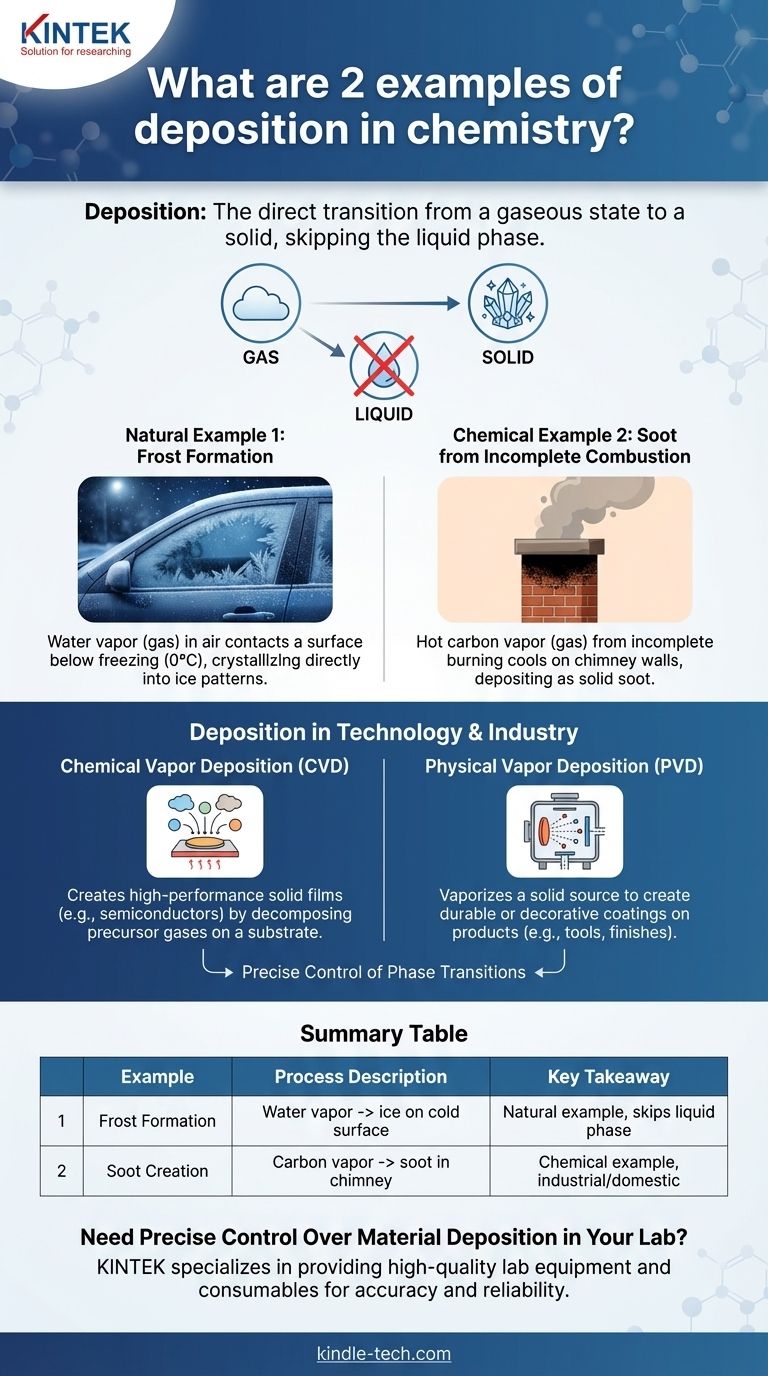
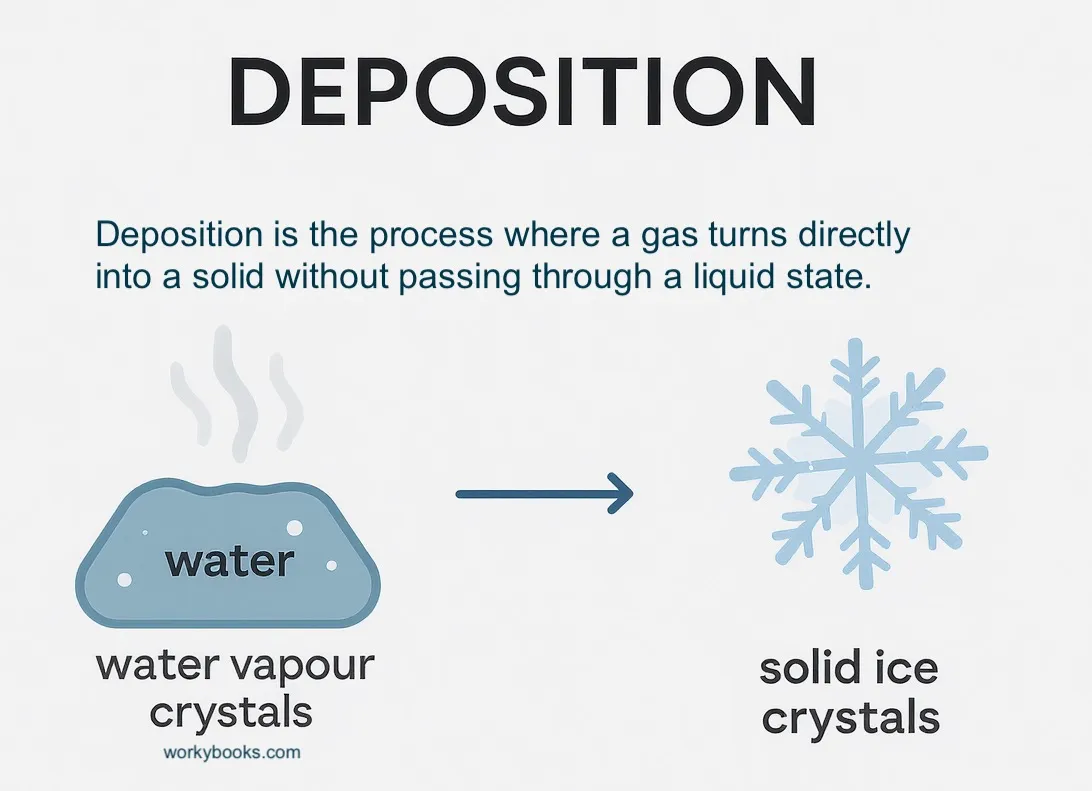
Deposition refers to the process where a substance transitions directly from a gas or vapor phase into a solid phase, skipping the liquid stage entirely. It is also used more broadly in materials science to describe any technique where thin layers of material are deliberately laid down onto a substrate surface. The word shows up in atmospheric physics, semiconductor manufacturing, chemistry education, and geology, which means you will find conflicting definitions depending on which circle you are in. I learned this the hard way when I started cross-referencing papers from different fields and kept getting confused about whether someone was describing frost formation or sputter coating. The phase-change definition is the strictest one. Water vapor turning into ice crystals on a cold window is textbook deposition. Carbon dioxide gas becoming dry ice at standard pressure is another clean example. These are spontaneous processes driven by temperature and pressure conditions, not engineered ones. The applied-materials definition is where most lab work happens, and it is what you will encounter if you are dealing with Examples Of Deposition In Science courses or research groups that work with thin films.
Examples Of Deposition In Science
Here is the thing about thin-film deposition that nobody tells beginners: the choice of method depends almost entirely on what you need the film to do, not on what equipment your lab already owns. I used to assume that thermal evaporation was sufficient for most basic coatings because it is simpler and cheaper. I was wrong. Thermal evaporation produces films with lower density and poorer step coverage compared to sputtering or chemical vapor deposition. If you are building a device that requires conformal coating on a patterned substrate, thermal evaporation will leave you with gaps and weak adhesion points that you will not notice until your device fails during testing. Sputter deposition uses a plasma to knock atoms off a target material, which then land on the substrate. It gives you good control over film thickness, usually in the range of nanometers to a few micrometers, and the films tend to be denser. Chemical vapor deposition introduces precursor gases that react or decompose on the substrate surface. This method can produce extremely uniform films even on complex geometries, which is why it dominates the semiconductor industry. Atomic layer deposition takes things further by using self-limiting surface reactions in alternating pulses. One pulse of precursor A, a purge, one pulse of precursor B, a purge, repeat. Each cycle adds roughly one angstrom of material. You get near-perfect thickness control and exceptional conformity, but the process is slow. Growing a 100 nanometer film by ALD can take several hours depending on your cycle time and reactor design. Let me give you a specific problem I ran into. I was doing PLD, pulsed laser deposition, to grow thin oxide films for a project on resistive switching memory devices. The substrate was patterned silicon with trenches about two hundred nanometers deep and five hundred nanometers wide. My first batch of films showed severe gap filling defects inside the trenches. The laser plume was too directional and the adatoms did not have enough surface mobility to reach the bottom of the features before the film bridged over the top. I solved it by heating the substrate to four hundred Celsius during deposition, which increased surface diffusion enough for the material to flow into the trenches properly, and I also tilted the substrate holder by thirty degrees so the plume hit at an oblique angle rather than straight down. The second run had acceptable fill factors. It cost me about a day of setup and characterization, but it saved me from scrapping three weeks of growth time.
Common Deposition Techniques And When To Use Them
Physical vapor deposition covers evaporation, sputtering, and laser ablation. These are all line-of-sight processes to varying degrees, meaning the deposited material travels in relatively straight paths from source to substrate. Shadowing effects are real and they matter. If your substrate has topography, features on the far side of a step will receive less material. This is not a defect in the technique, it is a fundamental constraint you have to design around. Chemical vapor deposition is not line-of-sight. The precursor molecules diffuse to the surface and react there, which allows coating of recessed areas and even interior surfaces of complex structures. The tradeoff is that you need precursors that are volatile enough to transport safely and reactive enough to deposit at practical temperatures. Some precursors are pyrophoric or toxic. I once had to replace a TMGa supply because the bubbler had been slightly overheated and the purity dropped below spec. The resulting GaN layer had unacceptable dislocation densities and the LEDs were practically useless. Checking precursor storage temperatures and tracking batch certificates is something you do once and then never think about again, right up until the moment your data is garbage. Electrochemical deposition, also called electrodeposition, is relevant when you are working with metals or conductive polymers in solution. It is inexpensive, scales well, and can deposit thick layers quickly. The catch is that it only works on conductive substrates and the film quality depends heavily on electrolyte composition, current density, pH, and temperature. A fluctuation of five degrees Celsius in your bath temperature can change your deposition rate by ten to fifteen percent. If you are doing precision work, you need a properly controlled bath, not just a hot plate and a stir bar.
Get the Full Details
Practical Pitfalls That Waste Time
Substrate cleaning is where most people cut corners and then blame their deposition results. I have seen people load substrates that were rinsed with deionized water and dried with nitrogen, then wonder why their films delaminate. A proper cleaning sequence usually involves solvent degreasing, acid or base treatment, and a final rinse followed by immediate loading into the deposition chamber or storage in a desiccator. If your chamber base pressure is above one times ten to the minus six torr, you are depositing onto a contaminated surface regardless of how clean your substrate was beforehand. Pump-down time matters. A well-maintained turbomolecular pump with a proper cold trap can reach high vacuum in twenty to forty minutes depending on chamber volume. An older system with degraded seals might take an hour or more and still never reach the same base pressure. Deposition rate monitoring is another area where people make assumptions. Quartz crystal microbalances are convenient but they measure mass per unit area at a specific point in the chamber. If your deposition is not uniform across the substrate, the QCM reading might be accurate locally but misleading globally. I learned this when depositing gold films for surface plasmon resonance experiments. The QCM read three nanometers, but ellipsometry measurements across the wafer showed a variation from two to four nanometers. I switched to using in situ optical monitoring for subsequent runs, which tracked the interference fringes in real time and gave me a much clearer picture of actual thickness distribution. Adhesion promoters are not optional when you are working with dissimilar material pairs. A thin chromium or titanium adhesion layer between silicon and gold can mean the difference between a film that peels off during sample handling and one that stays put. Two nanometers of chromium is usually sufficient. More than five nanometers and you start affecting the electrical or optical properties of your overlayer in ways that may not be desirable. It is a balancing act that requires you to know what your final device needs to do.
A Note On Limitations
No single deposition method is universally superior. Sputtering gives good density but can cause substrate damage from ion bombardment if you are not careful with the plasma conditions. CVD produces excellent conformality but often requires high temperatures that are incompatible with many substrate materials. ALD gives unmatched thickness control but is prohibitively slow for high-volume production of thick films. Plasma-enhanced CVD lowers the processing temperature compared to thermal CVD but introduces potential hydrogen incorporation and plasma damage that you need to characterize out. Your choice should be driven by the specific requirements of your application, not by convenience or what your advisor prefers. If you are new to this, start with a technique that matches your available equipment and your material system, characterize everything you produce, and keep detailed logs. The difference between a successful deposition run and a frustrating one is often a parameter that was changed without being recorded. I still have notebooks from my graduate work that document things like rough pump-down curves and anomalous discharge behavior in my sputter tool, information that would have saved me significant time if I had kept better records earlier in my career.