Flex Pcb Design Guide
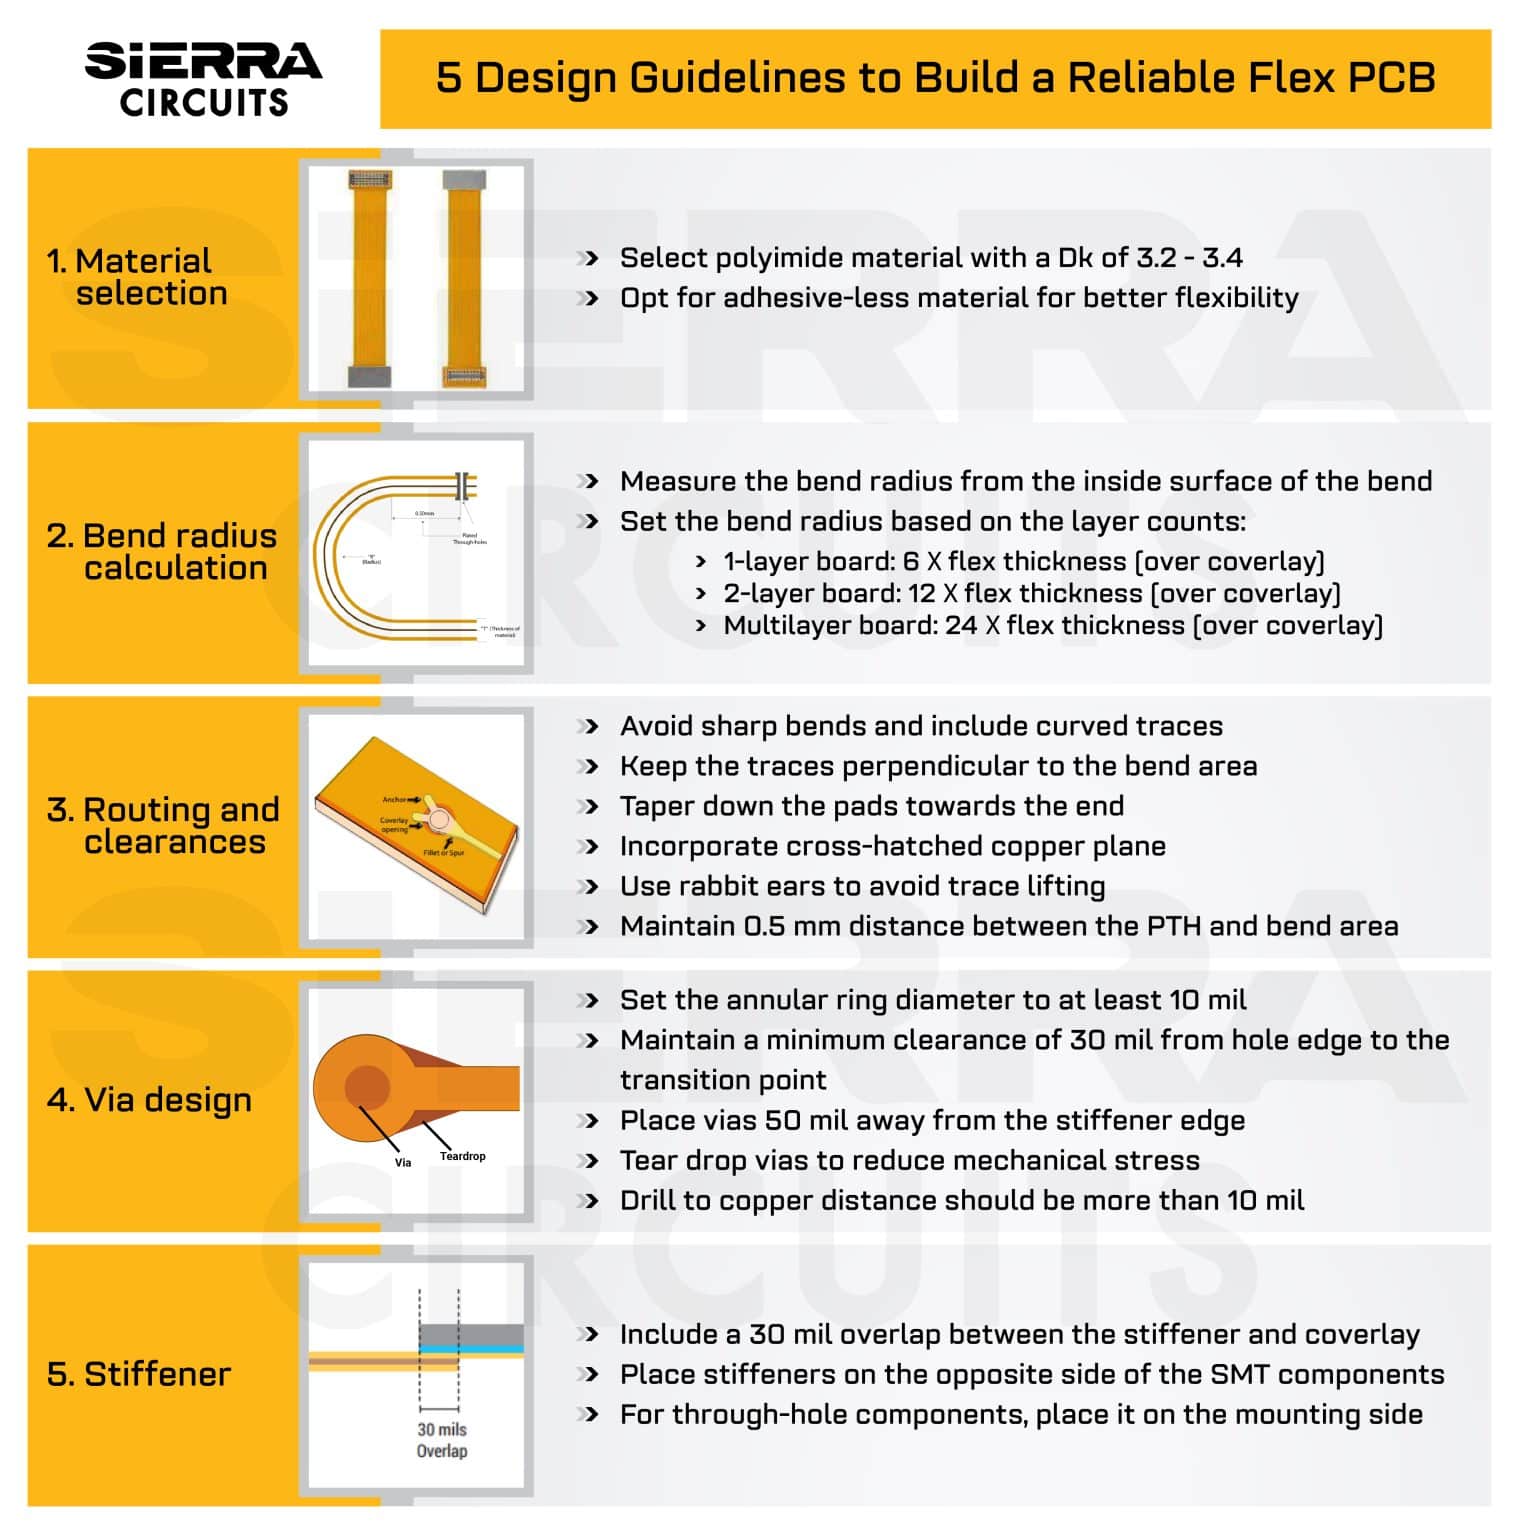
The first time I properly designed a flex circuit, I learned pretty fast that the bending radius isn't just a textbook number. I had a project where the trace width needed to stay under 4 mil for impedance matching, and the bend area kept failing after 500 cycles. The standard rule about keeping the inner radius at least 3x the copper thickness worked on paper but fell apart in production. My workaround ended up being adding an arch-shaped copper pour near the bend with gradually widening traces, which distributed the strain over a larger area without breaking the signal path. If you're starting out with flexible circuit boards, there's a decent entry point called Flex Pcb Design Guide that covers the basics. It walks through material selection, the difference between single-sided and double-sided flex, and how to calculate bend zones. The guide is useful but it doesn't really drill into the messy stuff that happens when you're dealing with stiffeners or multi-layer builds. You'll find more practical value once you've made a few mistakes yourself.
Choosing the Right Substrate and Copper
You've got a few options when it comes to the base material. Polyimide is the standard choice for most applications because it handles heat well and stays flexible across a broad temperature range. PET is cheaper but only good for low-temperature processes and minimal flexing. If your design needs to survive repeated bending, stick with polyimide and don't cut corners on the copper weight. The usual options are 1/2 oz, 1 oz, or 2 oz copper. For flexible sections that will actually move, 1/2 oz copper gives you better fatigue resistance. Heavy copper cracks faster when bent repeatedly. One thing most guides don't emphasize enough is how the dielectric constant changes when the board bends. A substrate that measures 3.5 at rest might shift to 3.8 or higher once it's under tension. This affects impedance calculations, especially for high-speed signals. You can compensate by adjusting trace width slightly in the bend zone, but the effect is small enough that you often don't need to worry unless you're running signals above a few hundred megahertz.
Routing Traces in Bend Zones
The key rule here is that copper traces should run perpendicular to the bend direction. Parallel traces get stretched and compressed as the board flexes, which leads to cracking. I once had a design where the signal traces ran along the bend axis and failed after about 200 cycles. Switching them to run across the bend direction instead extended the life to over 5,000 cycles. It's a simple change but one that makes a huge difference in real-world durability. Another detail worth noting is how to handle vias in flex areas. Vias tend to crack when they're in the bend zone because the plating doesn't flex the same way as the copper. The workaround is to avoid placing vias in high-strain areas entirely. If you must route through a layer change, position the via in the flat section away from the bend. Some designers use filled vias to reduce the risk, but the simplest solution is just to keep vias out of moving areas.
Get the Full Details
Stiffeners and Layer Stacking
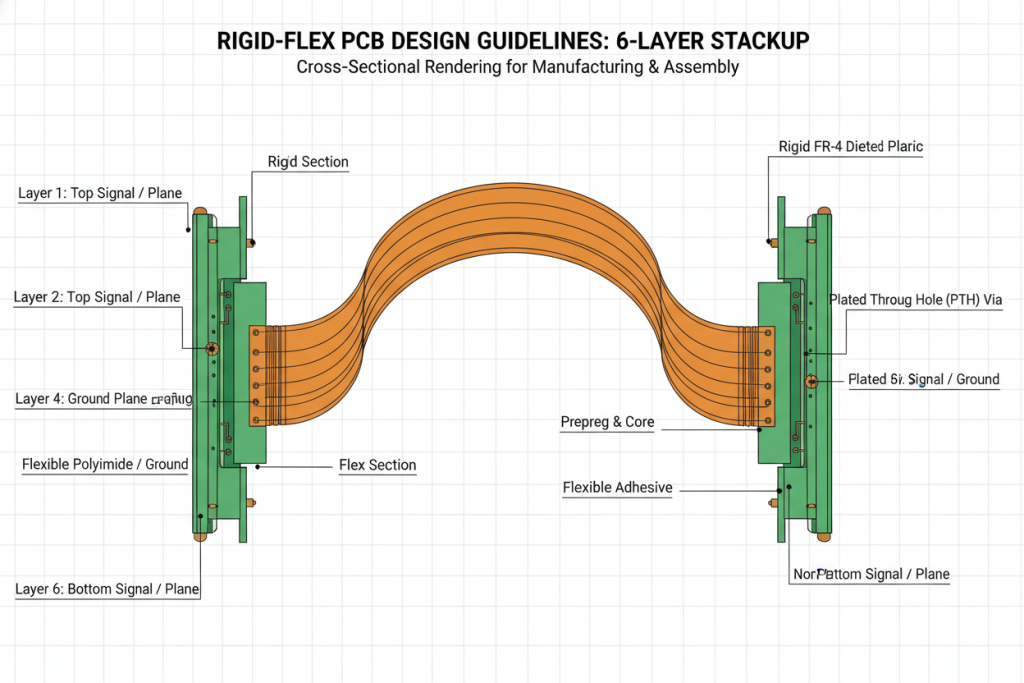
Stiffeners add rigidity to specific areas of the flex circuit. Common materials include FR-4, polyimide, and metal. The choice depends on how much rigidity you need and whether the area will be exposed to heat during soldering. FR-4 stiffeners can withstand reflow temperatures but add bulk. Polyimide stiffeners are thinner and more flexible but may not handle high heat as well. Mutli-layer flex builds introduce additional complexity. Each layer needs to align properly during lamination, and the expansion rates of different materials can cause warping. I found that using a gradual taper when transitioning from rigid to flex sections reduces stress concentrations. The process takes longer than a simple single-layer design but the reliability improvement is worth the extra time.
Common Pitfalls and Limitations
One misconception about flex PCBs is that they're universally better than rigid boards. They aren't. Flex circuits cost more, take longer to manufacture, and require special handling during assembly. If your design doesn't need to bend or fold, a rigid board is cheaper and simpler. The trade-off becomes worth it only when space constraints or mechanical movement demand flexibility. Another limitation is the minimum trace width and spacing. While flex boards can support finer features than rigid boards in some cases, the manufacturing tolerance is tighter. Most fabricators can achieve 4 mil traces with 4 mil spacing, but going smaller increases cost significantly and may not improve performance. For most designs, 4 to 6 mil features strike a good balance between capability and price.
Testing and Validation
Before committing to full production, test your flex design through a few bend cycles. A simple test fixture with a programmed bending motion can simulate years of use in a few hours. I usually run 1,000 cycles at the specified radius and check for continuity breaks or impedance shifts. The test takes about 2 hours on a basic setup but catches most failures before they reach the field. Impedance testing on flex boards requires special care because the bending changes the effective dielectric constant. Time-domain reflectometry can help identify discontinuities, but the measurement setup needs to account for the board's curvature. A flat test coupon gives a baseline reading, while the bent configuration shows how the signal behaves in actual use.

When Flex Pcb Design Guide Falls Short
The standard Flex Pcb Design Guide provides a solid foundation but doesn't cover every edge case you'll encounter. Real-world designs often involve combinations of rigid and flex sections, mixed materials, and tight space constraints that require creative solutions. The guide is a good starting point but you'll develop true expertise through hands-on experience and learning from failures. My recommendation is to build a prototype with a small batch and test it thoroughly before scaling up. The upfront cost of prototyping pays off by catching design issues early. A failed production run due to untested flex design can cost ten times more than a proper prototype cycle.