The Actual Process
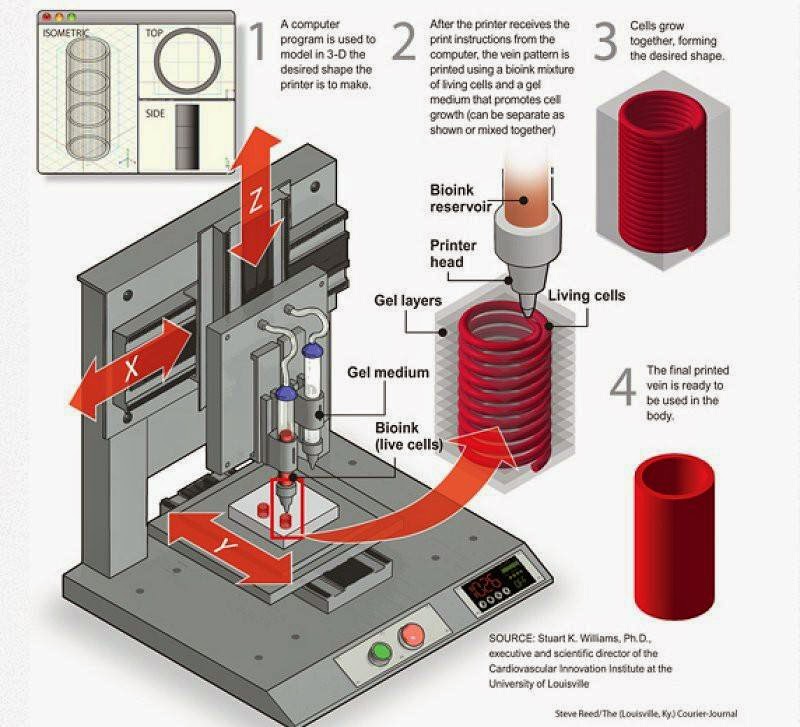
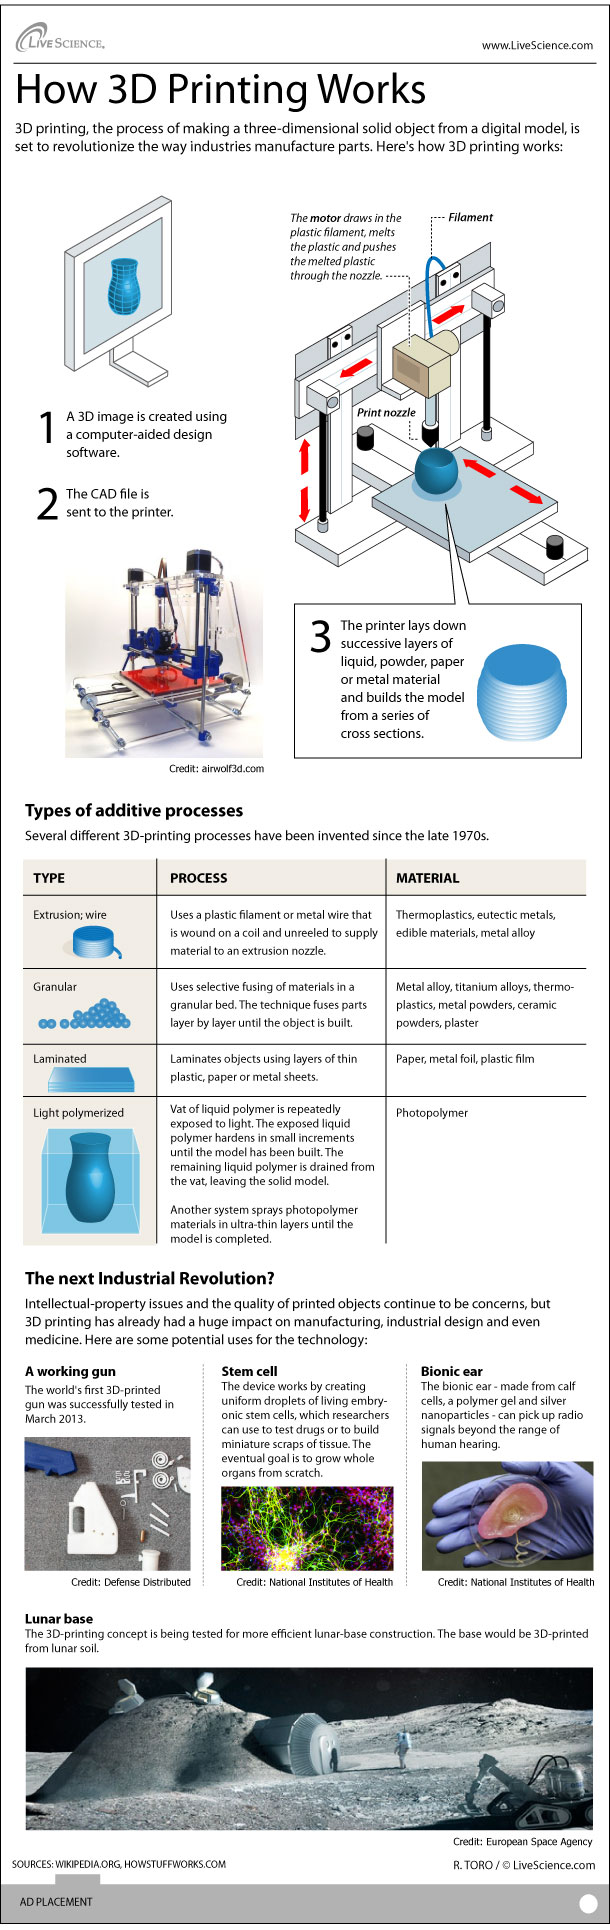
3D printing builds objects layer by layer from a digital model. There are several methods, but the two you will actually run into are FDM (fused deposition modeling) and SLA (stereolithography). They operate on completely different principles, and choosing between them matters more than most people realize. FDM works by melting a thermoplastic filament and extruding it through a heated nozzle. The printer moves the nozzle in X and Y, while the build plate moves on Z. Each layer bonds to the one below it as the plastic cools. A typical hobby FDM printer uses PLA or PETG, runs between 190 and 240 degrees Celsius at the nozzle, and deposits layers anywhere from 0.1 to 0.3 millimeters thick. That 0.2 mm layer height is the default for a reason: it balances speed and surface quality without requiring calibration you probably do not have time for.
How Does 3D Printing Work
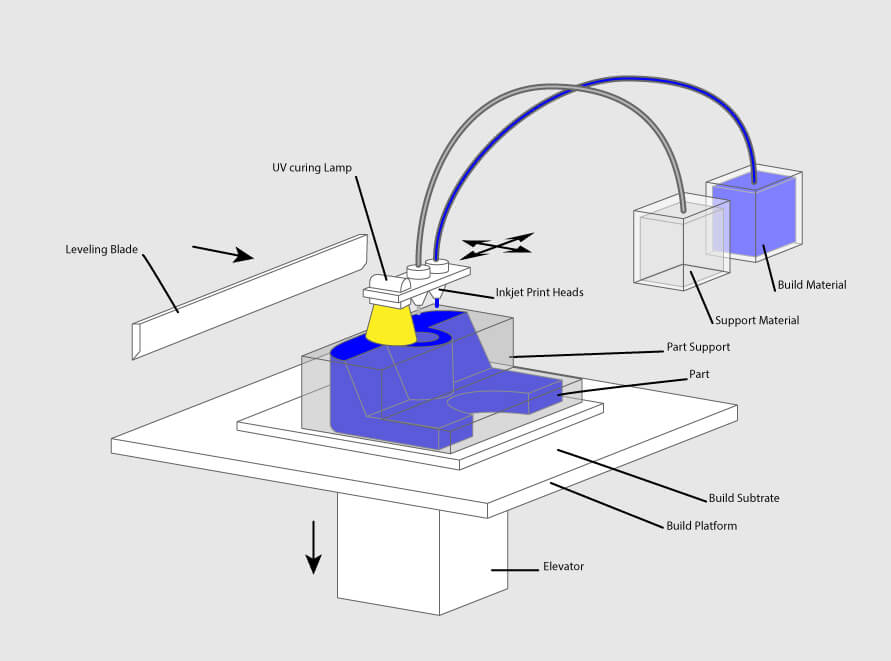
SLA does the opposite of melting. It uses a UV laser or a projected light source to cure liquid photopolymer resin into solid plastic. The resin tank sits below the build plate, and each layer is pulled from the surface of the liquid. This produces significantly finer detail because the resin does not have the same flow characteristics as extruded filament. You get smoother walls, sharper text, and less visible layer lines. The tradeoff is that resin is toxic, smells bad, requires ventilation, and the parts are brittle compared to printed thermoplastics. If you are printing miniatures or jewelry castables, SLA is the right tool. If you are making functional brackets or enclosures, it is not. The slicing software is where the digital file becomes machine instructions. You take an STL or OBJ file and import it into a slicer like PrusaSlicer, OrcaSlicer, or Cura. The slicer calculates toolpaths, infill patterns, support structures, and print parameters for each layer. It outputs G-code, which is the language every FDM printer understands. The G-code tells the stepper motors exactly where to move, how fast, and how much filament to push through the hotend at every point. I used to think support generation was something you could ignore. That changed when I printed a 60-millimeter cantilevered drone arm with a 45-degree overhang and zero supports. The result was a stringy hammock of PLA that looked like a failed spiderweb project. I learned that anything over roughly 45 degrees needs support material, and the slicer can generate tree supports or standard brick supports. Tree supports use less filament and are easier to remove, but they only work well on resin printers. For FDM, regular supports are usually fine, and you should set the Z-distance offset to 0.2 mm above the layer so the support does not fuse to the part surface.
What Actually Goes Wrong
The first failure mode everyone encounters is poor bed adhesion. If the first layer does not stick, the print detaches and curls into a ball. The fix is usually mechanical rather than software-based. You need a flat build surface, and the nozzle height at the bed level has to be correct. The paper trick still works: slide a sheet of printer paper between the nozzle and the bed, lower the bed until you feel slight resistance on the paper, then start printing. If you have an auto-leveling probe, run it and verify the mesh by printing a single-layer 40-millimeter calibration square. Check the corners and the center. If the corners look thin or stringy, your Z-offset is off. Stringing and oozing happens when the hotend leaks filament during travel moves. This is controlled by retraction settings. On a direct-drive extruder, you might need 4 to 6 mm of retraction at 25 to 45 mm/s. On an Bowden setup, you need more distance, usually 5 to 7 mm, because the flexible PTFE tube compresses and delays the retraction response. If you are seeing goosebumps on vertical surfaces, your temperature is too high for the material. Drop it by 5 to 10 degrees and watch what happens on the next print. Warping is the problem that ruins prints without warning. It happens when the bottom layers cool unevenly and shrink, pulling away from the bed. ABS warps badly. PLA barely warps under normal conditions. If you print ABS, you need an enclosed chamber and a heated bed at around 100 degrees. A brim in the slicer helps by increasing the contact area with the build plate. I once printed a 120-millimeter ABS gear housing on an open-frame printer with no enclosure and a bed temperature of 90 degrees. The bottom three layers peeled up within the first hour, and the entire print warped into a shallow bowl shape that was unusable. I switched to PETG the next day and had it finished in under two hours with perfect flatness.
Get the Full Details
Calibration Is Not Optional
Every printer needs an E-steps calibration at minimum. This tells the firmware how many stepper motor steps are required to extrude exactly one millimeter of filament. If your E-steps are off by even a few percent, your prints will have consistent under-extrusion or over-extrusion, and you will waste material chasing a software problem that is actually mechanical. Measure 120 mm of filament marked with a pen, command the printer to extrude 100 mm, and measure what remains. If 30 mm remains, your E-steps are correct. If 28 mm remains, your steps are too low. Adjust the value using the formula: new_E_steps = current_E_steps × (expected_length / actual_length). Flow rate calibration is the next step. Print a calibration cube at 100 percent flow, then at 95, 90, and 85 percent. Measure the wall thickness with calipers and compare to the theoretical value. The setting that gives you the closest match is your optimal flow rate. This matters because slicers assume perfect extrusion by default, and no printer achieves that out of the box. I typically run my main printer at about 95 percent flow, which eliminates the need for infinite inset perimeters and keeps dimensional accuracy tight.
When to Use What
FDM is the workhorse. It is fast enough for prototypes, strong enough for functional parts in PLA and PETG, and the materials are inexpensive. A spool of PLA runs about fifteen dollars. A cubic inch of resin runs about twenty-five dollars, and you need a lot more resin to get the same volume of material because of the waste from vat walls and failed prints. Factor in post-processing time for resin prints as well: you need an isopropyl alcohol wash, a UV cure station, and disposal procedures for leftover resin. That is not free. SLA wins on detail. If you need sub-0.1 mm resolution, if you are printing minisatures, dental models, or investment casting patterns, resin is the only option that makes sense. FDM simply cannot reproduce fine surfaces at that scale without extreme patience and expensive hardware like micro-nozzles. For high-strength production parts, neither FDM nor SLA is ideal. Injection molding or CNC machining is what the industry uses, and the per-unit cost drops dramatically once you pass roughly two hundred parts. 3D printing competes on speed and customization, not on bulk economics. If you need five identical brackets tomorrow, print them. If you need five thousand, do not bother.
The technology keeps improving, but the fundamentals have not changed in fifteen years. You have a digital file, you slice it into layers, the machine lays down material one layer at a time, and you hope the physical result matches the simulation. Most of the skill is in understanding why the result diverges from the plan and fixing the root cause rather than spinning dials randomly. That is the difference between someone who prints and someone who prints well.